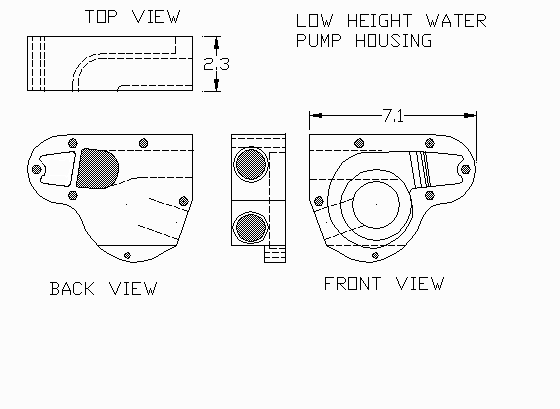
This is a low height version of the stock pump in the stock
location. I will incorporate Jeff's and Paul Yaw's improvements when
I have more info. Some hand smoothing and porting will be required using
a hand grinder and a burr. Tubes can be welded in using the
hose connecting method of your choice. A slight counter bore
where the tubes would be welded in would help locate them.

The passage holes are 1.25 inches in diameter which is equal to
or better than the stock pump housing. Particularly on the return
hot water flow out of the block to the rad. The return flow passage
area benefits greatly from the elimination of the bypass passage.

The dimensions are rough and the stock cartridge should be used to locate
the mounting holes. There is a large chamfer where the impeller meets
the housing. My suggesting is make a cutting tool out of an old
stock Mazda impeller to cut this chamfer.

Templates  can be made from Lexan to help with the shape of the
scroll and bolt mounting locations using the stock housing as
a pattern.

I kept this simple so it could be made by hand on a simple mill.
6061 T6 is the preferred material. Anodizing would be nice after it
was welded to keep down corrosion.

All this becomes much clearer if you disassemble a stock pump.

If anybody wants to make one make one for me too.

Paul Lamar

The Aircraft Rotary Engine Newsletter.              Powered by Linux.

http://home.earthlink.net/~rotaryeng/            http://www.linux.org