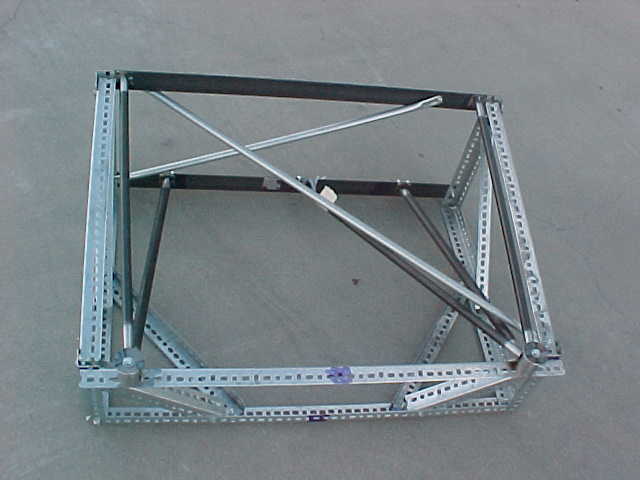
My first design (first gif) has proven to be less than ideal.
The problem is I can't get my head far enough inside to see
the weld with my bi-focal glasses  due to the size of
the welding helmet and the diagonal braces. I can weld some
of it but I will have to take the motor mount out of the jig
to finish welding it.

Here is my suggestion for model two. Make a sketch and take it
to your local welder and have him cut it out and welded up.
Lot easier for him as he probably has a cutting torch
and an iron worker.

This is an inside out jig. The six inch
diameter steel tube is torsionally rigid so the 2 inch by 2
inch by 1/8 angle are held in the right positions.
Then the firewall and rubber motor mount 4130 steel brackets are
bolted to the ends of the angles. This way there is plenty
of room around them for welding the 4130 motor mount tubes.

A true universal design would have telescoping tubing so the
length could be adjusted for any position of the rubber
motor mounts on the engine.

Paul Lamar
The 6" tube is fine, but I'd bet a chunk of change that the end
brackets are flexible enough that your mount will move enough
to make it hard or impossible to reassemble after welding.
This stuff will move a LOT.  Getting .060" movement  or more
is common.  Either weld in place or drill in the mounting holes
after welding is all done.  Even heating of the whole mount
helps a bit, but these things just *move*.  Can be pretty frustrating.
Exhaust systems do it, too.   Pain the butt.  I have given up
and do all final welding *tightly* bolted in place.  Even then,
my exhaust needs to be tapped on and off of the studs.  It fit
perfectly before the final welding.

Bill
Long EZ builder & pilot
mechanical engineer
You could go up on the thickness of the angle or use channel instead.
My box jig or fixture did not work out as it was too hard to weld the joints.
This is what I wound up with. I had to cut my fixture down so I could get
to the joints for welding. Are you using tig Bill? Tig is supposed to use
less heat. BTW as you tack weld in the tubes the fixture gets more rigid.

Jerry Hey's suggestion of putting the grinder or belt sander right next
the fixture is right on and extremely important. I must have ground or sanded
on the ends of those tubes two to three dozen times. Thanks Jerry.

Paul Lamar

The AirCraft Rotary Engine NewsLetter.              Powered by Linux.

http://home.earthlink.net/~rotaryeng/            http://www.linux.org