7075 T6 would be ideal if you can find it in bar stock about
2-1/2
inches in diameter. The center should be .375 " thick  flat out
to a
diameter of about one inch with the afore mentioned hole of .635
(5/8").
>From there out, taper it down to .125 thick at the edges.

6061 T6 bar stock would also work fine. Probably a bit cheaper
than
7075 T6.

An NC late could whack out a 100 or more of these per hour.
Anodizing would be nice.
Paul Lamar
Ken Powell wrote:
Paul,
In the msg above you suggested making the motor mount snubbing
washers from 0.375 6061-t6 aluminum.  Is it acceptable to cut a
washer out of 0.25 6061 and another out of .125 6061-t6, then
stack them together for the 0.375 thickness.
Sure that should work.
The reason I am
asking is that I have some .25 and some .125 6061-t6 plate to
make these out of, but would have to order the .375.

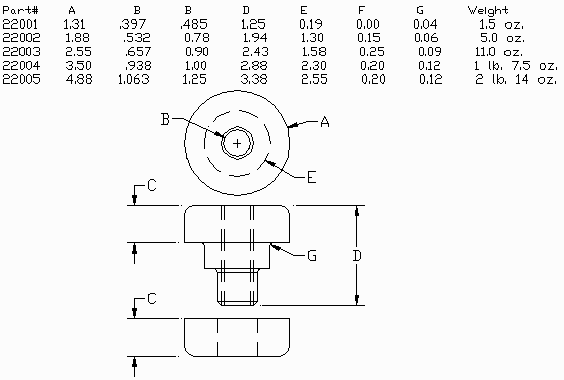
Also, did we decide earlier that the Barry mount 22002-15 is the
preferred motor mount?

Thanks,
Ken Powell
The load rating on the Barry 22002-15 is 630 pounds. A bit over kill.
Are your mounts near the CG of the engine? Do you have a sketch?
I will be using something softer on the Kis like 22002-12 175 pound
load rating with a half inch thick plate.

BTW the above message assumed the 22003 which has a 5/8 hole.
the 22002 has only a 1/2 inch hole. I think you can make them out
of two pieces of the 1/8 inch thick 6061 T6 in that case. A small one
and a two inch diameter large one.

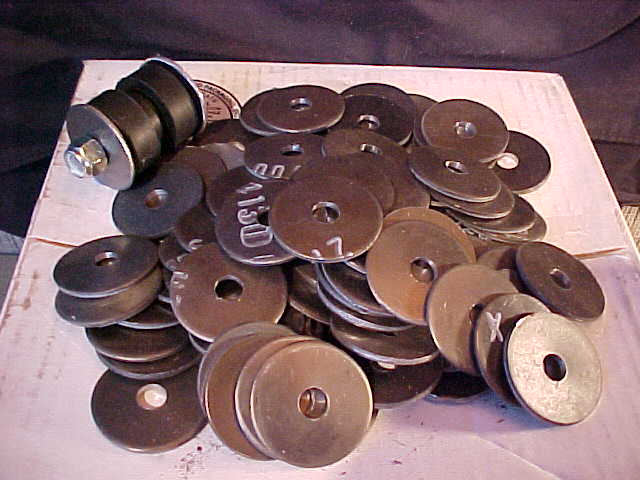
I have a bunch of these washers punched out of .096 thick 4130 and Lorin Thomason
was supposed to weld them up in cup form. I shipped him a bunch of parts
but have not heard back from him.
Lorin are you there? What happened?

Paul Lamar

The AirCraft Rotary Engine NewsLetter.              Powered by Linux.

http://home.earthlink.net/~rotaryeng/            http://www.linux.org