tom jelly wrote:
Well Jim Mederer is charging like $1200 each for aluminum end
housings.
They are not easy to make as the wear coating probably has to be
applied with what is called a detonation gun to be absolutely
reliable. A detonation gun shoots carbide particles at the wear
surface and then it must be ground and or lapped.
There is a new surface treatment that would be perfect for this. The
firm
that developed it has an ad in Racecar engineering magazine (can't
remember
the name though.  I posted it to the list a few months back.)

Tom
It's not exactly "new", but there is a technique called "flame spraying"
that I saw demonstrated a few years ago.  It involves using a large, high
velocity flame (plasma maybe?) jet to melt, atomize, and deposit continuous
wire or rod fed into the jet onto a cool/cold metal substrate.  At the time
it was still being developed and appeared to have a lot of very good
applications for hardfacing, etc.  The main market they were targeting at
the time was deposition of stainless steel or chrome-moly on softer carbon
for pipe linings, etc.  Seems something like this might work well and
economically for making machining blanks out of rough aluminum castings or
billets.
Most of this has been tried including Nickasil. None of it works
as well as detonation gun application. The particles travel
at near supersonic speed and imbed themselves in the aluminum.

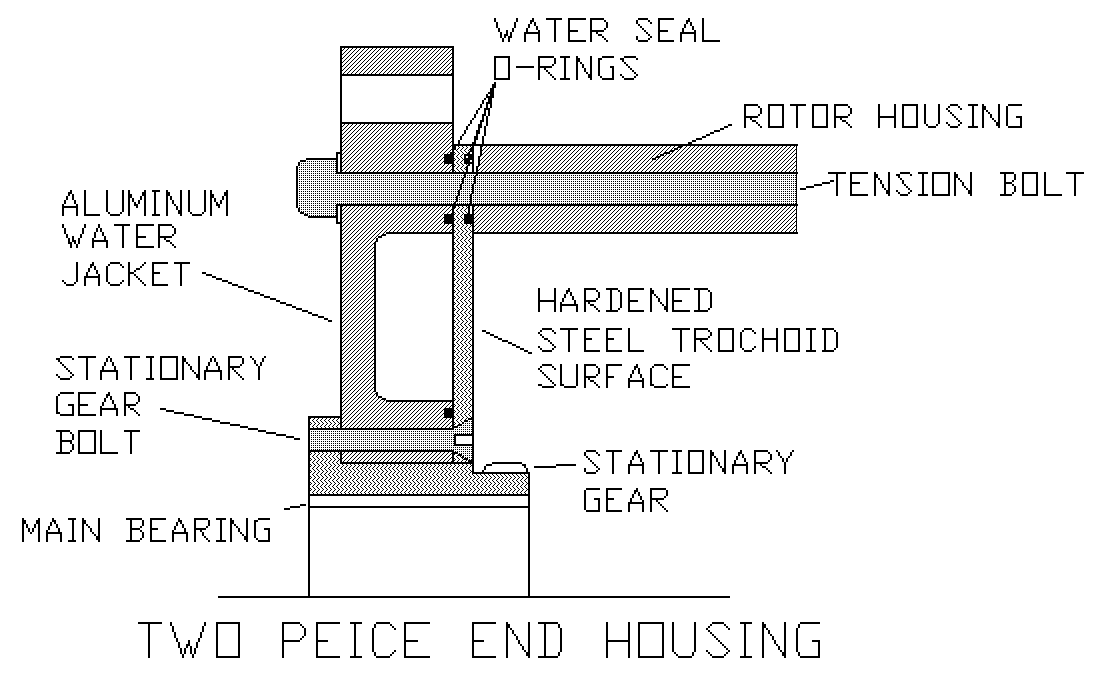
What has not been tried to my knowledge is a two piece end housing
like this. This can be made on an ordinary NC mill out of billet aluminum.

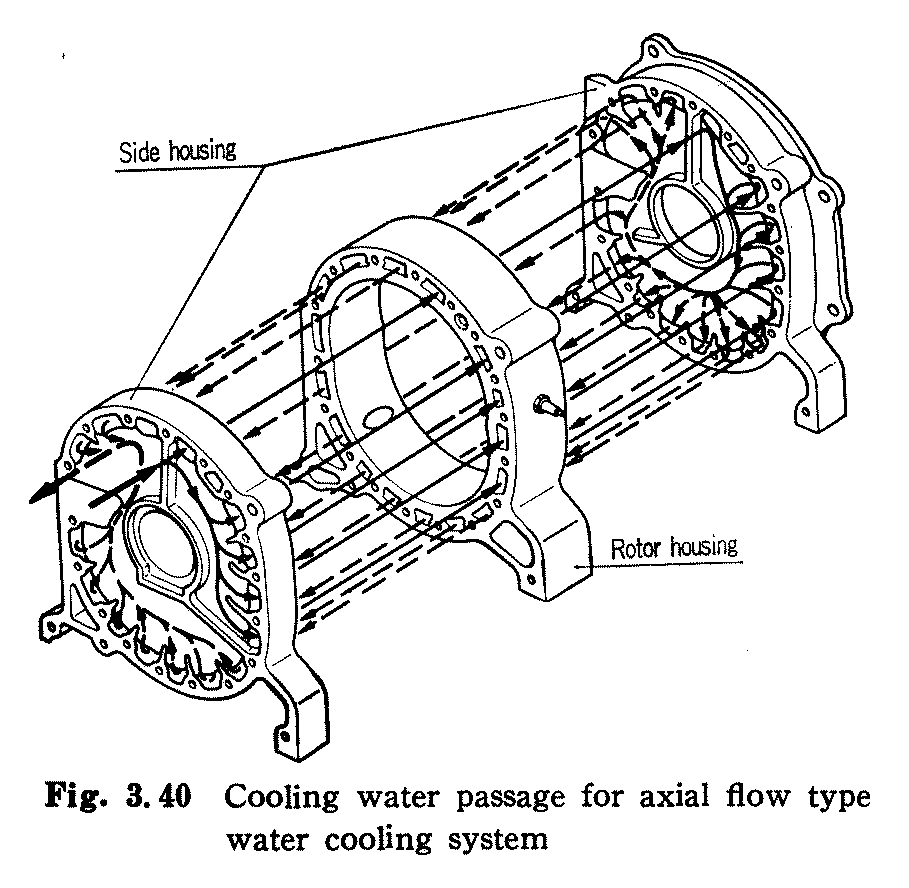
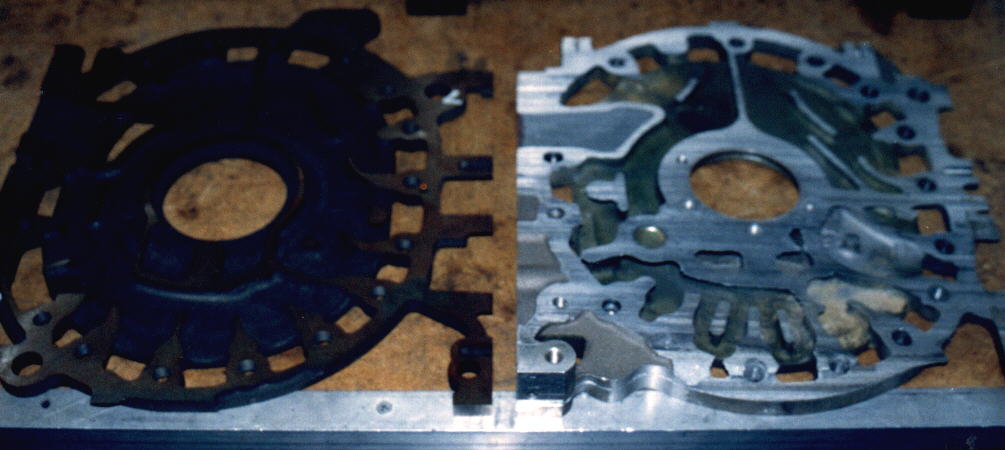
The water passages of the stock end housing must be duplicated.

Paul Lamar

The AirCraft Rotary Engine NewsLetter.              Powered by Linux.
ACRE NL web site.
http://home.earthlink.net/~rotaryeng/            http://www.linux.org