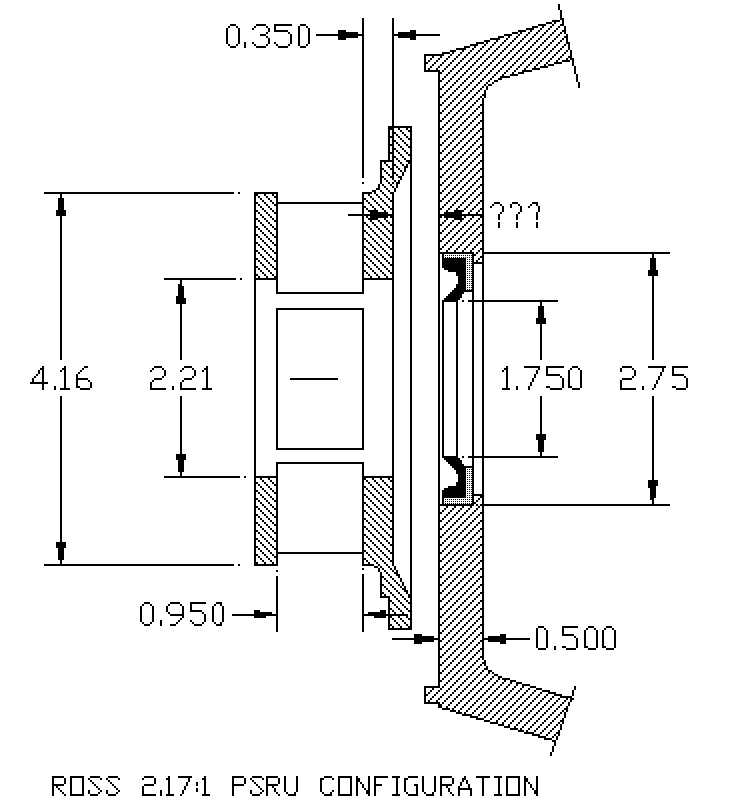
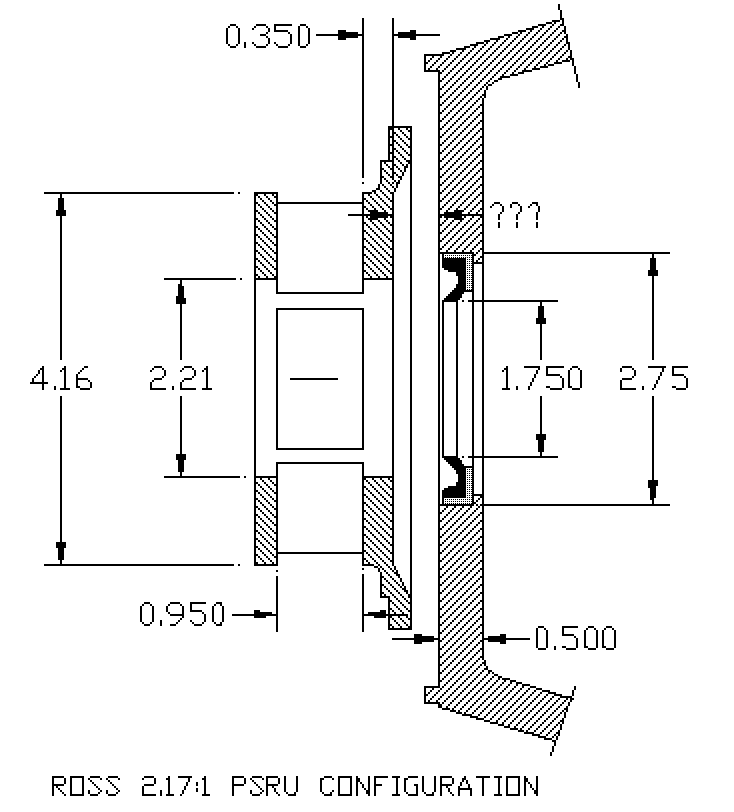
For those of you that would like to add a thrust
bearing to your Ross 2.17:1 gear box here is a
drawing that you might find useful. The sun gear, shaft
and planet pinions are not shown for clarity.

As far as I can tell, from the dimensions that Finn gave me
and measuring the planet carrier that I have,
this is the relationship of the Ford planet carrier
to the Ross bell housing. Some dimensions are still missing
and I am not sure about the dimension marked ???.

This will of course require a different shaft and sun gear.
The design of this shaft awaits a few dimensions on the sun
gear. Right at the moment I think the ID of the sun gear is 1.45
and the root diameter is 1.82.

Looks like a double needle thrust bearing with an OD
of 2.187" and an ID of 1.500" will partially fit inside
the 2.21" dimension of planet carrier if part of the gear
is ground down to 1.50. Obviously not practical so the
gear would have to be shortened to .950 which may
not be practical for attachment reasons.

There is another thrust bearing with an ID of 1.772 and an OD of
2.559. This possible could be fitted in if part of the gear was ground
down to 1.772 which would give a wall thickness of .161.
That does not look too bad. The thrust bearing would not fit
in the planet carrier so .3"  more room behind the planet carrier
would have to be found.

Also looks like that no matter the actual dimension of the missing
dimension marked ??? the seal size could be changed and
moved to the back side of the bell housing. The alignment of the
seal is way less critical than the alignment of the thrust bearing.

This would give even more room for a 2.75 inch diameter back up
plate that would fit in the current seal bore. Sort of a hat section
shape. The back side of this aluminum device could be extended
to hold the new seal. It could be pressed into the
bell housing. I will make another drawing of this part.

I think it better to forget using a pin to hold the gear to the shaft.
I think it better to warm the gear to 500 degrees and cool the
1.451 or 1.452 shaft with dry ice and press them together. Perhaps
a bit of tig welding on the ground down end would not affect the heat
treat of the gear on the other end.
Also possible is sweat brazing them together.

The shaft, aft of this, could then be ground to 1.500"
to provide a surface for  the seal to  rub on.

Paul Lamar

The AirCraft Rotary Engine NewsLetter.              Powered by Linux.
ACRE NL web site.
http://home.earthlink.net/~rotaryeng/            http://www.linux.org