Jerry Hey wrote:
Paul,  I spent the day figuring out the fly wheel cover.   One thing
I proved beyond a shadow of doubt is that rosette welding the cover
to the spools does not provide enough strength.  This is because the
weld area is too small and the very large difficulty of penetrating
the spools sufficiently.       On the other hand the rosette welds
served very nicely as tacks, to hold the spools in place until I
could put  fillet welds on the back side.   These will NEVER break.

I ended up making the cover out of .125 6061 T6 extrusion.  This is
marvellous stuff and will look and perform beautifully.  Very tough.
Although it is supposed to be 3 inchs wide , it was actually 3.08, a
perfect fit for the cover.

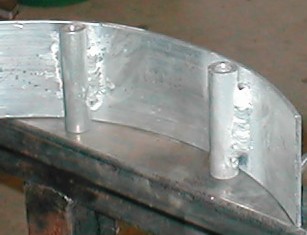
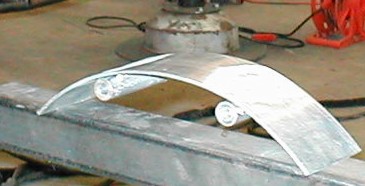
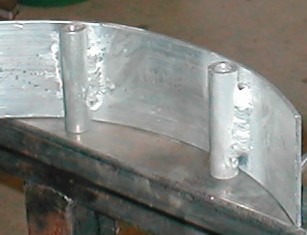
I am attaching a couple of photo's showing how the material looks and
how the  welds turned out.  I cut this section out of the entire
cover to avoid the  embarrassment of showing my previous mistakes and
disasters.    The cover actually wraps around about 330 degrees  of
the bell housing utilizing six spools.

Compared to a  cast spacer, this is much less expensive and can be
done one off no problem.   I think it is the right answer or at least
a very good solution for the near term.

One could sand the rosette welds flush and anodize the cover.   Let's
see.   Motor mount plate GOLD,  fly wheel cover  BLUE. .............

Jerry
 Looks good Jerry.

Paul Lamar

The AirCraft Rotary Engine NewsLetter.              Powered by Linux.
ACRE NL web site. Copyright 1998-2002 All world wide rights reserved.
http://home.earthlink.net/~rotaryeng/            http://www.linux.org