Paul, thanks for the mention.
>From the looks of it you should not have to cut out the material under the
flywheel, just pocket it a 1/4" locally.

...Chrissi

Cozy Mk-IV 13B Turbo
www.CozyGirrrl.com
Chrissi@BlueMountainAvionics.com
True but so far I have not found anyone that can pocket cheaply.
Apparently NC mills are so expensive everybody is making payments
on them and the payments must be made. If you don't do it with
an NC mill than somebody must stand there, operate the mill
and make reasonable wages.

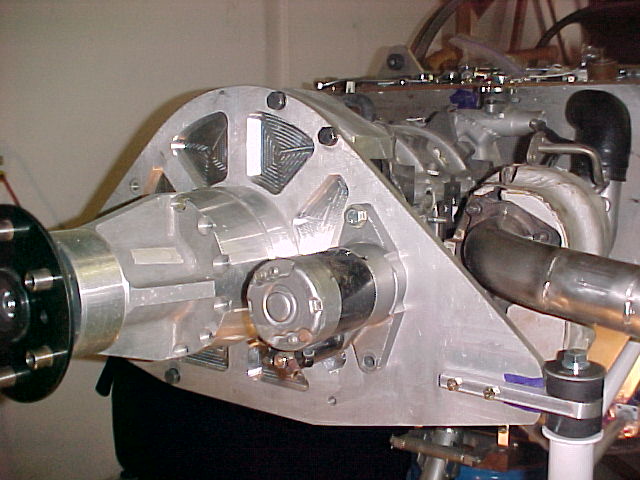
Hydra cutting on the other hand is much, much cheaper. A water jet
is used to cut holes in 1/2 inch aluminum plate. I calculated the
stress on the plate and it is way more than strong enough with
the hole shown. After all most of the loads are going in at the rubber
bushing locations. You may be forgetting that there are still
the 10 mm bolts and the Tracy supplied 1/2 plate spacers just
above the plate on both sides. (Not yet shown on the 3D)

Holes do tend to freak people out. We went through all that
already with the motor plate. We had a heck of a battle until
Jerry proved the deflection of the motor plate was minimal.
Good thing I got a lot of patience in my old age. When I was
a young engineer and I came up with a better way of doing
something I would run into some resistance from the troops.
"It just don't look right!"  Then it occasionally came down
to fist fights which I also won :-)

The reason my motor plate is pocketed instead of hydra cut
is for that reason alone. It would be plenty strong enough with
holes instead of pockets. We are dealing with emotions here.
People's emotions take over when they are uneducated on a
particular subject. In this case stress and strain and strength
of materials. The pockets are there to fool people into accepting
it as OK. And they look cool :-)

Paul Lamar

The AirCraft Rotary Engine NewsLetter.  Powered by Linux.
ACRE NL web site. http://home.earthlink.net/~rotaryeng/
Copyright 1998-2002 All world wide rights reserved.