Fred Osborn wrote:
A problem the single rotor guys have is how to get an oil
dipstick and filler tube set up since we don't have a
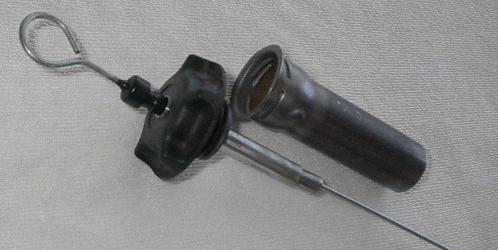
intermediate housing. Attached is what I am doing.

I have decided to change to an updated crank angle sensor
which leaves an empty hole in the front cover. It turns out
that the oil filler tube OD is a press fit into the lower
end of the crank angle sensor hole ID. Paul told us that the
oil filler and dipstick tubes were a press fit into the
intermediate housing. Sure enough, a little back and forth
with a rubber mallet and some penetrating oil and out they came.

I cut the filler tube to length, drilled a small vent hole
towards the lower end, smeared JB Weld around the upper end
and beat the filler tube down into the empty crank angle
sensor hole. The front cover was then set bottom up so the
JB Weld would flow down around the tube upper end before it
cured.

For the dipstick I drilled a hole in the filler tube cap and
reamed it to fit the dipstick tube. The upper end of the
dipstick tube was given a heavy coat of JB Weld and inserted
in that hole. Then I drove on a 3/4 " hard urethane foam
washer cut for a tight fit around the tube and into the cap
ID. More epoxy followed by a fitted steel washer followed by
more epoxy.

The dipstick will have to be shortened and remarked. Small
bends in the dipstick together with a chain guard mounted
under the heads of two stationary gear bolts will keep it
from any contact with internal moving parts.

Fred O.
The AirCraft Rotary Engine NewsLetter.  Powered by Linux.
ACRE NL web site. http://home.earthlink.net/~rotaryeng/
Copyright 1998-2003 All world wide rights reserved.