Butch,
Would you recommend welding in a plate rather than leaving the end
open.
My thinking is eliminating possible flexing and optimising stress
transfer.
George
******Yes George, by all means, since the weight penalty is minimal
after
adding a couple of Inspection holes....However caution must be taken
upon
welding these plates on:

The preferred way is to cut the Casting, fit and weld the plates PRIOR
to
machining. If this becomes an ordeal to do:

Fitting and welding on the Plates to a machined Bellhousing can be
done,
providing the Bellhousing is properly bolted on a scraped engine rear
housing
that has a good, clean mounting face on it......This is a job for a
"PRO"
guys, somebody like Ed.......I personally wouldn't touch it with a
10ft pole,
even though I'm an above average welder (ARC, MIG, TIG and
Oxy-Acetylene).
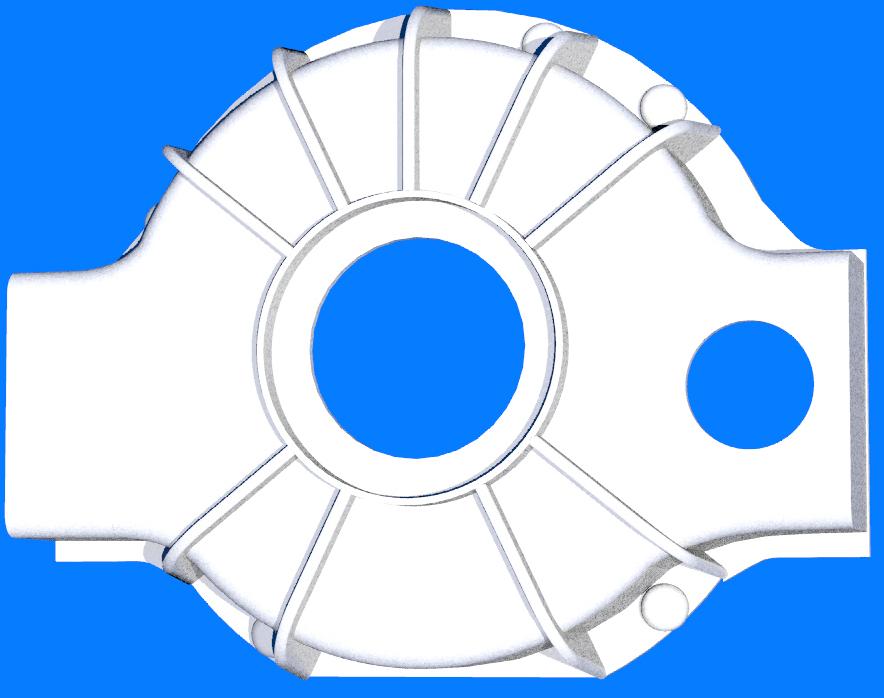
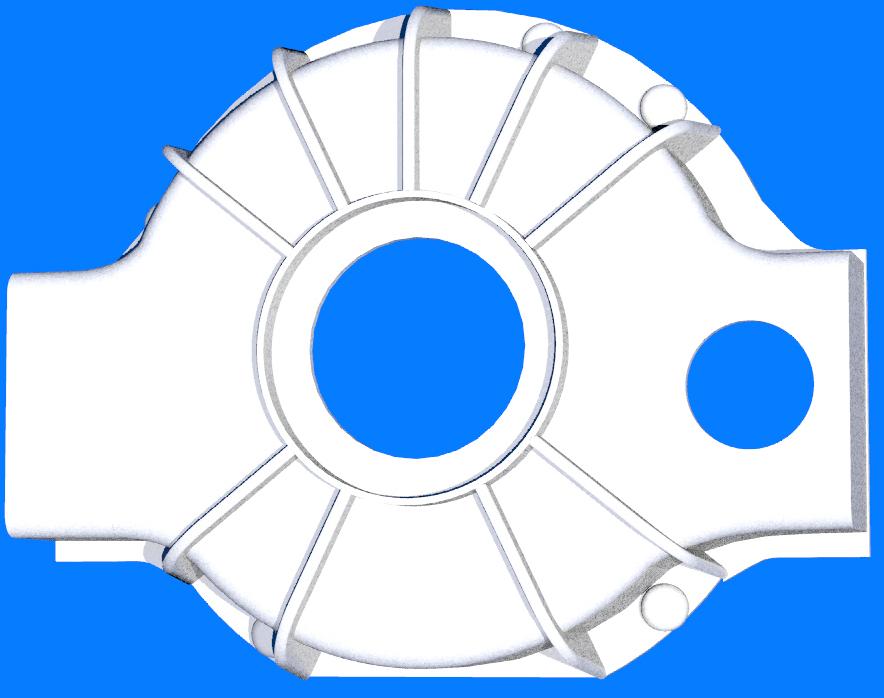
BTW Pushers, you can cut an add'l 1" off on the R/H side of the
Bellhousing
if you want to make it narrower and lighter......(See attachment)

Butch
George, I think this is something like what Butch had in mind.
He is probably off in God know where doing what ever he does there.

Paul Lamar

The AirCraft Rotary Engine NewsLetter.  Powered by Linux.
ACRE NL web site. http://home.earthlink.net/~rotaryeng/
Copyright 1998-2003 All world wide rights reserved.