I was going to e-mail you on this but the thread is going along
nicely - so
> what say you on 1/4" steel and would mild steel with nitrite
treatment do
     > the job ?
     >
     > I was thinking of attaching it at the centre and with about 4
stand-offs
> bolted through the aluminium housing - the edge being supported
by a ridge
> cut into the housing and held in place by the clamping action of
the rotor
     > housing when bolted -up.
     > George (down under)
George,
The thick plates should work fine. I believe the thin, (aproximately
1/8),
plates applied to both sides of the housing would work also. Pins
through would hold them in place. NItride treatment of the plates
would be the way to go. The factory has nitrided the side plates on
stock engines. I would not put the ridge around the outside. Simply
capturing the edge as Paul has indicated on the ACRE website would
be best. A captured edge (with a ridge) would put you back in the
warp problem.
Bill Jepson
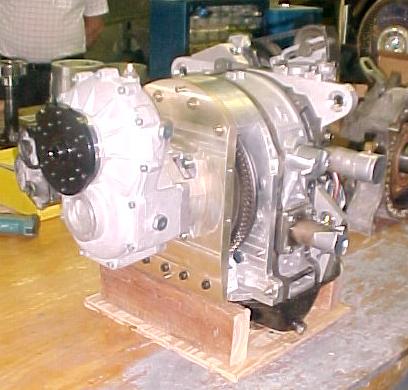
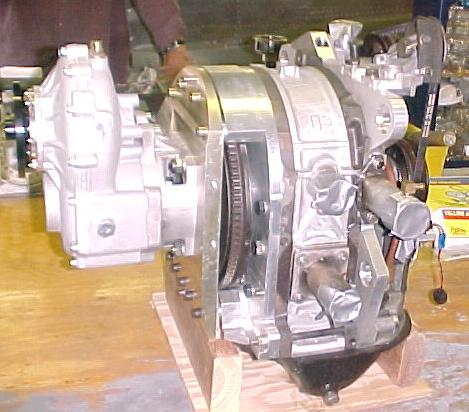
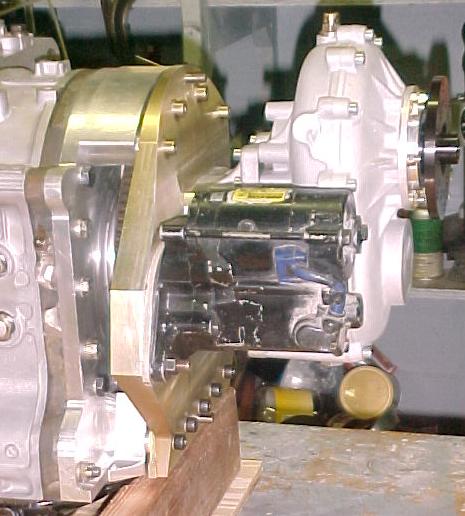
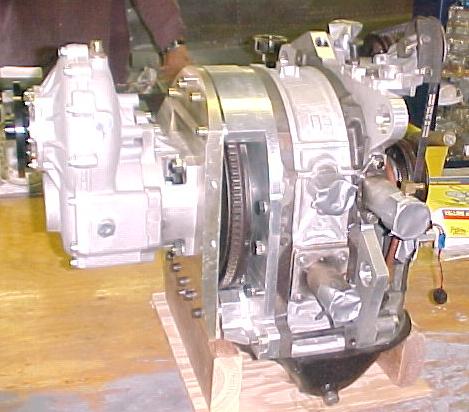
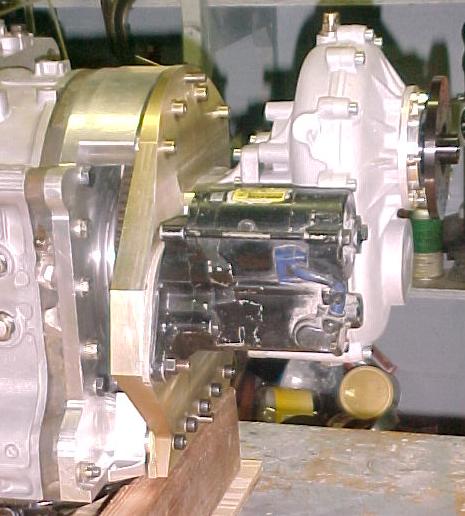
I am using one my one-rotor now a 16.5MM milled down side housing section.
This was done to establish a center connection around the bearing on the PTO
side and the stationary gear on the WP side. This configuration did go
through some severe testing, such as high temperature, up to 220F on water
and oil.
The next configuration will have a CI plate fixed on the inside and floating
on the outside. If this works, it would be directly applicable to a 2Rotor.

Richard Sohn
N-2071U
unicorn@gdsys.net
www.gdsys.net/WWWmembers/unicorn/
Are you going to bring your engine to Sun & Fun Richard?

Paul Lamar

The AirCraft Rotary Engine NewsLetter.  Powered by Linux.
ACRE NL web site. http://home.earthlink.net/~rotaryeng/
Copyright 1998-2003 All world wide rights reserved.