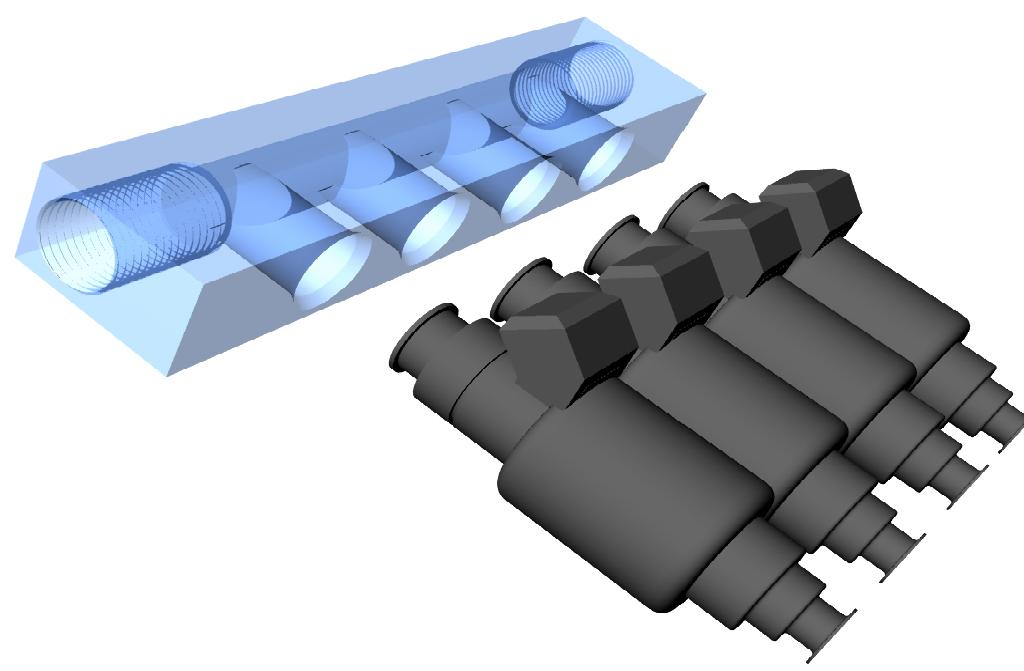
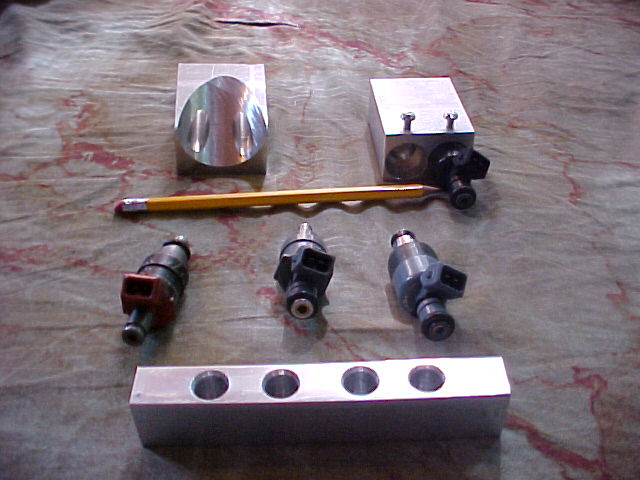
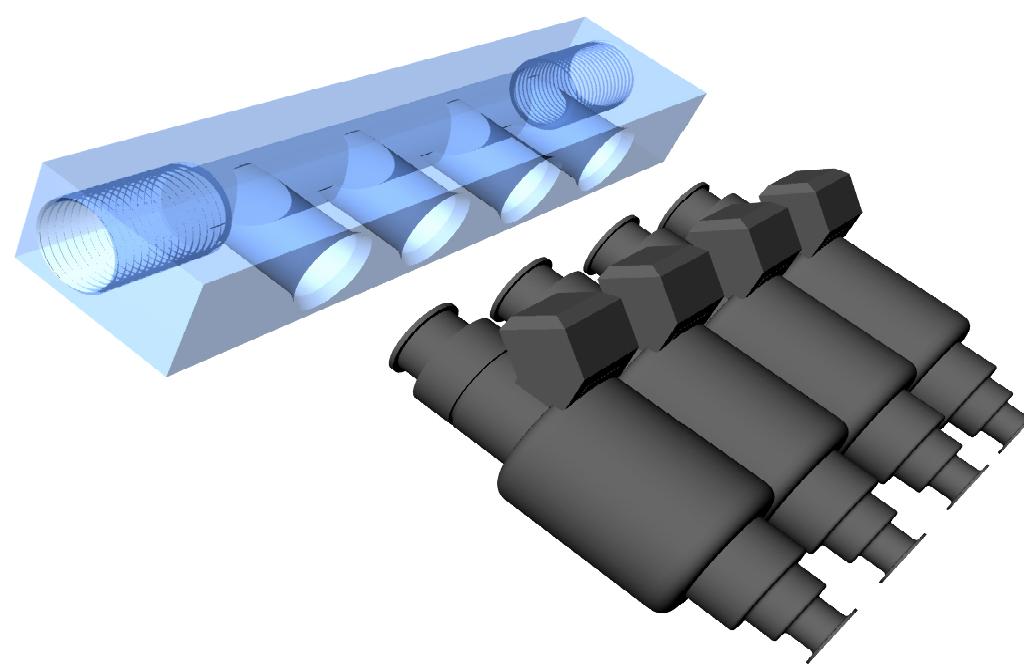
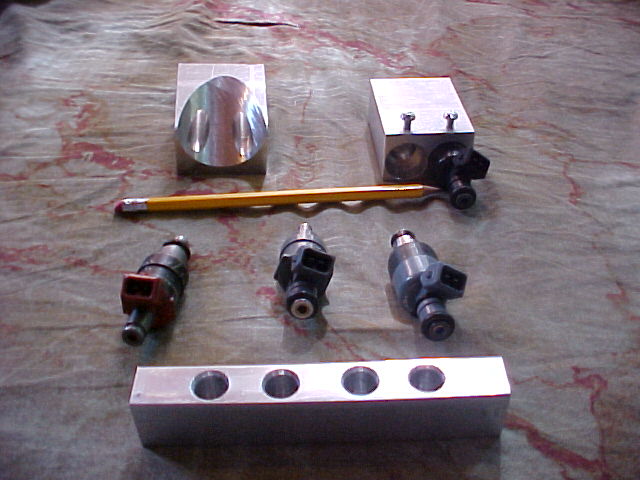
This is easy to make and can be done on a drill
press. All you need is the right tools.
A real long 1/2 inch drill.
A 17/32 drill for the injector holes.
A 3/4 60 degree counter sink. Same one used
on the injector holders.
A 9/16 18 tap for the AN -8 fittings.
It took me less time to make this than it did for me to
make this 3D by a factor of 3.
The first couple I made were out of 3/4" by 1" 6061 T6 bar stock
but they were not entirely satisfactory. Best to use 3/4" by 1-1/4"
obtained by mail order from Industrial Metal Supply in San Fernando
Calif.
Paul Lamar
The Rotary Engine NewsLetter. Powered by Linux.
ACRE NL web site.
http://www.rotaryeng.net
Copyright 1998-2005 All world wide rights reserved.