I thunk about it some more and discovered a few things on
the dyno. I am having trouble getting the runners short
enough so I made some changes. The 180 degree bend is
9.42 inches long by itself. Add four inches for the tube
stubs going into the engine and you have 13.42 inches. That
only leaves three or four inches for optimization.
We also needed to seal the
slide throttle in case somebody floods the engine during
starting. In normal operation and starting it is no problem
as is but if you flood the engine you could leak a bit
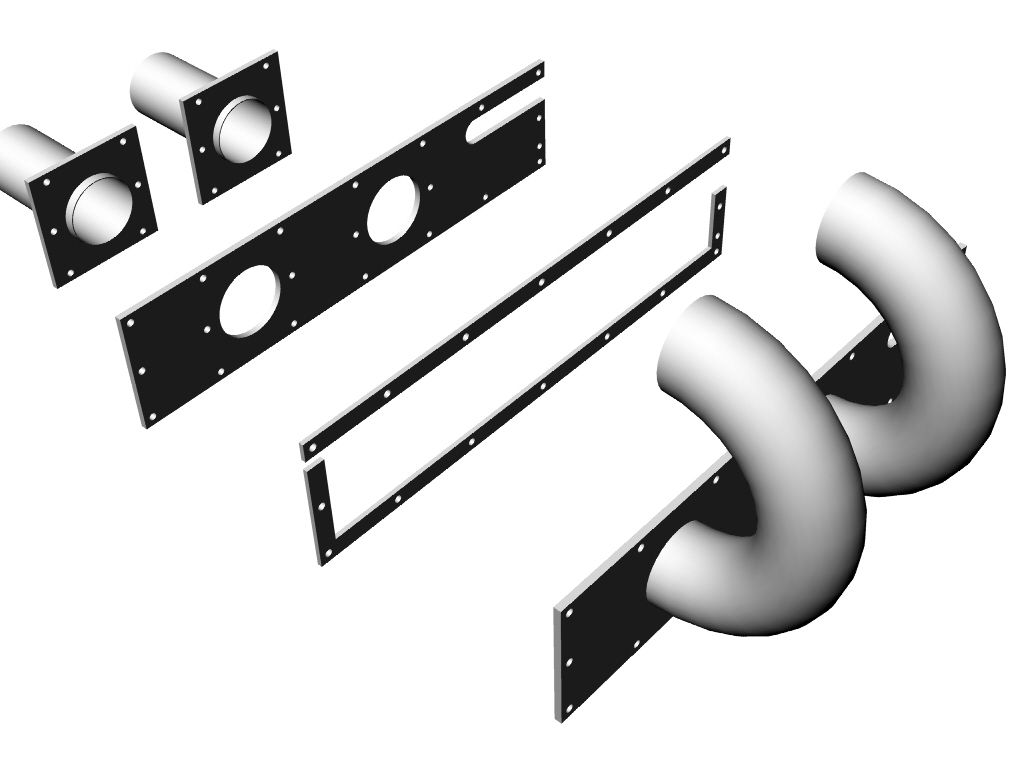
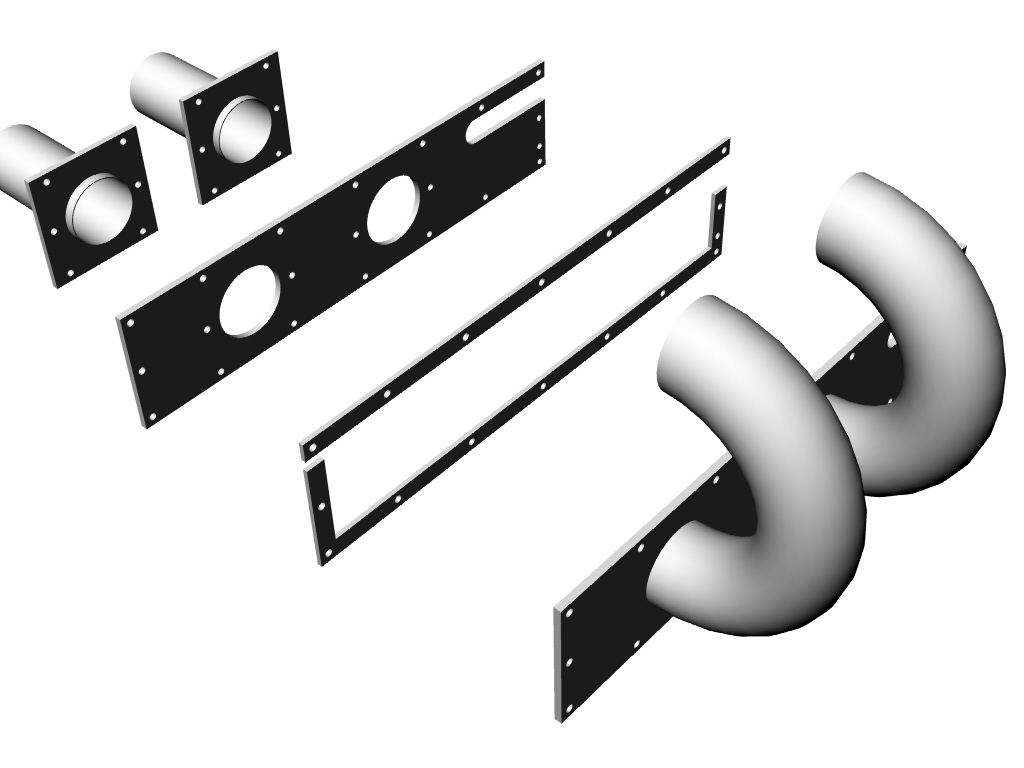
of fuel. I decided to weld the runners to the outer plate
thereby eliminating a couple of flanges and a whole bunch
of nuts and bolts. The inner plate must be still bolted
on or one would never be able to take the engine apart.
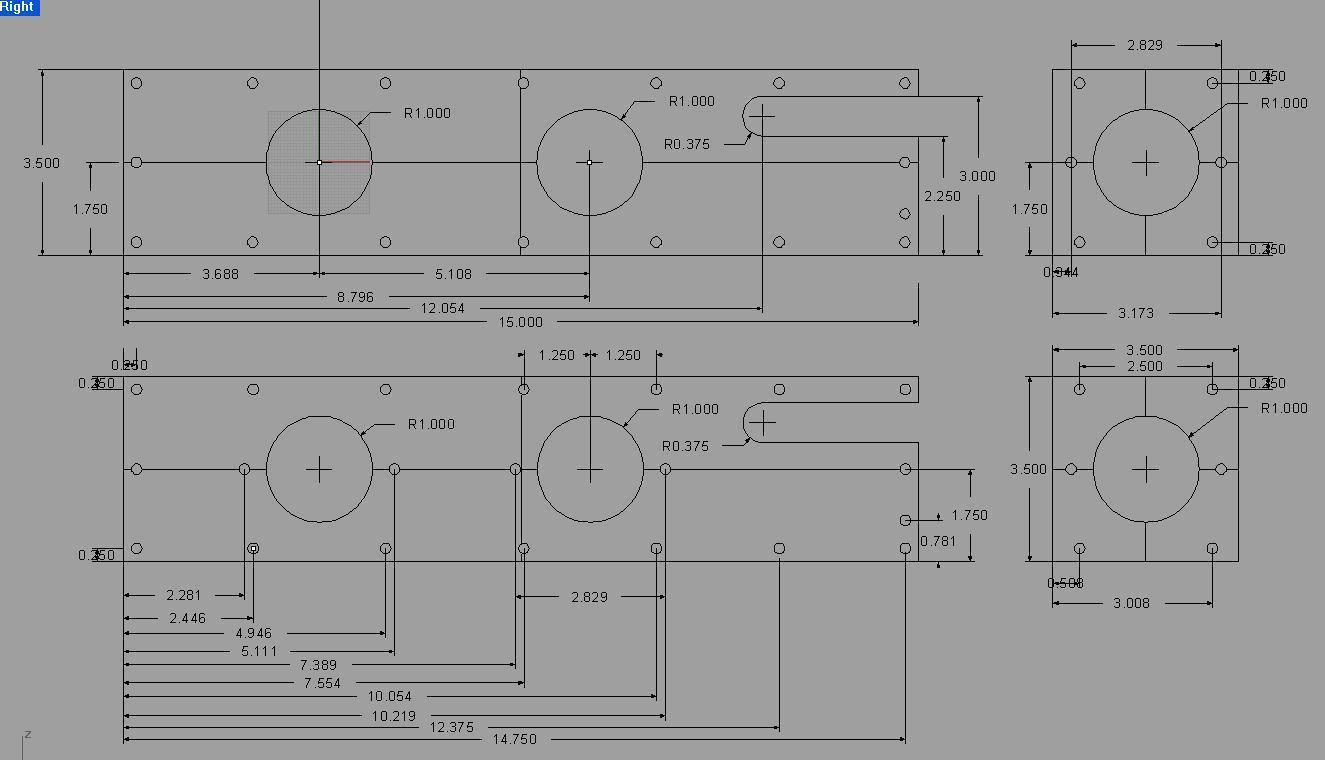
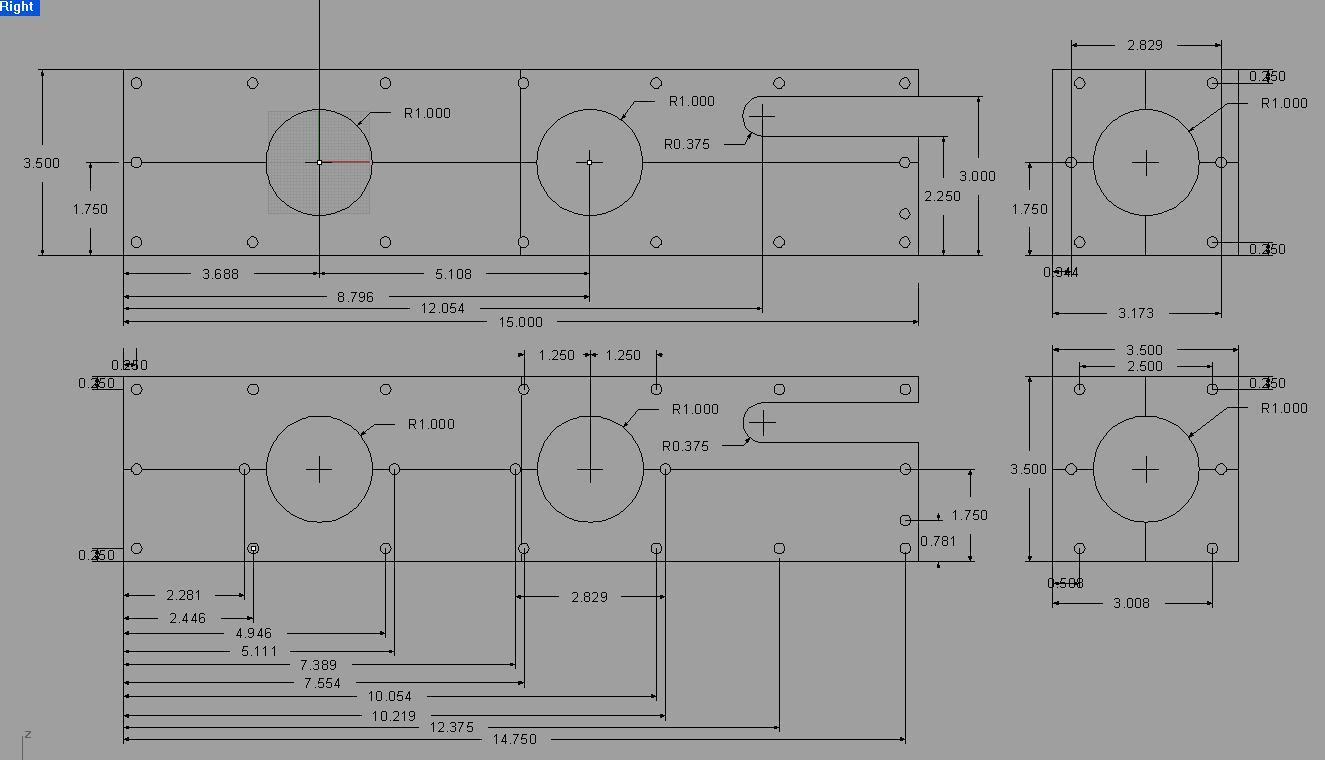
I also changed how the flanges and plates are welded to the
runners. They go into a 2 inch holes in the plates improving
the alignment and make the transitions smoother.
the plates are now 3/16 instead of 1/8 thick so welding
the runners to the plates do not warp the plate. Same thickness
as the old flanges. The inner flanges are larger so the same
bolts that bolt the plates together also bolt on the flanges.
This saves a few nuts and bolts and a whole bunch of counter
sunk holes.
The first two pictures are the current design with the long
runners. Way too long.
The third illustration is the new design. I will use ordinary
gasket material to seal the slide throttle. Not all parts
are shown.
BTW Dave did not want to run the dyno today so it will probably
be the middle of next week before we can try out the new intake
manifold vacuum referenced fuel pressure regulator and the EFI.
I hope to improve upon the 230 HP we are getting at 6250 RPM
with the long pipes and the 245 HP we are getting at 7000 RPM
with the short pipes using the Webber 58 mm carb.
Paul Lamar
Paul,
Looking at your rev #5 I was stuck by a suggestion. The outer plate is
Alum. for welding and strength purposes. The inner plate is mechanical
only, it could be made of another material that could be liquid welded or
bonded to the center perimeter slide frame, thereby needing only one side
sealed by the paper gasket. Does Teflon weld to its self? You could even
use phenolic board which joins to itself and is readily available
commercially, or is all of this redundant because you are already epoxzing.
the frame in? Just thoughts.
Tony2
Yea something like that would work. It could also be hogged out on a
mill. Kind of expensive however. Right now we are punching them out
on a big AMADA NC punch. Only takes three minutes per part. Less than $10
per part. The whole slide throttle is less than $50 including the
Teflon. Less costly to make than a 3 inch butterfly or worse, two two
inch butterflies. The slide throttle costs less than the two tubing
bends.
Paul Lamar
HI Paul,
That OMADA CNC punch machine looks like the same model used in my next door
neighbors factory. Runs on air pressure correct?
Thanks for the dimensions. Since you have welded up the plates you won't be
able to use my version on your test machine but I'll make it anyway in case
someone can use it in the future. I worry about warpage though. I assume
you are having the pipes welded to the plates flush and then ground flat if
needed?
Doug in Japan
I don't know about the air pressure but that is good news for you.
Offer to learn to program it and he will give you a good price
on some of these slide throttle parts.
There is a Windows PC programming program I think. All you do is
put in the drawing and it does most of the rest.
What about that Chris Talbot?
Yes on the pipes.
The plates don't need to be super flat. The Teflon is soft enough
to conform to whatever. A little fine sanding and polishing will
do the trick.
Paul Lamar
--
The Rotary Engine NewsLetter. Powered by Linux.
ACRE NL web site.
http://www.rotaryeng.net
Copyright 1998-2005 All world wide rights reserved.