Paul,
Are you going into production with the P port? I would be interested.
Have you thought about the rotor housing? Can we get a group buy for new
rotor housings and have someone bore them out for the 2" pipe? Just
thinking.
Joe Berki
Limo EZ
No. Tom is taking over the slide throttle project and I will
give you detail instructions on how to cut the hole in the
rotor housing. Here are a few shots on the subject.
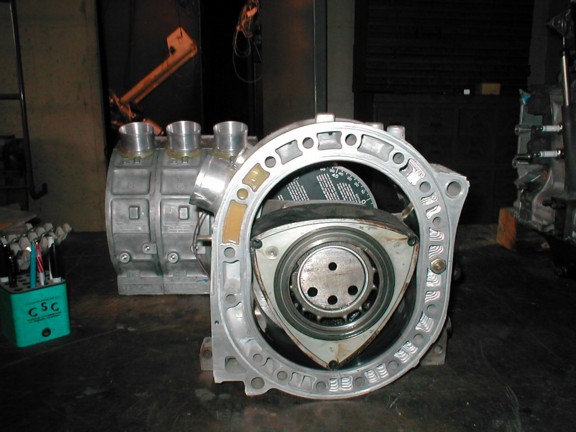
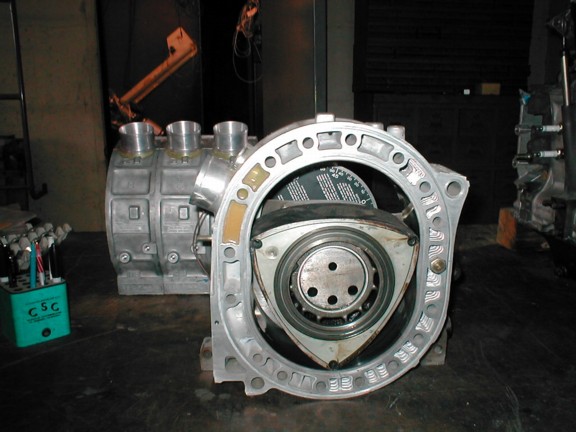
First you fill the water jacket cavities with JB Weld.
Heat the JB Weld in boiling water to reduce the viscosity
before you mix it so it will pour easily. First picture.
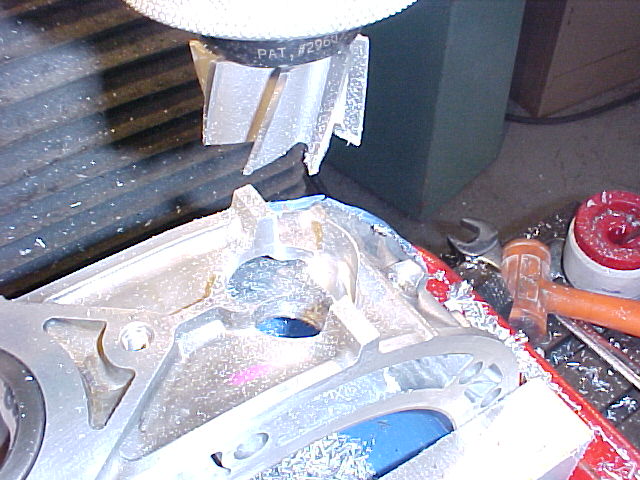
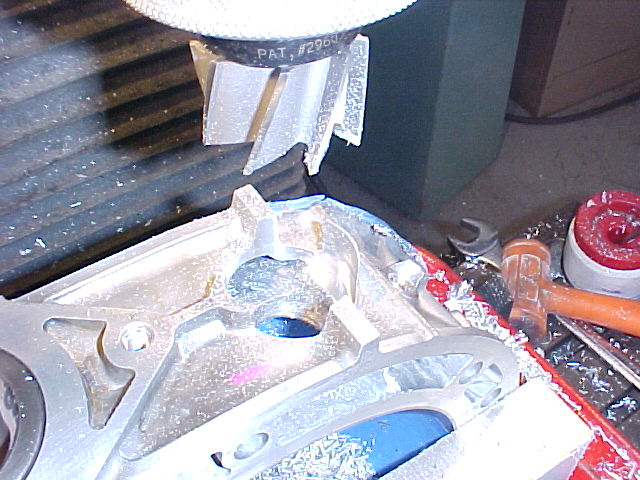
You start with with a small drill and work your way up to
a 1 inch drill, a 1-3/4 shell mill and finish off with a boring head.
Second picture.
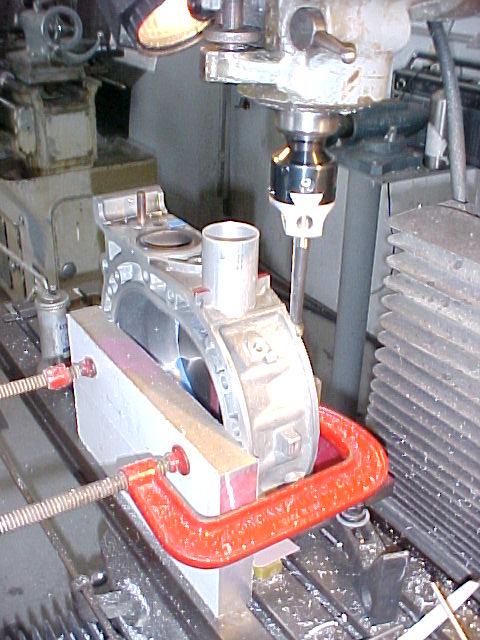
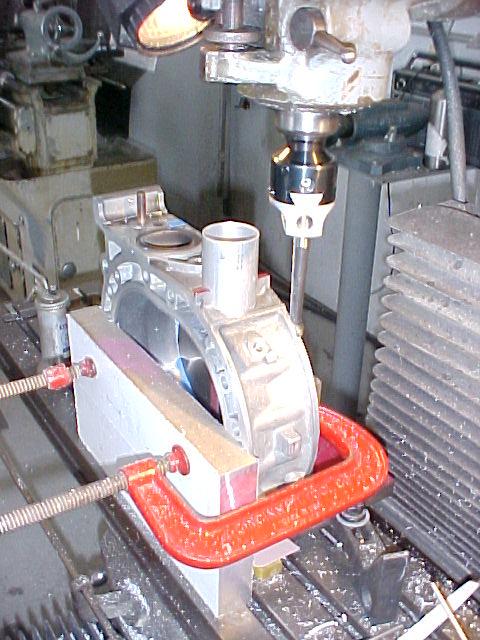
The final hole size is 1-7/8 with a 2 inch counter
bore shy of the steel rotor housing liner. Third picture.
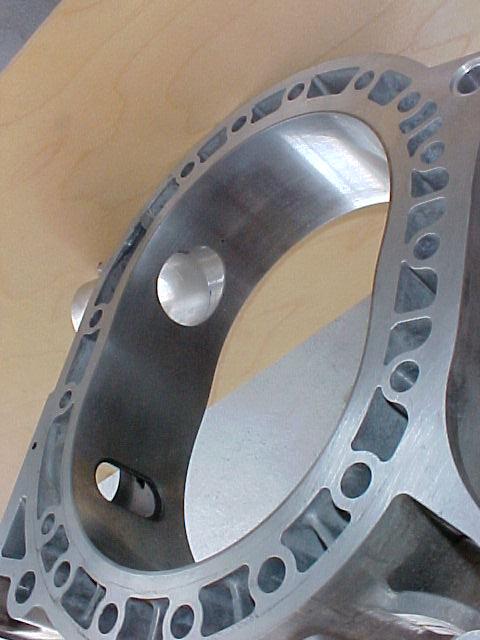
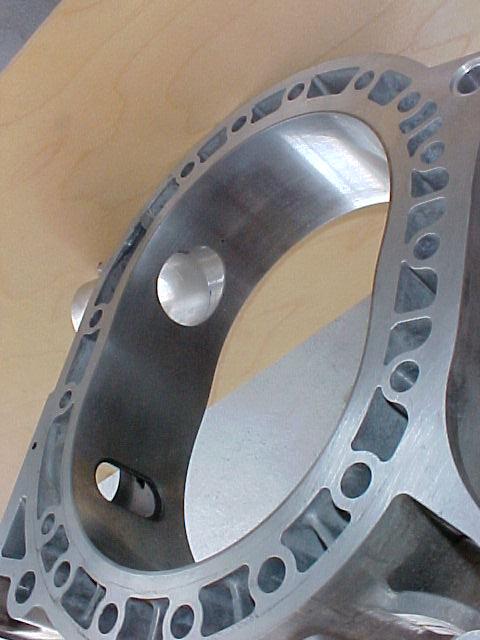
Fourth picture where you can see the depth of the two inch
counter bore.
Takes about 1/2 hour once you have the mill set up.
Bond the tubes in with the pre welded flanges using
JB Weld and the inner slide throttle plate for aligning
the flanges in the front and rear rotor housings.
The whole operation is very easy to do.
One guy did it with a hole saw but I don't recommend that.
Too imprecise.
Paul Lamar
The Rotary Engine NewsLetter. Powered by Linux.
ACRE NL web site.
http://www.rotaryeng.net
Copyright 1998-2005 All world wide rights reserved.