>
> Hi Paul, I'm back from Florida. Please put me back on the
list
> when you get the
> chance. How was your excurstion to Hangtown? Any feed back
on the
> Slide components?
> Thanks T.W.
>
> Hi Tom, Thanks for allowing me to pick up the slide throttle
parts
> in Placerville. You have quite a menagerie on your estate up
there.
>
> Our land is not far from yours. It is on Red Robin road if
you know
> where
> that is. We just put it up for sale.
>
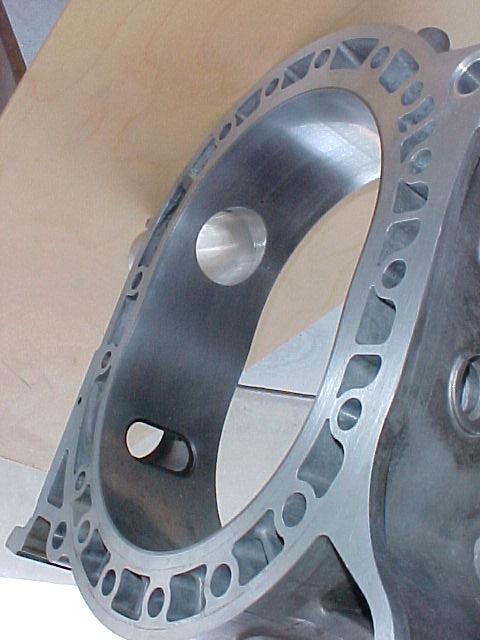
> I got the inner plate machined to fit Mark's P-port engine.
I also
> have some
> 1/4 thick Teflon to make the slide itself as soon as I get
over the
> flu.
> When I get that done I am going to ship it off to Mark.
Hopefully
> Jerry will have Mark's motor mount fixed and we can soon run
the
> engine
> with your slide throttle unless we run into some more snags.
>
> I notices the 2 inch holes are slightly over size. You might
want
> to reduce their diameter by about .050". I measured them and
they
> are about .050" over size. People can always file them
> out to fit. Everything else looks just fine.
>
>
> Paul Lamar
>
> Ok, sounds good, I used a bimetal hole saw for these
holes. I"ll
> be using a better (closer tolerance) for future copies. I'm
> interested to hear how this works, so we can move forward.
Oh by
> the way I would like to have two rotor housings fitting with
the
> PPorts. Who did you use and can I have a set of housings drop
> shipped to them for the installation? Let me know Thanks T.W.
>
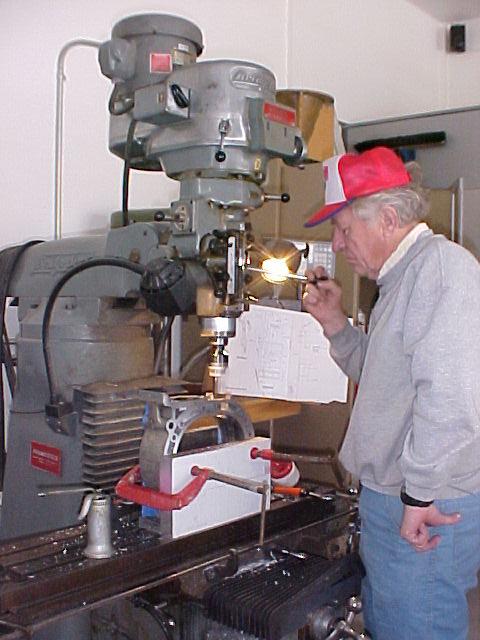
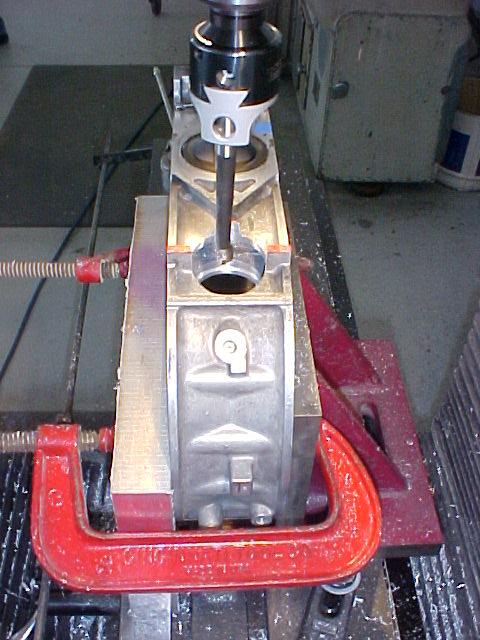
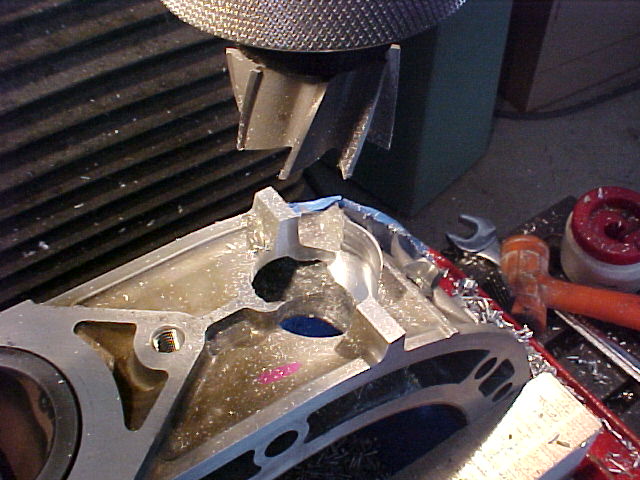
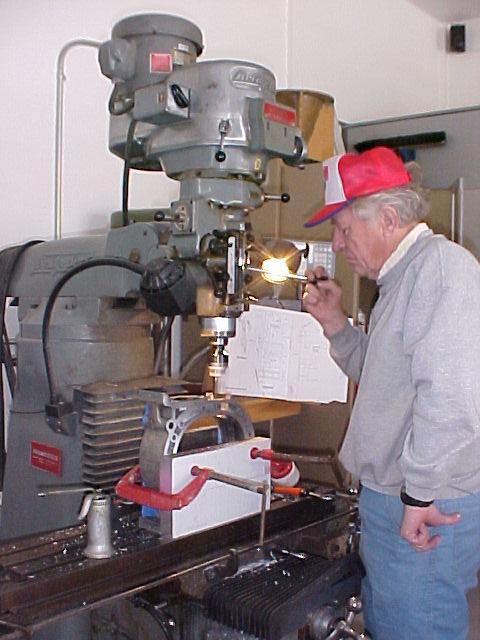
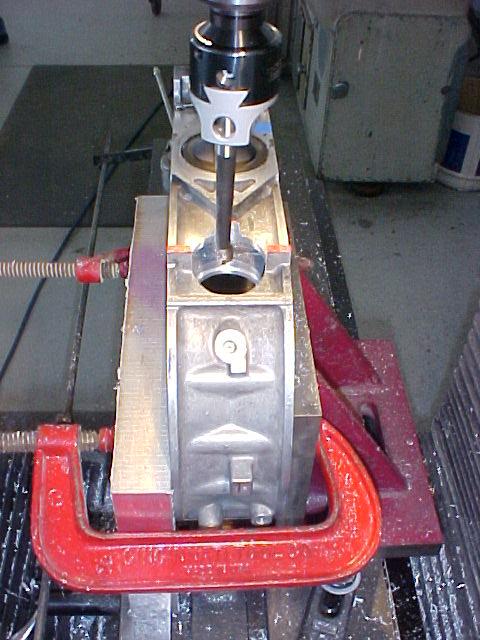
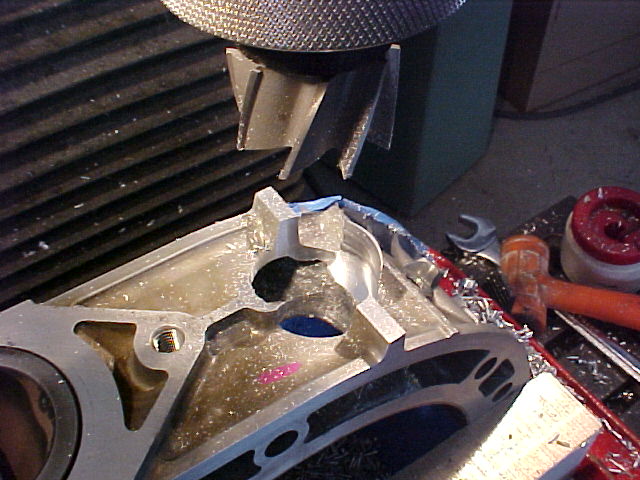
> My next door neighbor, Jim Poole did it on a Bridgeport.
I'll ask him
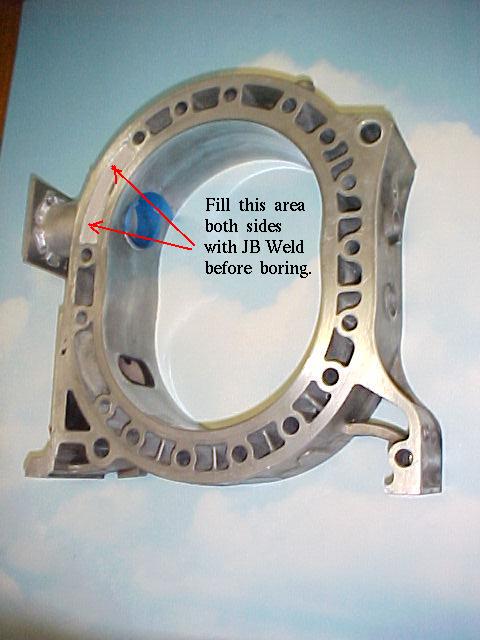
> if he is interested in doing some more. You will save a lot
of money
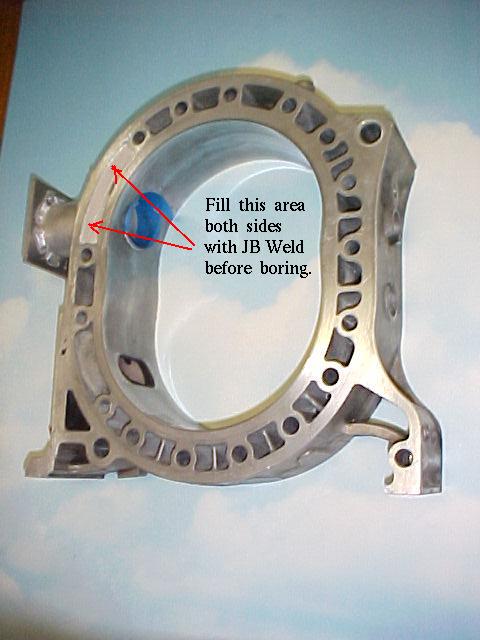
> if you pre fill the area with JB Weld. Heat it in boiling water
before
> you mix it and it will pour easier.
>
> Paul Lamar
Are you still holding the insert in with epoxy? How do you do
this
if you fill the voids prior to boring? Jerry
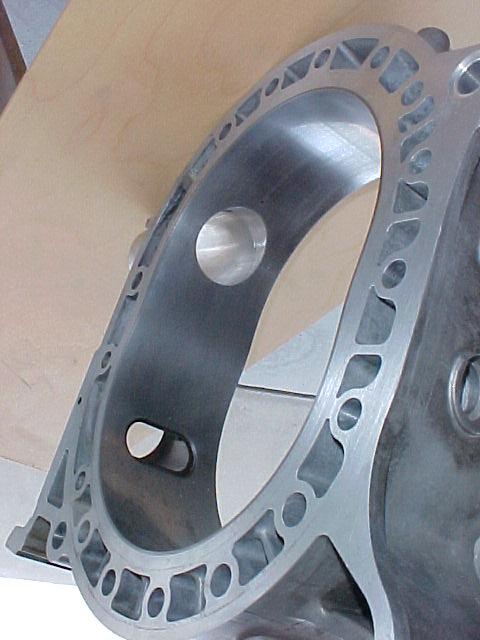
After it is bored we do a trial fit. There should be a loose
slip fit. Then coat the outside of the insert with JB Weld and
stick
them
in there aligning the two inserts with the inner slide throttle
plate. Use an assembled center housing to make sure everything
fits
together.
That insures all the bolt holes line up. Tom will have to do
that after
he gets the bored rotor housings.
JB Weld, like most epoxies, is good
to about 3,000 psi. The circumference of the 2 inch OD tube
is 6.28 inches. If the insert is only in there for one inch of
its
length that is a force of 18,840 pounds holding them in. They are
in there for good. Sand the insert tube lightly with fine sand
paper
before applying the JB Weld to remove the aluminum oxide coating.
Also they can be anodized if you wish. The epoxy sticks to the
anodize
better than tubing that has been sitting around and acquiring
an aluminum oxide coating.
Paul Lamar
Tom, I talked to Jim Poole. He is interested. He quoted me a very reasonable
hourly rate for boring the p-port holes in the rotor housings.
Contact him directly. His phone number is 805 933 2449.
I told him there
would be more people interested in the future. The more he can do at the
same times lowers his cost because of set up time. He knows nothing about the
JB Weld so make sure the rotor housings are potted in advance.
Paul Lamar
The Rotary Engine NewsLetter. Powered by Linux.
ACRE NL web site.
http://www.rotaryeng.net
Copyright 1998-2005 All world wide rights reserved.