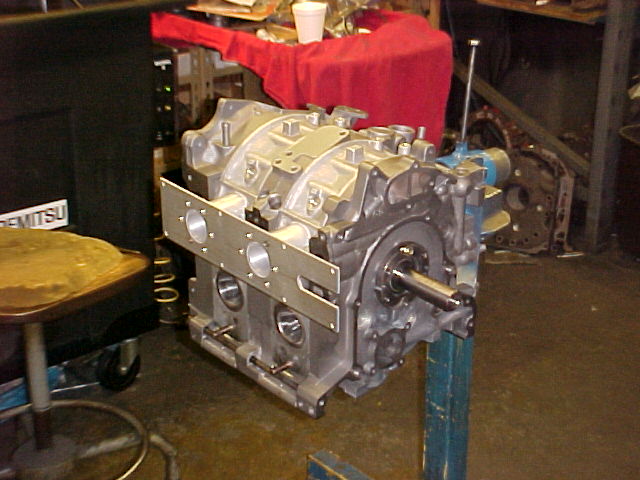
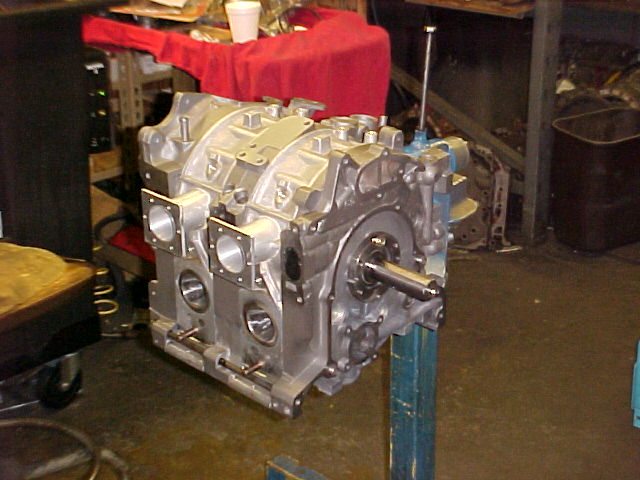
Paul do you have a Dxf file for the p-port? I have a machine
shop here, that will CNC machine both rotor housings for $150.
Tony
Great price. $75 each. How can you go wrong?
I predict in the next ten years you can sell hundreds.
No DXF for the rotor housings. I'll send the dimensions
shortly. Basically there is a 1.875" diameter hole all
the way through and a 2 inch diameter counter bore down to the
steel liner that the intake tubes seat on.
I just sent you the first two slide throttle parts.
Here are two more.
The O rings grooves in the Teflon slide are optional.
You can add them later if you feel you need them.
I don't think they are necessary.
That sounds great. I appreciate it. I'm using ACAD 2000 and RHINO
Tony
Did you get the DXF zip files Tony? zip is the only practical
way of sending them but some ISP's filter out zips.
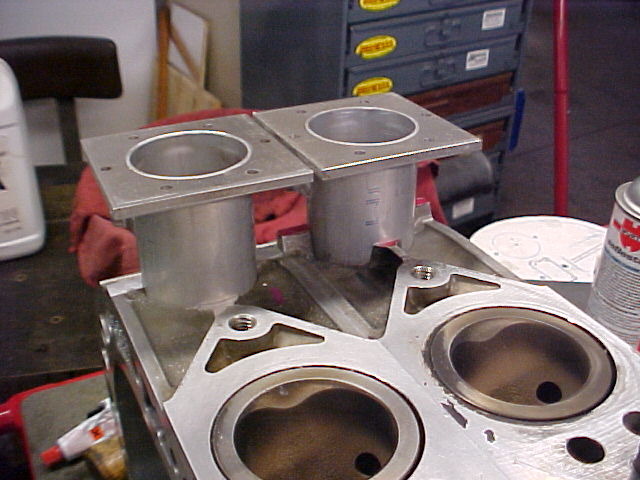
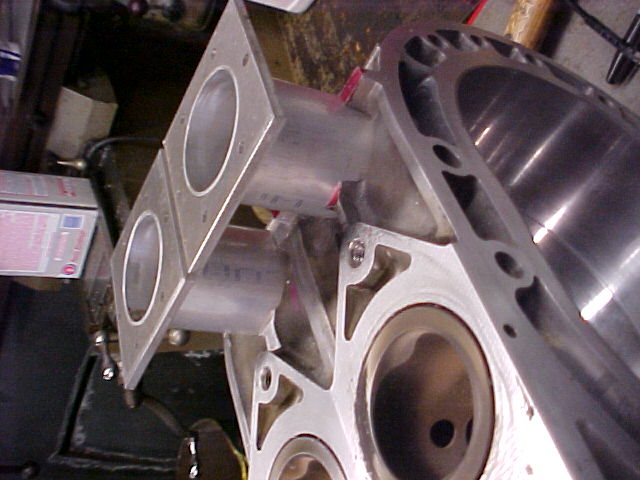
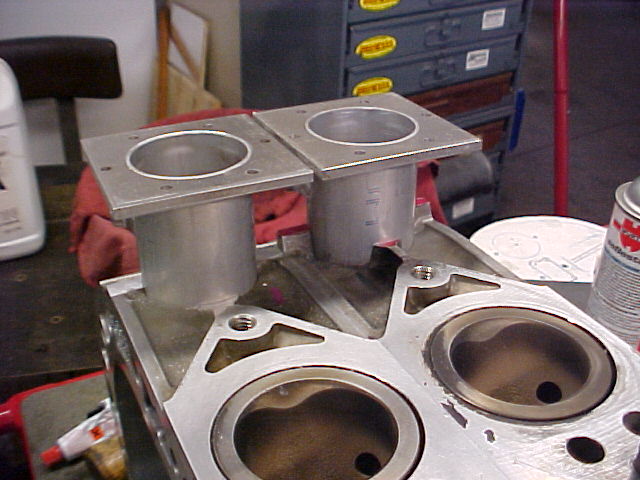
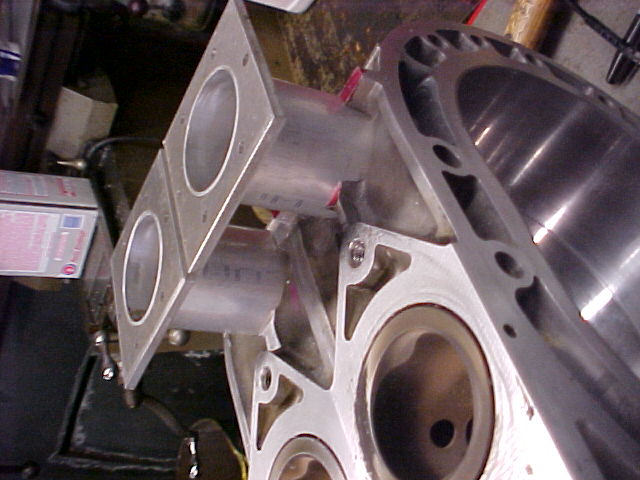
First you tig weld the 3/16th thick flanges to the short tubes
and then insert the short tubes into the bored rotor housings.
The tubes protrude through the flanges by the thickness
of the plate. In other words the ends of the short tubes
are flush with the inner surface of the back plate and align
everything. This is done to minimize leaks.
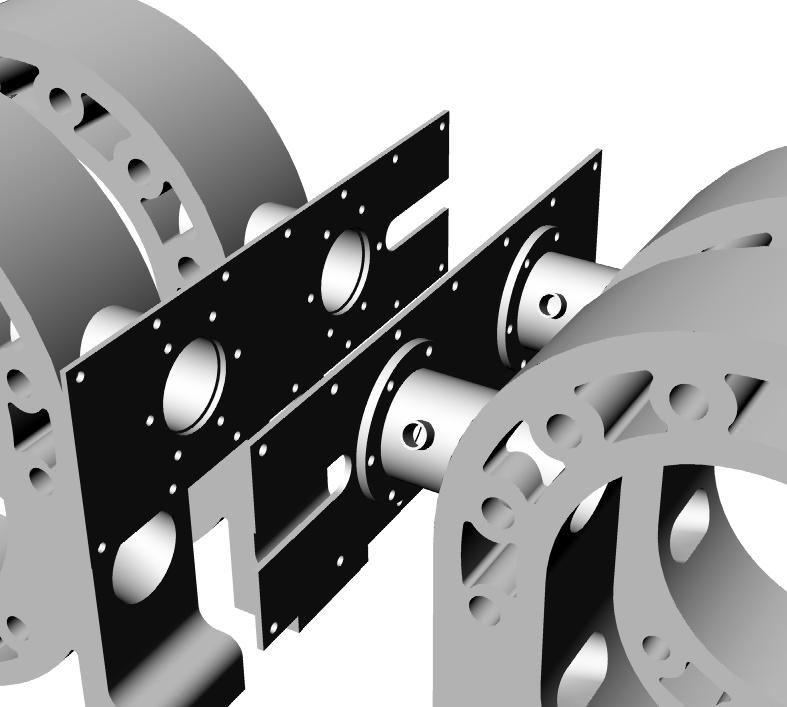
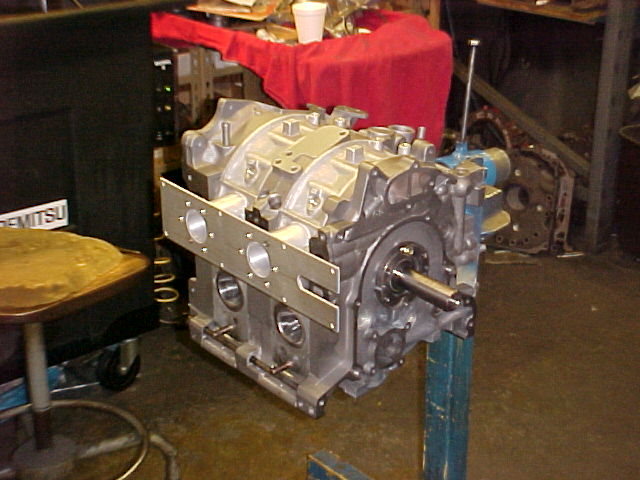
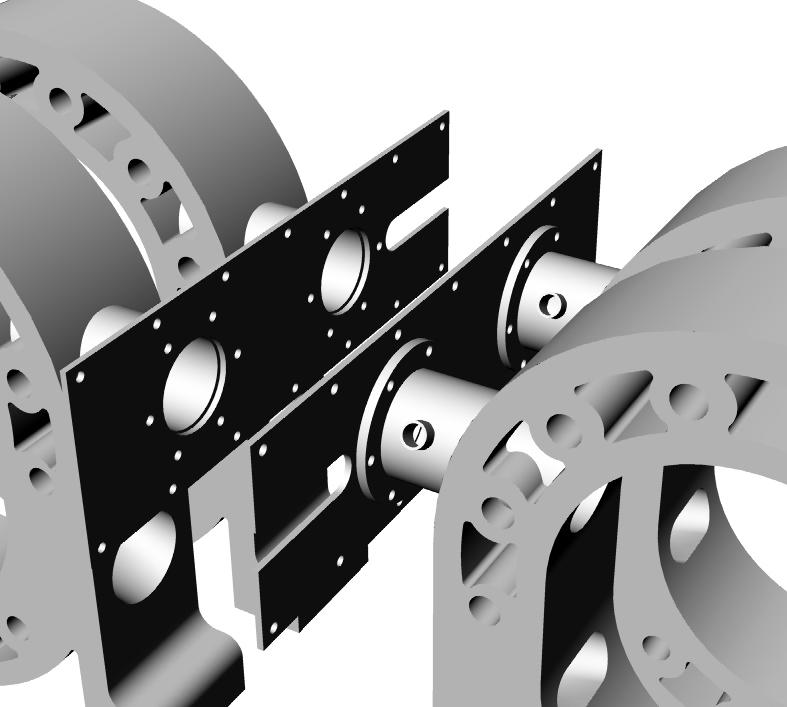
Place the rotor housings side by side and use one of the plates
to make sure the holes will line up when you assemble the engine.
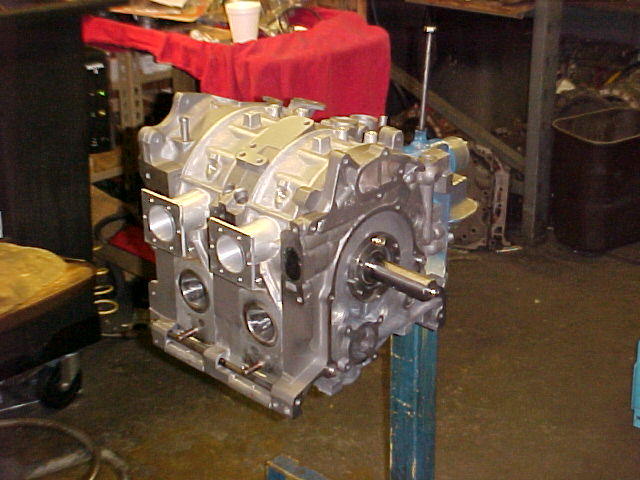
Some of these pictures were not done that way. This is an
improved method. Also the flange hole patterns have been
revised to eliminate a few nuts and bolts by having some
of them do double duty so the pictures show old hole patterns.
Then pot the water passages around the tubes with JB Weld.
--
Paul Lamar ...No rotor no motor.
The Rotary Engine NewsLetter. Powered by Linux.
ACRE NL web site.
http://www.rotaryeng.net
Copyright 1998-2006 All world wide rights reserved.