I don't know if it's applicable here, but I have heard that stainless
is
welded, the back side of the weld needs to be in an O2 purged
environment. I wonder if/how that's done when the inside of the pipe
is
being welded to a flange..
Matt-
That is true for tube butt joints such as headers. You need a
separate supply of nitrogen gas behind the weld. Not so for a
flange welded on the end of a tube as the slag, if any, can be
mechanically removed.
Paul Lamar ...No rotor no motor
Paul,
Let's hope that Matt mistyped O2 for N2! Oxygen wouldn't be used in
almost any weld process other than flame cutting.
Bill Jepson
Thanks Bill. I missed that.
Paul Lamar ...No rotor no motor.
Matt and Bill both agree; I think that darned English language is getting
in
the way. "Purge" means "to eliminate." In the old Soviet Union, for
example,
when an official was "purged" from the party, it meant he was sent on a
permanent vacation somewhere else.
So an O2 purged environment is just one where oxygen is not present and has
been replaced with another gas. Nitrogen was Bill's suggested replacement
gas; argon, available to TIG welders everywhere, would also work well.
Barry Gardner
Wheaton, IL
Darn! One of them there big words. You are right of course.
--
Paul Lamar ...No rotor no motor.
To your purging question; You can tape the end of the flange and purge it
all this does is to stop the sugariing of the stainless. Your flange would be
a fillet weld on the outside. If you have any more qestions on the stainless
welding dont hesitate to ask i have 35 yrs. exp. on welding
Peter Morrison
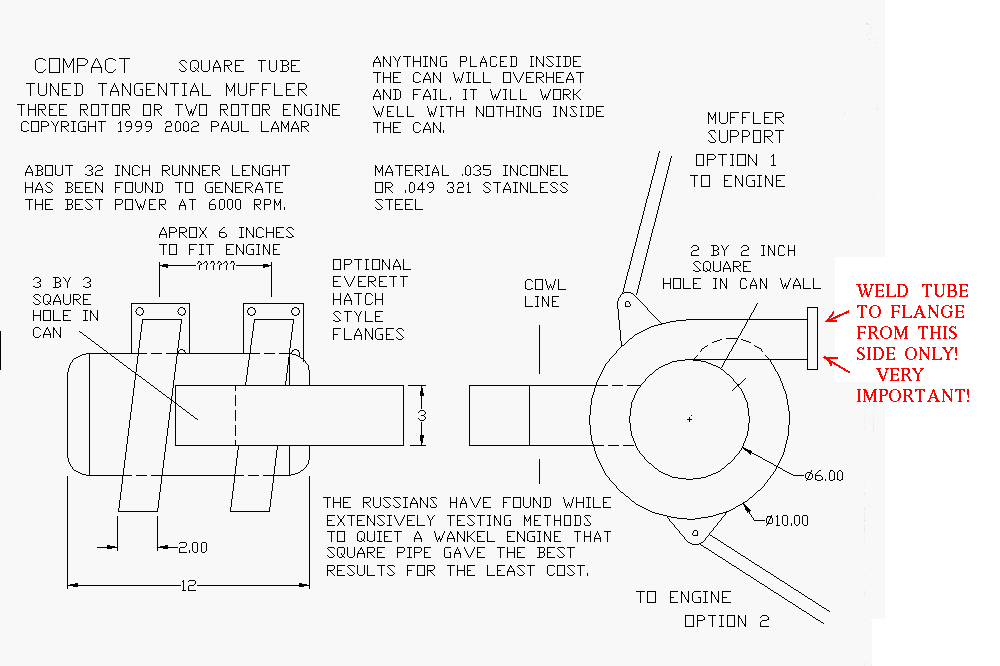
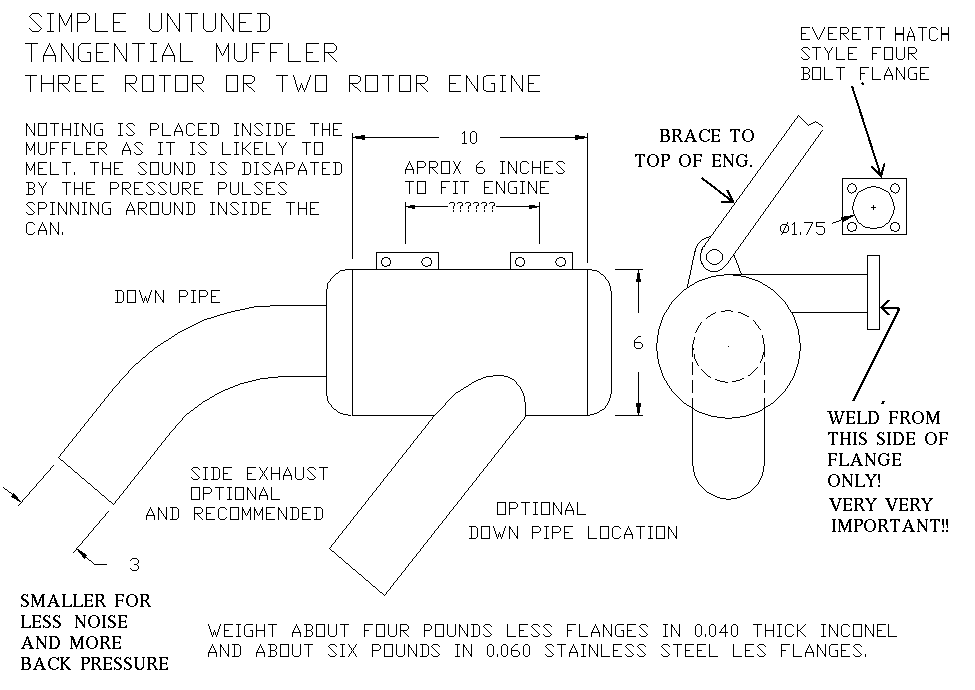
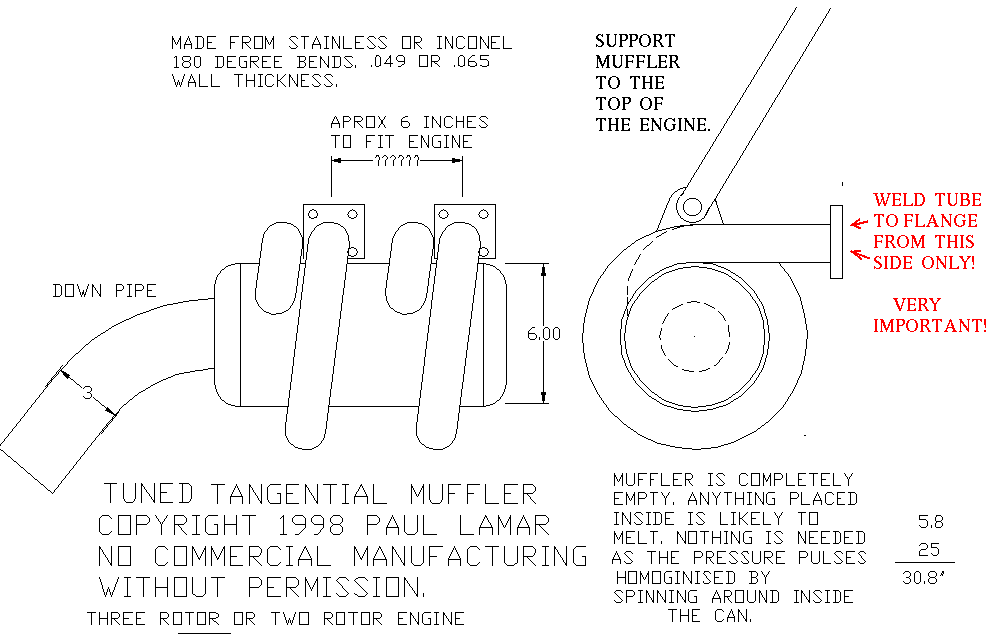
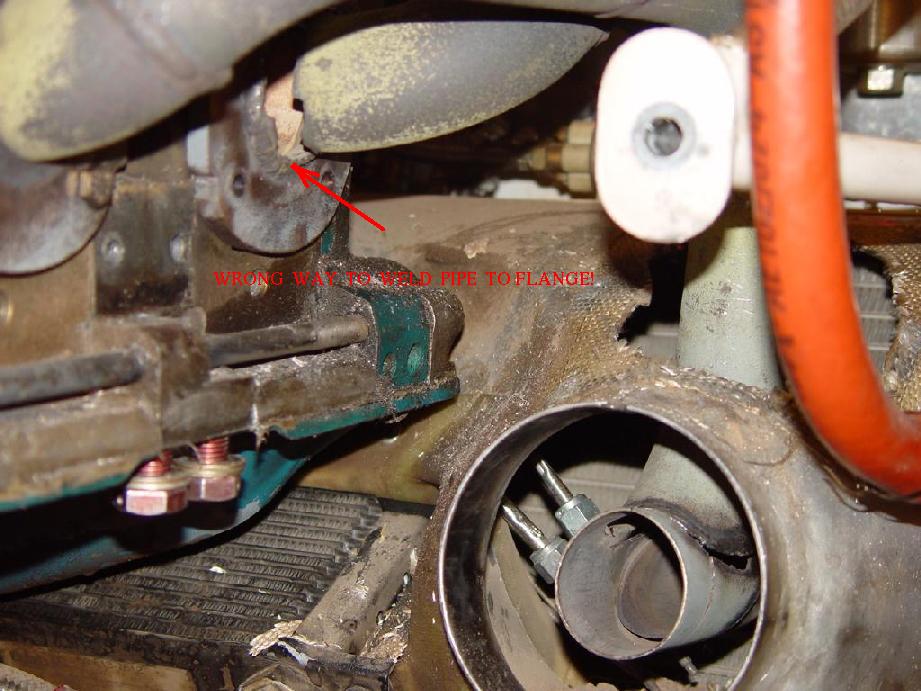
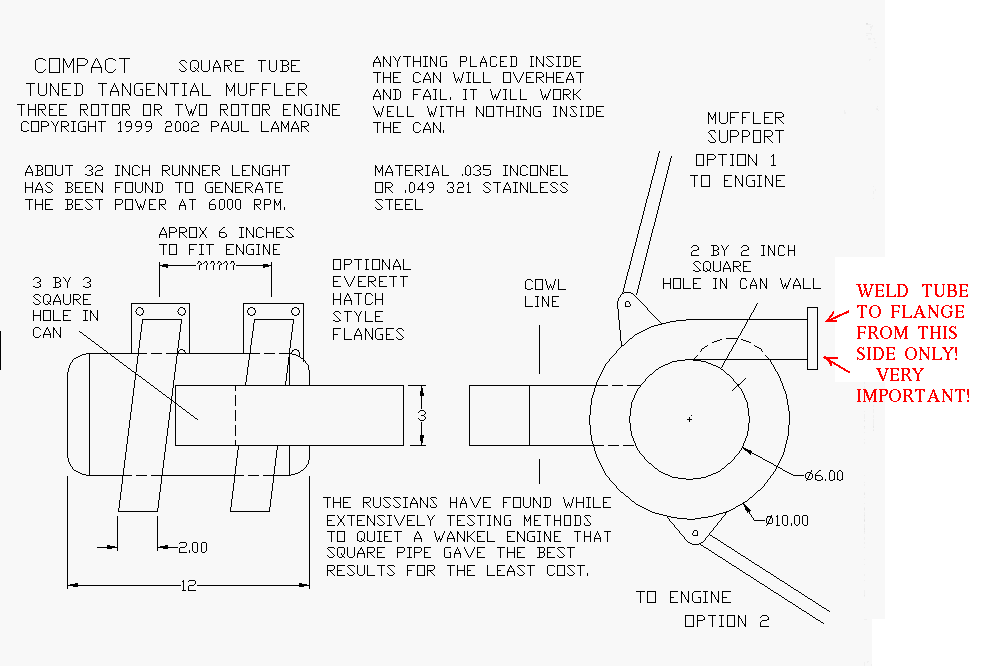
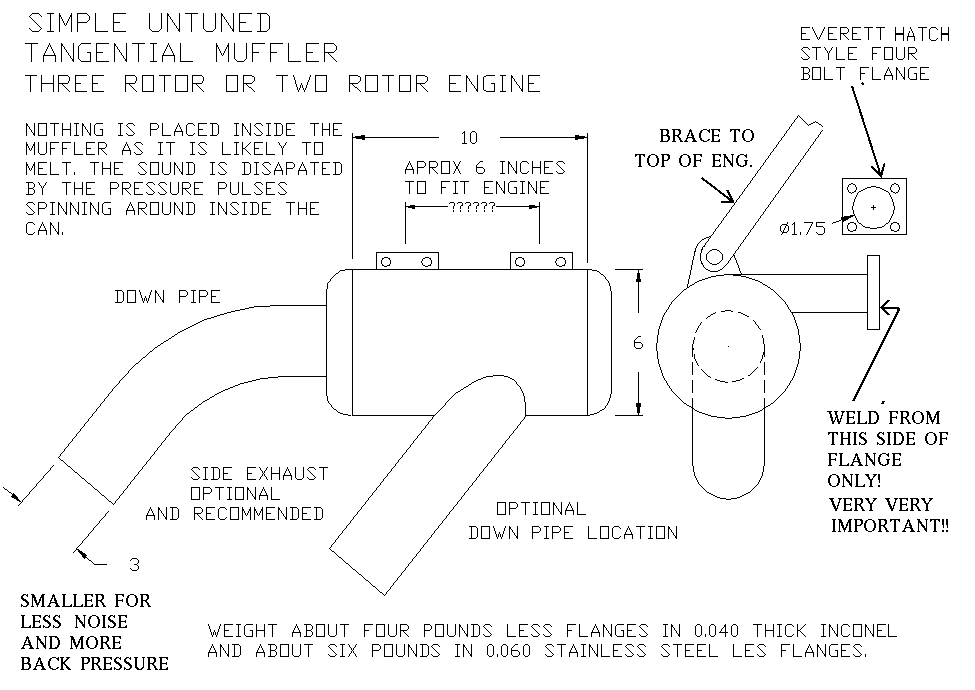
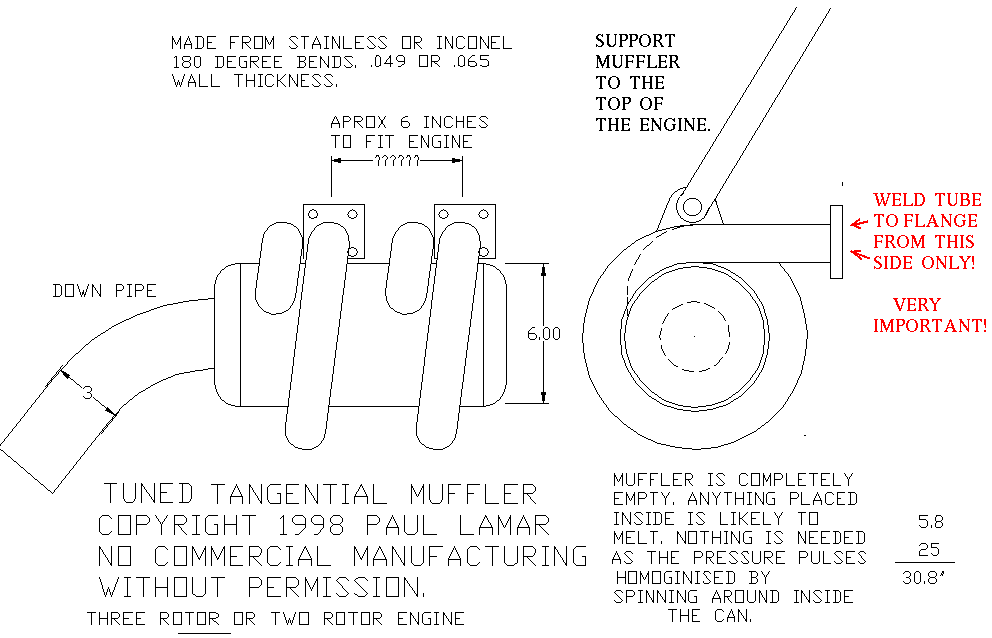
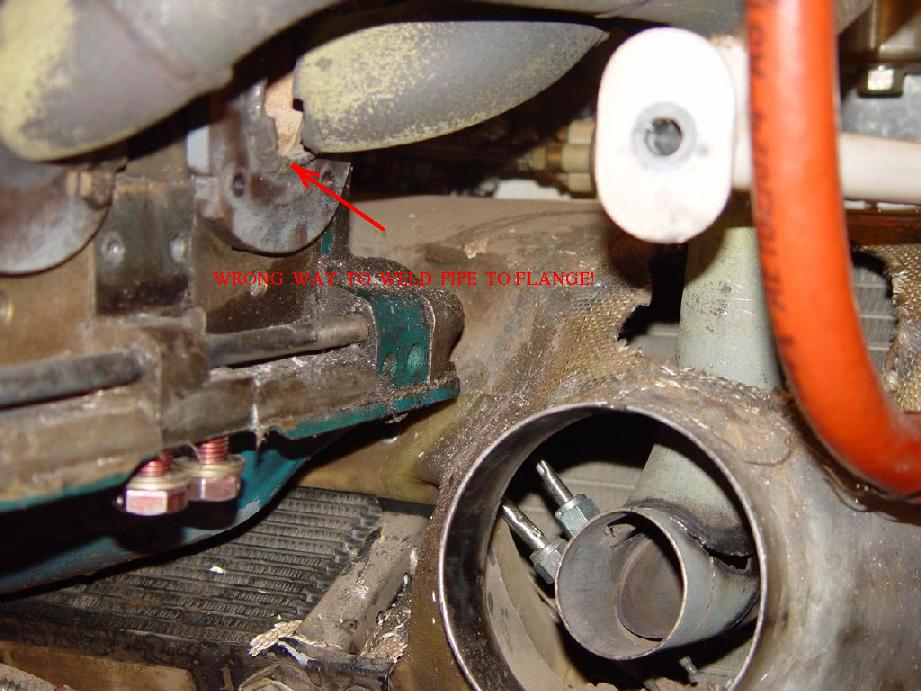
We have found and the car racers have found, a fillet weld on the outside causes
the exhuast tubes to crack just beyond the weld in the heat affected zone.
Paul Lamar ...No rotor no motor.
The Rotary Engine NewsLetter. Powered by Linux.
ACRE NL web site.
http://www.rotaryeng.net
Copyright 1998-2006 All world wide rights reserved.