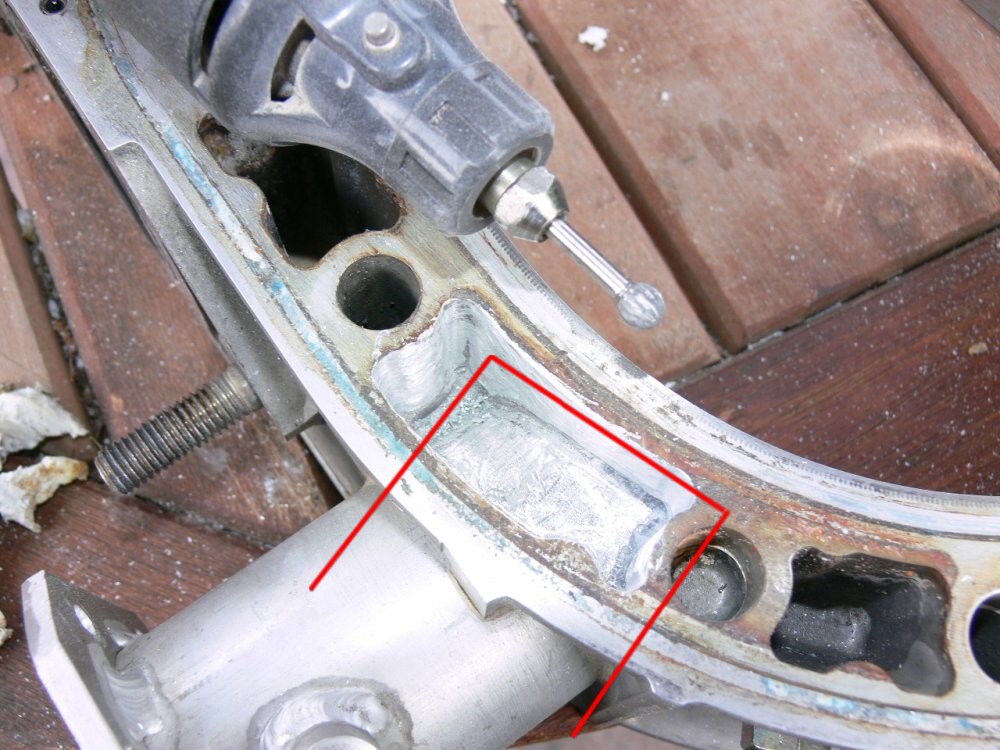
I just came up with an idea that eliminates the small hole.
Here are a couple of pictures of the problem area.
This is the other side of the rotor housing from that
side I repotted on Marks engine.
Just clean this area up with a die grinder and hand cut
a chunk of aluminum that just slips in. Bond it in with
JB Weld BEFORE you cut the hole for the tube. Problem solved.
It won't help Marks engine but the Stainless steel sleeve
will do the same thing.
--
Paul Lamar ...No rotor no motor.
I have been watching this thread with great interest as I also intend to
P-port my engine (to be installed in a BD-4).
Many pictures I have seen of P-port engines have the port cut at an angle
that more closely matches the angle of the trochoid. Would it be possible
to bore the hole at an angle such as this and still get the port timing
needed for our application? This would allow a stepped bore without a gap
that needs filling. The insert could then be a press or slip fit and still
have the surface area to eliminate the possibility of leaks.
Bryan
Yes Bryan but I will not guarantee you will get the same
power as the Lemans engine that had a straight in bore more
or less. I don't expect it will be very much different however.
--
Paul Lamar ...No rotor no motor.
The Rotary Engine NewsLetter. Powered by Linux.
ACRE NL web site.
http://www.rotaryeng.net
Copyright 1998-2006 All world wide rights reserved.