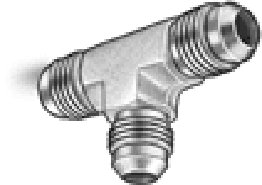
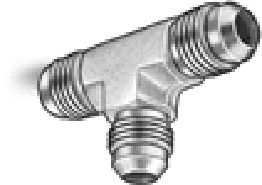
Take one of these 316 SS 1/8th Tee and grind or machine off
the threads on the left and right side so they slip into
two pieces of SS tubing. Drill in from the right side with
a larger drill to form a needle seat just to the left
of the top outlet fitting. The ID of a 1/8th jic flare fitting like
this is .175". The OD at the root of the threads is .35".
So a drill about .25 would be about right. Fuel comes out
the bottom of the fitting and goes to the slide throttle spacer.
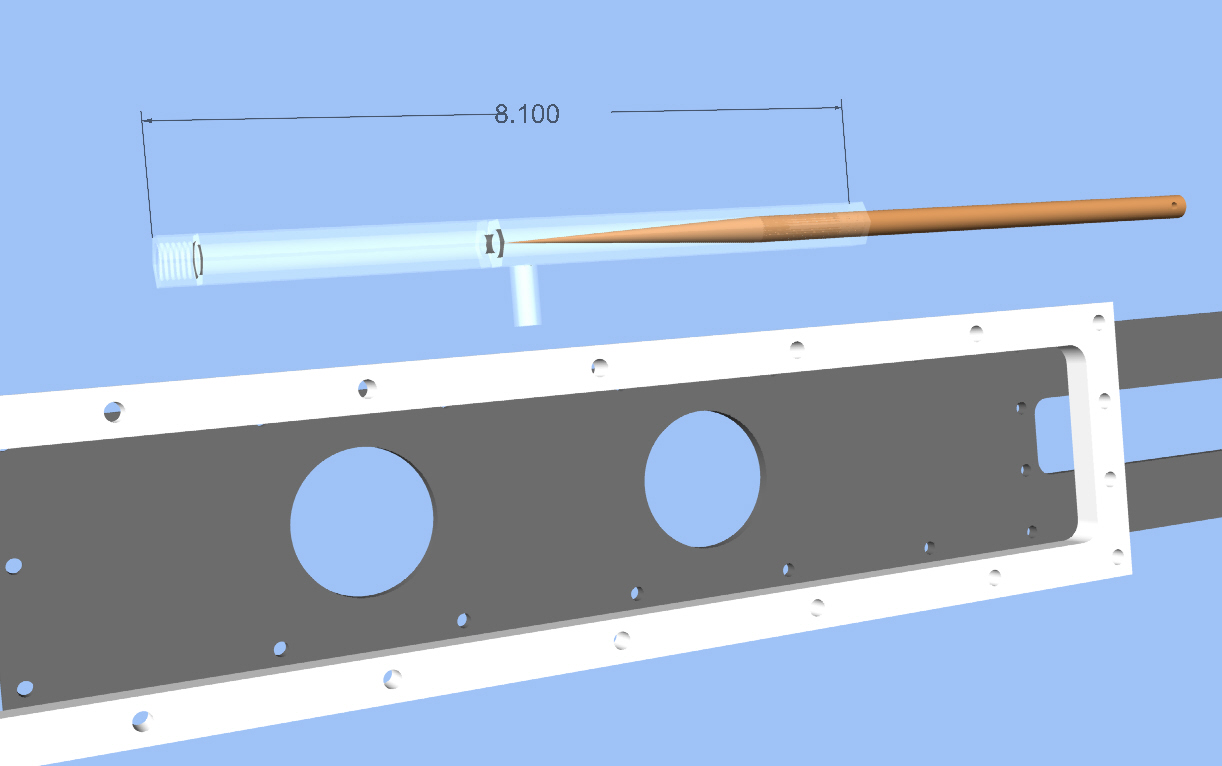
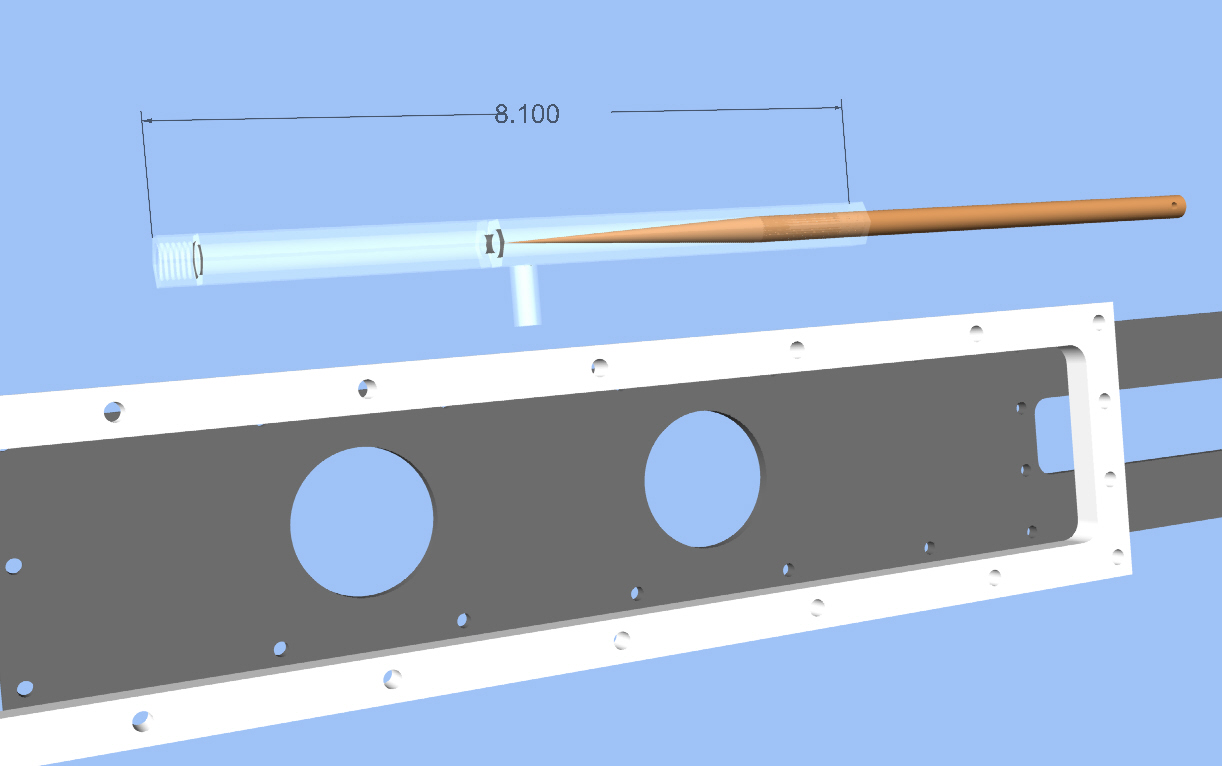
The left tube will be about three
inches long to store the needle when the valve is closed
and hold the input fitting on its left end. Male or female
your choice.
The right tube will be about 5 inches long to accommodate
the needle when it is fully open. There are O ring grooves
in the needle to seal the needle inside the right SS tube.
The total length of the SS needle is about six inches long.
The end of the needle is drilled and taped for the 10-32
vernier leaning cable end.
Tig weld the tubes to the T or use JB Weld. JB weld is good
to 4000 psi so a a fitting .35 OD and .5 inches long will
have a separating force of about 2200 pounds. More than enough
for a low pressure 2 psi fuel system.
BTW 316 SS is easy to machine unlike some other SS alloys.
Paul Lamar ...No rotor no motor.
The Rotary Engine NewsLetter. Powered by Linux.
ACRE NL web site.
http://www.rotaryeng.net
Copyright 1998-2006 All world wide rights reserved.