We cut another P-port today. I was going to try a Starrett 1-7/8" carbide
hole saw
to speed up the process but found the hex arbor would not fit in the
Bridgeport
mill using a chuck. We had the knee all the way down. It requires a hex
3/8th 5C collet
to fit in the mill above the rotor housing. I'll order one so we can use
it the next time.
I am planning on having Mazdatrix building up a p-port RX8 engine to see
how much power
it has using the Mazdatrix dyno.
Another alternate way is use a 3/4" shank 1-3/4" drill. Rather expensive
at around $80.
That also requires a one inch drill for the initial hole.
I am going to use this junk rotor housing as a test piece to see if the
tig welded 2" SS
intake tube works. We will try to tig weld the tube to the steel trochoid
liner. BTW the steel liner is hardened. We tested it with a file. I was
surprised. I
previously thought it was mild steel.
Jim Poole did the machining and he was a bargain at $35 an hour.
If you don't want to do it yourself Jim has done five so far so he is
getting
good at it.
This may also be done on a medium size lathe if you lay the rotor housing
on its side on the cross slide and using a boring head in the head stock.
Paul Lamar ...No rotor no motor.
We are getting ready to p-port a junk housing.
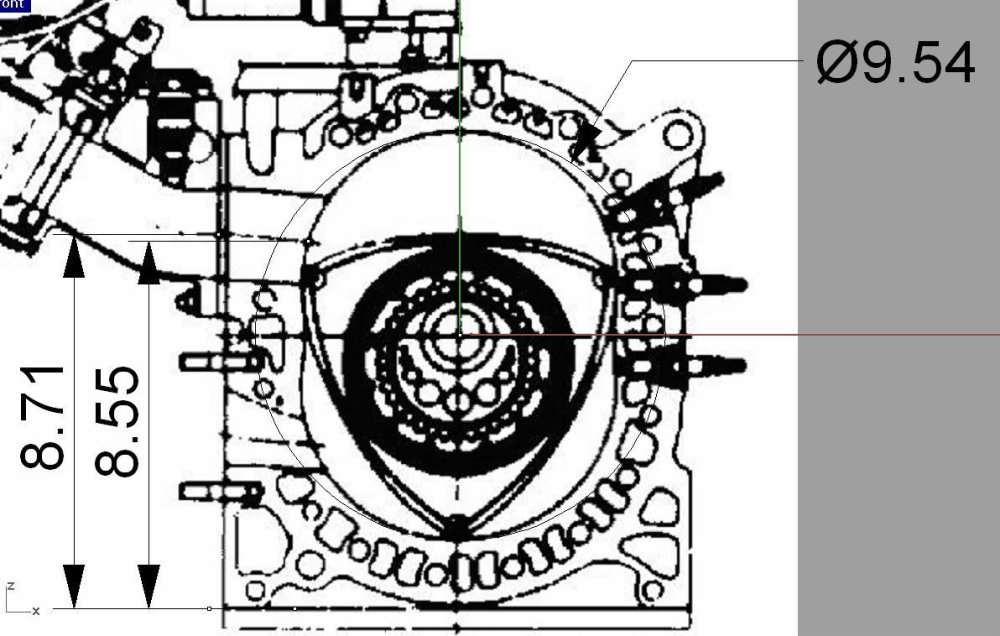
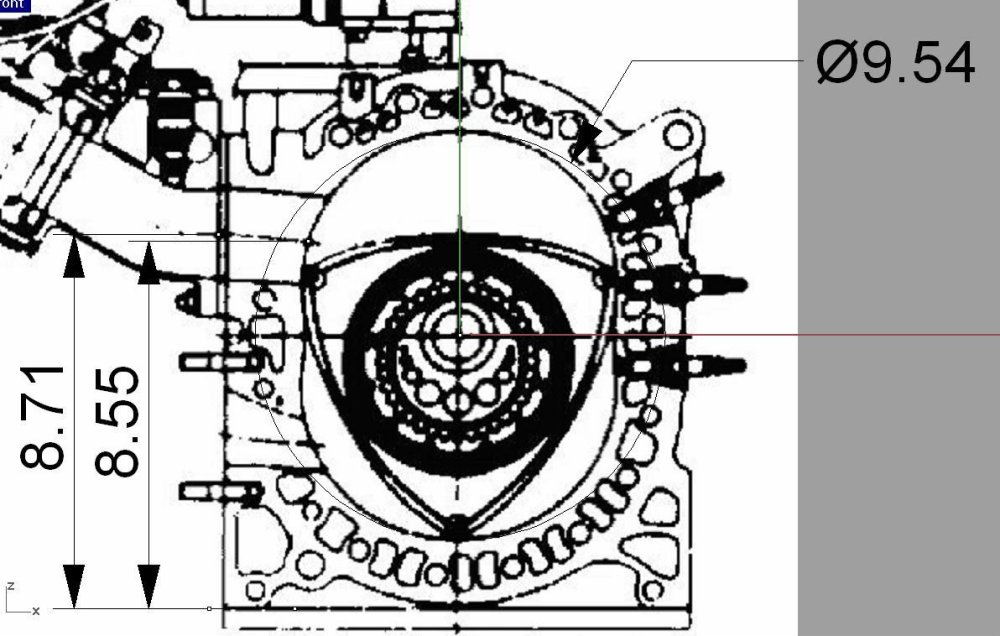
I notice that the hole is somewhat off center to the boss cast into the
housing in the direction of the exhaust port. How far should this distance
be?
Doc Custer
Retired Software Engineer and sometime Audiologist
From the bottom of the rotor housing it is 8.64 inches.
Paul Lamar ...No rotor no motor.
The Rotary Engine NewsLetter. Powered by Linux.
ACRE NL web site.
http://www.rotaryeng.net
Copyright 1998-2006 All world wide rights reserved.