I just had an idea that will take a lot of the technical risk
out of welding in SS P-port tubes.
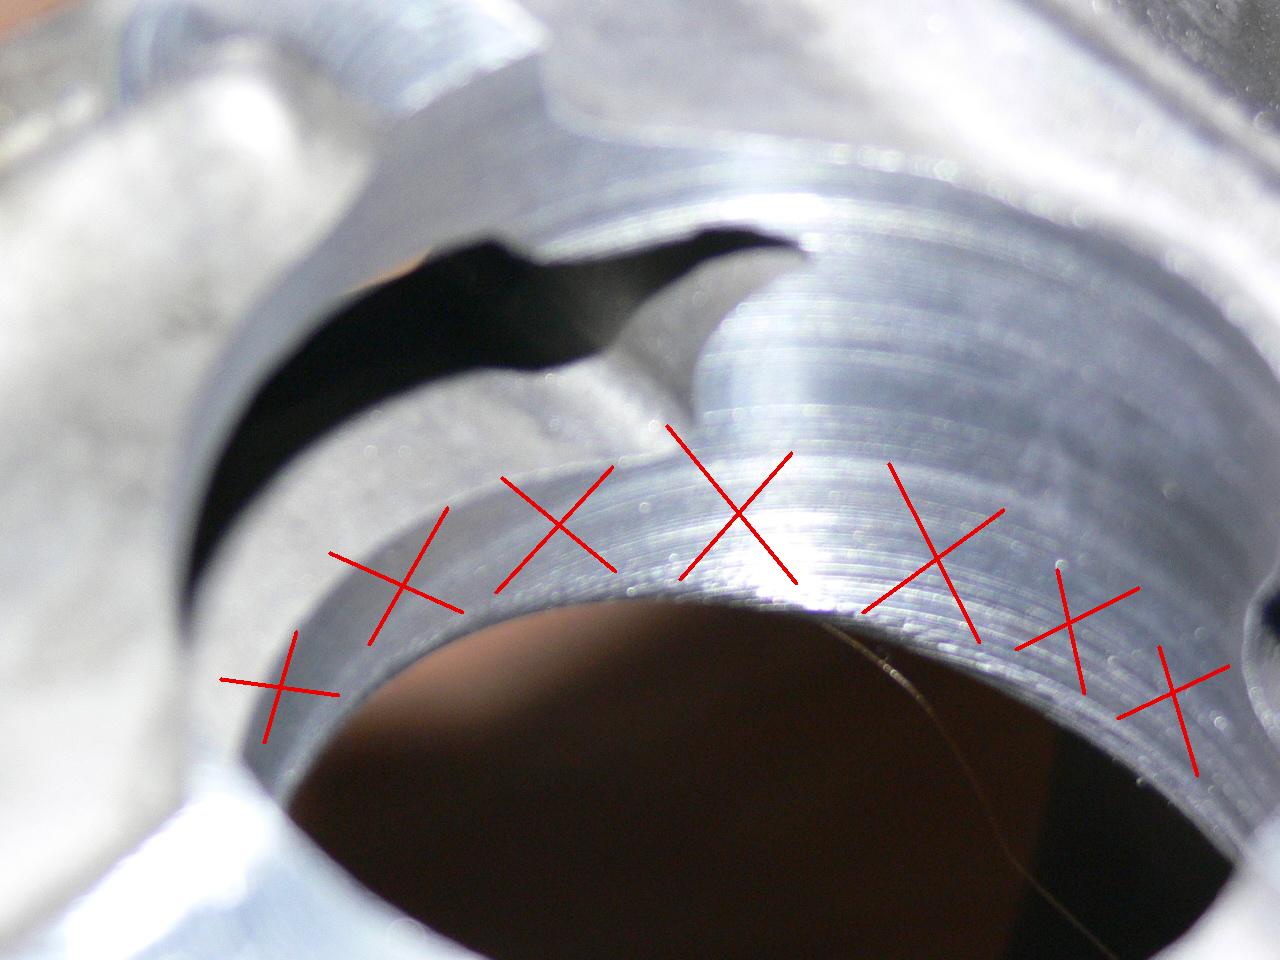
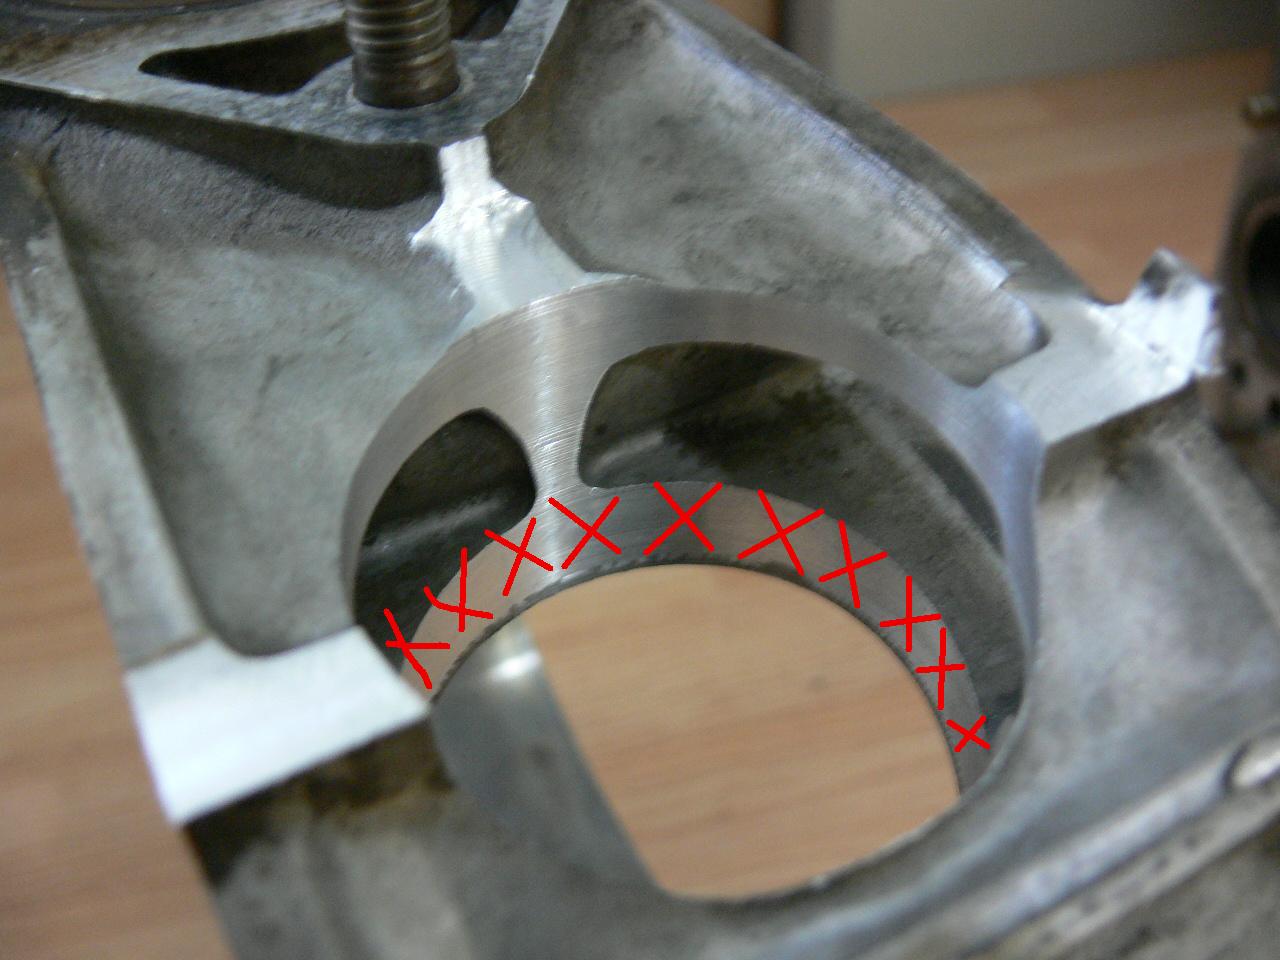
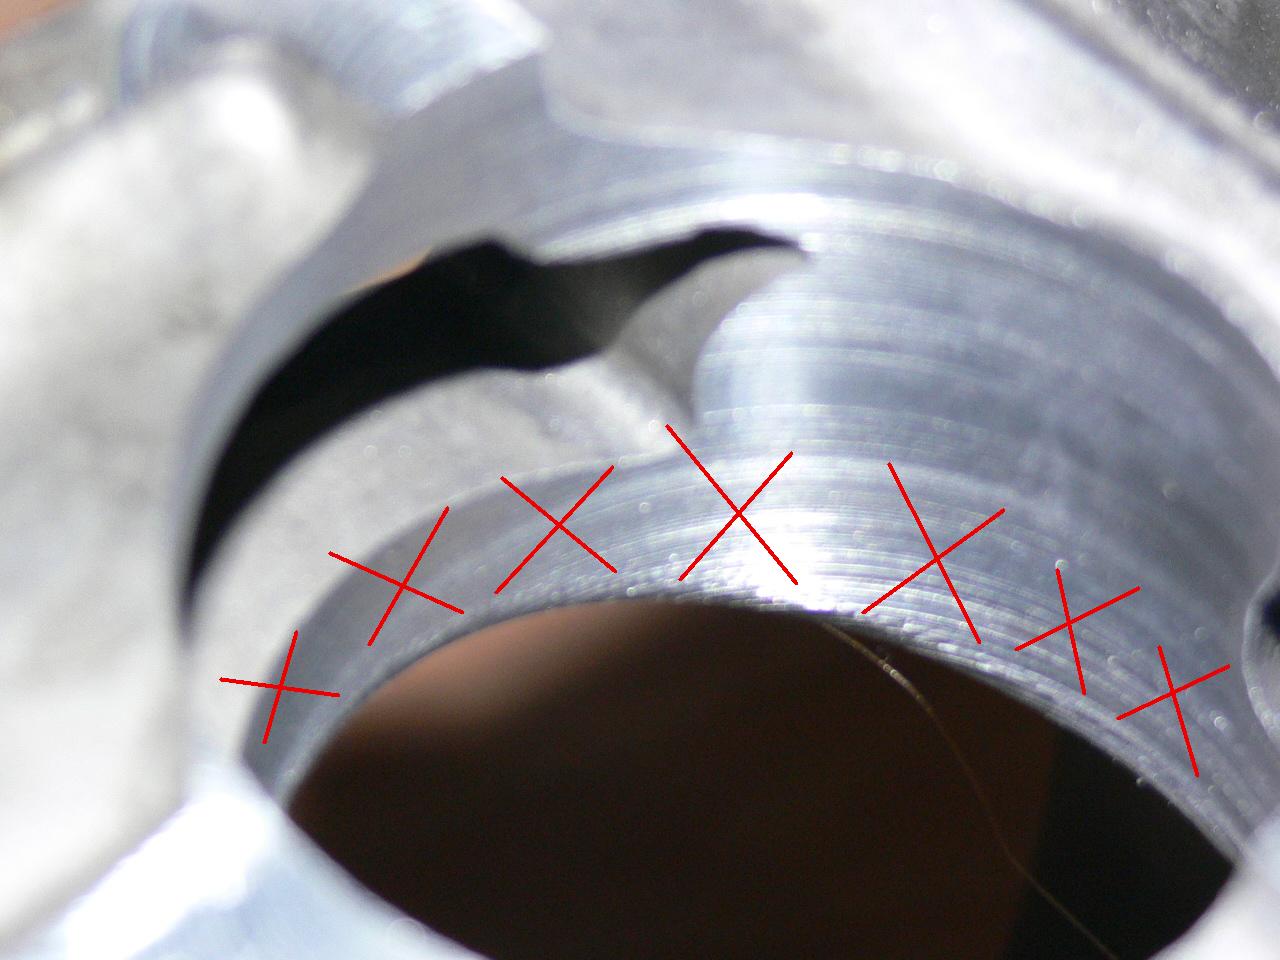
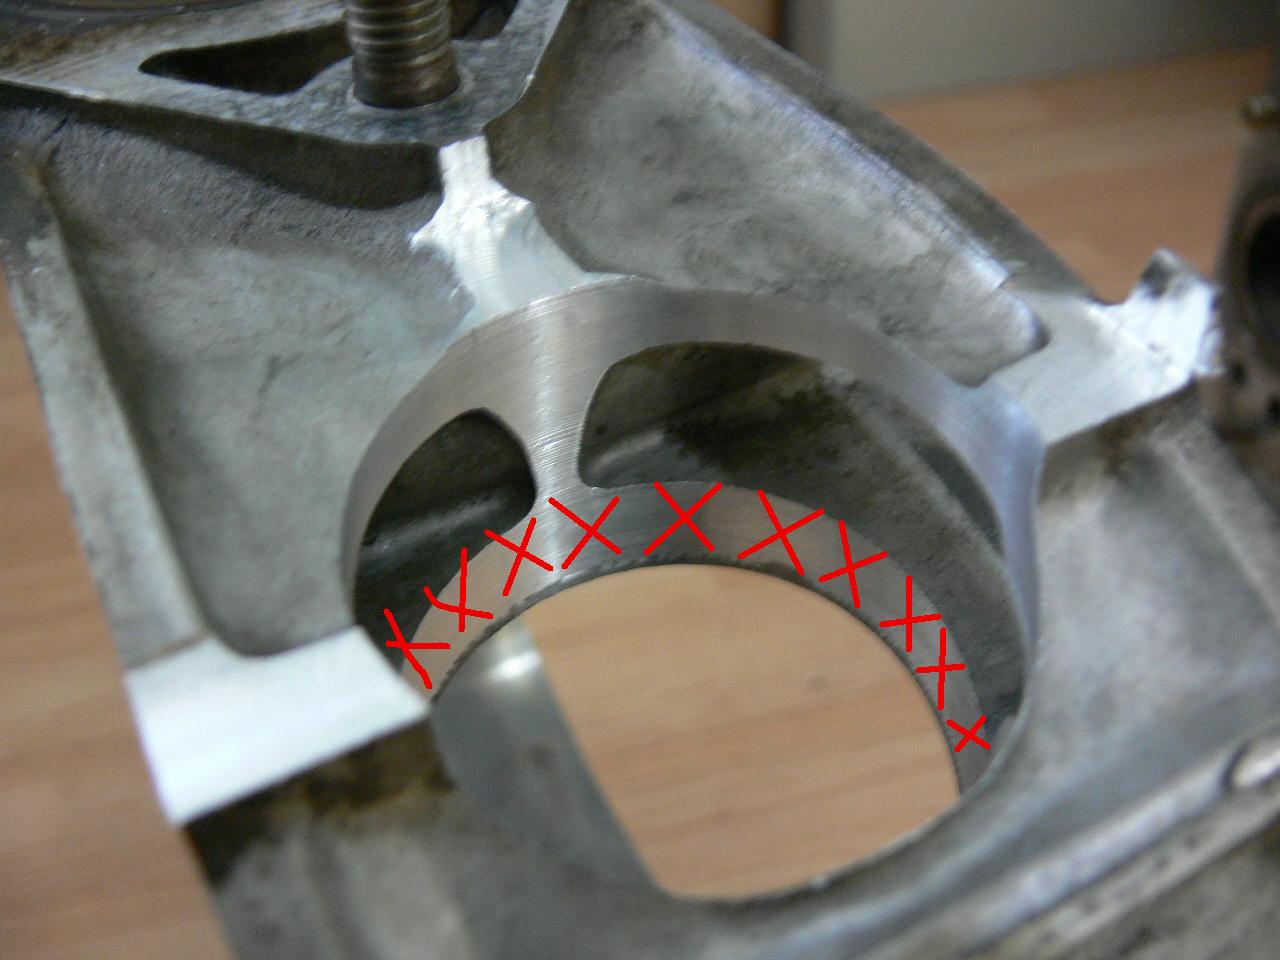
The procedure is; remove the aluminum back about 1/4 inch all the way around
the inside of the water jacket next to the steel liner. See the photos.
This will cut down on the tig welding heat required to weld in the SS tube
to the steel liner. Normally a lot of welding heat would be conducted away by
this aluminum or worse melt the aluminum. This aluminum will be replaced
by JB Weld when finally potted. The unsupported steel liner is not
a problem in this area in this area of the rotor housing as pressure
is very low to near zero.
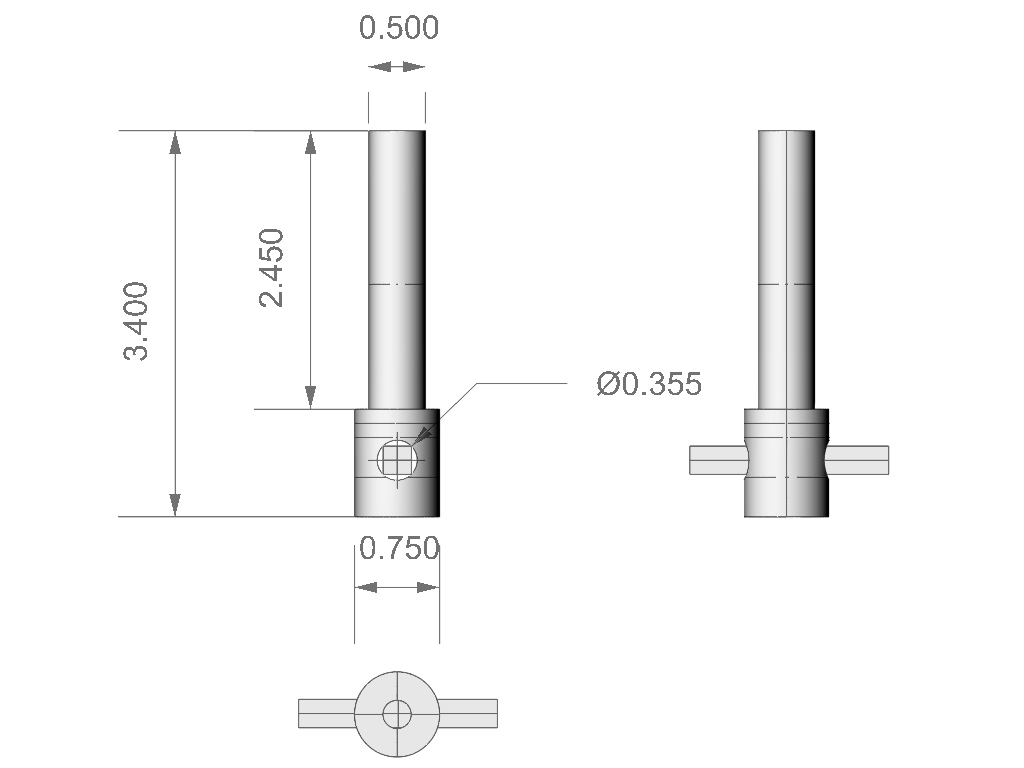
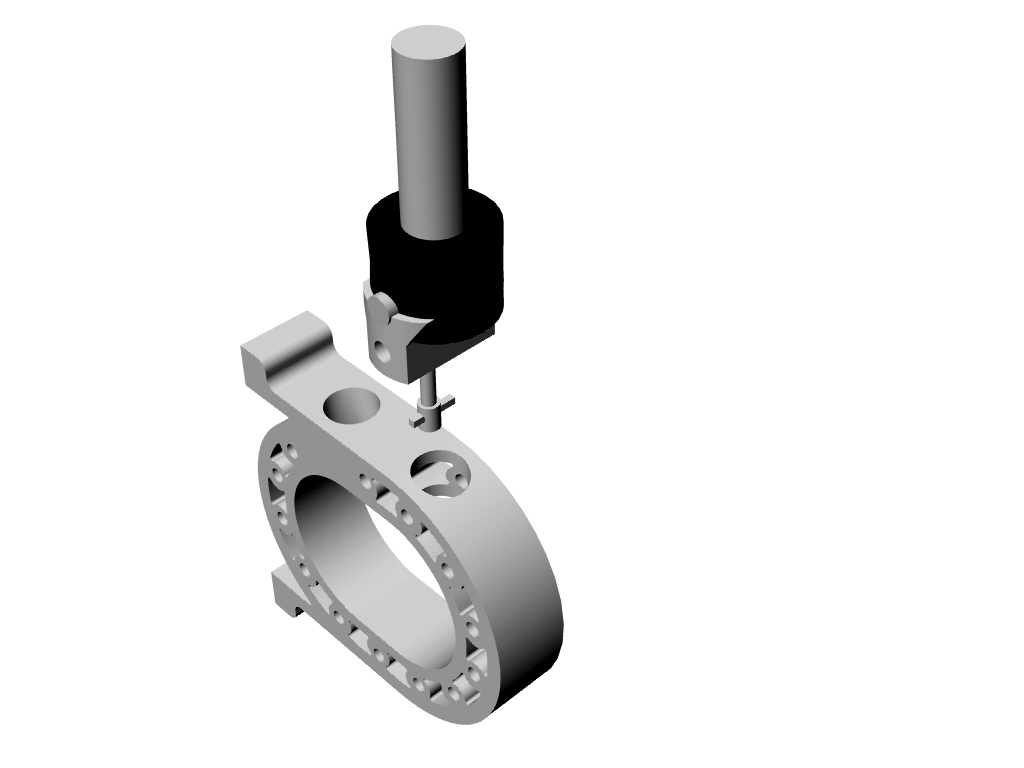
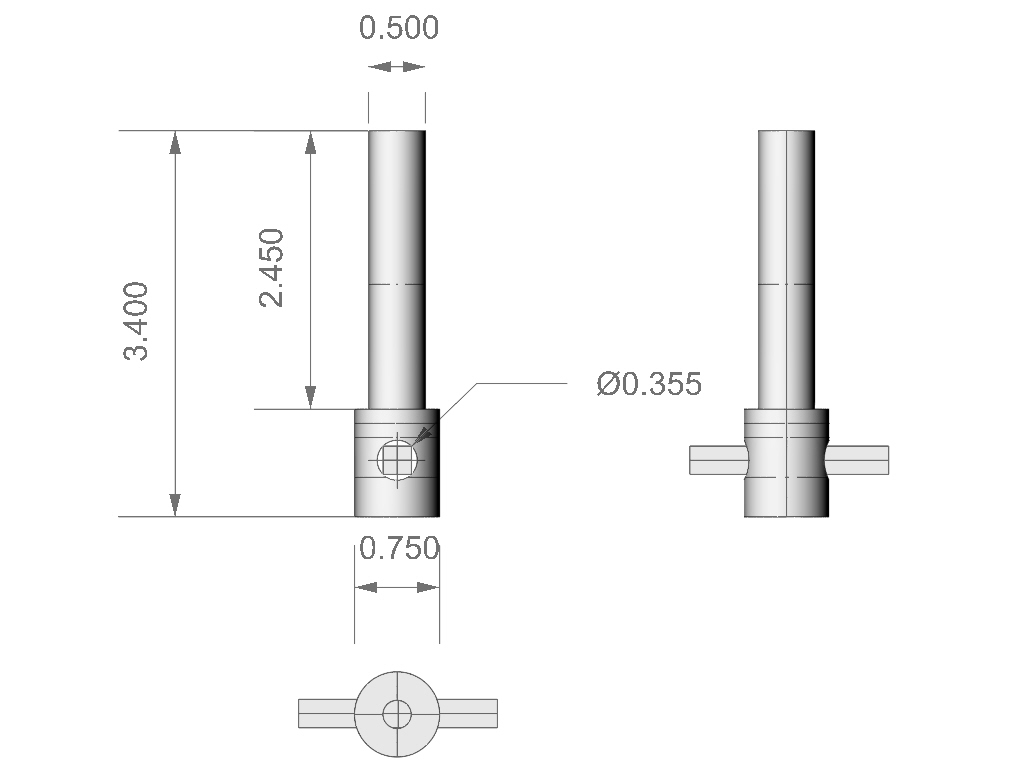
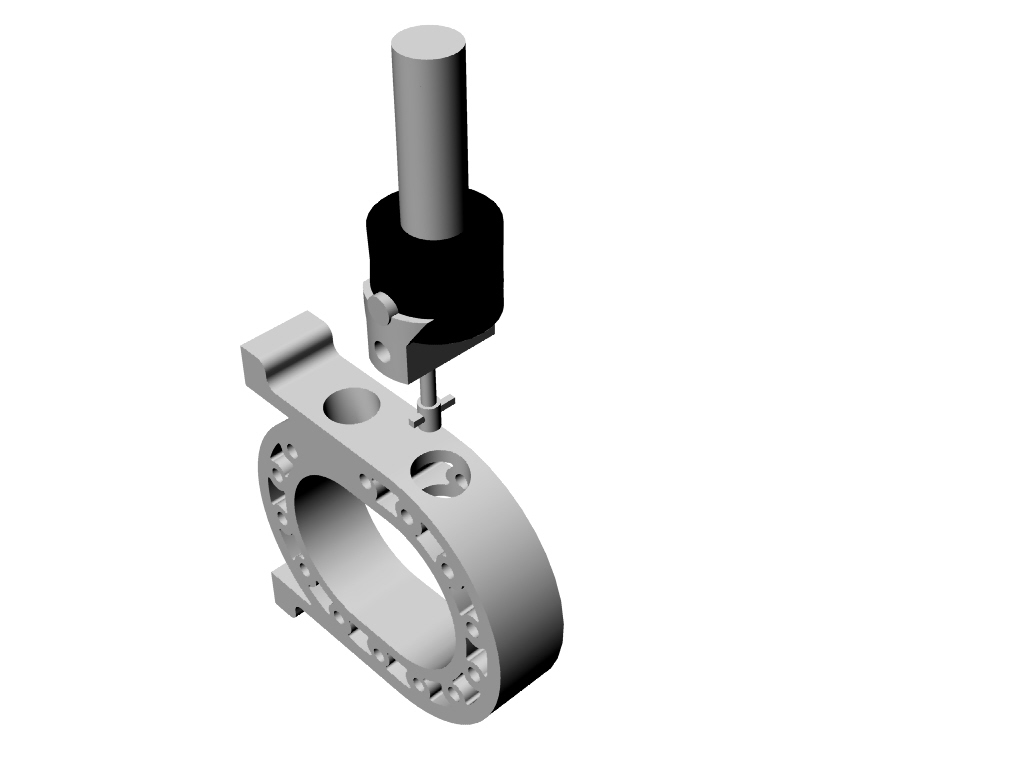
This is a peice of cake if done on a mill using a special cutter mounted
in a boring head holding an ordinary 1/4 inch lathe tool bit. See the 3Ds and picts.
Some clean up will be required using a die grinder.
It can also be done by hand with a die grinder.
For those new people on the list P-ports are good for 40 to 50 HP
more at 6500 to 7500 RPM range.
Paul Lamar ...No rotor no motor.
The Rotary Engine NewsLetter. Powered by Linux.
ACRE NL web site.
http://www.rotaryeng.net
Copyright 1998-2006 All world wide rights reserved.