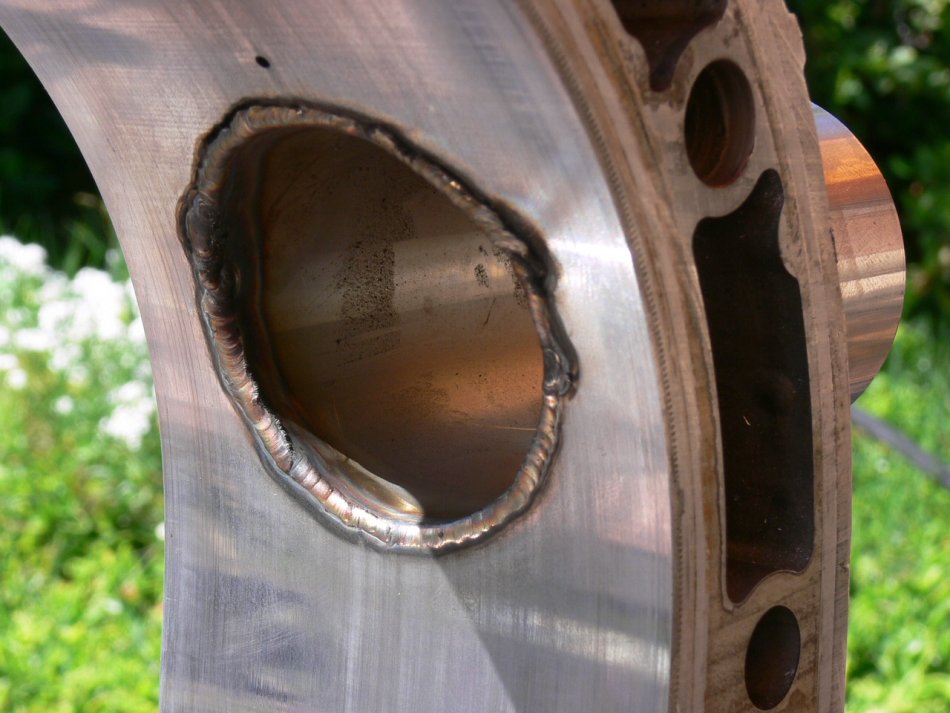
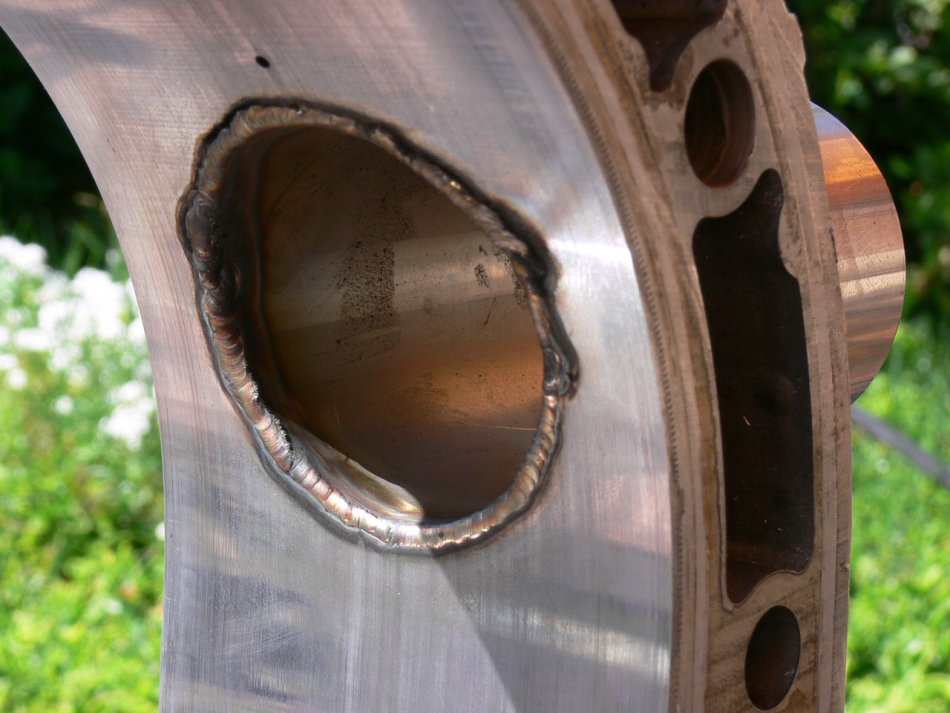
This was done by Matt who is the race car chassis builder
at Mazdatrix. It had some aluminum removed around the
steel liner where it was welded to the 304 SS .065 wall tube.
As Mark Steitle discovered this is totally unnecessary.
Removing aluminum is difficult to do and labor intensive as compared
to just welding it in.
It took Matt about five minutes to weld this and I paid him $22 bucks.
Welding them in is not completely necessary but it gives another
level of security against coolant leaks.
Sure is quick and easy to do. I am going to do it on
the RX8 P-port engine.
Paul Lamar ...No rotor no motor.
Paul,
How do you get the trochoid surface back to a smooth and bump-free
contour?
Bill
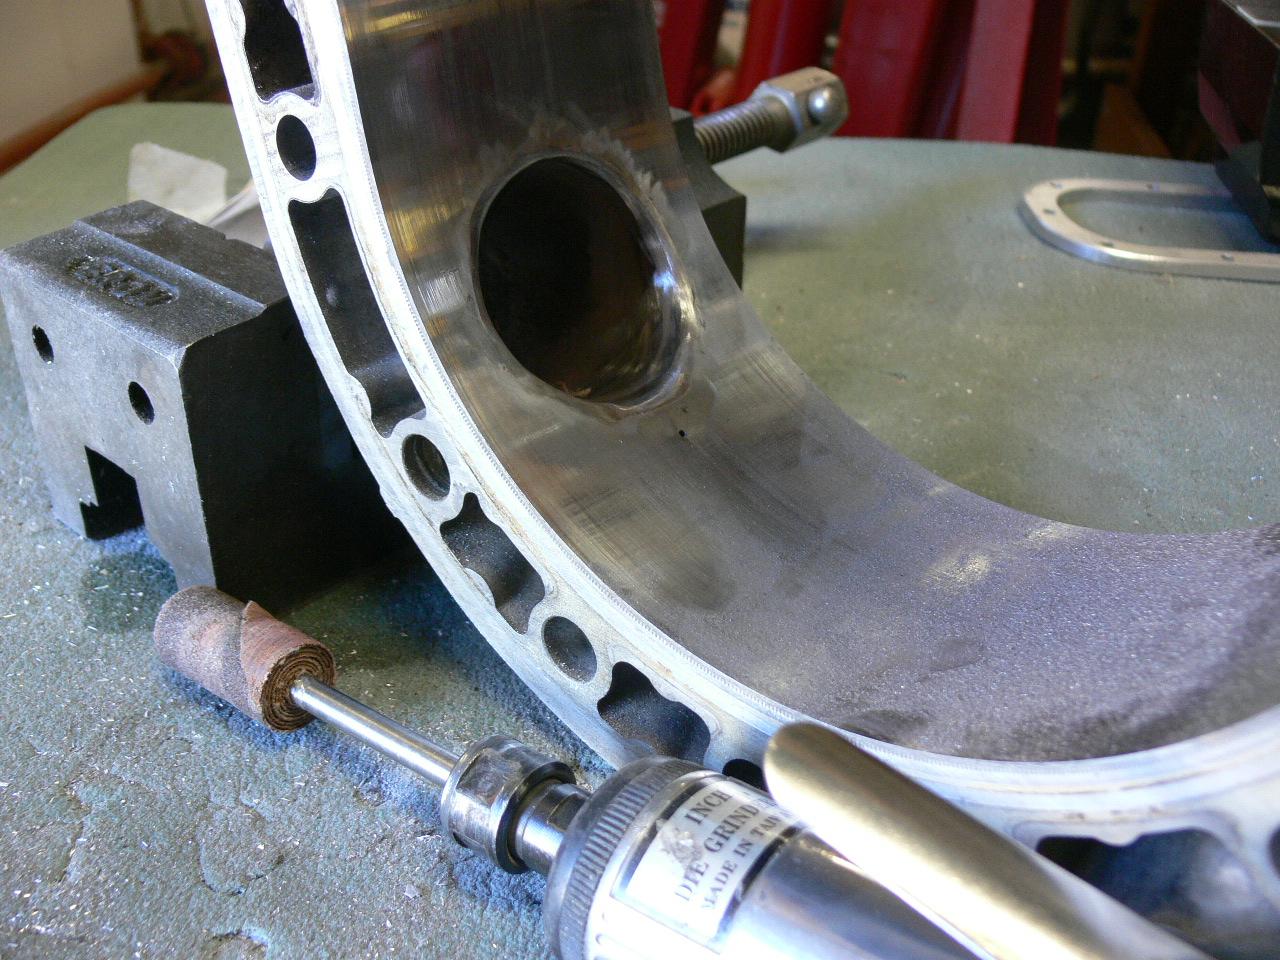
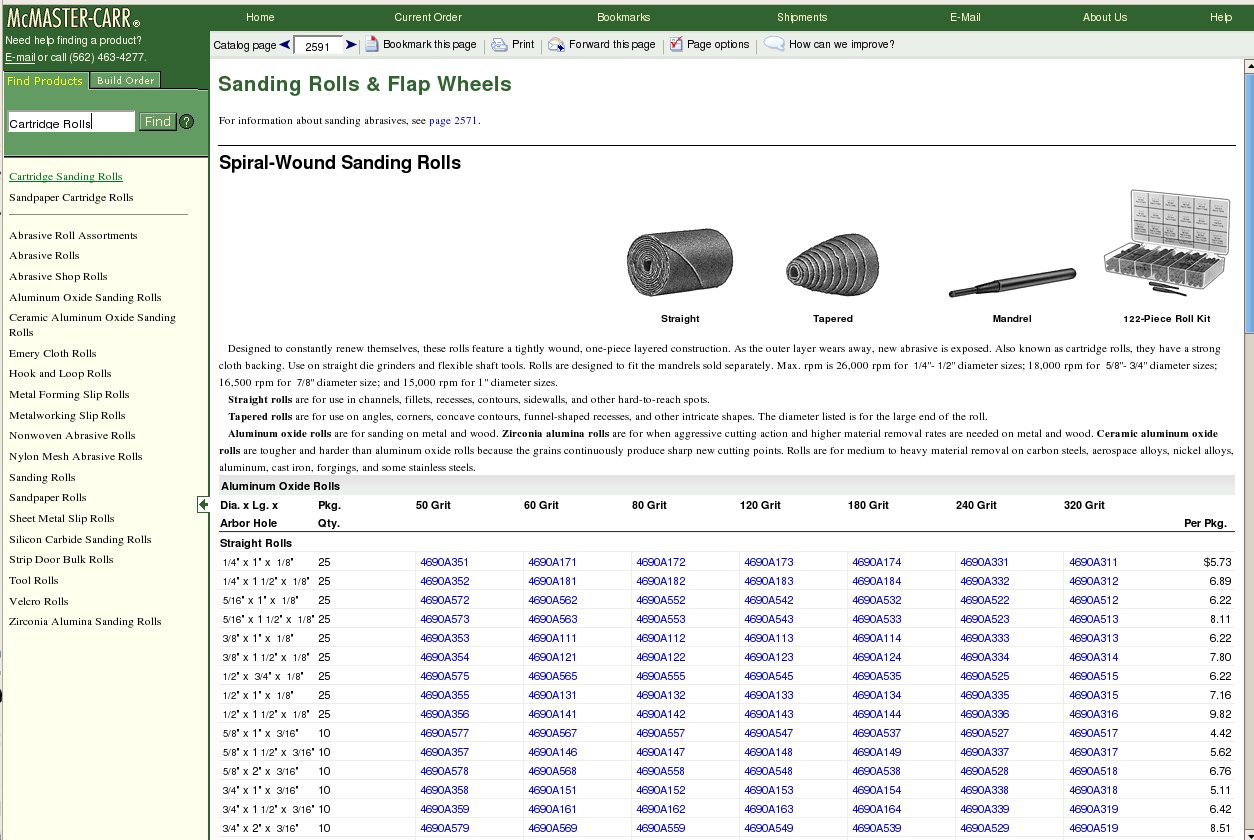
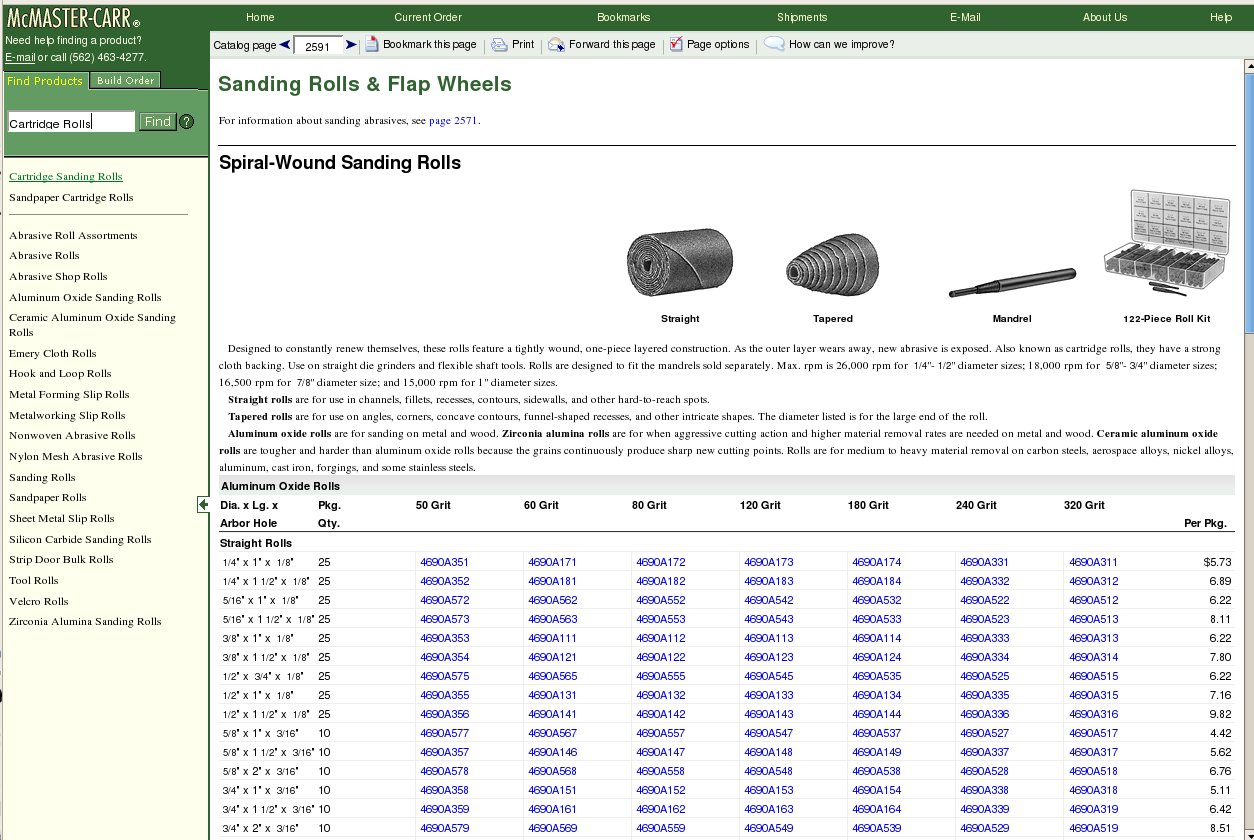
Use a dia grinder with sand paper spiral rolls. They are cheap and
work great. Start with course and finish with fine for a glass smooth
surface. Here is the Mc Master page. Don't worry if you grind
through the weld. The JB Weld will take care of the tiny leak.
These things will make an expert out of anybody on porting.
--
Paul Lamar ...No rotor no motor.
Bill,
It doesn't matter if it's a little low around the hole, the apex seal will
just drift over the top being supported by the ends. As long as it's not
high and hang up the apex seal.
George ( down under)
Right you are George.
Use bluing AKA Dykim on the end of the tube. Let it dry. Insert it in the hole and
uses a scribe to mark the tube end shape. Use a band saw or hand held cut off
disk and bench grinder to shape the end of the tube to fit. A .035" wall SS tube
can probably be cut with aircraft snips. Have it tig welded.
This is what I did today in about a half hour or 45 minutes.
Support the rotor housing with a clamp or vice so you can use both hands
on the dia grinder. Use a shorter mandrel than the one shown as that will
give you better control over the spiral roll sanding drum. Use a .035" thick wall
or .049" thick wall SS tube as that gives a smaller weld.
I used .065" thick wall which is over kill and harder to cut to shape.
There will be less weld to sand off and things will go faster.
Use bluing AKA Dykim on the end of the tube. Let it dry. Insert it in the hole and
uses a scribe to mark the tube end shape. Use a band saw or hand held cut off
disk and bench grinder to shape the end of the tube to fit. A .035" wall SS tube
can probably be cut with aircraft snips.
Practice on a junk housing to get your confidences up.
If you want to farm it out John at Mazdatrix has ported hundreds
of rotary engines and I am sure he will be glad to do it for you.
Paul Lamar ...No rotor no motor.
The Rotary Engine NewsLetter. Powered by Linux.
ACRE NL web site.
http://www.rotaryeng.net
Copyright 1998-2006 All world wide rights reserved.