George,
Nice work.
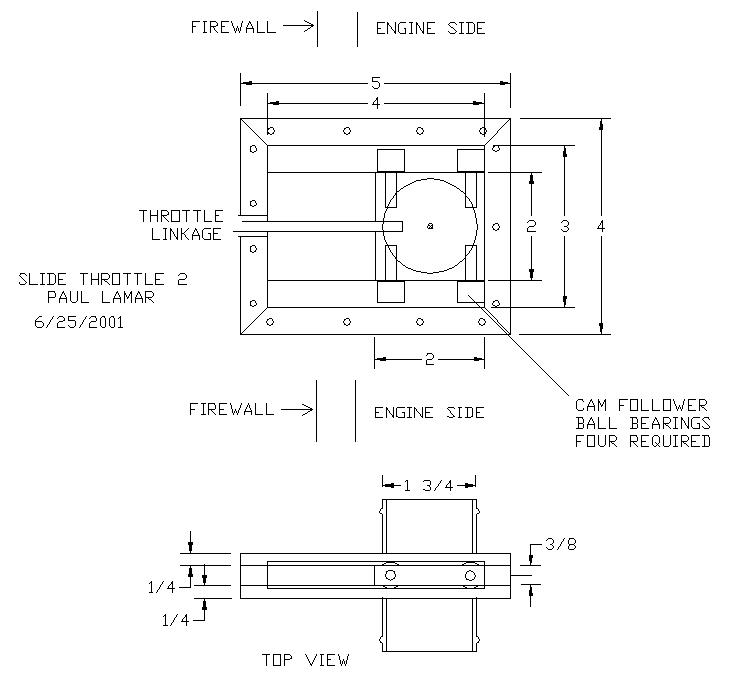
I just finished a design for slide throttles myself and it appears we
think
alike with very similar throttle plate design. I credit you with the
inspiration to use one unit per port. I don't understand the mass of
metal
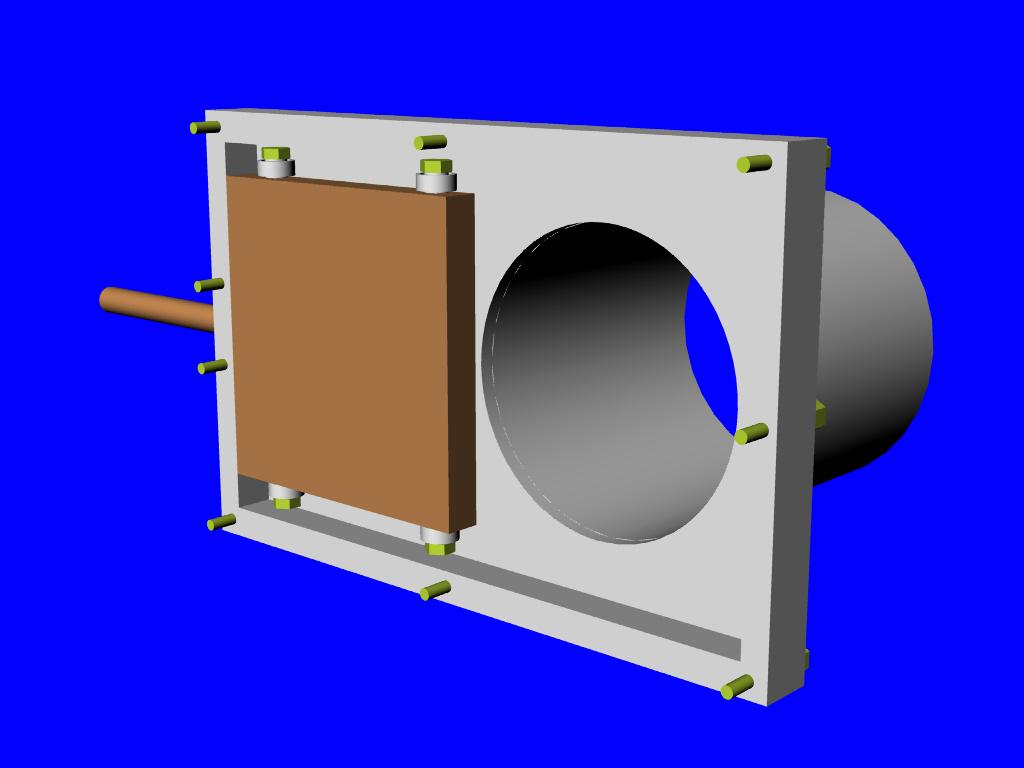
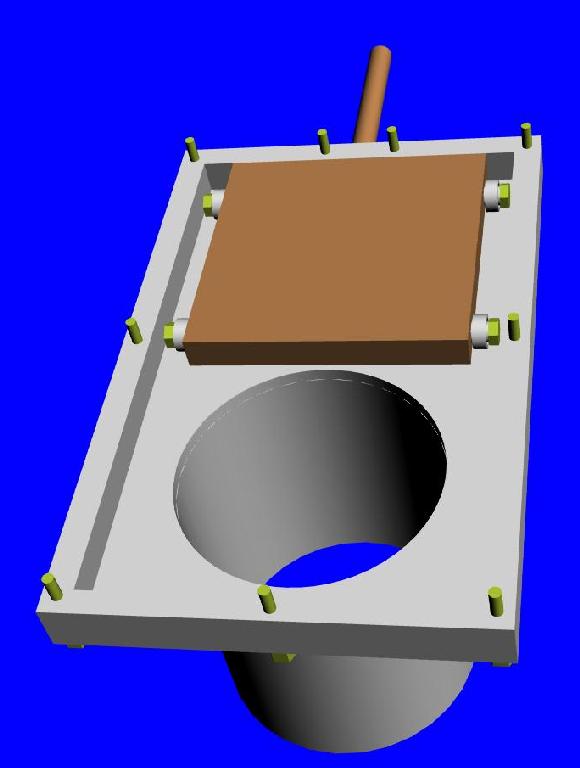
below the port though. I assume those four machine screws on the
throttle
plate are for holding the rollers in place?
Doug in Japan
Doug,
Thanks for the comments - it's the way to go alright, that is making it
yourself if you can't buy what you want.
That mass of metal that you speak of is there to accommodate the depth of
the needle ( rear tapered type). The needle itself is simple to make. Some
of that metal will be for machining (to lighten) and some will accommodate
the an adjustable inlet valve.
I will run a low pressure pump with an adjustable pressure valve with 1.5
to
2 PSI.
My needle will also be adjustable up and down for leaning and enrichening
(from the cockpit).
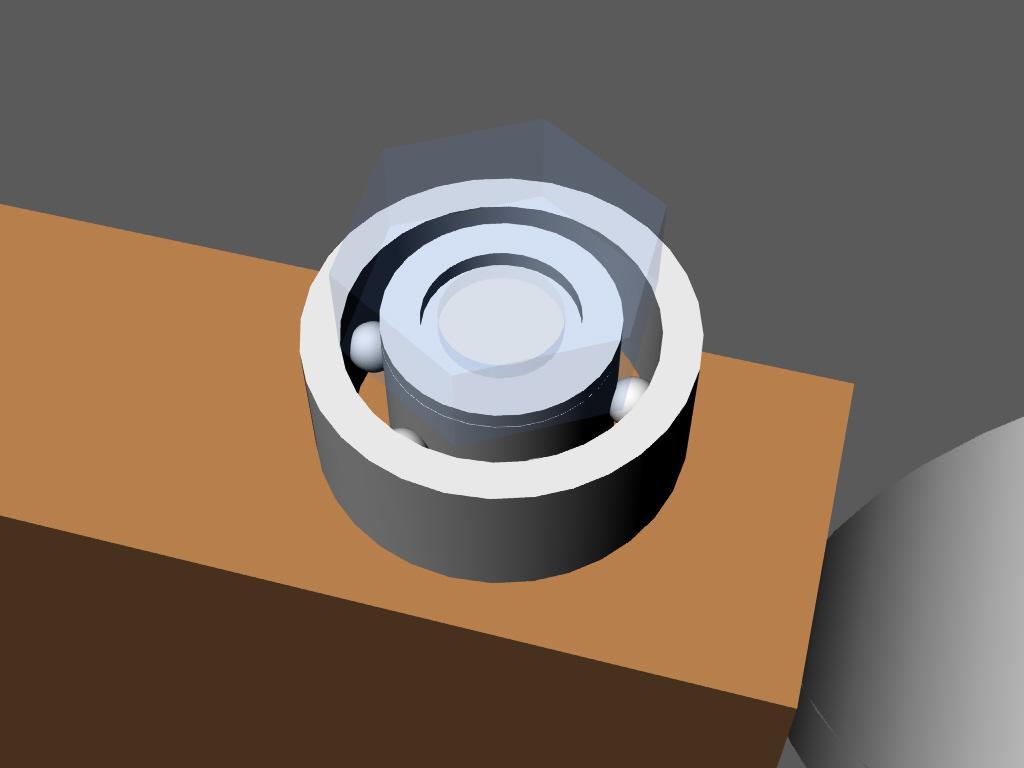
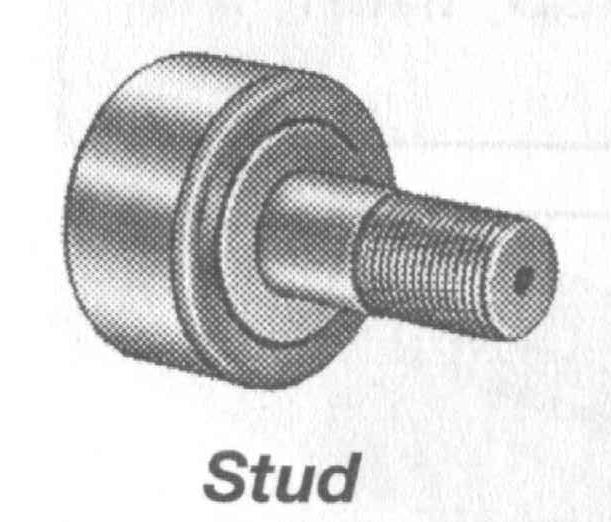
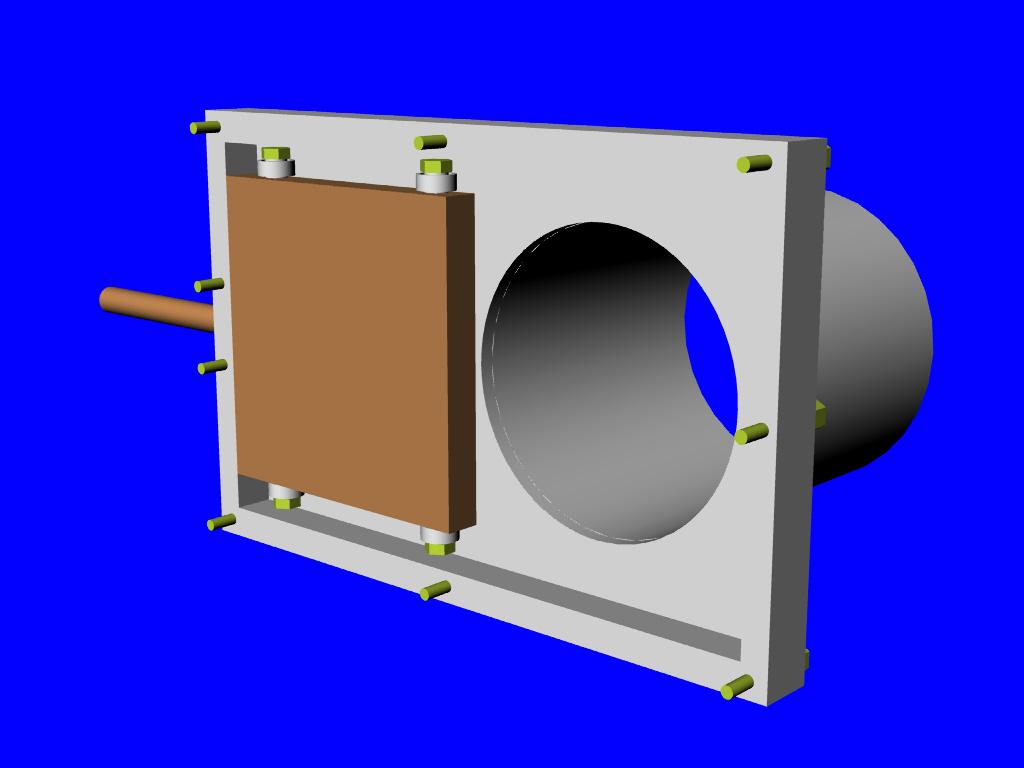
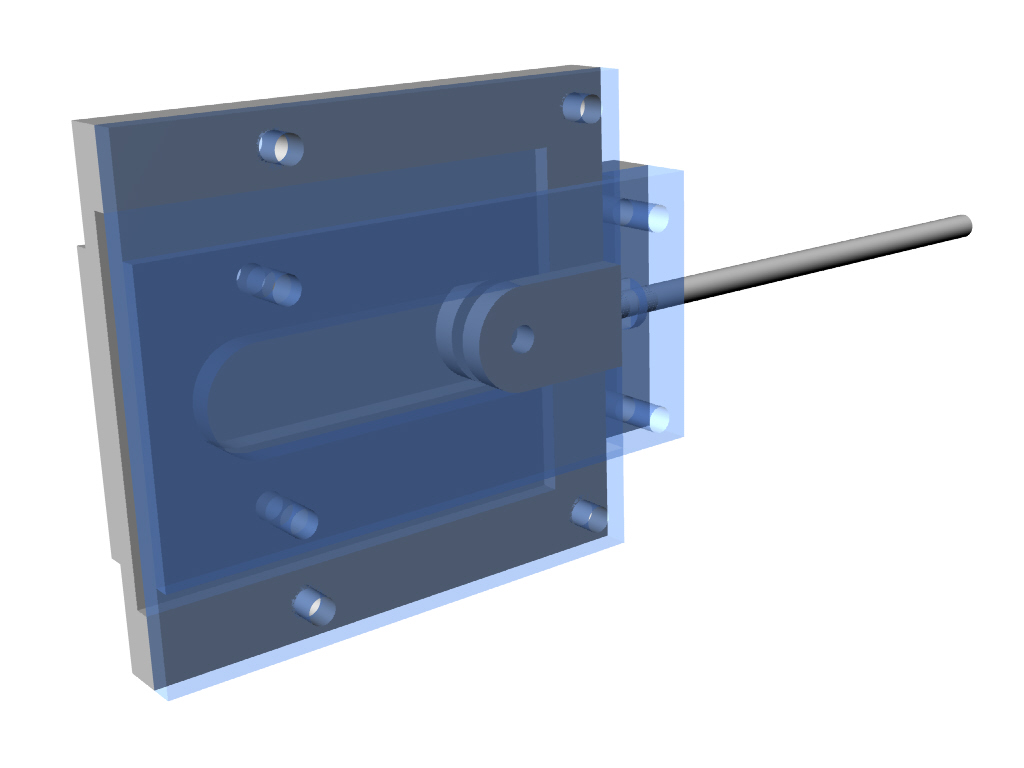
BTW those machine screws do hold the 10mm rollers in place - I have about
.03 to .06 mm rear slide tolerance and about .02mm bearing to side wall
clearance. The screws have a tapered head to precisely hold the bearings
centre. The threads are not cut but formed for strength.
Any suggestions from your end, from what you are planning.
George (down under)
So George what has it cost you so far in terms of machining?
--
Paul Lamar ...No rotor no motor.
Paul,
I'm a bit like yourself, I did it all myself , and although I'm not terribly
skilled, I had to take my time - I have the basic equipment.
Lets see, $20 for the aluminum and I purchased 10 bearings for $5 each. 4
for the bottom, 4 for the sides ( as per photo) and I only have enough room
for 2 as a spacer guide for the front of the slide. Another couple of
dollars for screws and washers for the bearings.
I will make my own jets from threaded SS and the fuel cut off the same
way.Not having the complexities of many types of carbs makes it doable.
I did order a velocity stack from Velocity of Sound and I will make a
trombone type inlet for tuning. Thanks for the latest info on lengths etc.
BTW I support both Larry's and Doug's comments on the testing of the RX8
engine - couldn't have said it better myself.
On Machining - perhaps this is another thing for Larry to consider - it
would be so easy on a CNC. He could machine the parts and builders could
assemble their own (labor intensive part). The beauty of this you can make
any size inlet you want.
I now have to machine O-ring grooves - that should be fun!
George (down under)
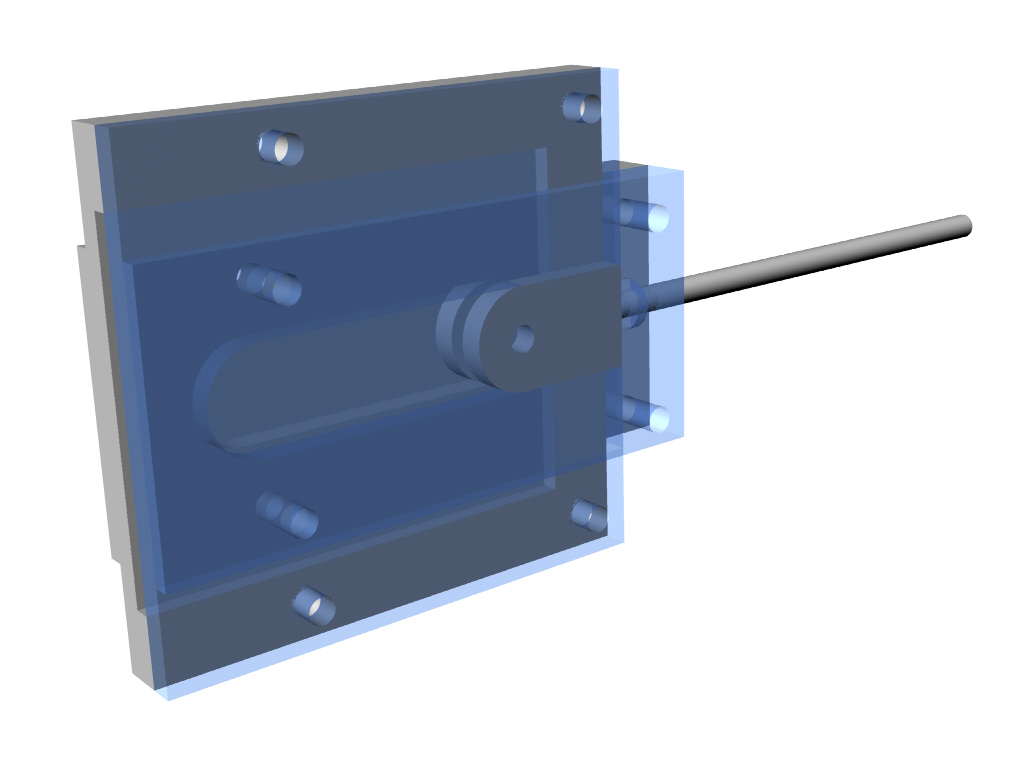
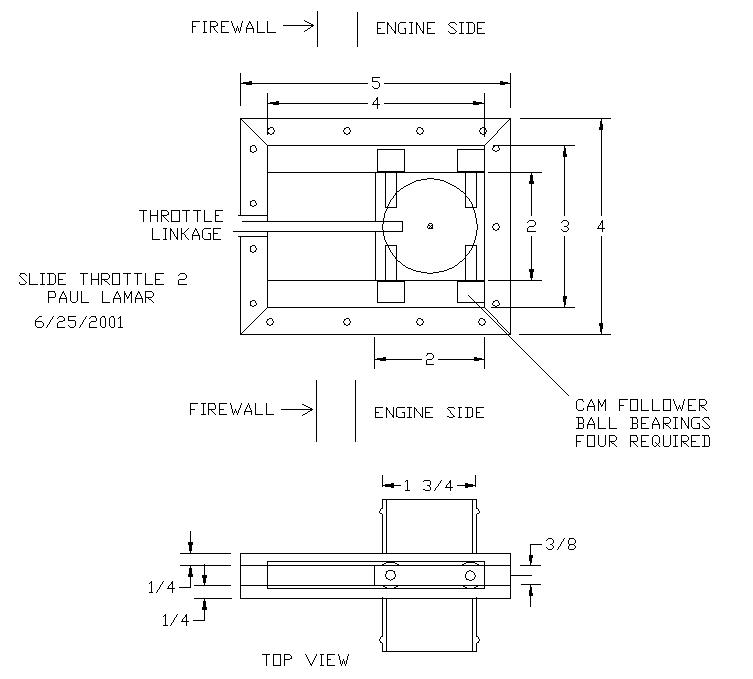
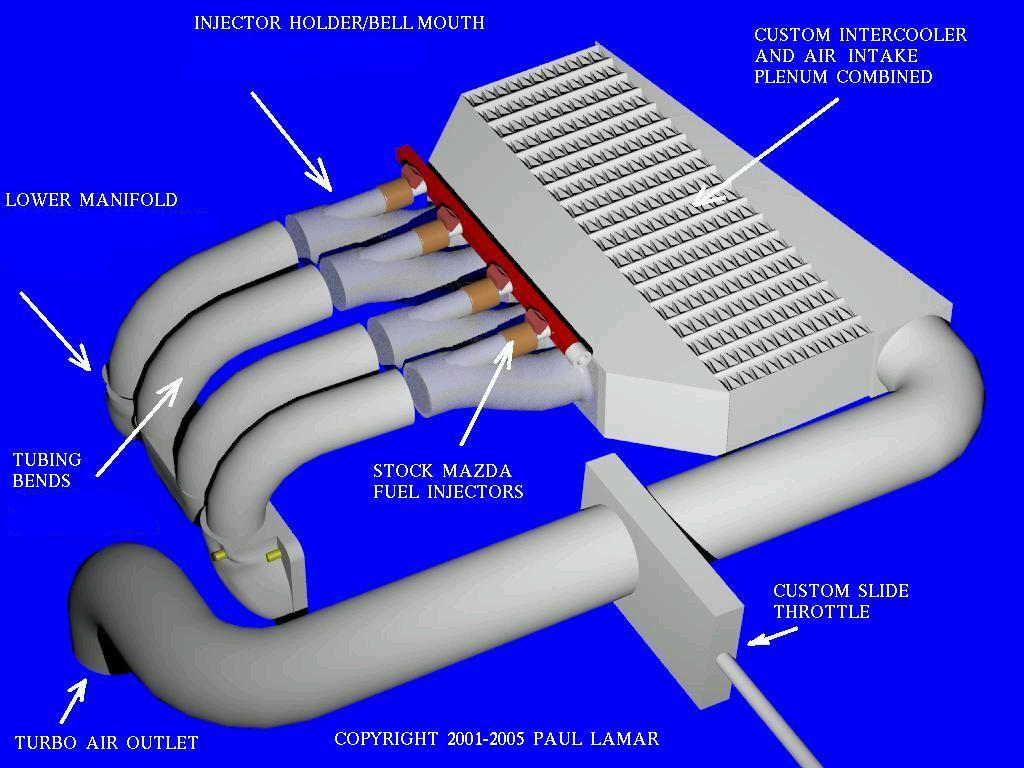
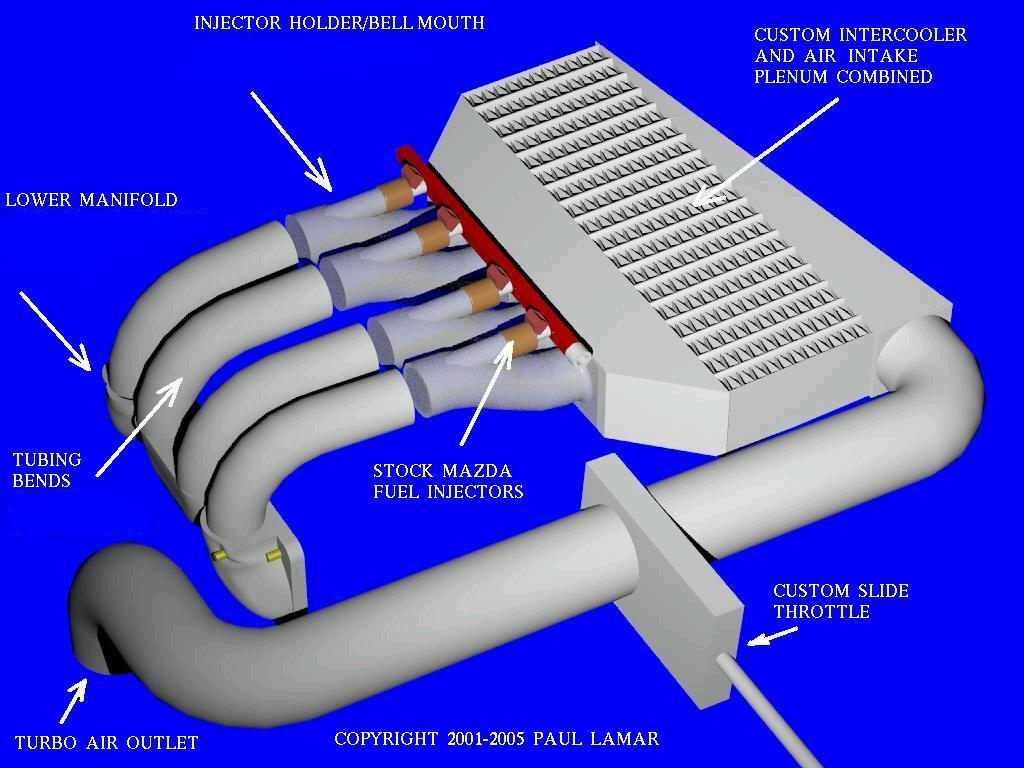
Got any more pictures. I can't quite figure out what you are doing.
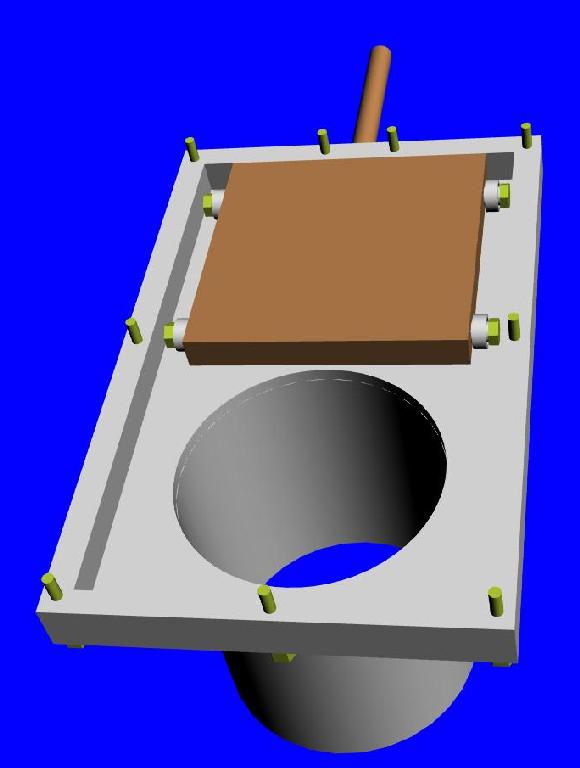
Is it something like this old one I did for the turbo engine?
--
Paul Lamar ...No rotor no motor.
The Rotary Engine NewsLetter. Powered by Linux.
ACRE NL web site.
http://www.rotaryeng.net
Copyright 1998-2007 All world wide rights reserved.