> >>> I found an old SAE paper 730119 on the OMC engine.
> >>> A very interesting paper.
> >>> I noticed that OMC had good luck with aluminum
> >>> side housings made from hypereutectic aluminum.
> >>> The same process used by GM on the Vega engine.
> >>> Does anybody have any direct experience with
> >>> OMC snow mobile rotary engine side housing wear problems?
> >>> >>> I wonder how Silicon Nitride ceramic
> >>> side seals would work on hypereutectic aluminum.
> >>> >>> Perhaps OMC was better able to control the casting
> >>> process than GM.
> >>> >>> >>> Paul Lamar ...No rotor no motor.
> >>> >>> Paul,
> >>> I mentioned this before, and perhaps you heard differently through
> your
> >>> Chapparal contacts, but I was told the engine blocks on the Vega
> engine
> >>> worked fine by people in the know. Many other problems including
> valve
> >>> guides which caused most of the smokers rather than the block.The
> >>> Porsche 928 V8 and many of the current MB V8's use the same
> technology.
> >>> I thought this might be a good possibility, but I doubt that Mazda
> would
> >>> have missed it if that had been the case.
> >>> Bill Jepson
> >> >> >> BMW had problems with the sulfur content in US gasoline eating
> up the
> >> bore in their aluminum blocks on the 3L V8 (530i cars) - 10 years ago.
> >> I haven't heard of more recent issues.
> >> >> Other question.. It's my impression that the apex seals take more
> >> abuse than the side seals, and similarly the rotor housing wear
> >> surface needs to be tougher than the side housing wear surface. Is
> >> this correct? Does that allow using a coating that's less tough on
> >> the side housing? It's apples to oranges, right?
> >> >> >> >> Regards,
> >> >> Matt-
> >> >> I would say yes Matt. Just an impression I get. However the side
> housings
> >> wear more than the rotor housings. Once the ridges are over a couple
> of
> >> thou the housings need lapping or replacing. I suspect the cast iron
> side
> >> housings could benefit from the same chrome treatment given to the
> >> rotor housings.
> >> >> The wear on the rotor housings are well within acceptable limits
> as long
> >> as the apex seals remain intact. With the Mazda system of chrome over
> >> steel.... cast iron apex seal wear is projected to be about 3,000
> hours.
> >> With Silicon Nitride ceramic apex seals wear is projected to be
> 30,000 hours.
> >> Of course no one has worn out a ceramic apex seal yet.
> >> -- >> Paul Lamar ...No rotor no motor.
> > > > Paul,
> > > Ethanol fuels will dissolve unprotected aluminum.
> > > Doug
> > > Looks like it is out for Porsche's, BMW's and Mercedes.
> > Not to mention all the other companies that are planning to
> > switch to un lined aluminum cylinder bores.
> > > Paul Lamar ...No rotor no motor.
>
>
> Paul
>
> Anodized aluminum works.
>
> Doug
>
> I don't think so. That is a very thin coating.
> I also don't think anodizing works on silcon. I could be wrong.
>
> Paul Lamar ...No rotor no motor.
>
> Paul, You are correct. The anodize would be very blotchy. I am at a loss
> though
> as to how the aluminum in the block would be effected (by ethanol) when
> the bores are
> prepared for final hone by hydrocloric acid.
> Bill
Paul, regarding your question about experience with aluminum side housings,
in our Powersport prototype engines, we made our own aluminum housings for
over 10 years. Various configurations were used as the design was developed
over years. Various wear surfaces were also tested over those years.
We made our patterns and core boxes. I made most of the sand cores by hand.
We started experimenting with aluminum housings casting included Reynolds
390 (hyperutectic aluminum-silicon alloy) in the 1980's. The tricky part of
these was the proper surface finishing/lapping. We ground the surface then
flat lapped with silicon carbide compound. My notes show that OMC used a
LapMaster machine and silicon carbide slurry with a final lap with aluminum
oxide. We consulted with Reynolds on the casting and surface preparation
process and they were very helpful. The folks with whom we talked at
General Motors at the time told us the factory processes worked very well
but when engines requires disassembly/machining/assembly in the field, the
precision surface required created too many field service problems. I
think they went to the Iron Duke at that point and shelved the Vega aluminum
engine due to these field service consistancy issues. For the rotary
housings we did, the 390 lapping process would work fine on one housing but
not as well on another. Our results were just too inconsistant. Based on
our experience it is clear this process can be made to work but it requires
a very precise approach using the best equipment and technique.
Rather than mess spending a lot of time and also money on equipment to get
it right on a consistant basis, we went to arc then plasma sprayed housings
which we could simply grind and flat lap. Vendors we used for these
included Flame Spray Northwest in Seattle and Miller Thermal in Appleton,
WI. These castings included 356 and other for the metal sprayed wear
surfaces. We experimented with various wear surfaces materials (usually on
the same engine). A thin metal sprayed surface appears to be what Jim
Mederer at Racing Beat is using on his new housings. I looked at a set of
these this week. We were using a thicker application ( machined a .024
recess in the housing, then grinding and lapping to final finish).
The last of our aluminum housings were for our "short shaft" engine for the
RV-3. This was first assembled in 1991. I found a photo of this engine on
our dyno with the test club installed and will try to get it scanned and
sent to you with other photos of the dyno. These last iteration aluminum
housings were anodized .002 with nickel-carbine by Tiodine in Huntington
Beach, California. They had a propriety process called Hard-Tuff where they
used a teflon overlay to fill in the anodizing porosity in the anodizing.
For race engines coming through the shop we had been using pistons they were
doing with this process for JE and Venolia (JE called it KoolKote). That
same year we also used Progress For Industry in Saegertown, PA to do
electroless nickel with silicon (i.e. Nikasil) that worked very well. Their
propriety process was called Prowear Plating. And Mahle/major manufacturers
have used Nikasil for years in cylinder liners and pistons.
The upshot of all this is these aluminum housing wear surfaces can work very
well. But they do add to the cost of the engine. We put these efforts on
hold to develop the lower cost Mazda conversion engine with the internal
spur gear reduction drive using as a reference the Allison of WWII. Just as
the Reynolds 390 parent material was its own wear surface, so is the iron
Mazda housing. But with those Mazda iron housings we simply used our same
lapping machine we had used for the "Vega" type housings. But so much
easier with the iron vs. 390 housings. We could do the Mazda housings
easily. And if necessary these were nitrided again if more than .002. Here
in Portland, Met-Tek did most of our nitiriding on gears, housings, etc.
The other day Phillip Groelz called them and I think Phillip told me later
they said the cost to nitride a full set of housings would be only $150.
Eric Wagoner here on the airstrip has a precision grinding shop and as an
experiment the other day took one of our old junk front housings and
precision ground it. It was .002 out of parallel when he started and had a
nice precision surface when he finished. As a test we are going to have
Eric grind some old housings and then have Met-Tek nitride them. Will then
run them on the dyno to see how they work without lapping.
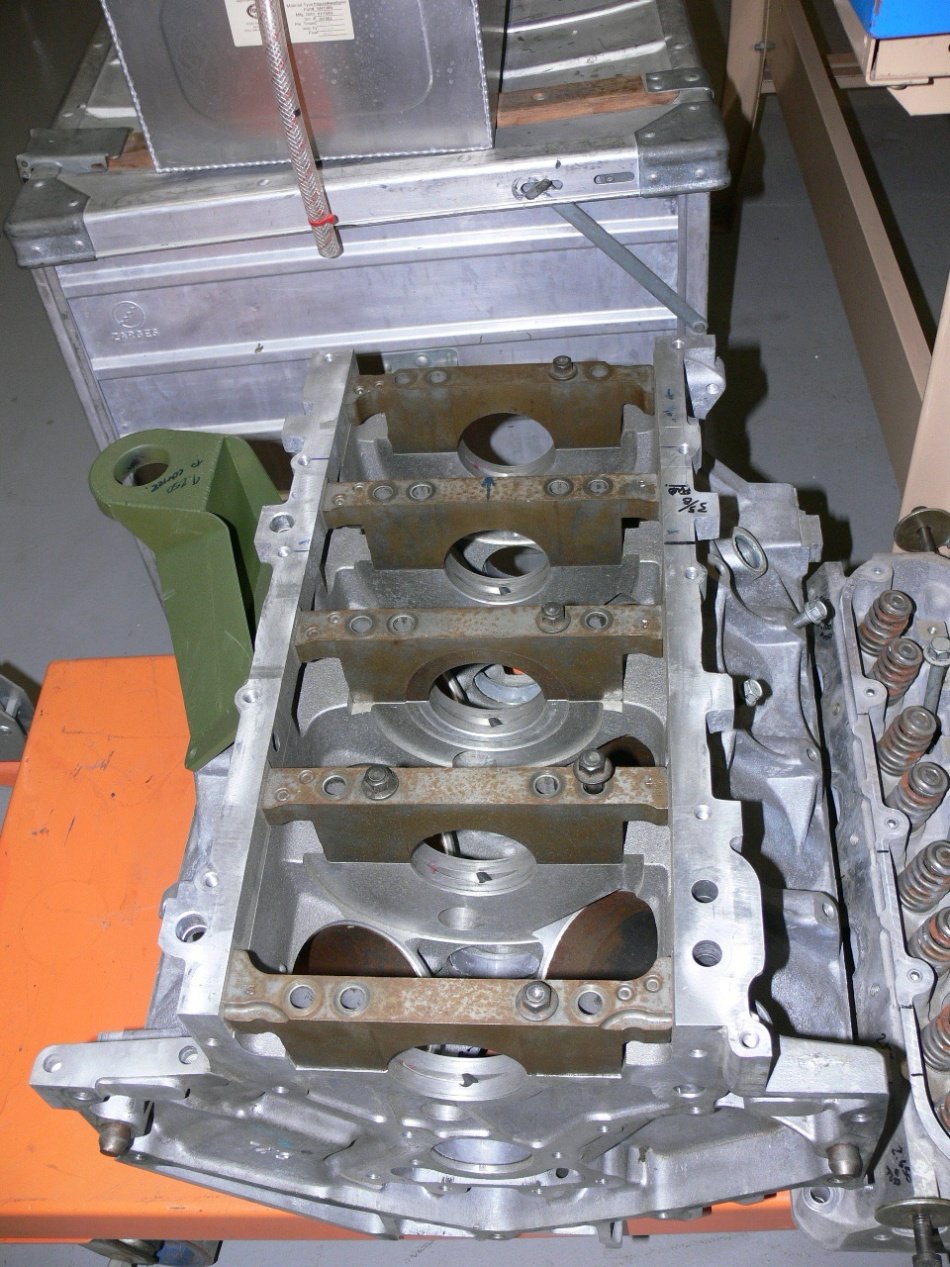
A final note on the aluminum housings. Based on our experience, these
suffer from the same design challenge as did all the aluminum block V-8 race
engines that came through the shop. At sustained high power settings both
the the aluminum block V-8's and rotary end housings experienced creep
distortion. The engines with the closest duty cycle to our aircraft engines
were the off-shore race boats and as you can imagine, these were the worst
due to sustained how power setting. At the end of the straight stretch, the
automotive engines get a rest.. But even then, the oval-track engines would
have the main line move around. As you know this is generally not a problem
with the automotive iron block/ the stock Mazda iron housings. But hopefull
with further development these issues can be addressed in the aluminum side
housings. On his new aluminum housings, Jim Mederer significantly increased
the number of gear retention bolts in his end housings. Probably also
beefed up the center section of the casting also. Sure hope they can be
made to work at sustained high power settings. The weight savings is
significant.
Steve Beckham
There is a fairly large market in LSA for all aluminum one rotor Mazda engines.
Paul Lamar
Thanks to Steve for writing up all of this interesting background information.
When talking about creep, has there been much study of what the source
is (other than sustained temperature)? We've talked about bolt
tension and lack of stretchiness (too high modulus)... Has anyone
actually tried the Ti bolts we were talking about before.
When talking about sustained high power levels, how hi is it? Would
there be significant/detrimental creep at 250hp on a two rotor?
Does the problem depend on cooling?
Regards,
Matt-
I think Steve means deflection rather than creep. The modulus of elasticity of
aluminum is one third that of steel and 2/3rds that of cast iron. Creep happens
when there is a significant static load on a part over time and it becomes
permanently deflected. Some times at room temperature.
Aluminum does not suffer from creep. Aluminum yields and takes a permanent
set if over heated and loaded. Many plastics do however suffer from creep.
Aluminum engine blocks do move around under combustion loads. Especially if the
wall thickness is the same as the cast iron part it replaced. It must be
thickened up to compensate for the lower modulus of elasticity.
BTW the old Rolls Royce V8 aluminum block was considerably thicker than the
cast iron block it replaced. This was done for noise reasons as the walls
of the cast iron block were vibrating and radiating noise.
Panel stiffness was the main design criteria. The stiffness of a panel
is proportional to the cube or fourth power of the thickness while
the weight is only directly proportional. An aluminum panel two or three
times as thick as a cast iron panel is much much stiffer. The weight
may be the same or lower as aluminum is one third the weight of cast iron or
steel.
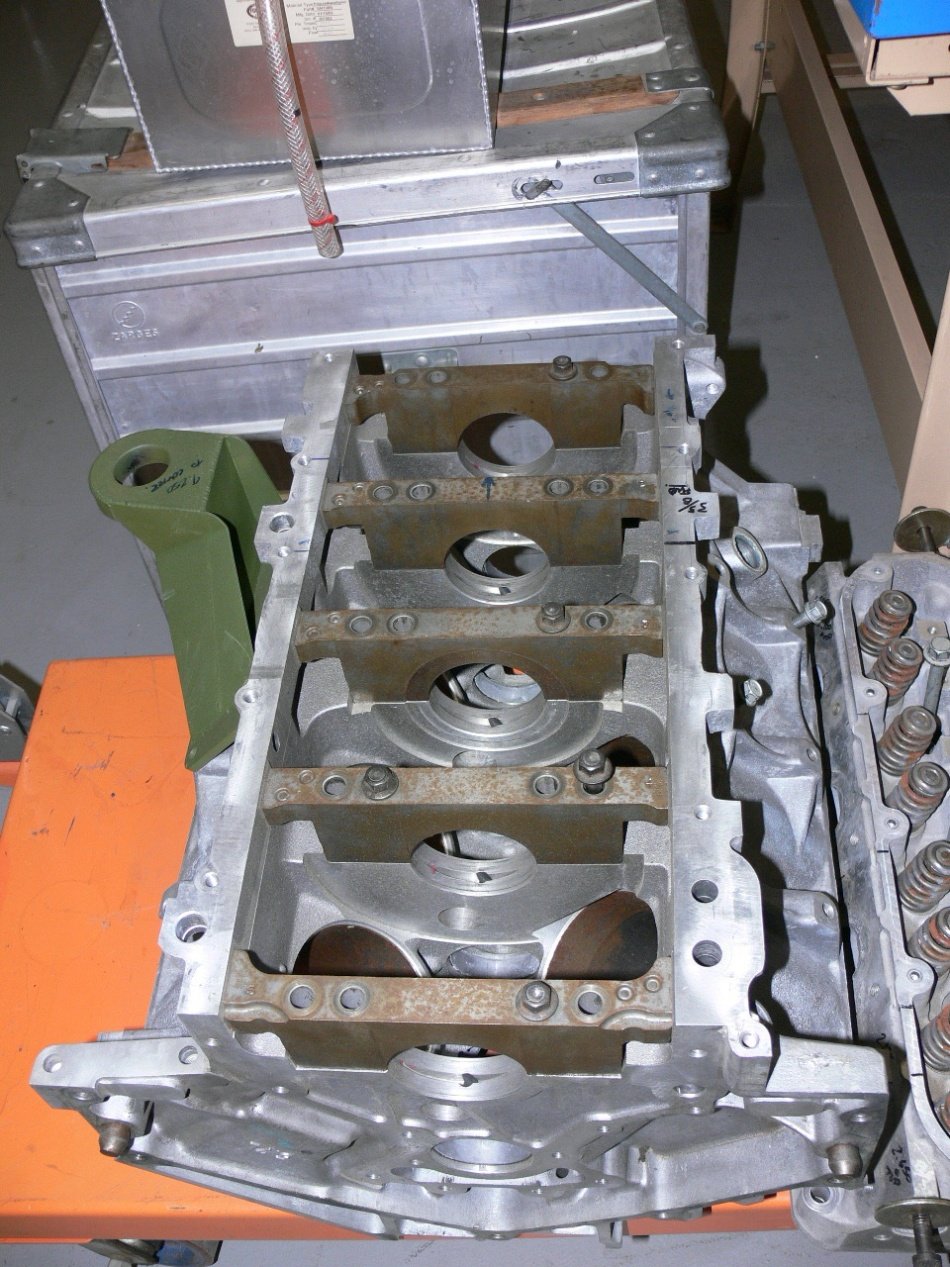
I think Steve is probably referring to aluminum Chevy blocks. More modern aluminum
engines have girdles to stiffen the main bearing area of the block. In line engines
and V engines are always trying to shove the crankshaft out the bottom of the
block. Consequently they are inherently heaver than horizontal opposed
engines where loads from opposite cylinders balance out more or less.
Honda engines are famous for main bearing girdles :) In some cases they
are cast iron or even steel. The aluminum Jag V8 has a cast aluminum oil pan
with steel inserts that doubles as a girdle.
I drove both a Corvette with an aluminum block and a Jag XKS with an
aluminum block. There was a world of difference at 6500 RPM. The Chevy
felt like a hand grenade while the Jag engine was still smooth.
This was part of a sports car test we did for Pop Science about six or so
years ago.
Paul Lamar
The Rotary Engine NewsLetter. Powered by Linux.
ACRE NL web site.
http://www.rotaryeng.net
Copyright 1998-2007 All world wide rights reserved.