What amazes me the Brits were using WW II era RR58 aluminum
alloy pistons
up until about 1997 for engines turning 14,000 RPM.
With oil spray for cooling. Earlier Formula 1 turbo charged
pistons used an oil gallery built into the piston
for cooling. Oil pressure was sent up the (probably titanium)
connecting
rod, through the piston pin and into the oil gallery.
The same approach could be used in the rotary.
Instead of squirting the oil up inside the aluminum alloy rotor
the cooling oil could be fed through the rotor bearing
into a matrix of oil galleries inside the rotor.
X2020-T6 would have been a better choice than RR58 IMHO.
Paul Lamar ...No rotor no motor.
Paul,
Good idea and is already being successfully done up to a point.
As the single rotor has difficulty having sufficient space for an
oil jet
like the two rotor, some are drilling a hole in the centre of the
rotor to
take the rotor cooling oil directly from the bearing supply hole of the
e-shaft.
There could be 3 holes drilled one facing the centre of each rotor
face, if
necessary, keeping the hole size small so that it doesn't starve the
bearing
lubrication.
Can't see why this system couldn't be used in a lightened rotor.
George (down under)
+++++++++++++++++++++++++++++++++++++++++++++++++++++++++++++++++++
This relatively recent development is REAL promising.
Quote:
NASA Marshall Space Flight Center - Huntsville, AL
Revision Date: 01/18/2007
Information : High Strength Aluminum Casting Alloy for High
Temperature Applications
A hypereutectic alloy such as A390 is a conventional aluminum alloy
used to make pistons
in U.S. automotive engines. This alloy has adequate strength, is
easily cast, and is
low in cost.
However, a typical alloy such as A390 aluminum alloy used in the
design has inadequate
tensile strength in the required 500° to 600° F temperature range.
In 1995, Marshall Space Flight Center's (MSFC's) metallurgists began
working with Ford
under a Space Act Agreement to develop a new, castable aluminum
alloy that had a 30%
improvement in tensile strength during operation in the required
temperature range.
The result was an aluminum-silicon alloy that meets or exceeds all
original automotive
criteria. Figure 3-3 shows a 600° F, tensile strength comparison of
available aluminum
alloys against the NASA alloy. The projected cost of the
aluminum-silicon alloy is 95¢
per pound versus 87¢ per pound for A390. Since less of the new
alloy material is required
due to its higher strength, the cost per piston is expected to be
comparable. MSFC has currently
filed a patent on the aluminum-silicon alloy, and negotiations are
ongoing with Ford and
other U.S. automobile manufacturers regarding its use.
End of quote.
No details yet of the percentages of different materials in the alloy.
600 F will work fine for a rotor with internal oil cooling and steel
inserts
for apex seal slots. The rotor might weigh about half of the current
9 pound
iron rotor so RPM might be 1.50 higher or about 16,500 RPM. HP might
be as much
as 480 for a NA P-port two rotor and 720 HP for a three rotor. It
will be
a lot cheaper than BeAl alloy.
Paul Lamar ...No rotor no motor.
Paul, Would coating the rotor faces with ceramic make this NASA
alum-silicon work? Dave D
Perhaps but it would have to be very thick. I would say
a minimum of .032" thick. It would also have to be very tough
as if it came off it would destroy the rotor housings.
The track record so far is very bad. I have seen rotor housings
that have been destroyed by failed ceramic coated rotors.
Not pretty. A fitted SS sheet mechanically fastened would be more reliable.
This has been done with heavy duty pistons.
Perhaps the entire high silicon aluminum rotor encased in thin SS sheet tig
welded
along the sides as cost is no object on this type of racing engine.
The sheet could be formed in a press.
The apex seal slots could be incorporated in SS. SS has low thermal
conductivity
which in theory improves the combustion efficiency as it contains more heat.
--
Paul Lamar ...No rotor no motor.
Paul,
A Ti rotor would probably now be possible by using DLC coatings in all the
seal grooves to prevent galling. It can also be investment cast very
accurately.
Just out of curiosity, do you know if anyone has tried DLC on the side
housings? Wouldn't be cheap, but the stuff is hard and slippery. Some racing
connecting rods are now being built without wrist pin bushings by DLC
coating the wrist pin. Also used on many racing flat tappet cams, and that
is an extreme high pressure area known for failure.
Larry
Don't know Larry. Sounds like a good idea.
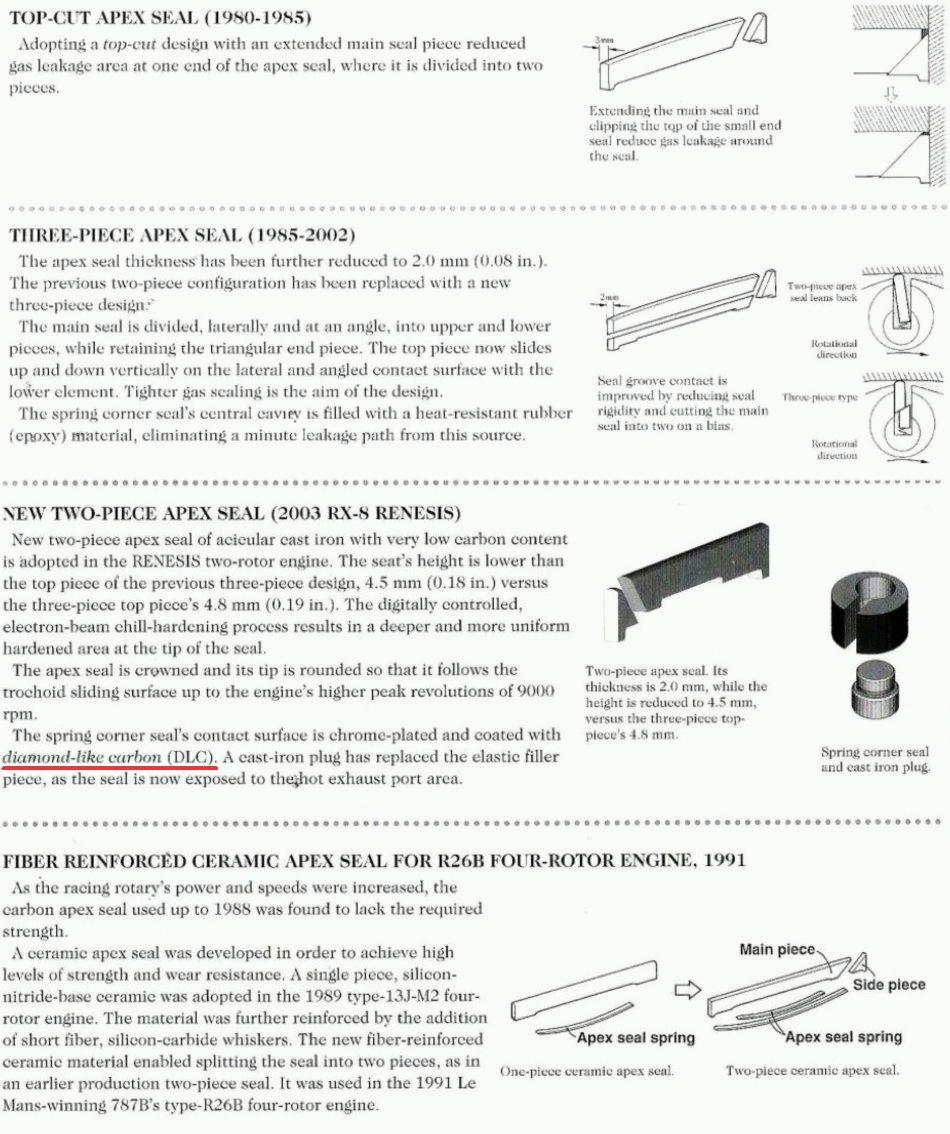
Mazda currently uses DLC on the stock corner seals.
http://www.rotaryeng.net/history.html
The side seals IMHO are less likely to gall as there is little or no reversing
of loads. I think all you need worry about is the apex seal slot.
Is it possible to cast in steel inserts in titanium castings?
Paul Lamar ...No rotor no motor.
The Rotary Engine NewsLetter. Powered by Linux.
ACRE NL web site.
http://www.rotaryeng.net
Youtube key word UTUBPLEASE
Copyright 1998-2008 All world wide rights reserved.