Hi Paul,
Are the Hatch exhaust ports available anywhere or must one fab his own?
Also, is anyone building and selling an aluminum oil pan for the 20B
engines? I thought maybe Ed Klepeis was but I dont know how to reach
him. Can you help me contact him? Thanks much!!
John Bell
Hey Steve Beckham, do you want to build and sell those exhaust flanges?
Jerry Hey at jerry@jerryhey.com can build a 20B oil pan.
Paul Lamar
Paul, you ask about possibly making and selling the ports/exhaust flanges.
We hope to do this with a refined design to make them more affordable and
easier to build. If the vendors cannot be found who can make them
affordably, we'll simply make those drawings available through you.
Apologize for the length of this response but there are a lot of factors in
play. Following are some.
Phillip Groelz, Francis Romig and Chuck Smith are contributing to
development work on various engine components with an eye on possibly Chuck
providing these and other components, including complete engines sometime in
the future. But if this happens it will not be in the short term. The
exhaust is a good example.
We'll have to come up with a more cost-effective way to make the single
piece that is a combined port insert/four stud flange/and pipe attachment.
When Everett, Francis and I did the prototype integral ball joint
swivel/flange and port insert, it was a test of the basic approach. It
worked well but as with any first piece had areas that needed refinement.
And we spent way too much time building the damned things. Francis
fabricated the dies to stamp the female part of the swivels and machined the
male part of the ball joint from SS 321 stock. After machining, this male
portion of the ball joint was welded to the flange. The port insert was
welded to the flange from the inside and the insert wall built up to
properly transition from the insert to the relatively small exit diameter at
the flange. The interior weld-up on the port insert was necessary for
transitioning from the port insert to the flange because we used relatively
small diameter exhaust ports and pipes and the matching male/female joint
pieces sized accordingly. The male portion of the ball joint was welded
from both the inside and the outside using a machined recess. Following all
that welding, the back side of the flange was again machined flat. When
finished, it produced a solid, single part . With good welds, there was
nothing to break or leak and nothing cantilevered off the flange. The port
insert, flange and the male portion of the ball joint were all registered
and held in place by the four studs and washers/nuts. But many, many hours
of work involved in each.
We went to all this trouble with the port insert because we found the
effectiveness of the insert helped tremendously with noise reduction while
lessening the demands on the muffler and keeping it light. The relatively
small back pressure penalty associated with the port insert was considered
well worth it. The SAE paper that documents Mazda's findings when they
finalized the port insert show that little insert is very effective at
reducing exhaust noise and well designed. The same mufflers we were using
for dyno and flight tests immediately worked much better and lasted much
longer with the port inserts installed. And no more numb feet from off the
concrete slab where the dyno stood and also helped eliminate loose rivets on
the bottom of the fuselage during flight tests.
The revised design needs to avoid the adjustment/preloading hassles relating
to the ball and socket. I was always having to adjust the preload. We
tried springs for this but with them right at the port, we just could not
figure out how to make them work with repeated cycles of up to 3.5 to four
hour flight legs at WOT. And there was no sort of redundant safety feature.
A major safety concern. It may have been that we should have used different
materails for the capture plate on the outside of the socket. But this
experience is what led us to what you see in your photos with the outer
female capturing flange held on by four 12 point high temp nuts.
We hope to work to test some configurations that refine the concept to where
we can come up with something shown in tests to be safe and proven.
Retaining the ball/socket arrangement right at the port is my preferable
choice. So far unable to locate any commericially available exhaust ball
and socket assemblies that are of the correct design, robust material
(Inconel preferably), the right sized pipe and light weight. A complicating
factor is the design needs to incorporate provision for a nice tight radius
right out of the port for tight cowlings on single or tandem seat aircraft
(worst case scenario). You can see in your previously distributed photos of
our protype set that they worked very well in that regard in both the RV-3
and RV-4 where we had engine mount tubes located in the vicinity and the
cowling a coupleof inches from the ports. Space wise, no big deal for a
side-by side aircraft --except we found that cantilevering any heavy
components (i.e. mufflers) out to the side, ultimately proved to be
problematic. So we simply kept everything in as close to the engine and
centerline as possible and this helped with both structural and space
considerations. The ball joint eliminated the stress and cracking of pipe,
weld and flange while using relatively thin, light weight components
throughout. And it concurrently eliminated the expansion/contraction
stresses and related cracking in that area as well.
The followup design we are currently building for dyno and flight testing is
slightly different than the prototype shown in your photos. We are using
two prototype Inconel ball sockets an experienced aerospace fabricator did
to spec for us to test. These ball joint swivels are located immediately
following the short bend out of the port. Hopefully that short lever from
the port to the ball joint will not stress the pipe/flange intersection due
to the combination of factors including the ball joint and the short lever.
And the ball swivels are a pratical help as well by providing some lattitute
in pipe location. The Inconel material cost alone makes cost containment a
challenge. But safety is a paramount concern with these components. If we
can make something like this work, we can try it out of thicker section 321
and see how that holds up. If those two Inconel units test well, and we
can get him to produce them, that may be a good first step.
Meanwhile, the plan is to get the first engine fully integrated with the
airframe, including exhaust, heat exchangers, baffling, plumbing and fuel
system completely installed. Then will take it out of the airframe and do
dyno testing and tuning with the reduction gear and test club installed.
Depending on what kind of numbers we get from those tests, we may
disassemble the engine and install a second set of rotor housings with
larger diameter port inserts, throttles, intake runners and a different
configuration plenum then put it back on the dyno to get more numbers. The
first engine for testing uses fairly small diameter ports, throttles and
induction tubes. The power section of the engine is assembled and ready to
install in to the aircraft but we need to do some work in the fuselage
including installation of Don Rivera's dual electric fuel pumps/filter/
relief valve package and fuel selector (duplex valve for automatic return
line switching when tanks selection is made). The aircraft was on the gear
with wings installed but we took all that off and put the fuselage on a
rotisserie to rotate it so that old men with bad backs can more easily
install all the fuel and electrics. That done, we'll put it back on the
gear and install the engine and reduction gear and then finish the exhaust,
etc. When done there, the engine will come off and go on the dyno.
Following that program, the plan is to then conduct some extended flight
tests to see what kind of numbers it produces and if everything holds up.
If all of that is to satisfaction, we'll see about offering various
components, complete fuel injection system and/or components, possibly
through Don Rivera at AirFlow Performance. And Chuck Smith has indicated
interest in producing other components as well as complete engines with
reduction gear. We'll test that prototype reduction gear on the dyno and
RV-3 as well.
Regardless of what transpires ultimately, if we can't get vendors who will
produce the exhaust tooling and finished parts, we'll simply give you one
for you to make detail drawings for anybody who wants to use them for
reference. Apologize for the length of this reply.
Steve Beckham
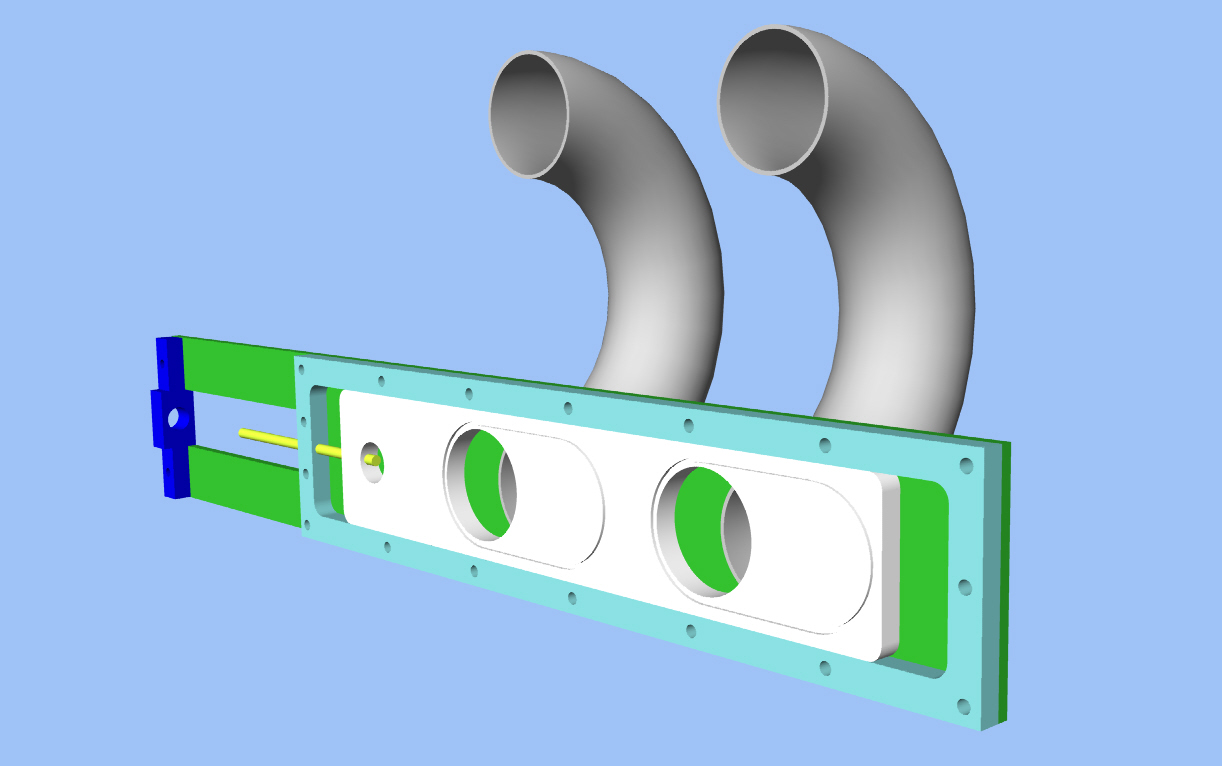
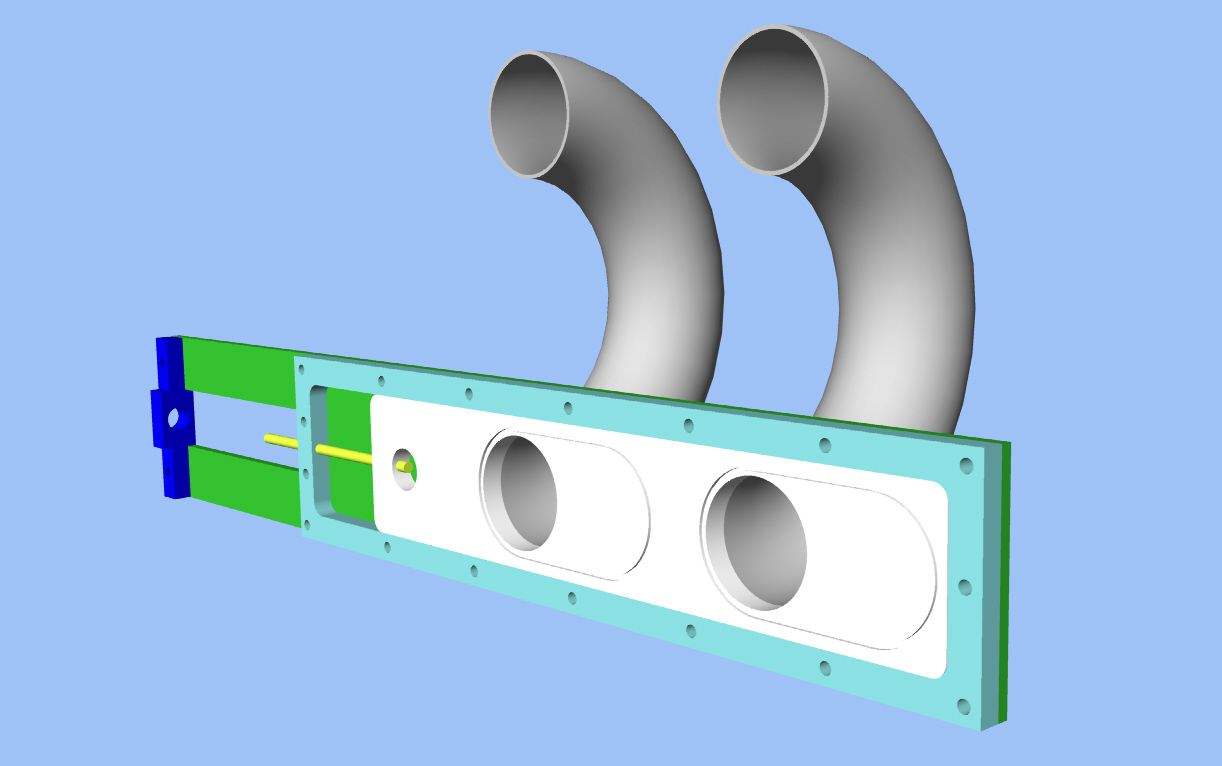
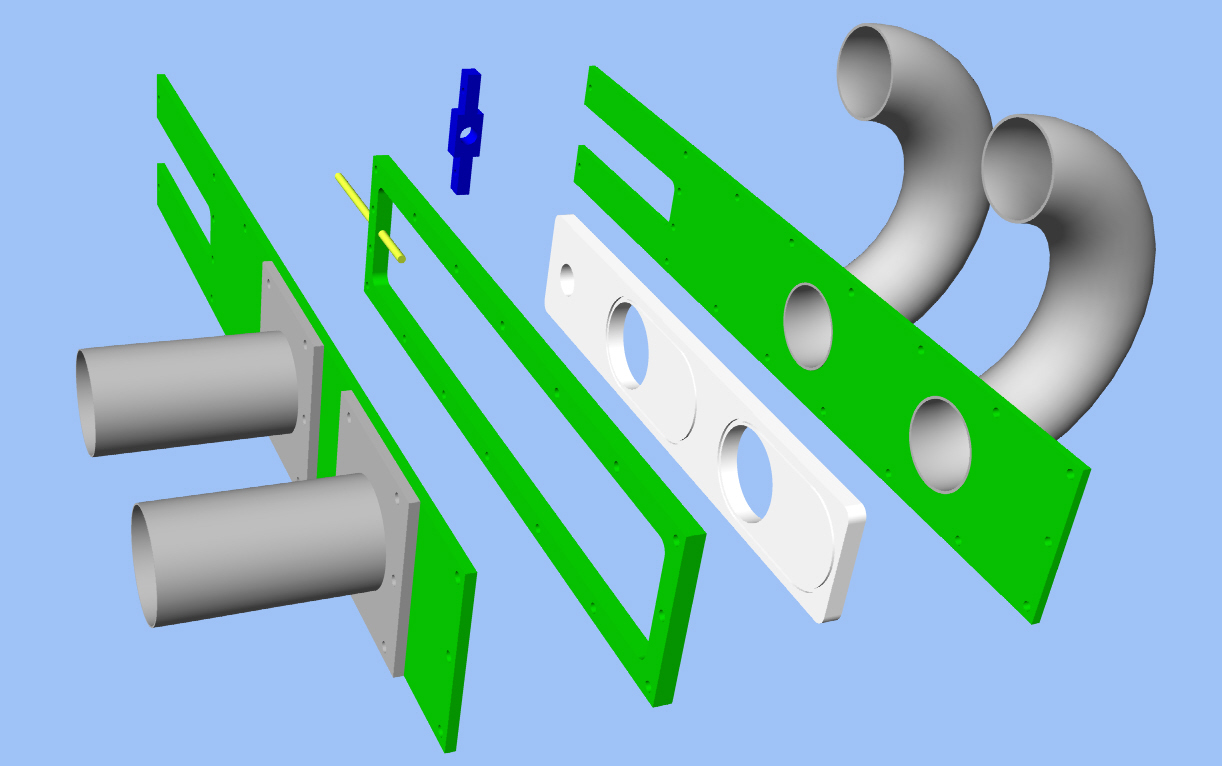
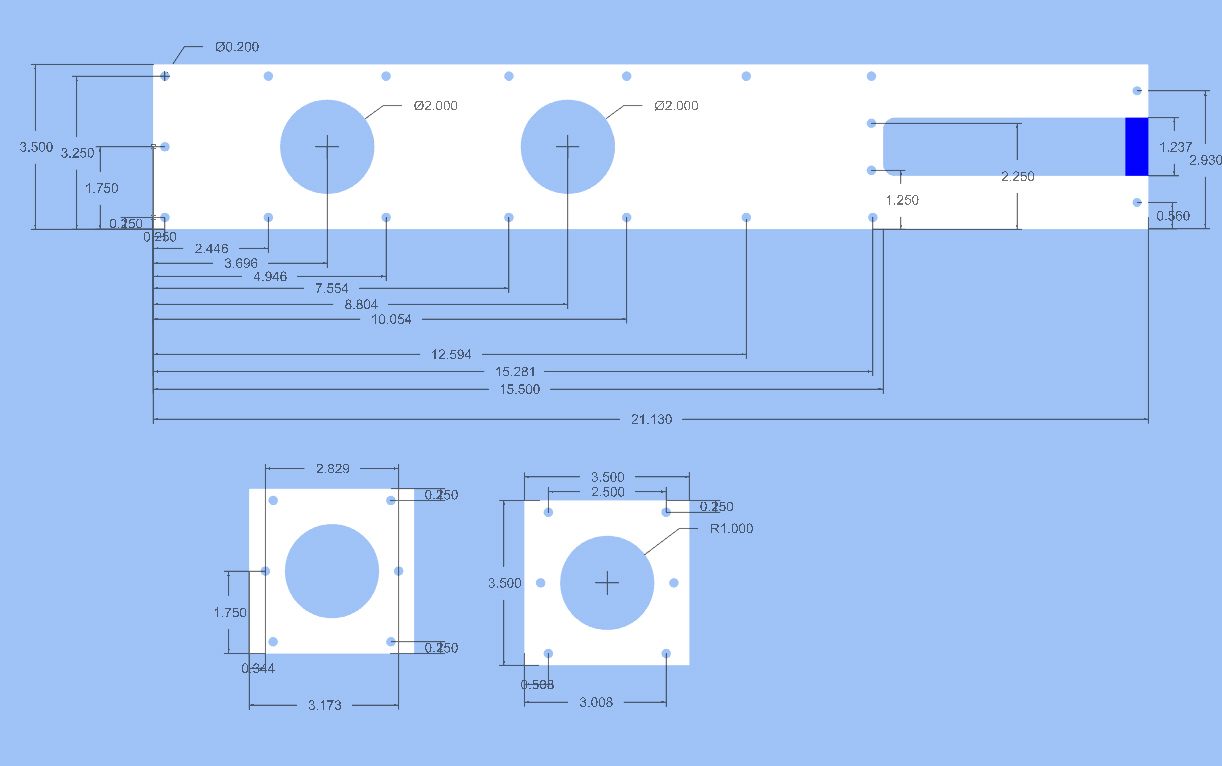
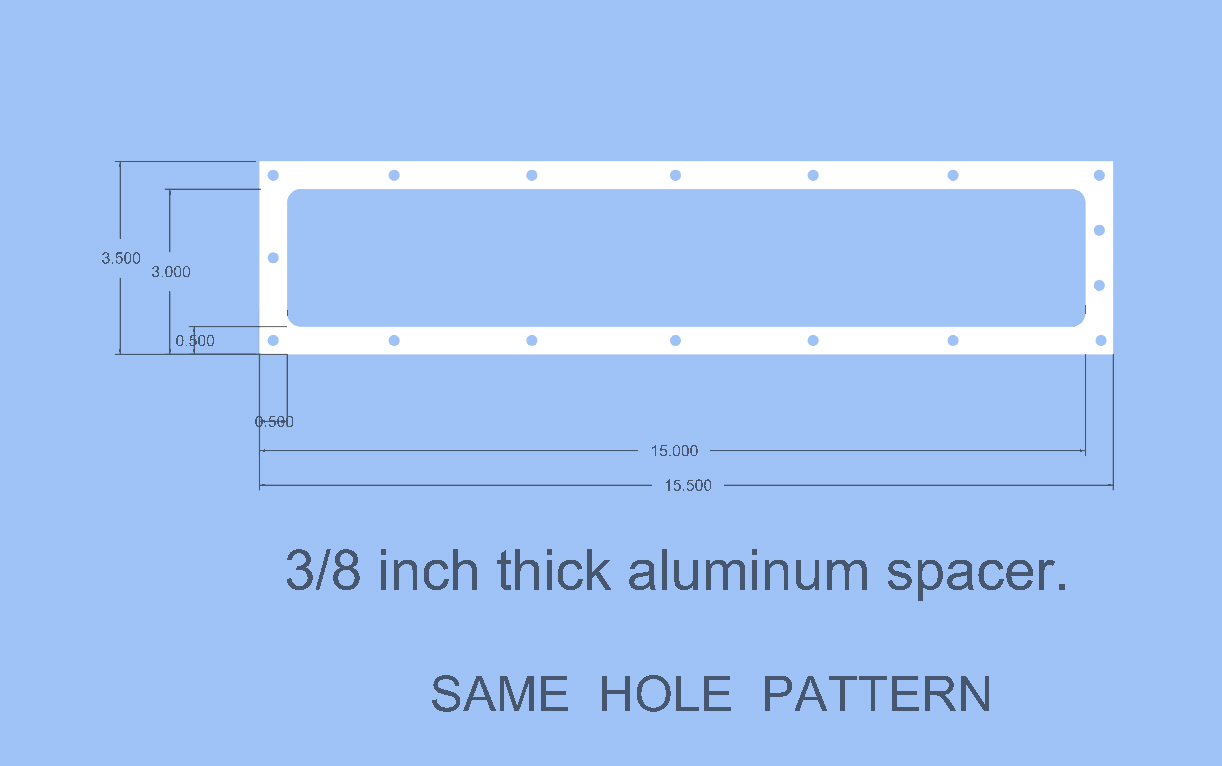
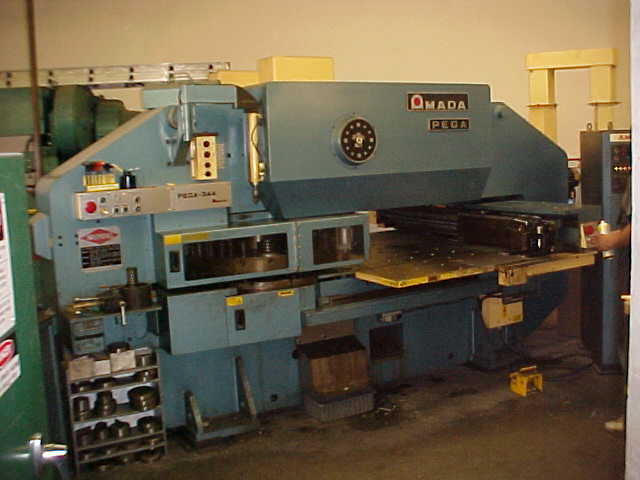
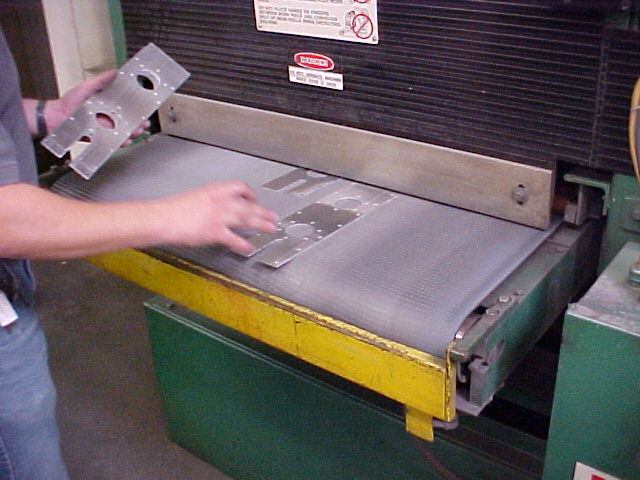
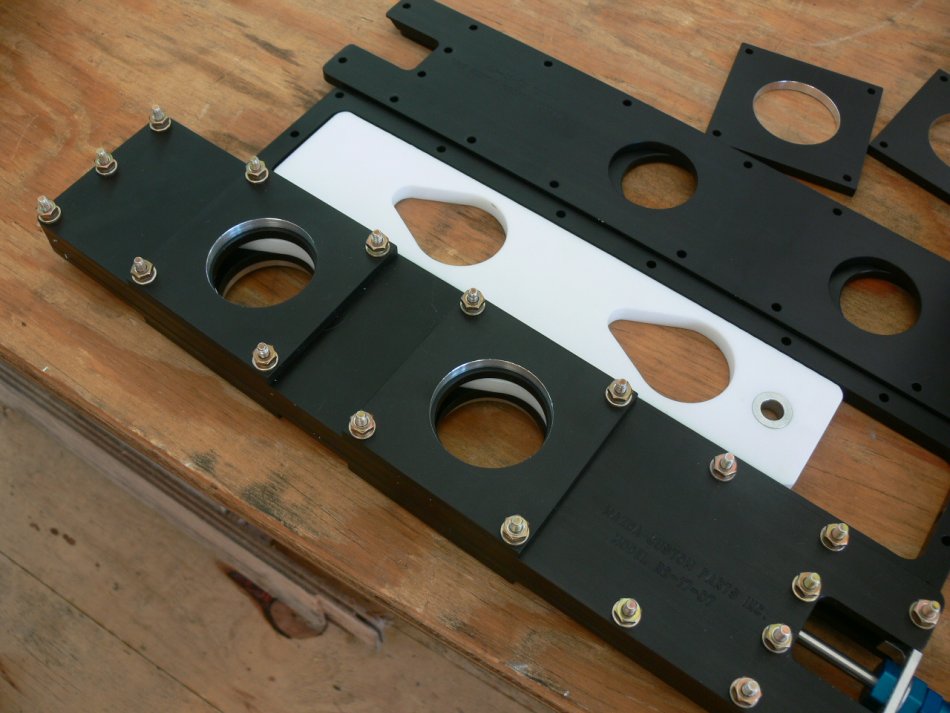
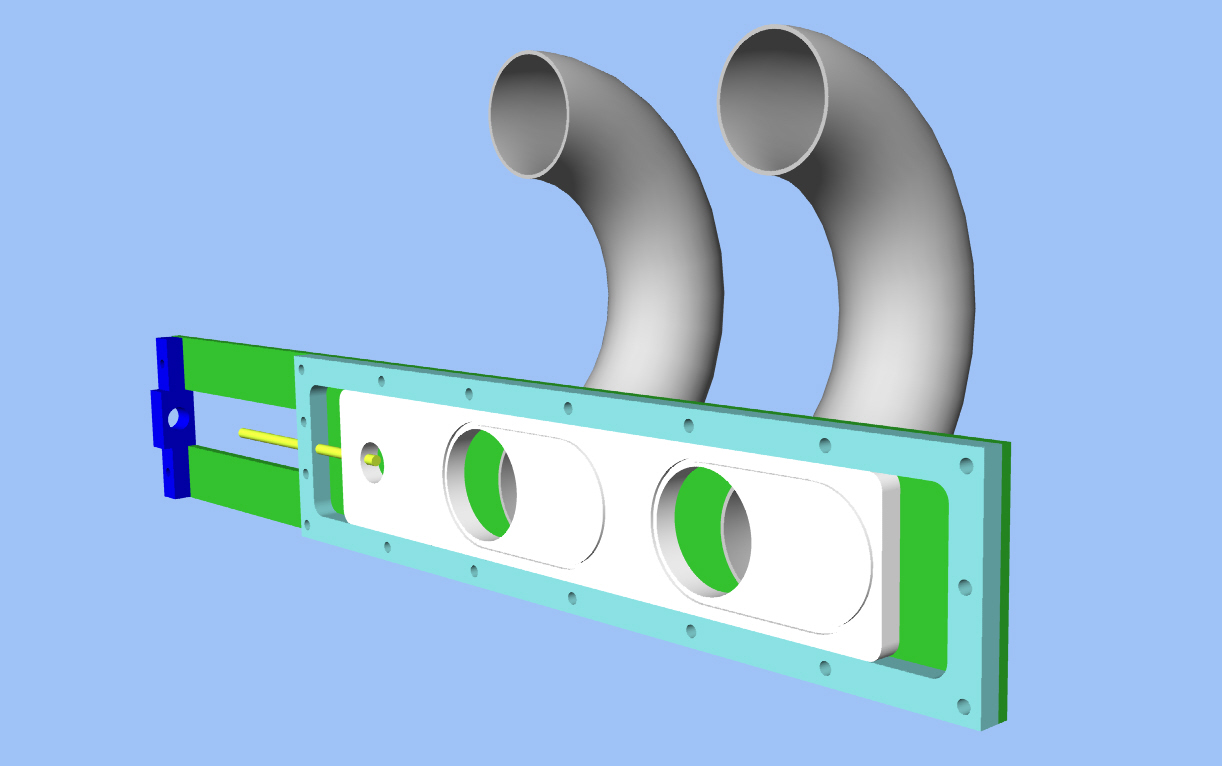
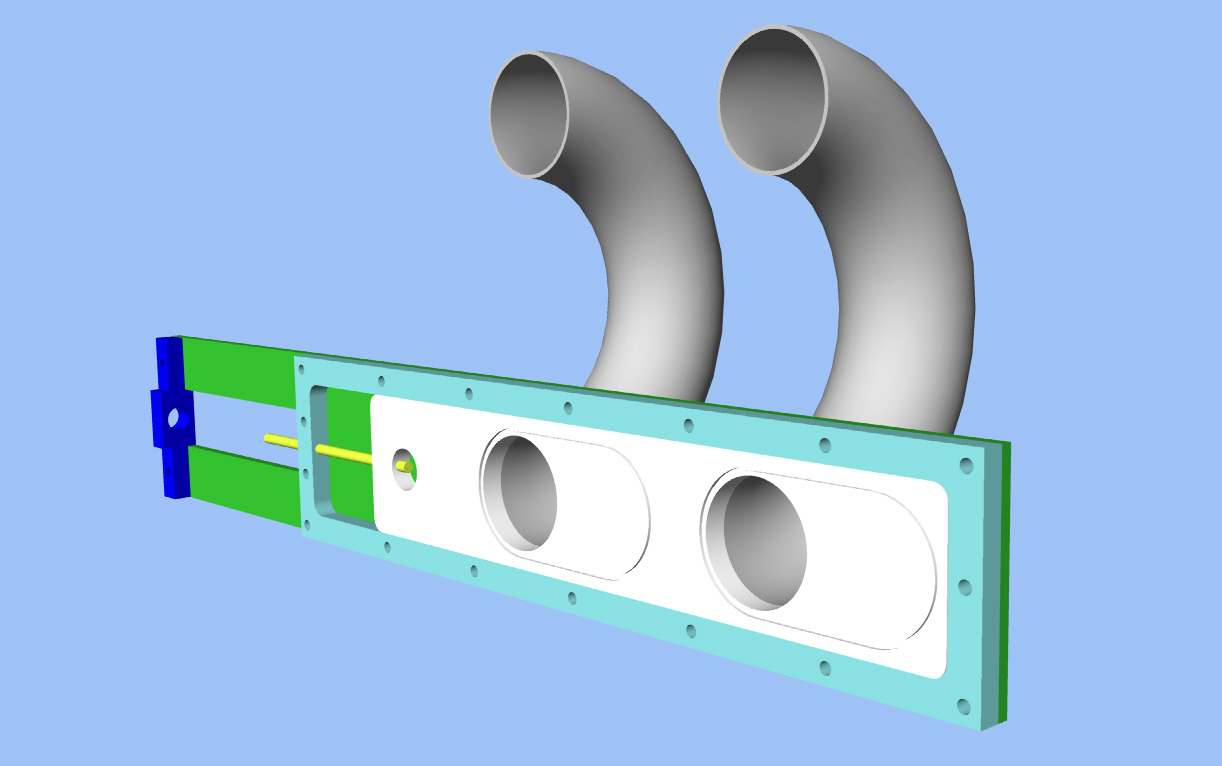
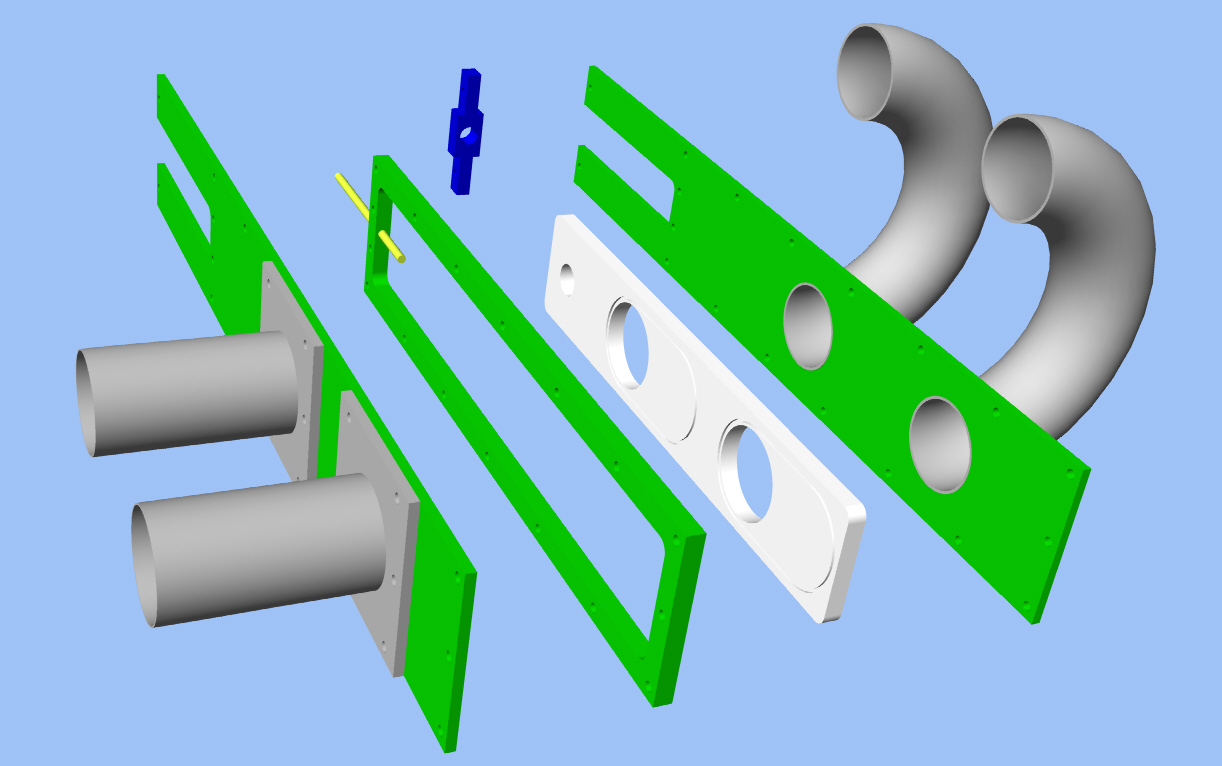
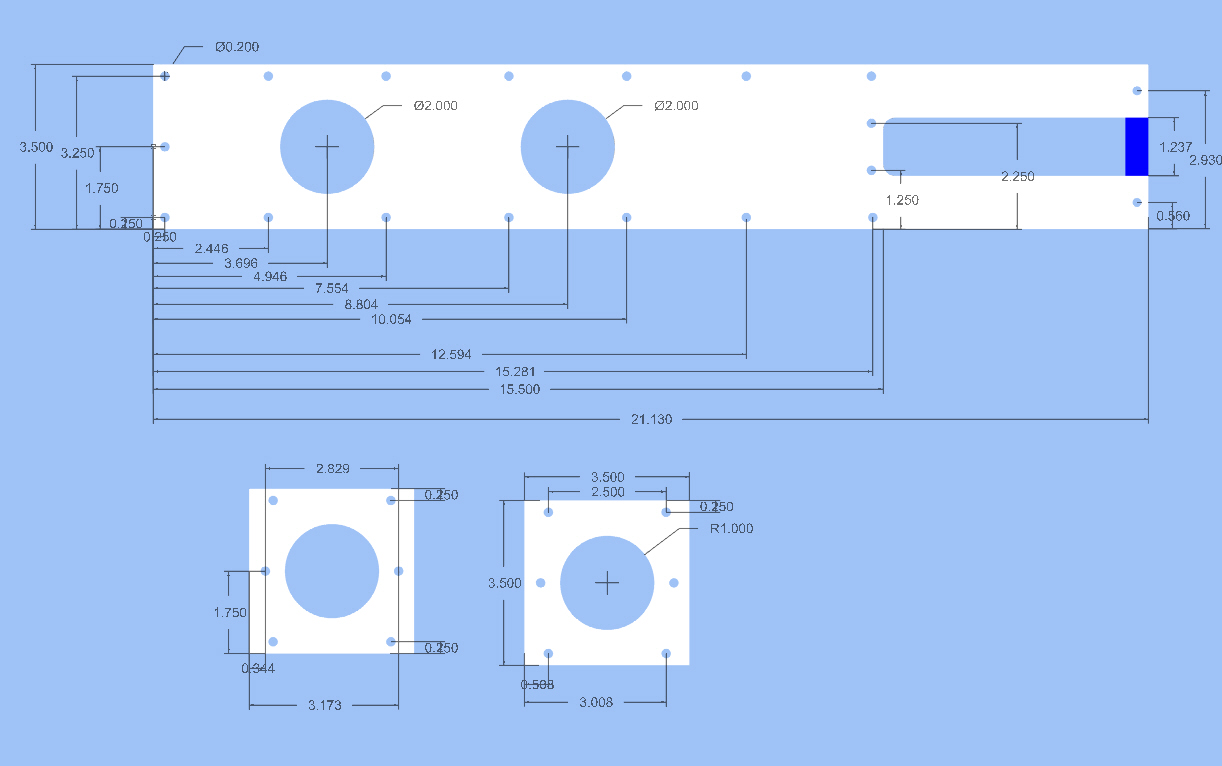
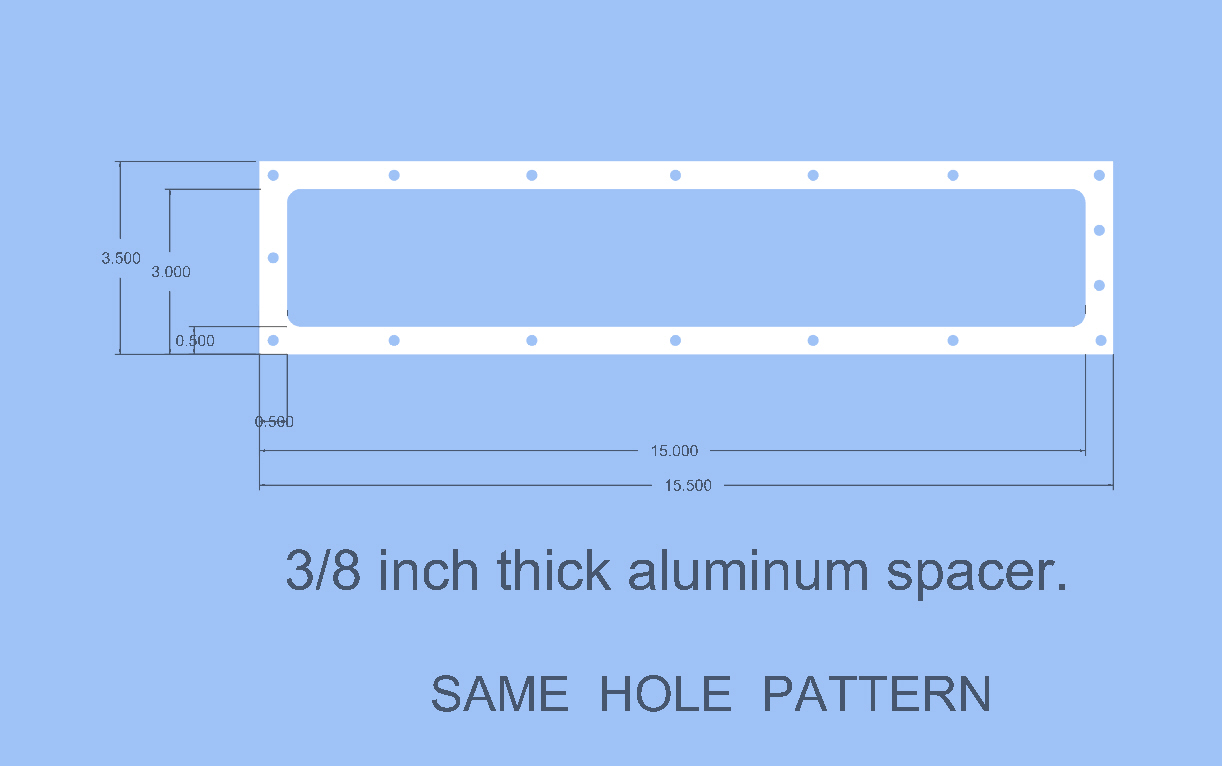
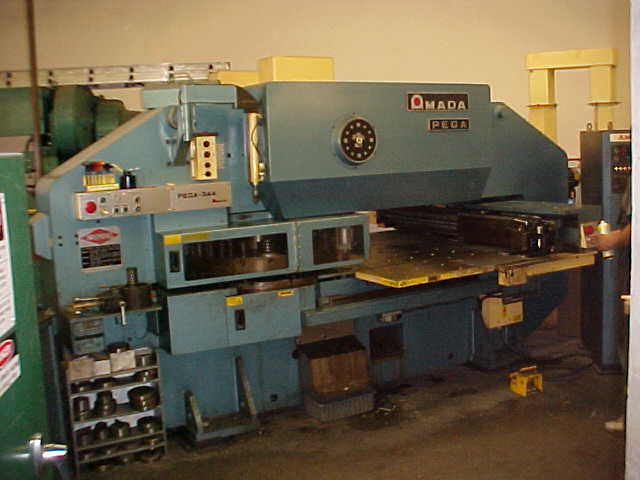
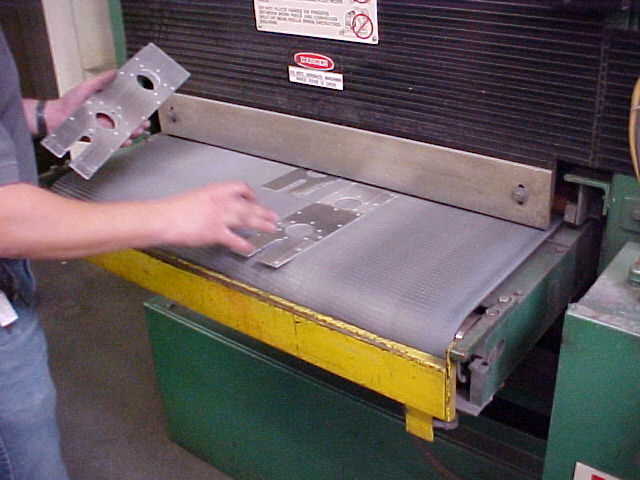
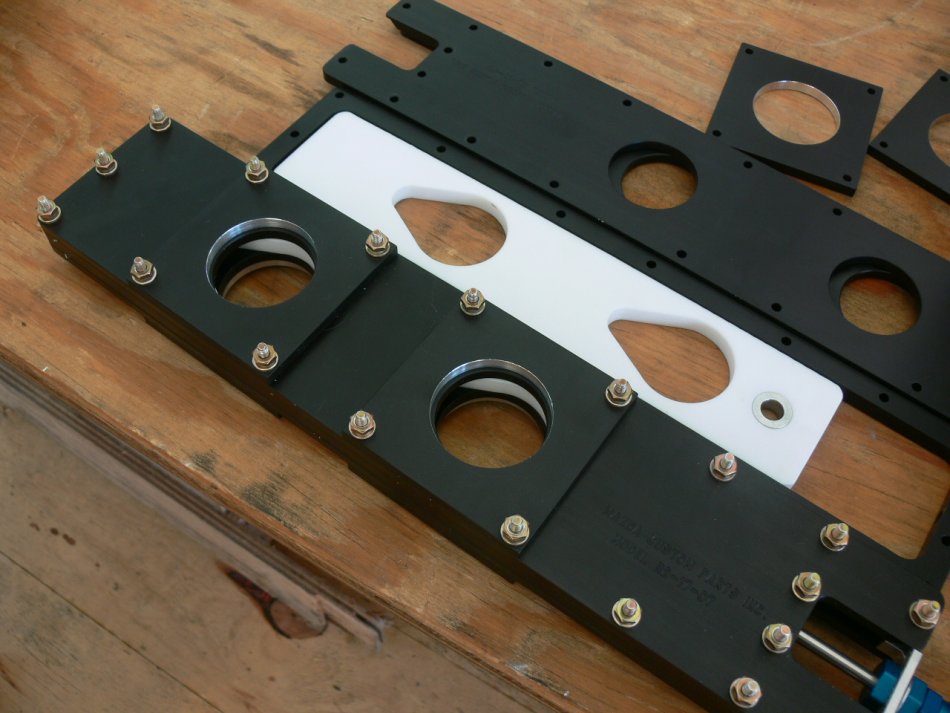
Steve, consider offering the Teflon slide throttle. Aircraft engines spend 90%
of the time WOT and the slide throttle has no internal aerodynamic drag so the
BSFC and power is better. Here are some pictures. It is cheap if punched out on
an NC punch. Ten or more holes sets are punched at one time and then the covers
are sheared to final size. People have complicated them with oblong holes, NC
mills and rounded ends but all that does is increase the cost. Mazda engines are
chosen for aircraft because of the lower cost so the idea is to keep the cost down.
Paul Lamar
--
The Rotary Engine NewsLetter. Powered by Linux.
ACRE NL web site.
http://www.rotaryeng.net
Youtube key word UTUBPLEASE
Copyright 1998-2008 All world wide rights reserved.