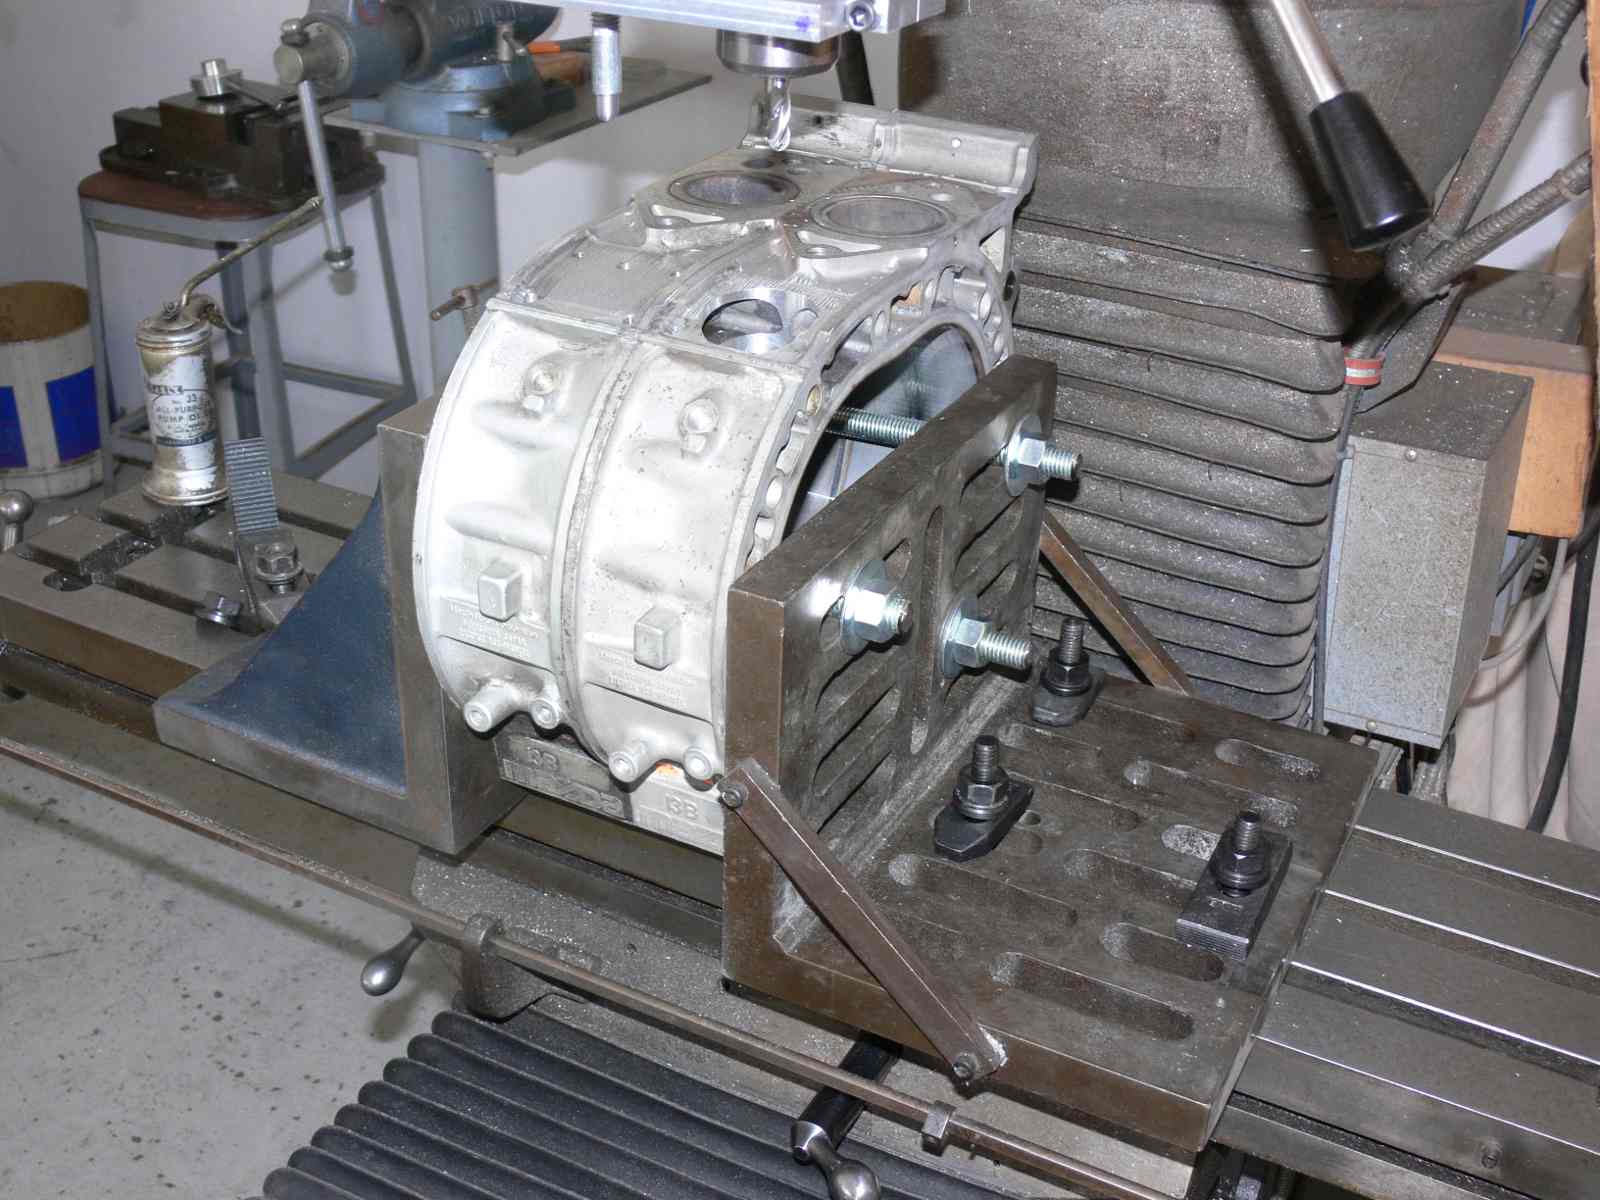
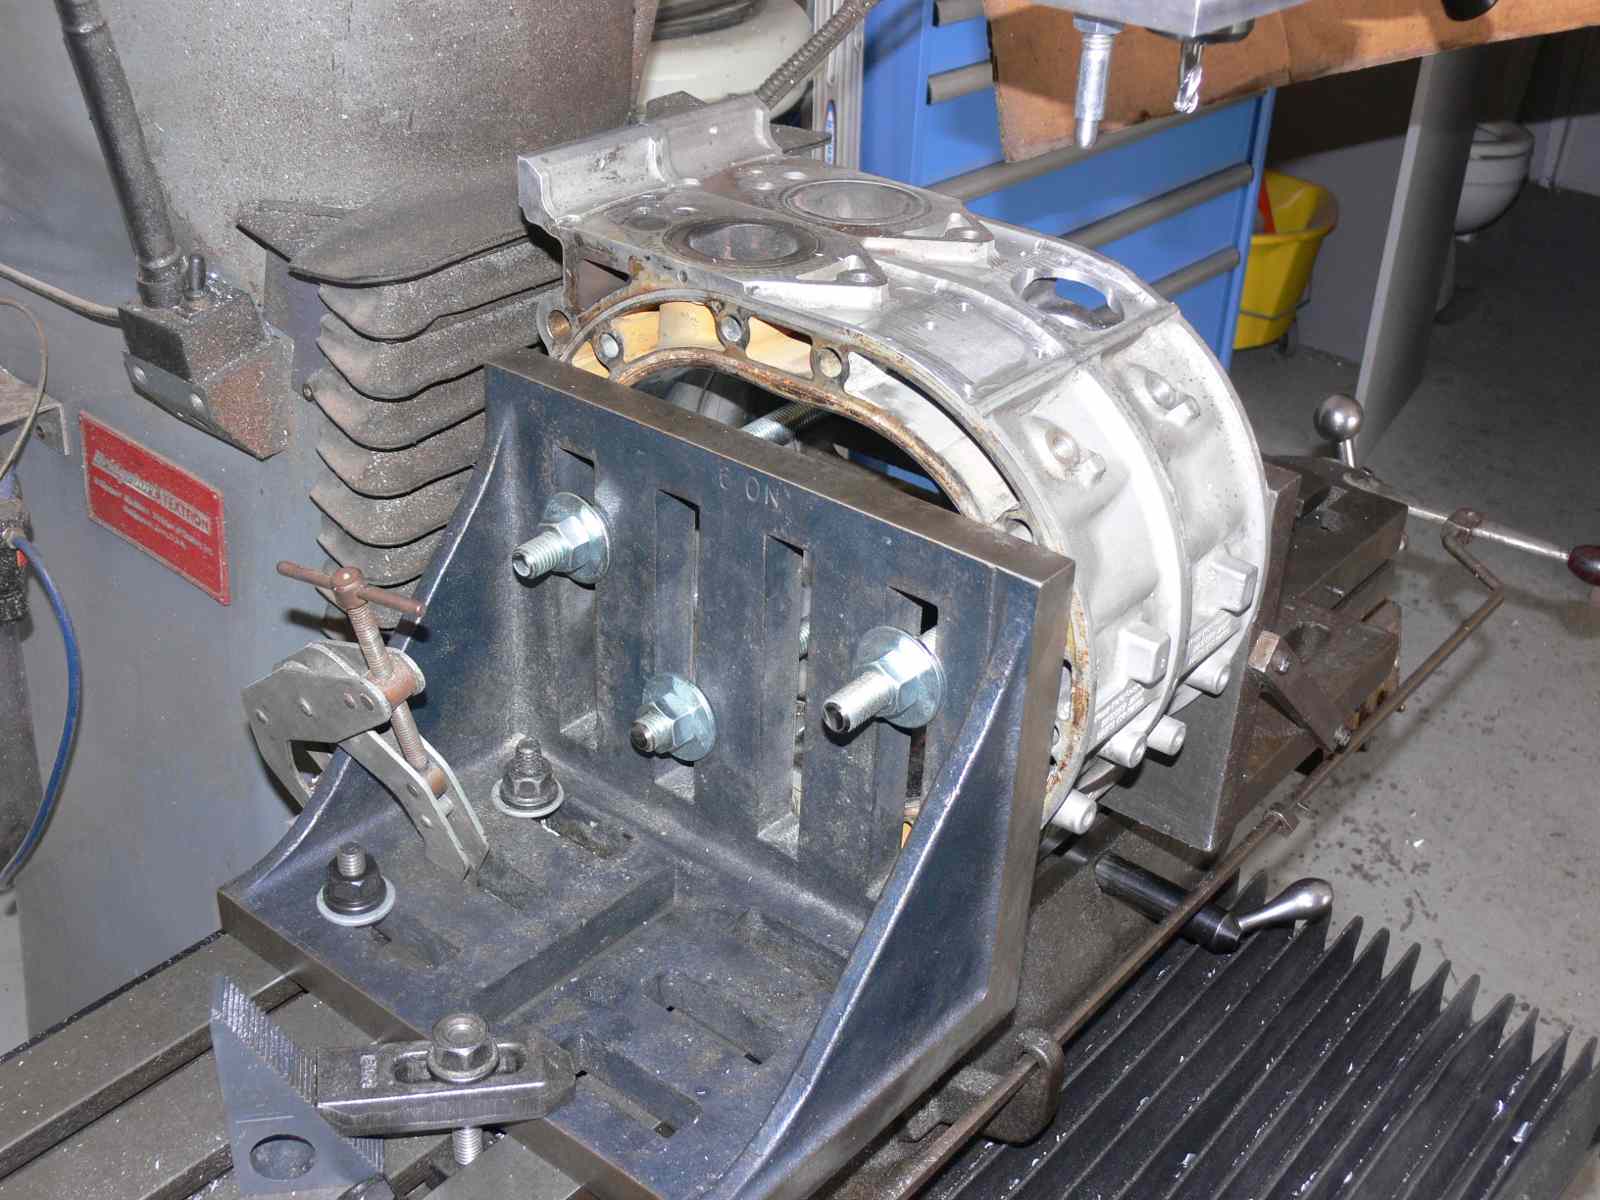
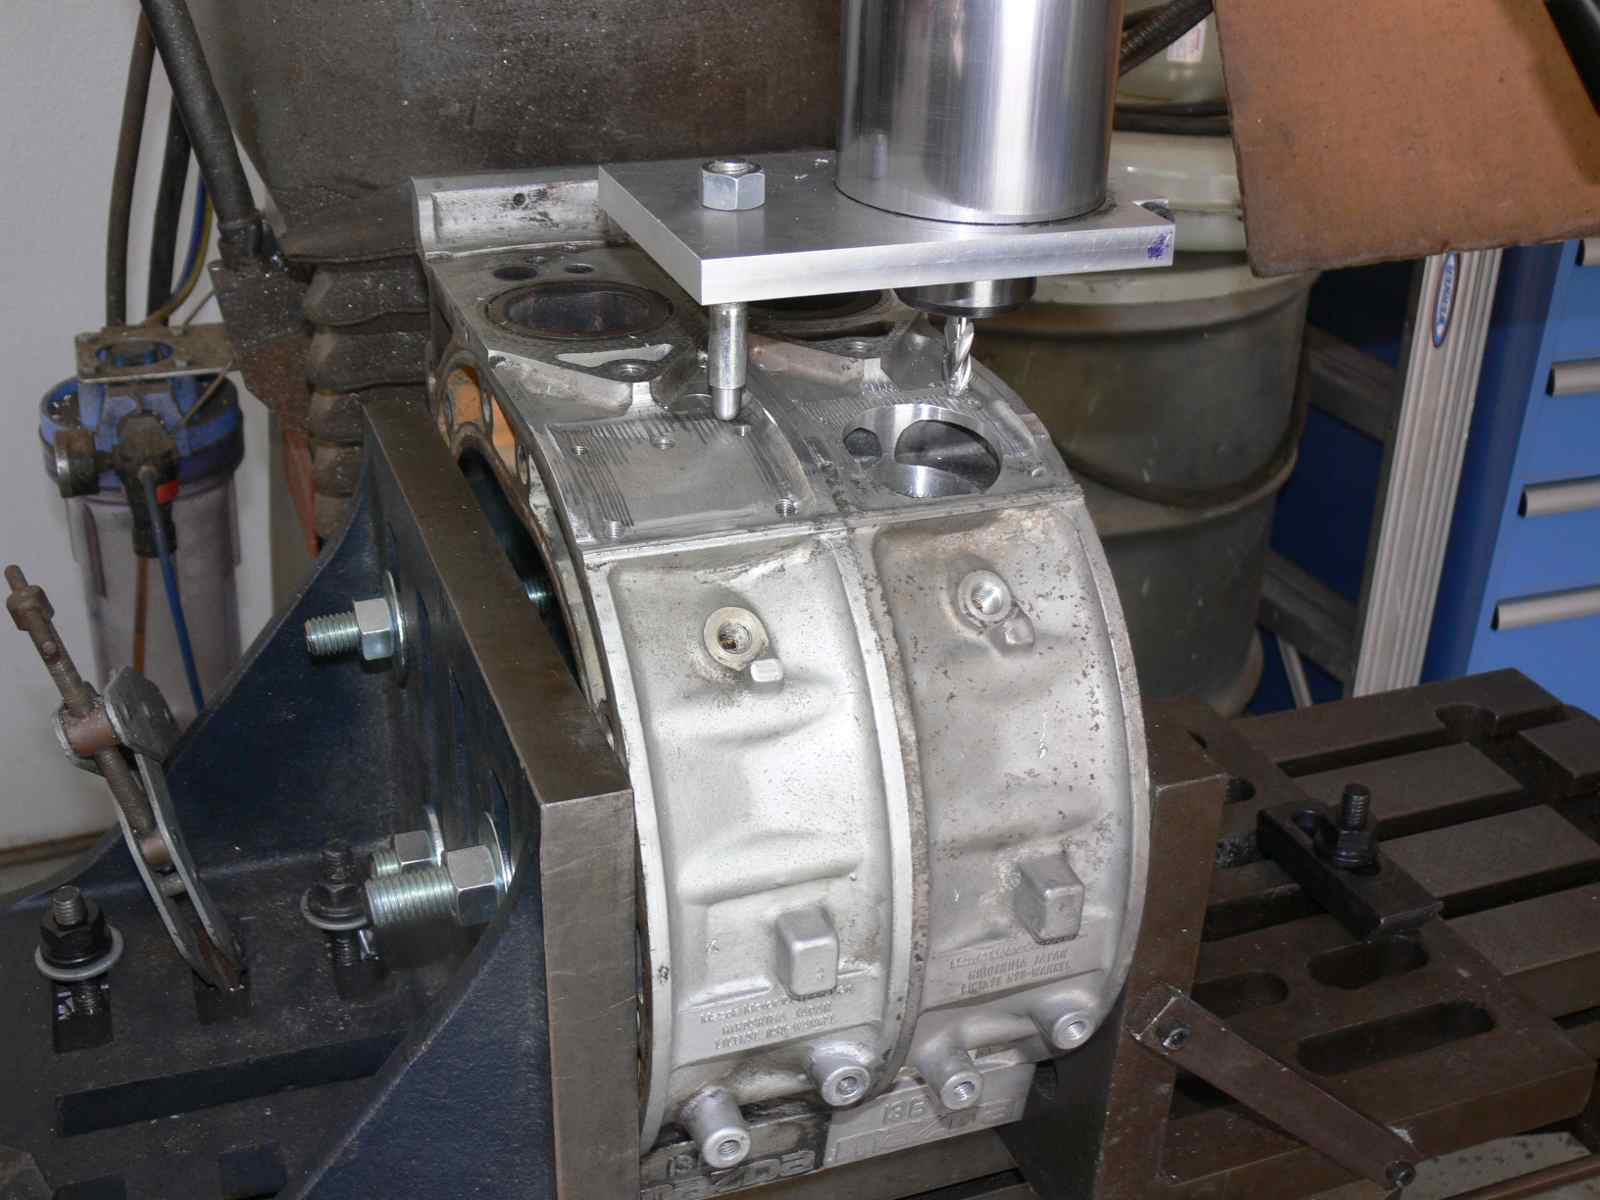
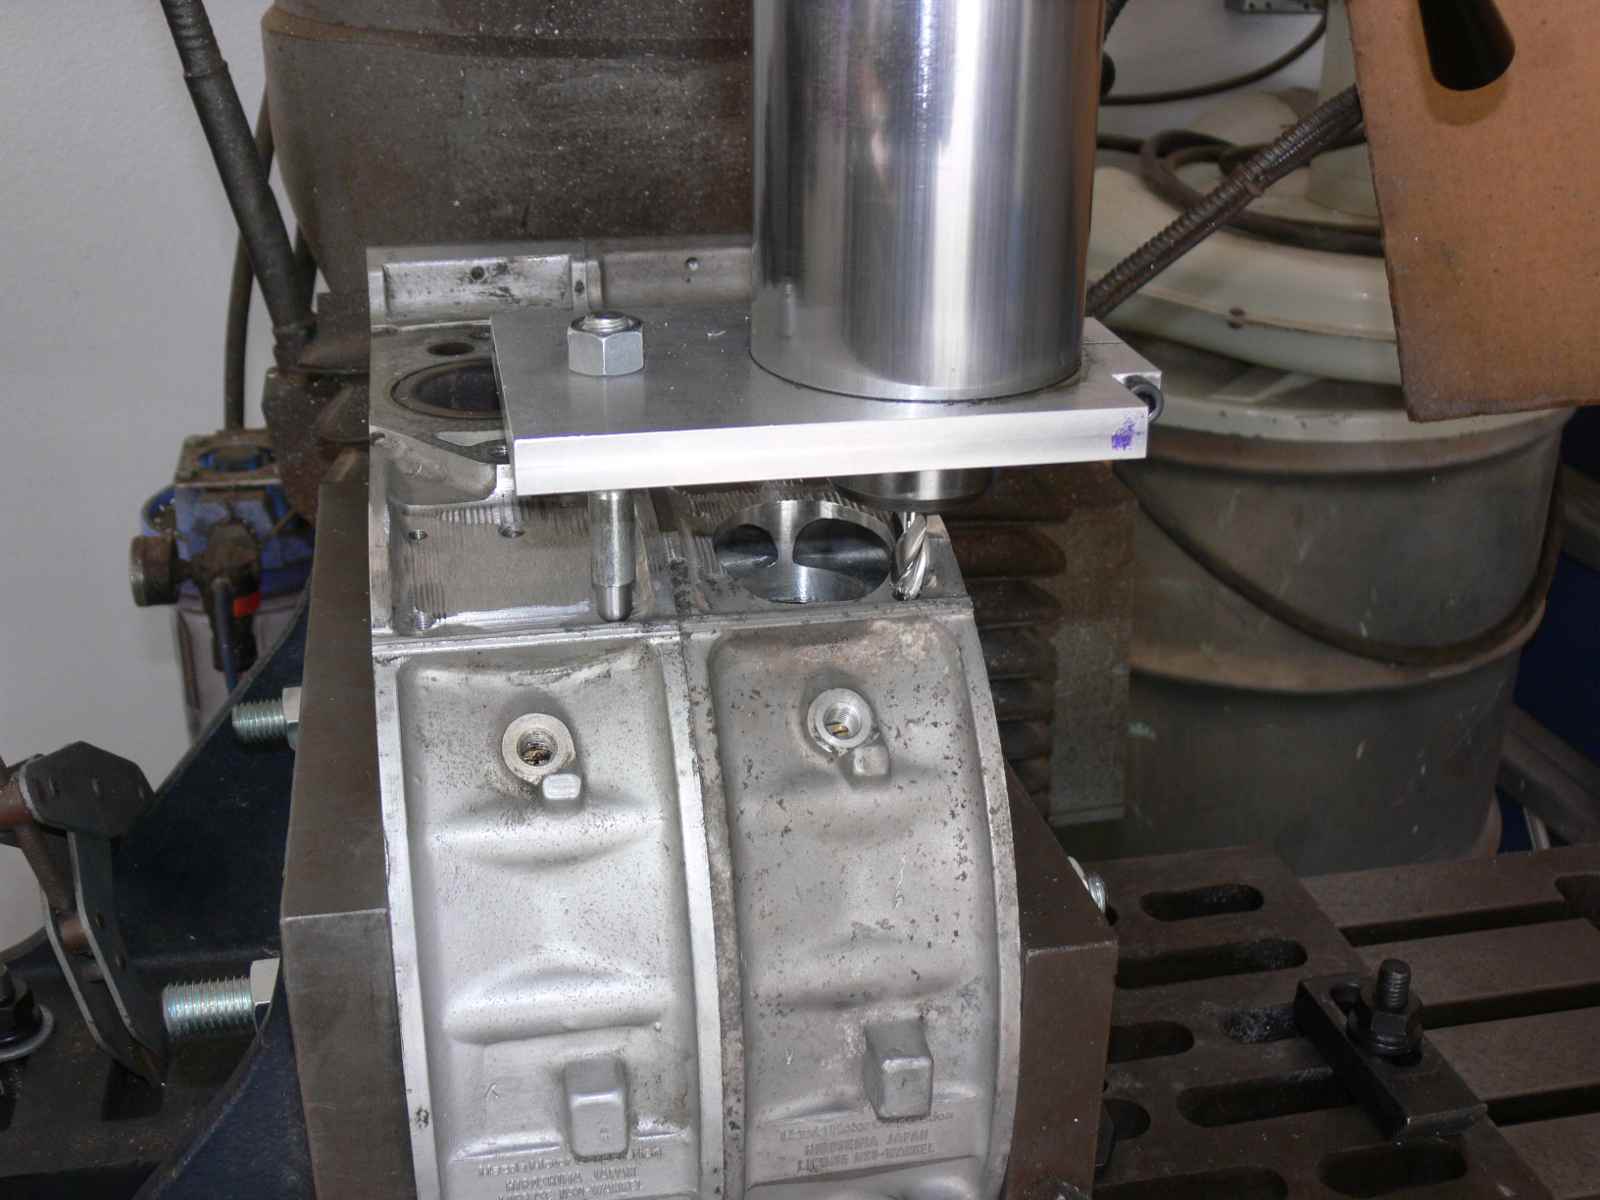
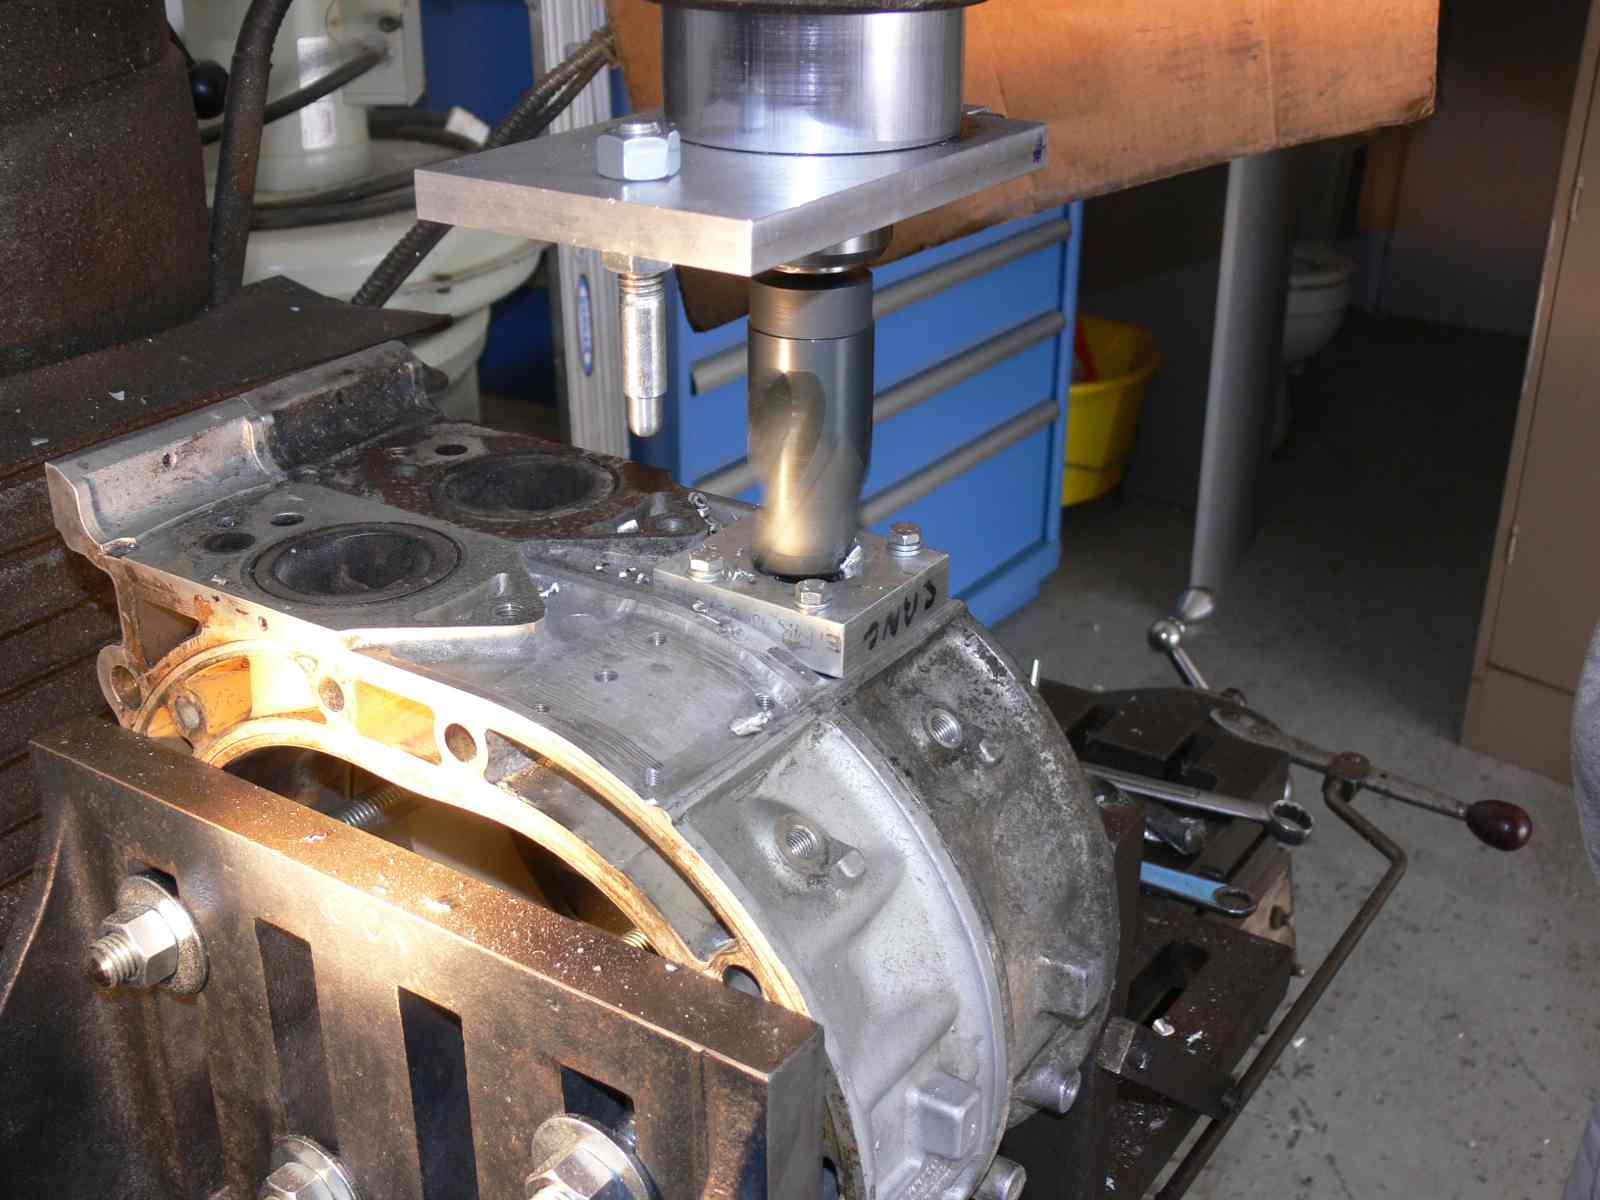
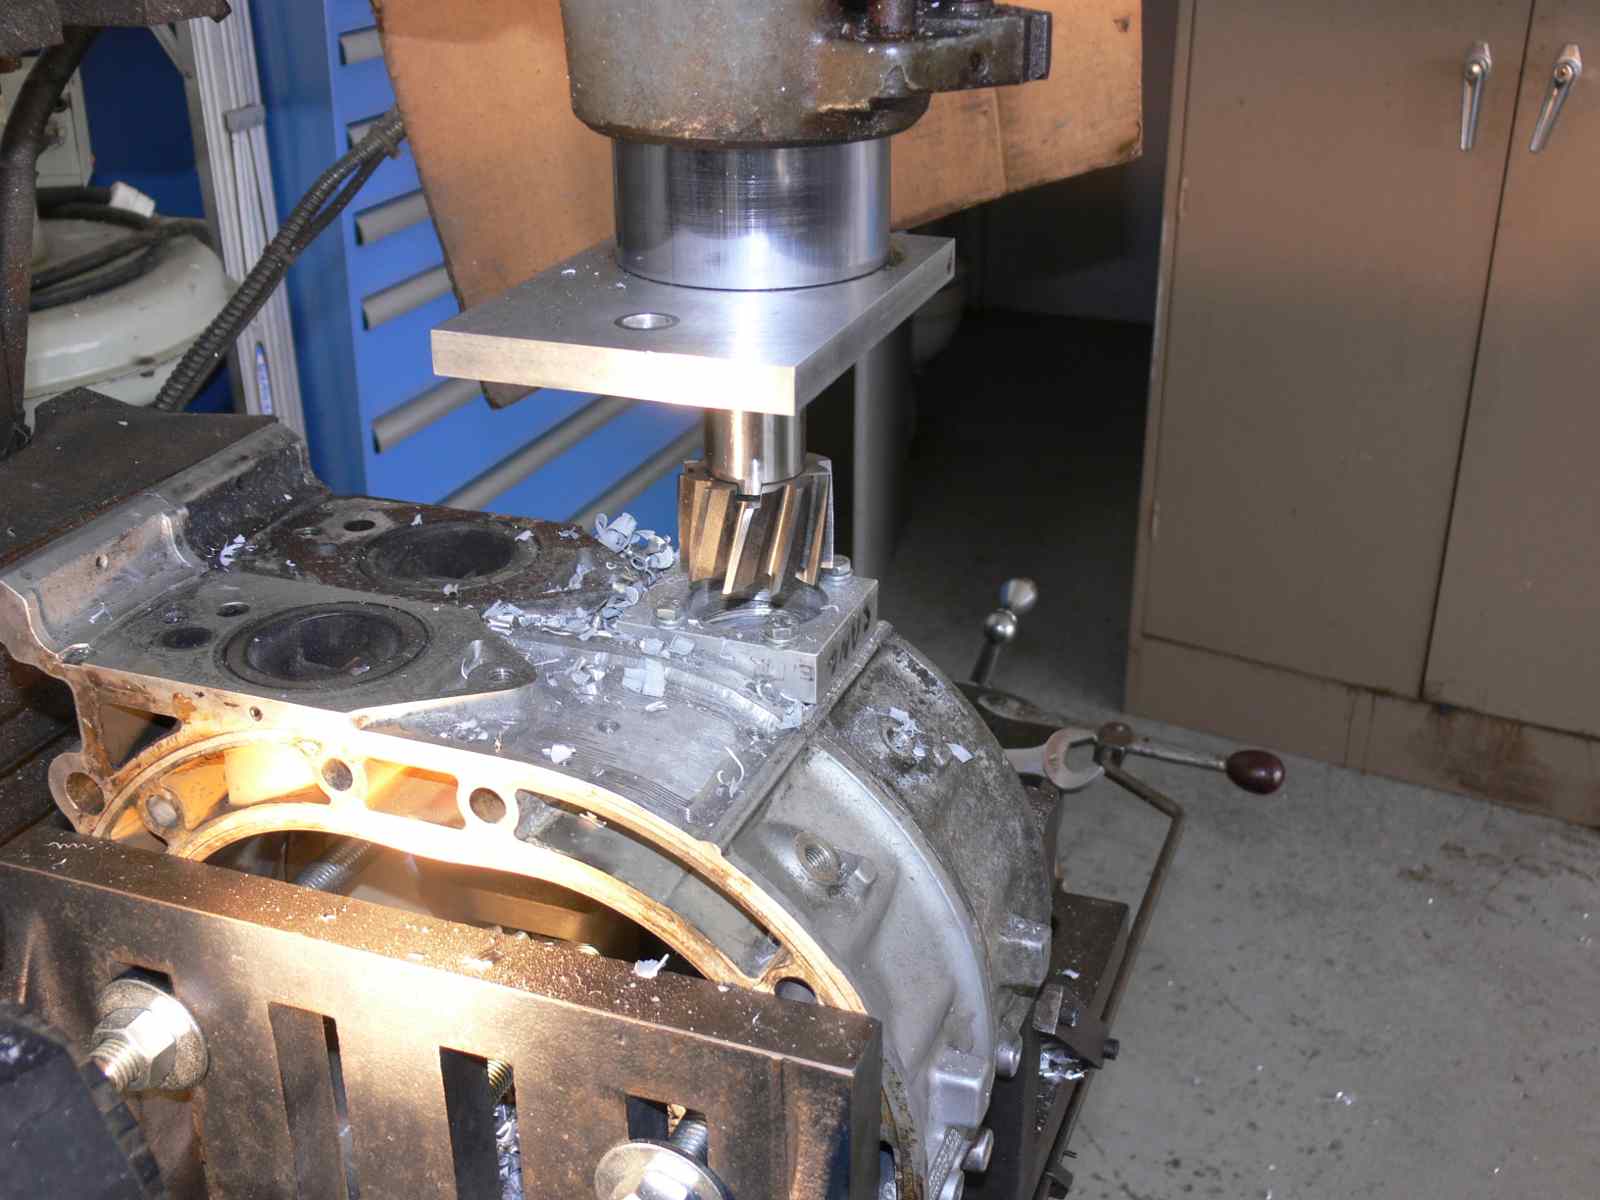
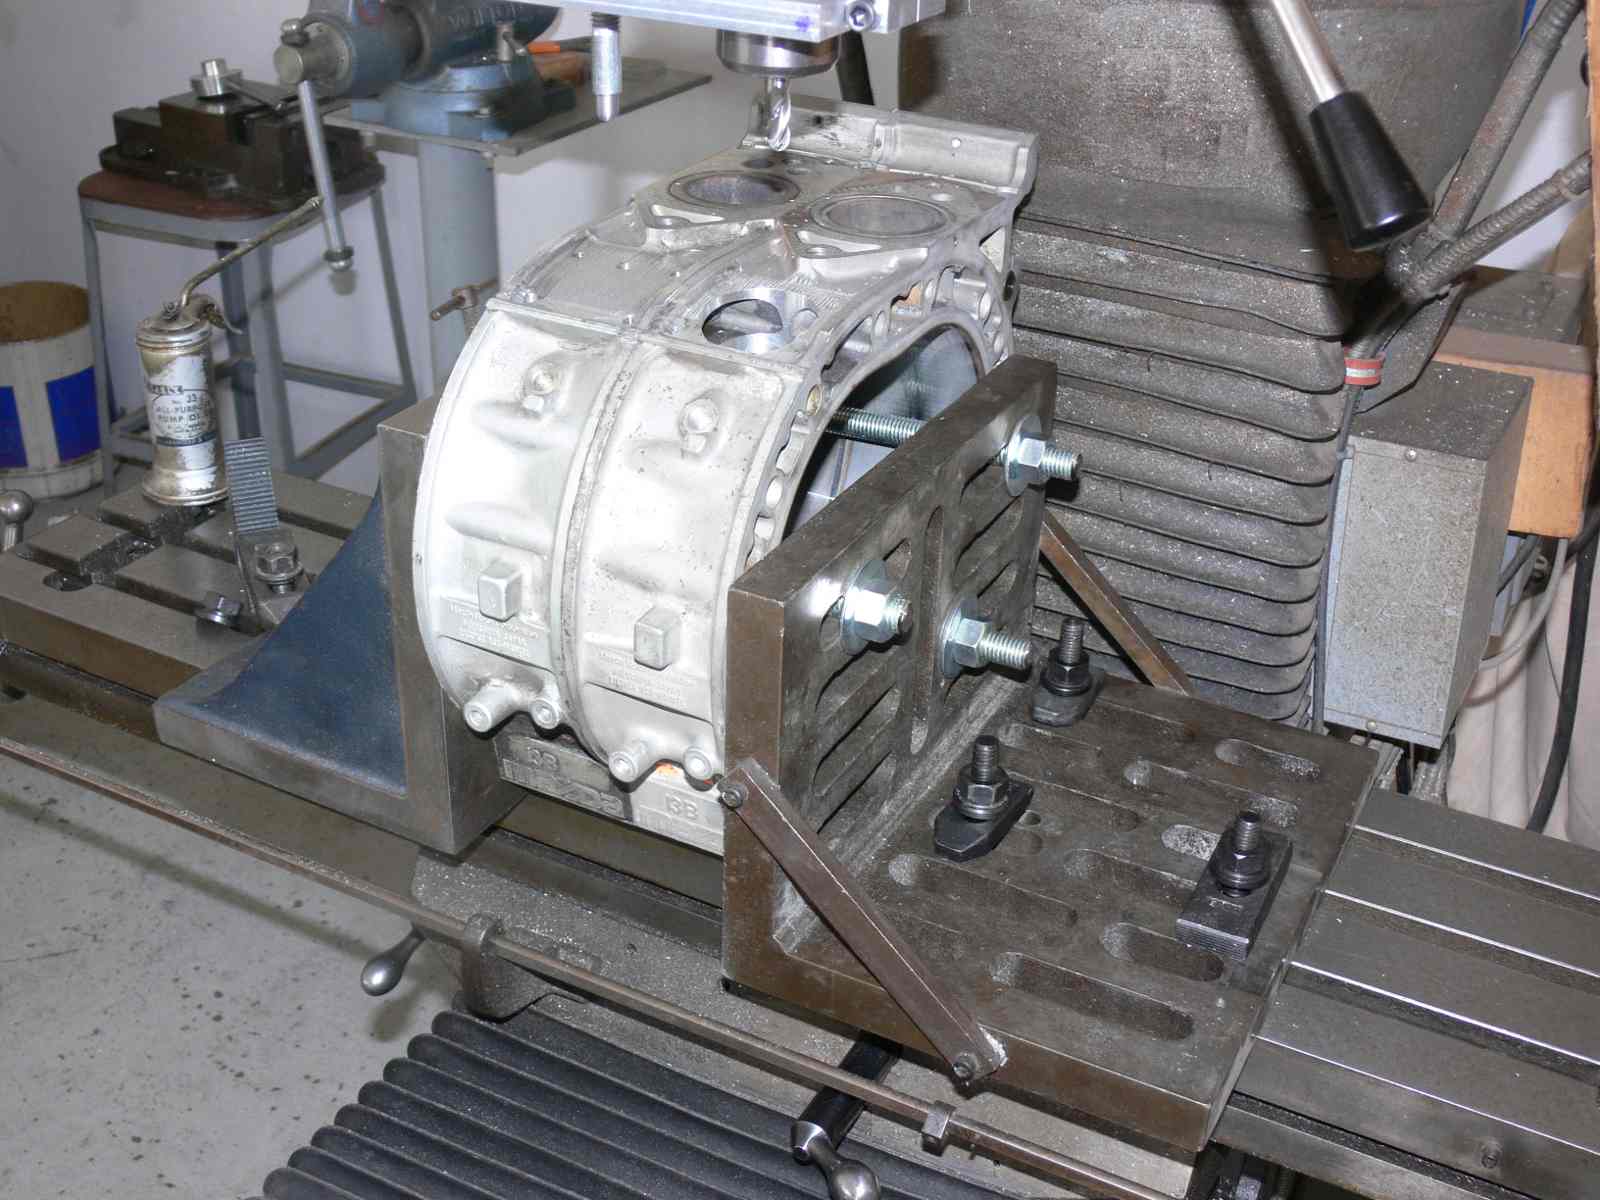
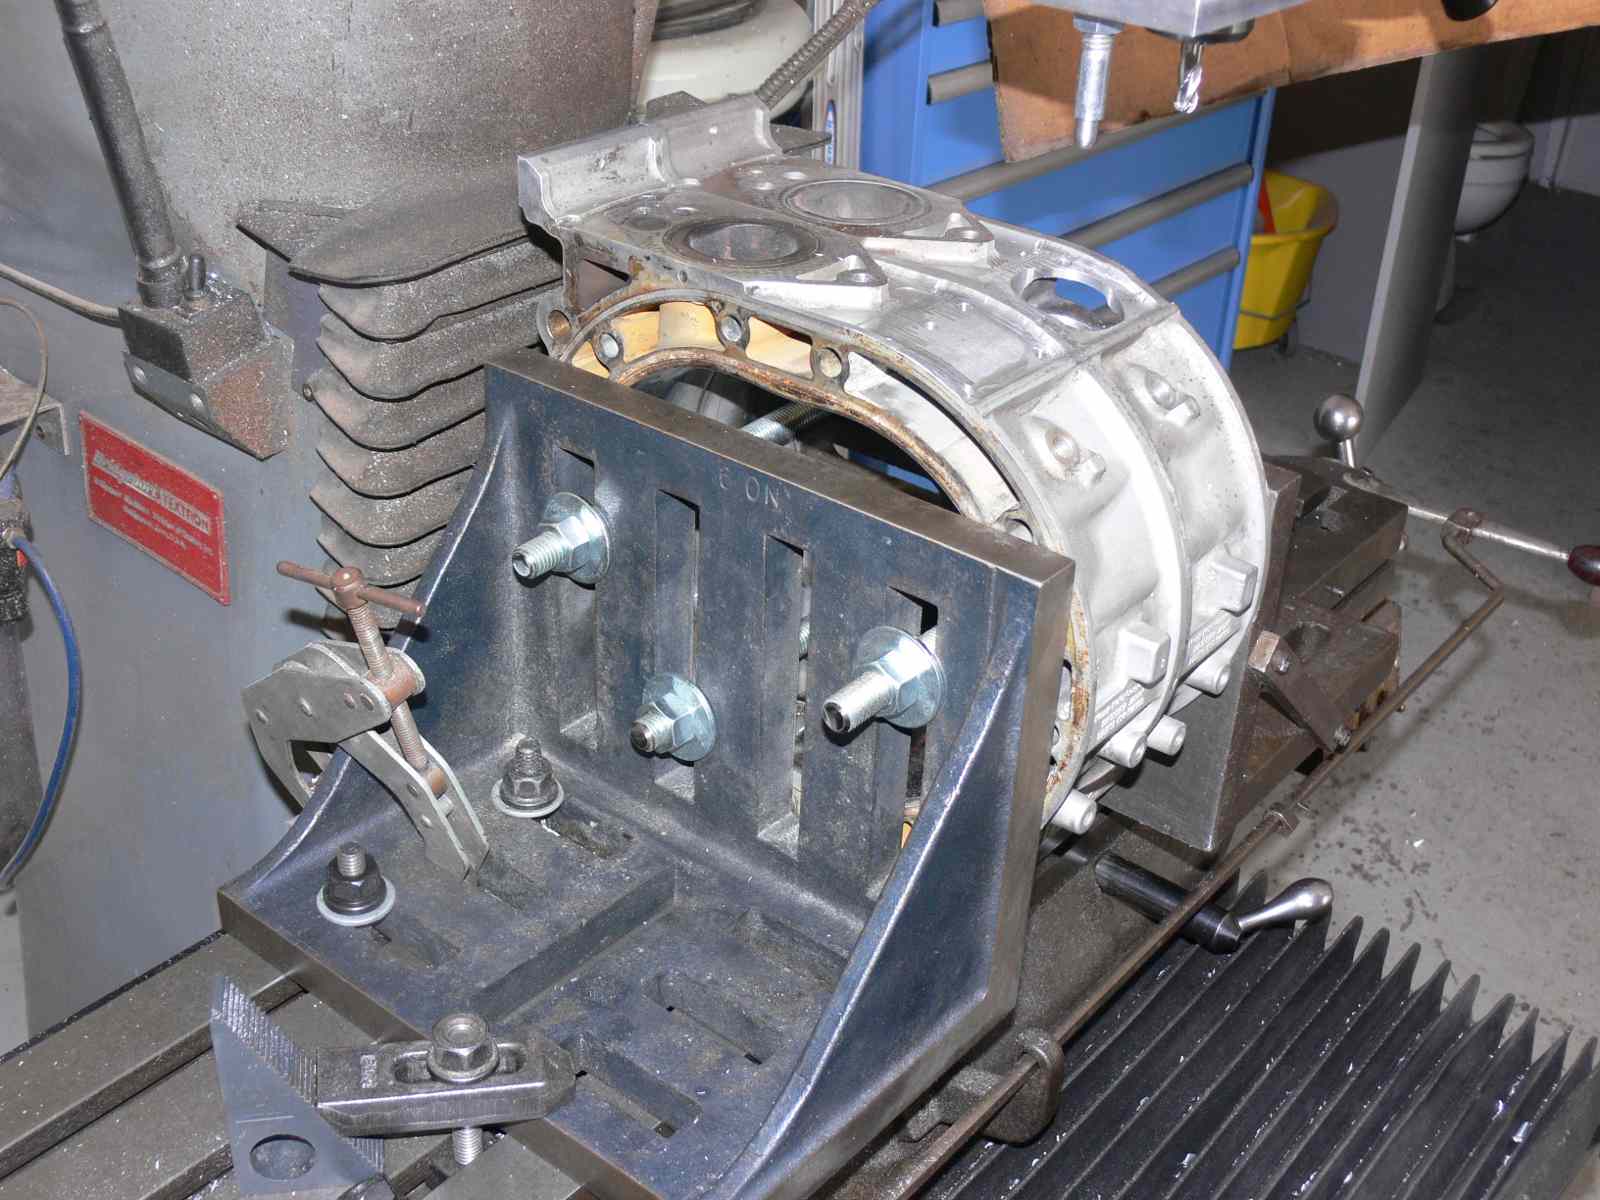
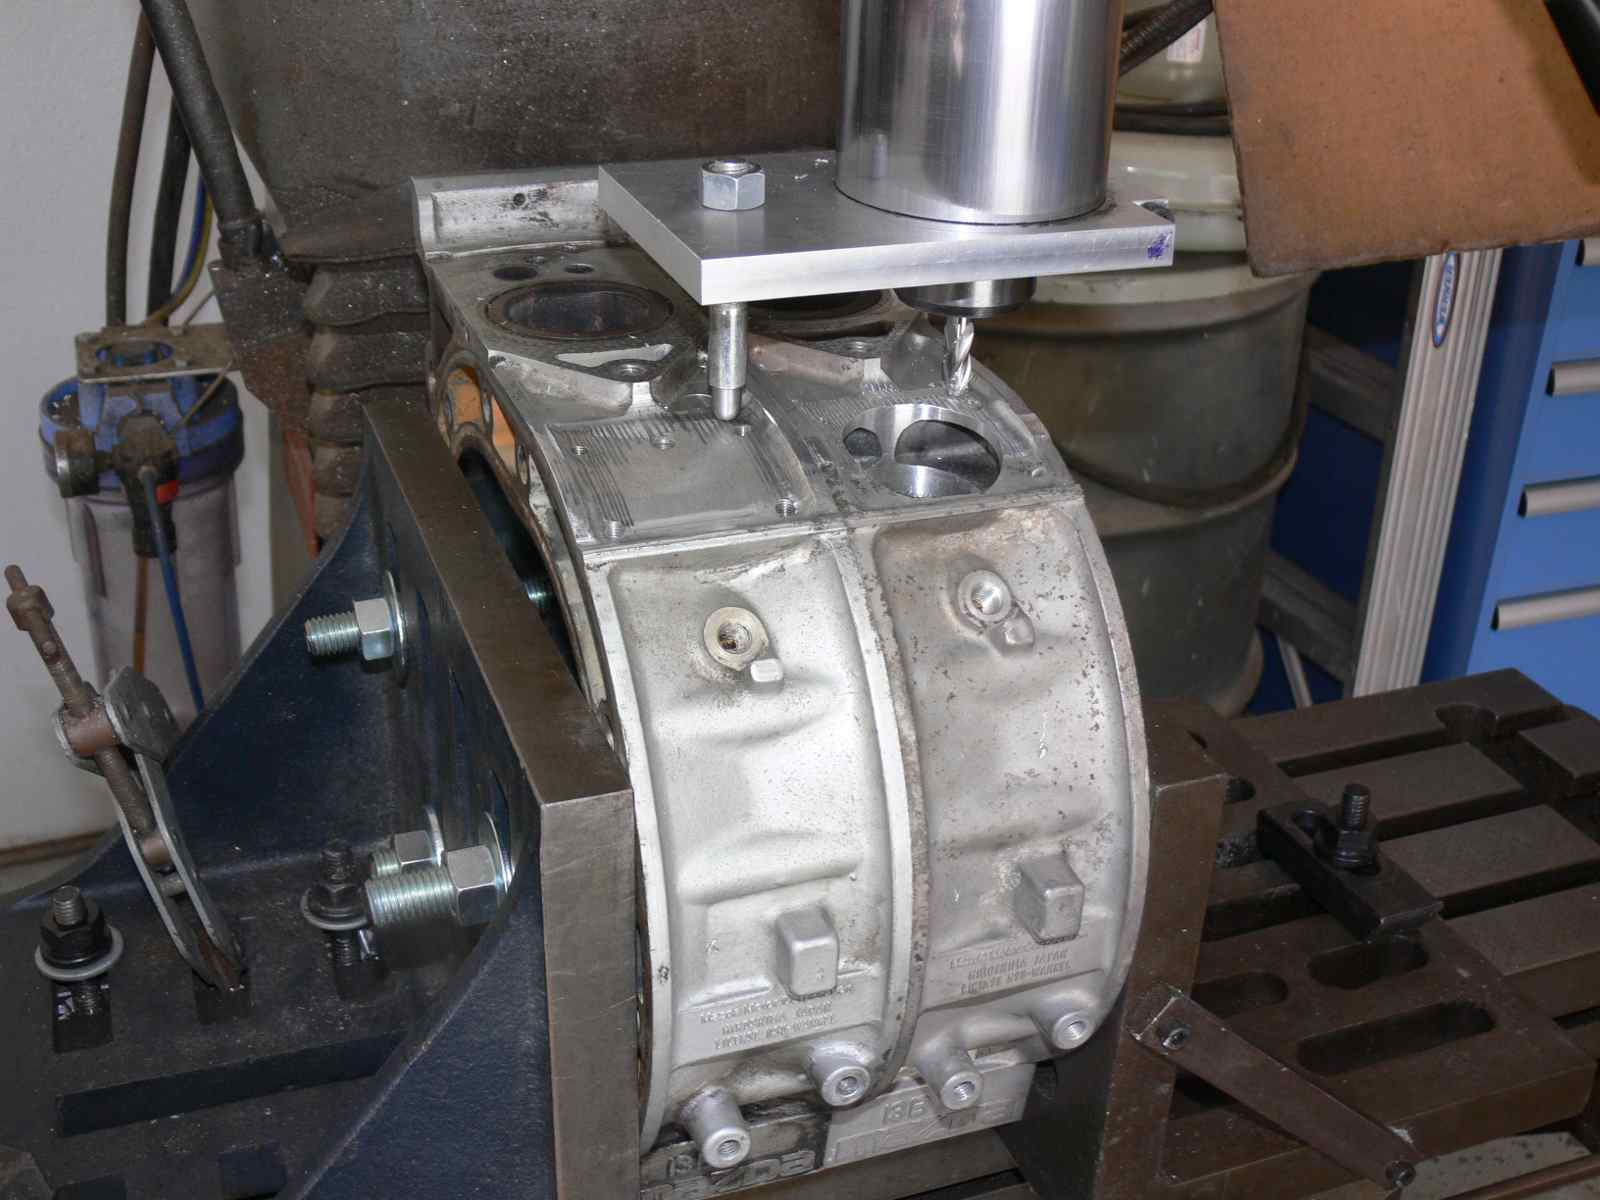
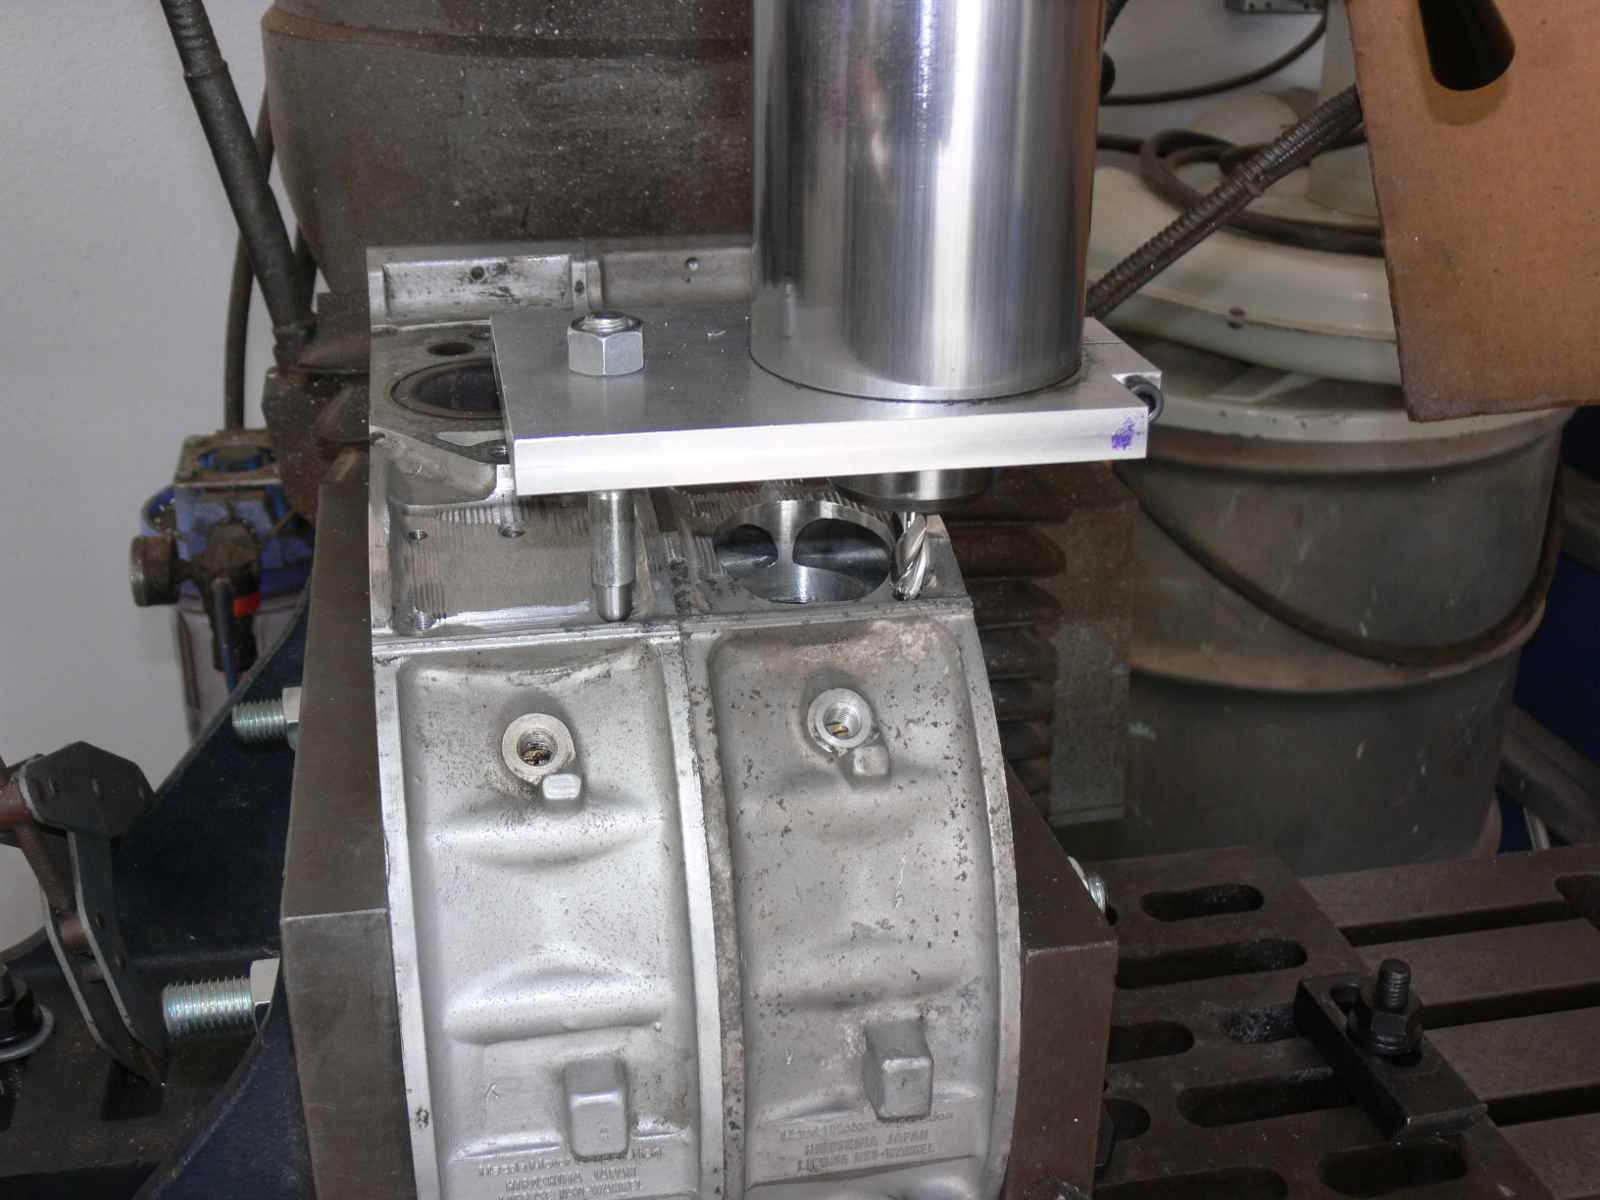
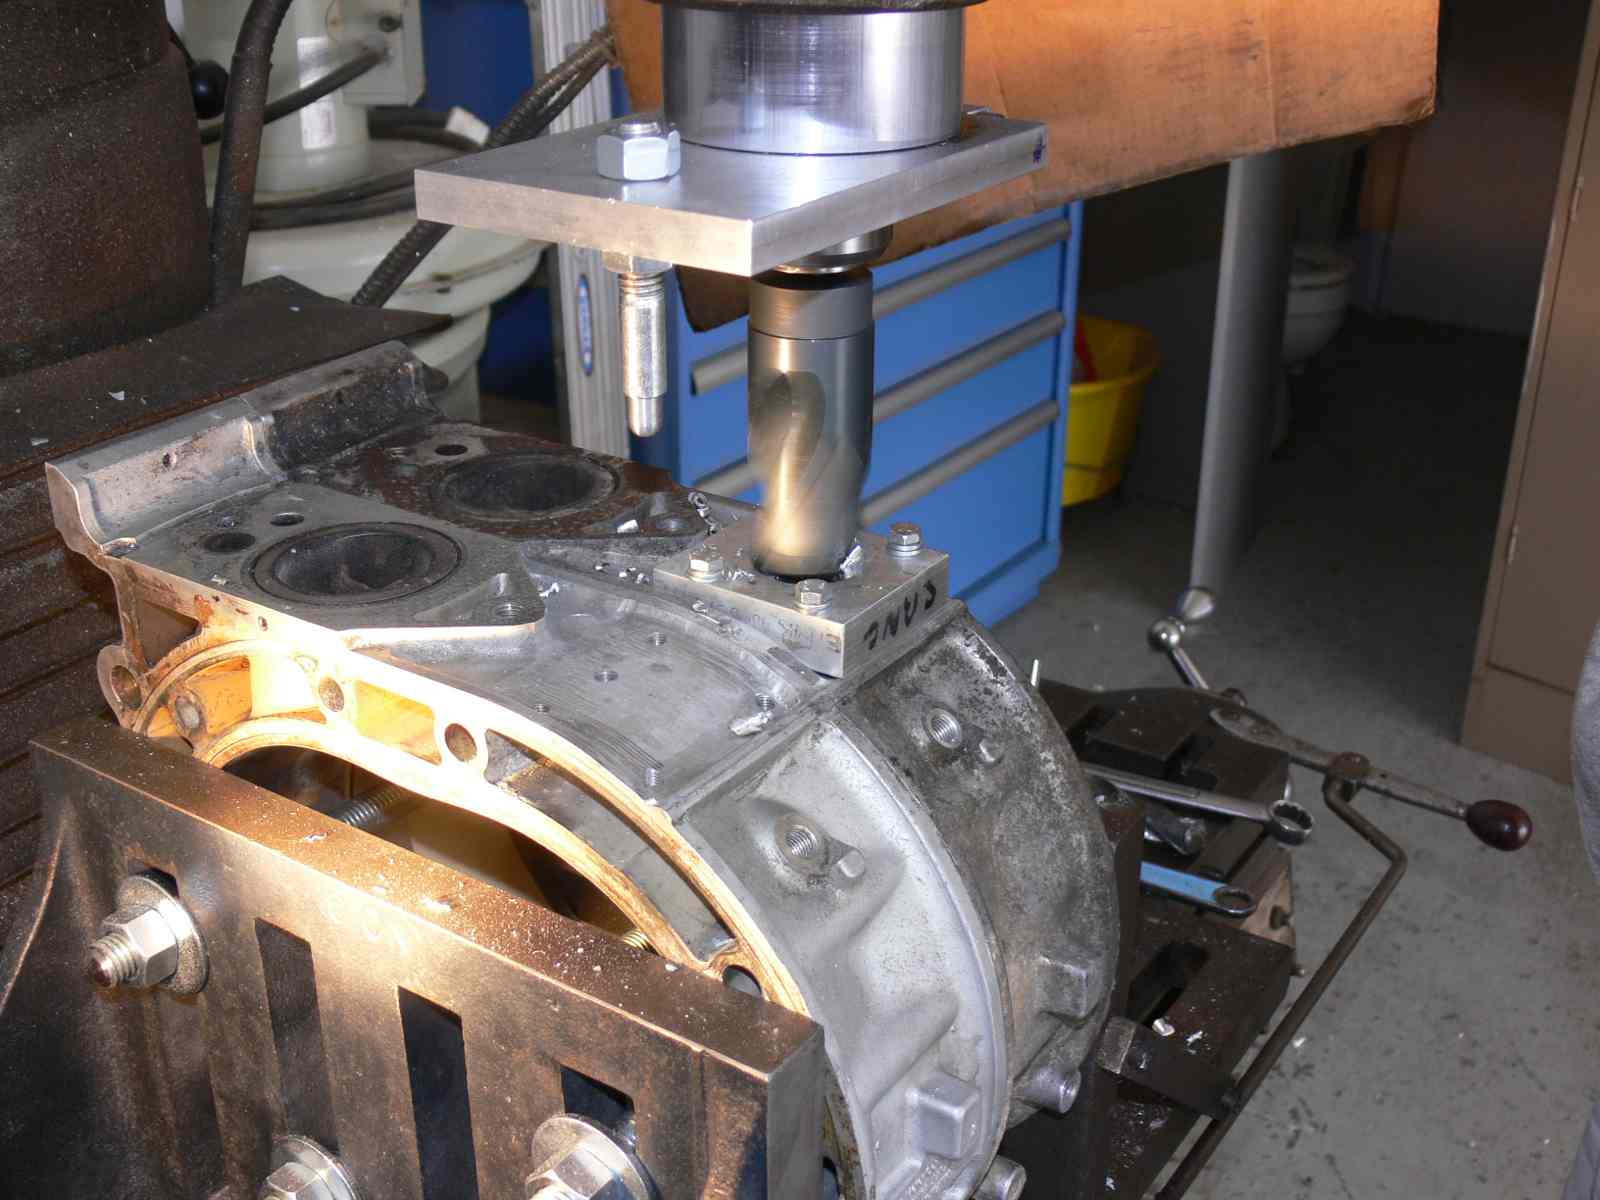
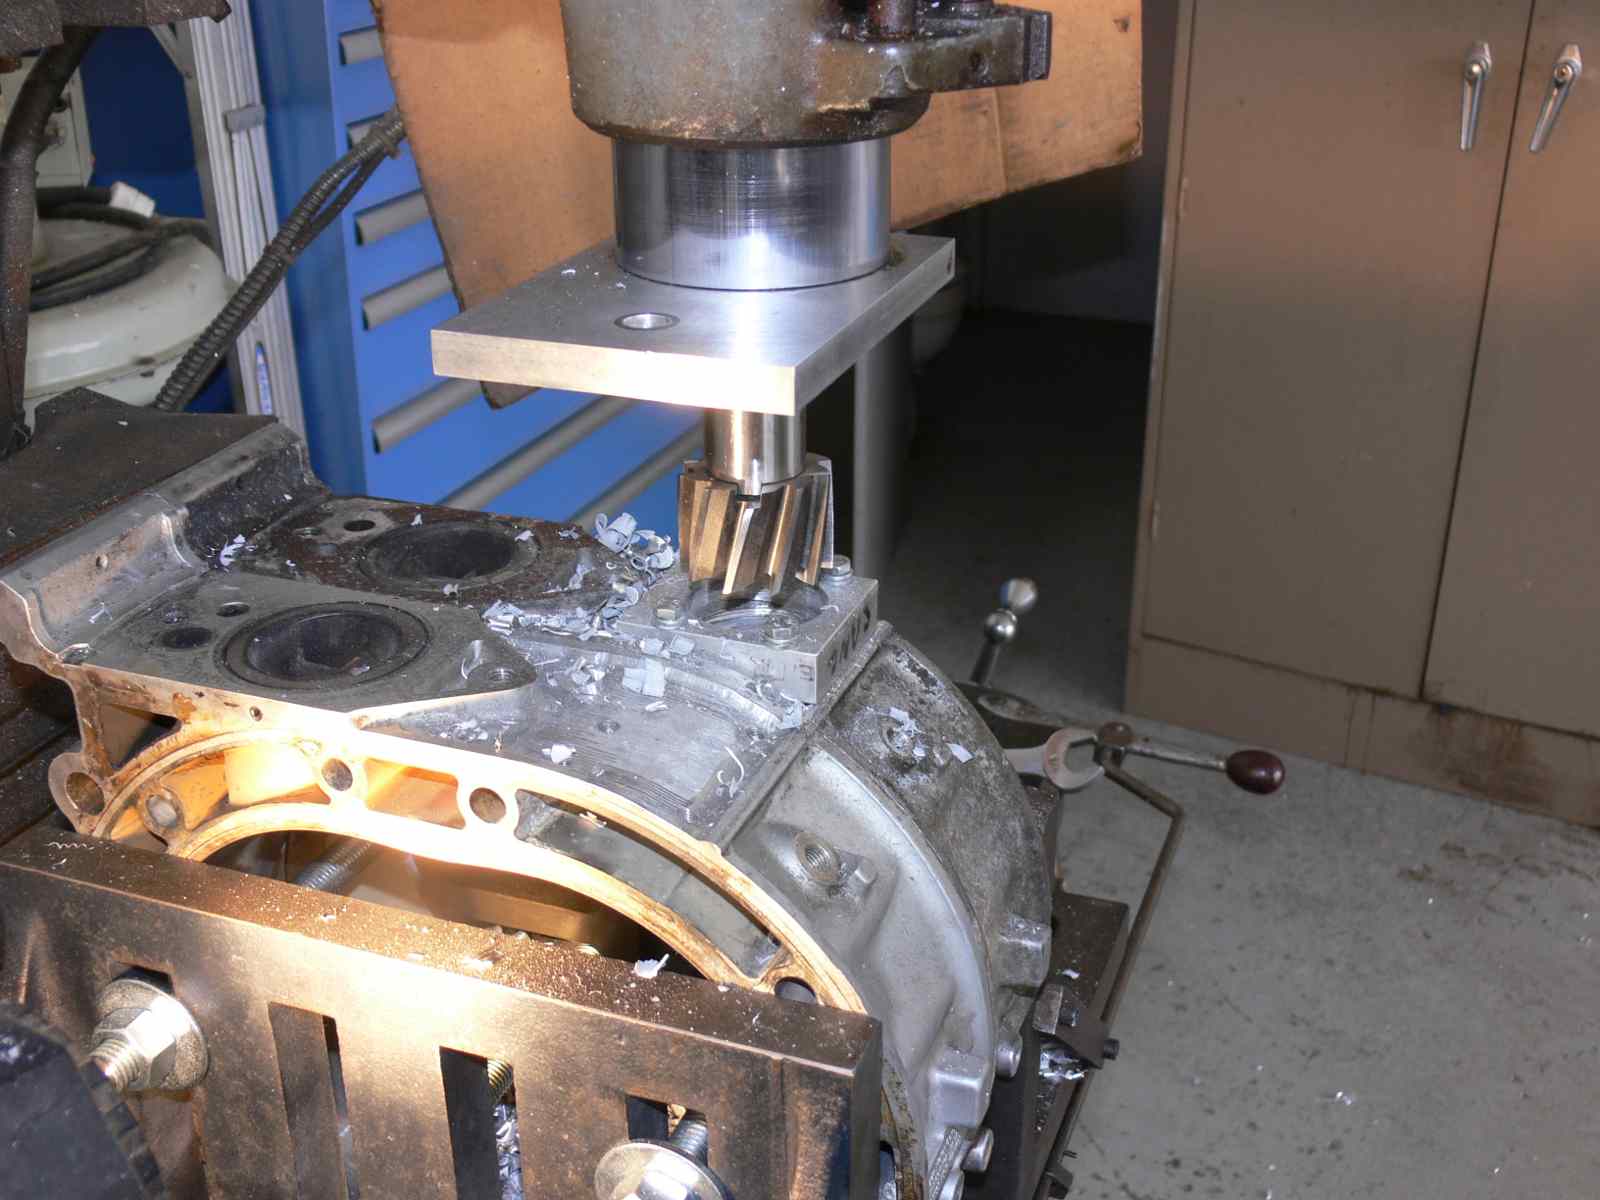
This is not all of them. There are four more.
We have done a couple of junk rotor housing so far to tune the process.
The biggest limit on how fast you can drill a 2 inch hole in a rotor
housing is the
rigidity of the mounting fixture and the power and rigidity of the
mill. Compared to a
Cincinnati or Kasuga a Bridgeport is a wimp. There is NO substitute
for tons of cast
iron and lots of HP :)
http://www.youtube.com/watch?v=7odN-h7rsGQ
We now have two angle plates bolted together with four pieces of
5/8th inch diameter
threaded rod and eight 1/2 inch hold down T bolts on the Bridgeport
mill. I wish my
Kasuga were running.
-----------------------------------------------------------------------
One of the other things we tried was an experiment with the weld on a
junk housing.
We recessed the tube 1/32nd into the bore resulting in a much lower
profile weld so you
won't have to do much die grinding to clean up the transition. The
weld bead is almost
flush with the rotor housing wear surface. It never ceases to amaze me
how well these
welded p-ports work. IMHO it is the only way to go.
On the other hand you will need a special long tap so the tap handle
will clear the SS
tube. The tube protrudes about 1.5 inches at the top. This needs to be
done to clamp the
sealing blocks to the rotor housings. I recommend a Greenfield
EM-AL-GUN-TAP 1/4-20
Rutland Tool & Supply part number 7116 4207 Cost is $12.73. This tap
is 3.15 inches
over all length. Drill the top left tap hole about one inch deep. That
is the only blind
hole. The other three are through holes into the water jacket.
Take your time and don't screw this up as a repair with a helicoil set
could be real
difficult.
We have done the hard part. It is up to you to do a bit of time
consuming finishing
work. I can't promise when we will ship as the blocks are in the NC
shop for the O-ring
groove. I think I will order the right O-rings for you and install
them in the blocks.
Here is another idea. Instead of using uncured red RTV silicone rubber
one can buy cured
RTV in films to use as a conformal gasket. Good to 500 F.
http://www.mcmaster.com/#rubber-sheets/=4geun0
Paul Lamar
Paul,
what filler rod is he using when he welds the housing?
Thanks,
Larry
I don't know. I don't think it needs much. There is no load on them so weld strength is
not an issue. A good weld without porosity is more important for pin hole leak problems.
I'll ask him what he is using.
--------------------------------------------------------------------
Here is what the set up looks like.
Don't be fooled by the sealing blocks. One person sent us the rotor housing with the
sealing blocks already installed and teh cavity potted with JB Weld. We left them on
there as an experiment when we bored the housings. We will replace them with the new
sealing blocks with the O-ring in them.
The blocks are finished and waiting for me to pick up in the NC shop.
Paul Lamar
--
The Rotary Engine NewsLetter. Powered by Linux.
ACRE NL web site.
http://www.rotaryeng.net
Youtube key word UTUBPLEASE
Copyright 1998-2009 All world wide rights reserved.