HI PAUL
There is there up dated design gearbox for constant speed prop shaft ,
Jean Prudhomme
Jean,
I am curious about where the oil supply for the CS prop is getting into
and
out of the PSRU. Is it feed off the engine oil? If so, is the PSRU lubed
with
engine oil?
Dale Davies
Yes Paul [Dale?] from the engine oil system true prop governor and return
to
engine oil pan,the casting have already a port connection for the return
line on
the middle of larger bow part of casting it can be turned a different
position
on bottom of side depends on oil retention on gearbox.
The prop governor have to be driven by belt but the spline shaft have to
be
lubricated or if already one available for belt driven
Jean Prudhomme
Paul
I have to built passageway to each main shaft bearing and return to the
main
housing.
Cutted Half small aluminum tubing heavy gauge will be welded outside of
the 4"
dia round part as oil lube feeding and the other as return.
I am not at this stage but i do have an idea.
I am well equipped with 250 amps tig welder
Jean Prudhomme
Good morning Paul
I did order a pce of 9"dia by 4" long alum bar,instead of making the rear
pce with 3 pces of tubing and weld involved i found it will be cheaper and
faster to machine from a block.
I found a company who sell by the inches and my pce cost $164.00 with
shipping.
See attachment
https://www.speedymetals.com/c-8342-aluminum.aspx
Jean Prudhomme
Yes that does happen. Thick wall aluminum tubing is EXPENSIVE,
The trick is to find somebody with a really
big old powerful lathe and a bunch of 2 or 3 inch drills to drill it
out. I was lucky as there is somebody on the field here
in Santa Paula with a really BIG lathe.
The next problem is finding somebody with a powerful
tig machine to weld thick wall tubing.
Milo has a pattern in the foundry for these castings.
He plans to drop some of them off here Dec, 20th so
if you need a couple let me know and I will ship
them to you.
Paul Lamar
Jean and Paul,
Yes, I was wondering about going from 2 pcs to 5 plus welding for the case.
Is this change still just to use the existing bolt pattern in Jeffs plate?
Please ask Jeff about changing this pattern vs all the machining still
required for the latest design. As a former manufacturing guy I would
rather change one hole size/pattern than make more complex parts to mate up
to other existing parts, AND machine the existing part (bell housing) to
match. How do the stress and weight changes look? (even eyeball over
thumbnail to prints, IMHO easier machining/lighter weight/less stress with
mods to the previous design of Oct 25 and mating changes to the mounting
plate) *:*D How about eliminating one snap ring and installing the input
shaft seal from the inside?
Also, it appears that there are roller bearings on each side of the sun
gear. Will there be stress problems with the input shaft due to engine
crank pilot bushing alignment? How to guarantee this radial fit within say
.005 over 5 or 6"? Does Jeff have alignment bushings in his spacers and
mount plate? Should one of the bearings be eliminated? Just my 2 cents
worth. Project is looking good!
Dan F
I'll let Jeff to speak for himself however
he was kind enough to do these plates for us far below his cost
and he has some left in stock. There is no real need to change
as Tracy's bolt pattern is adequate for Ford based PSRU's.
It is best to standardize on a few things and IMHO this
is one of them. Jean is going off on his own with the
Mini Sprint car cast bell but IMHO that is not the best way
or the cheapest or the lightest given Milo's smaller casting.
The Mini Sprint bell is larger and heavier than it needs to be.
Sand castings are not the lightest way to do things.
One must design them with almost the thinnest wall
the foundry can cast. Usually about 1/4 inch.
Tracy's PSRU works fine it just needs to be ten pounds
lighter IMHO.
Paul Lamar
Paul,
Thanks for the republish of PSRU info. I agree about Tracy box suitability
and weight for 2 & 3 rotor. I am interested for LSA single rotor so will
have modify design for less weight. Jean design has many features that I
can incorporate using 3:17 & 2;85 ratio parts. A local company does carbon
infusion for airplane parts so I will get a quote for housing when I get CAD
proficient. Not expecting it to be cost effective though. What do you
think of thin wall 4130 steel weldment (heat treat and grind to shape) as a
low cost main housing?
Dan F
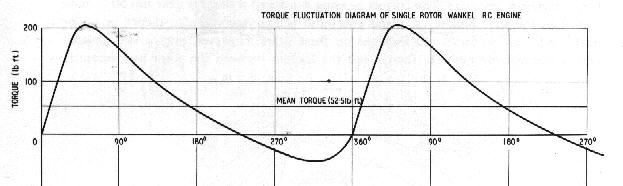
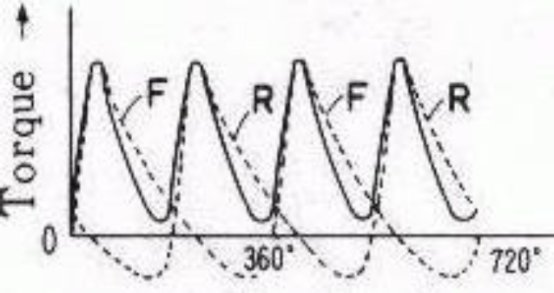
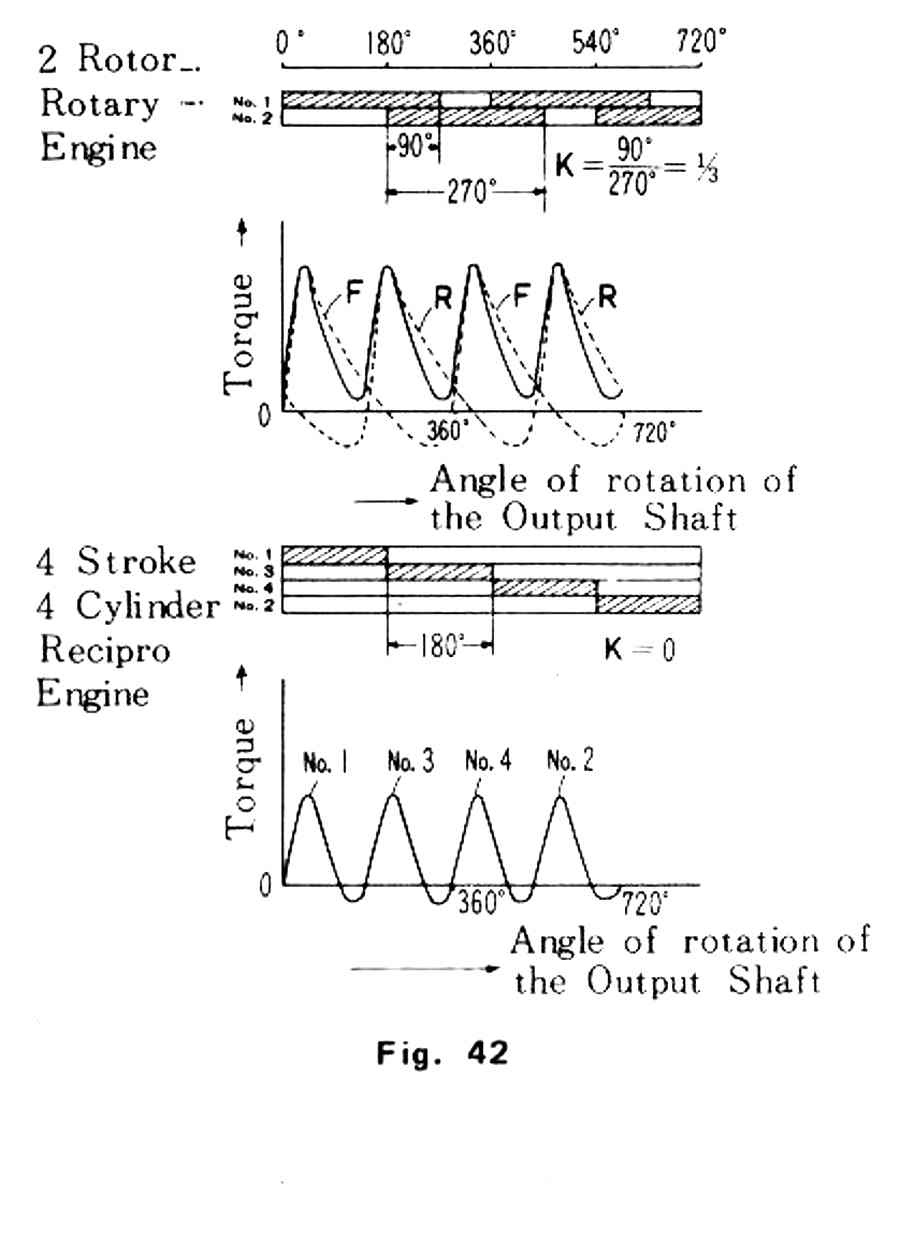
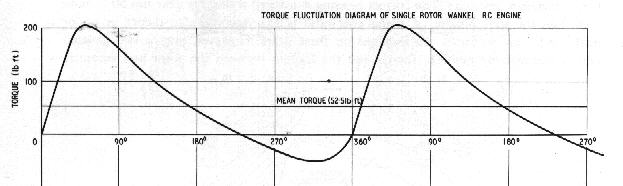
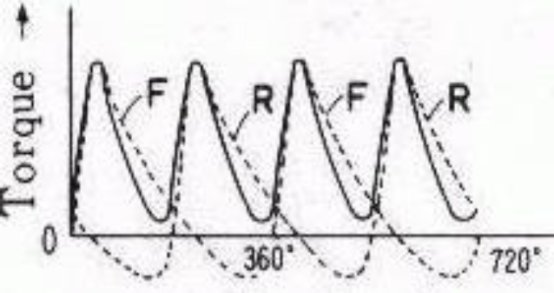
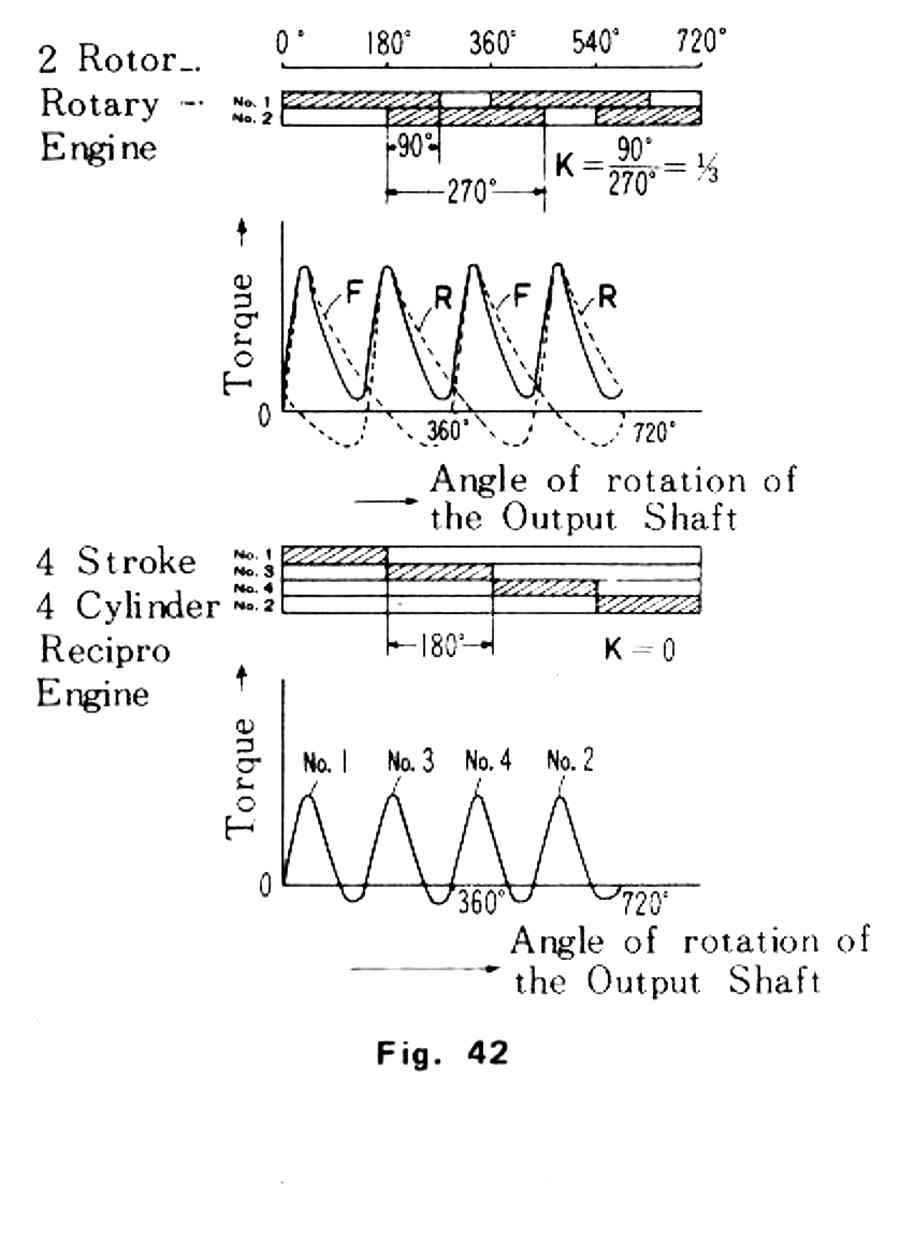
The one rotor puts out an equal torque pulse as a two rotor.
The difference is the 1 rotor torque goes strongly negative so
be wary of cutting the strength of the one rotor gear box.
4130 must be one third as thick as an aluminum housing to have
the same weight. The stiffness to weight ratio will be the same.
Case cracking however will be a much more remote possiblity as
4130 has superior fatigue characteristics. Heat transfer from
the oil inside the case to the air will be less.
Paul Lamar
--
The Rotary Engine NewsLetter. Powered by Linux.
ACRE NL web site.
http://www.rotaryeng.net
Youtube key word PaulLamar2
Copyright 1998-2010 All world wide rights reserved.