Paul
I can purchase round metal to machine my prop shaft and the material
available by the inch is the 8620 cold roll steel.
I will machine the shaft myself and have the splines made it by
outside shop.
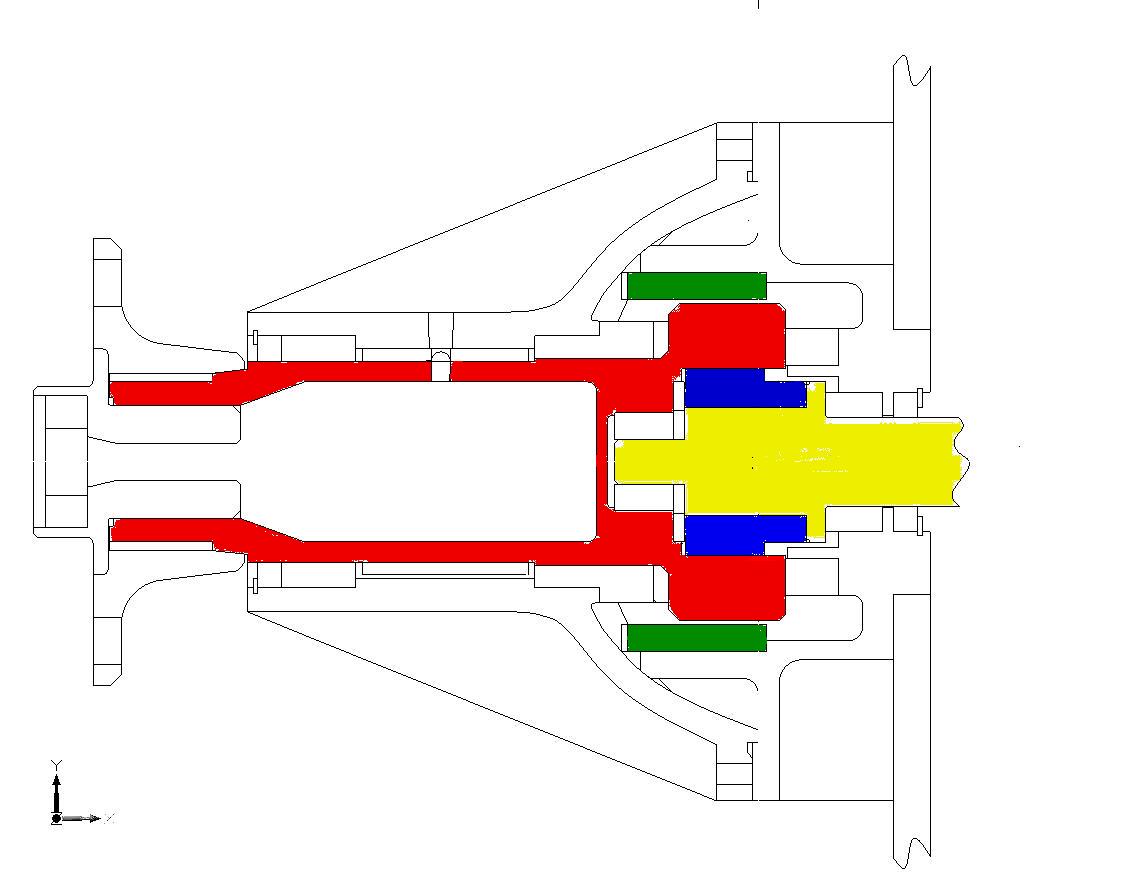
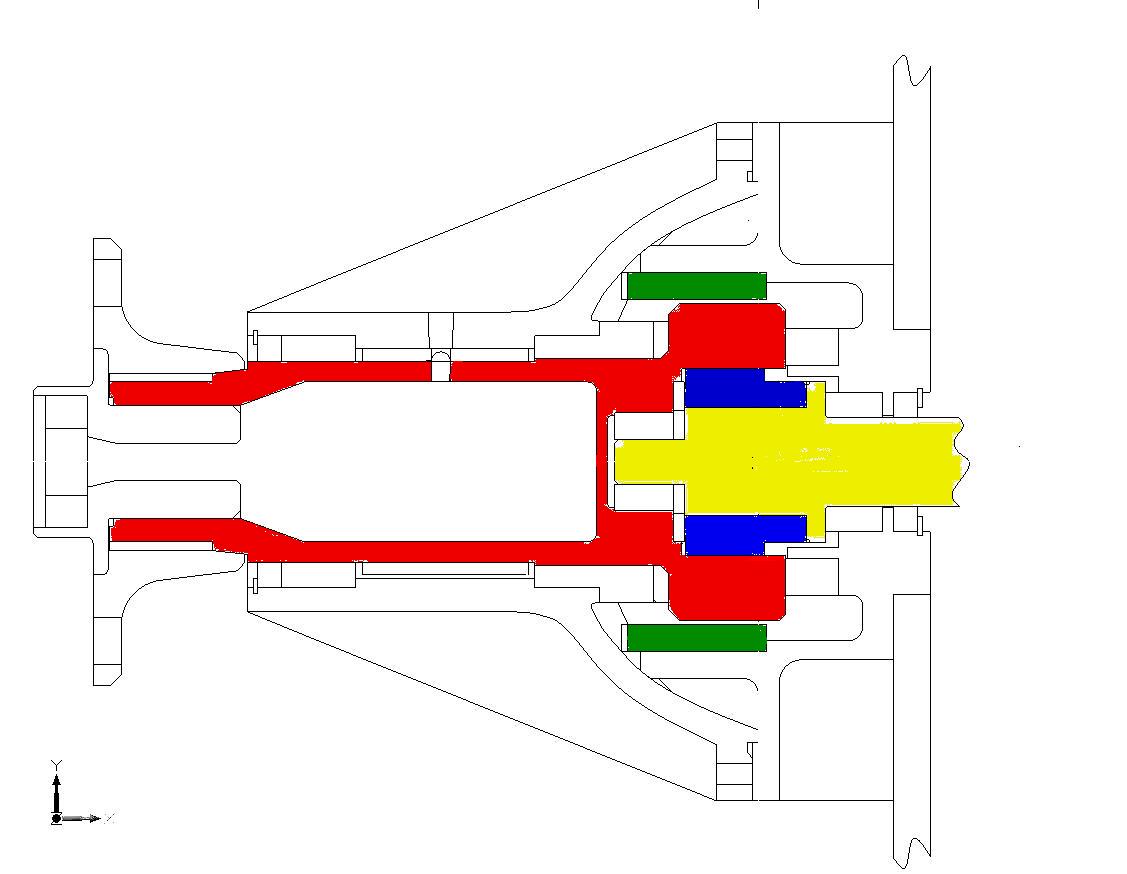
I do have an alternative ,built the shaft with the planet driven by
outher splines or built the shaft complete with the planet housing
and it will be in one pce,the price for material difference is $50.00
but more milling machining for the pinions cages.
I wondering if Jeff can do the milling parts
9" long 4.25"dia is $124.00
8" 3.75"dia is $72.00
I bought a 9"x 24 lathe from Harbor Freight and i should have it soon
There is the 8620 specs;
8620 Cold Roll Steel
Analysis
Mechanical Properties
Applications
Machineability and Weldability
Heat Treating
Tolerances
Speedy Metals items
AISI 8620 is an alloy carburizing steel when thermally treated
develops a hard outer case with a soft ductile core. Carefully
controlled proportions of chromium, nickel and molybdenum are
responsible for the extensive use as a carburizing alloy steel,
with valuable features including extreme surface hardenability
and good internal strength. Has minimum distortion and growth
characteristics. 8620 has good machinability and responds well to
polishing.
ANALYSIS
Carbon (C)
Manganese (Mn)
Silicon (Si)
Chromium (Cr)
Nickel (Ni)
Molybdenum (Mo)
Phosphorus (P)
Max
Sulfur (S)
Max
18-0.23
0.7-0.9
0.15-0.35
0.4-0.6
0.4-0.7
0.15-0.25
0.035
0.04
8620 cold roll bars conforms to ASTM A331
MECHANICAL PROPERTIES
Condition
Tensile Strength (PSI)
Yield Strength (PSI)
Reduction of Area
Elongation in 2"
Brinell Hardness
Annealed
100,000
85,000
60
21
185
APPLICATIONS
8620 applications include gears, pinions, cams, cranks,
clutch shafts, shafting, axles, tie bars, collets, bushings,
heavy duty pins, bolting, springs, hand tools, die cases,
and a multitude of machinery parts and components.
MACHINEABILITY AND WELDABILITY
8620 has a machinability rating at 66% of B1112. Average cutting
speed 127 ft/min.
8620 can be forged at 2200° down to 1800° F prior to hardening or
carburizing.
8620 is excellent for welding applications
HEAT TREATING
8620 can be hardened to 1500° F followed by water quench. Carburize
at 1650° - 1700° F in an appropriate carburizing medium and oil
quench to harden. Tempering of carburized parts is done at 250° - 300° F
and will result in the alloy having a core strength of approximately
135,000 psi minimum. Tempering of heat treated and water quenched
parts (not carburized) is done at 400° - 1300° F, with greater
hardness the lower the tempering temperature.
TOLERANCES
Rounds
Up to 1-1/2" incl.
-.002
Over 1-1/2 to under 2-1/2
-.003
Over 2-1/2 to 4" incl.
-.004
SPEEDY METALS ITEMS
3/8" {A} Rd Cold Finished 8620
1/2" {A} Rd Cold Finished 8620
5/8" {A} Rd Cold Finished 8620
11/16" {A} Rd Cold Finished 8620
3/4" {A} Rd Cold Finished 8620
7/8" {A} Rd Cold Finished 8620
1" {A} Rd Cold Finished 8620
1-1/8" {A} Rd Cold Finished 8620
1-1/4" {A} Rd Cold Finished 8620
1-3/8" {A} Rd Cold Finished 8620
1-1/2" {A} Rd Cold Finished 8620
1-5/8" {A} Rd Cold Finished 8620
1-3/4" {A} Rd Cold Finished 8620
1-7/8" {A} Rd Cold Finished 8620
2" {A} Rd Cold Finished 8620
2-1/8" {A} Rd Cold Finished 8620
2-1/4" {A} Rd Cold Finished 8620
2-3/8" {A} Rd Cold Finished 8620
2-1/2" {A} Rd Cold Finished 8620
2-5/8" {A} Rd Cold Finished 8620
2-3/4" {A} Rd Cold Finished 8620
2-7/8" {A} Rd Cold Finished 8620
3" {A} Rd Cold Finished 8620
3-1/4" {A} Rd Cold Finished 8620
3-1/2" {A} Rd Cold Finished 8620
3-3/4" {A} Rd Cold Finished 8620
4" {A} Rd Cold Finished 8620
4-1/4" {A} Rd Cold Finished 8620
4-1/2" {A} Rd Cold Finished 8620
4-3/4" {A} Rd Cold Finished 8620
5" {A} Rd Cold Finished 8620
5-1/2" {A} Rd Cold Finished 8620
6" {A} Rd Cold Finished 8620
Jean Prudhomme
-----------------------------------------
Jeff is on here so I think he will answer.
Paul Lamar
Jean,
Good information. Thanks, I was considering chrome moly 4130 for
the same application but was not happy about the way it machines.
I am interested in purchasing a chunk of 6 inch round by about 8
inches long. My thinking, is to have the six inch prop flange on the
outer size machined down to the outer seal step, and then reduced down
the 3 inch dia. bearing step and finally machine the inner spline. On
the Bell PSRU the forged planet gear housing has a female spline plate
that is bolted to it. Like Mistral's design I will have the Prop
shaft necked down after the spline and threaded to accommodate a 52mm
Hex nut. This nut locks the unit together The most inner partt of the
shaft reduces down to about 20mm and rides in the inner bearing. The
inside of the bar will be bored out to lighten it up. For maximum
toughness I would prefer starting with a forged bar though. If you or
anyone else is thinking the same way I would be willing to go in on a
group buy of material. Any info on a forged piece?
Doug in Japan
Doug
Just read your request....sounds interesting..I can help if you want,
let me know.............
BTW 4130 is not difficult to machine annealed, choose the best material
for the application.......
jeff
Jeff is right, you may wish to use annealed 4140 tubing, HT to Rc 60 or so.
milo
Jean,
Please tell me how you would attach the prop flange. Taper or key way? Both? I
assume the inner piece is threaded.
Doug in Japan
--
The Rotary Engine NewsLetter. Powered by Linux.
ACRE NL web site.
http://www.rotaryeng.net
Youtube key word PaulLamar2
Copyright 1998-2010 All world wide rights reserved.