On a different note, I am learning how to do aluminum castings. I am
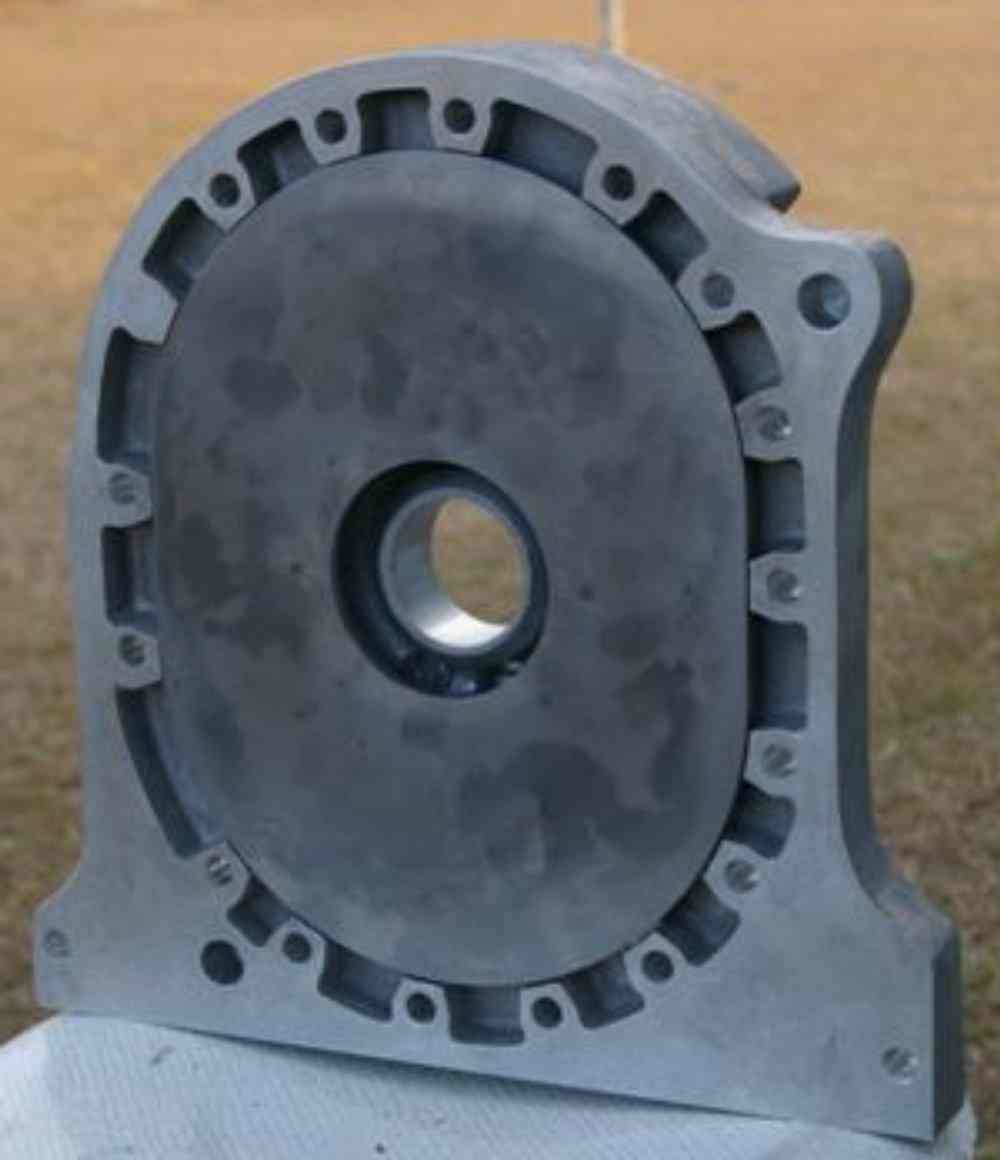
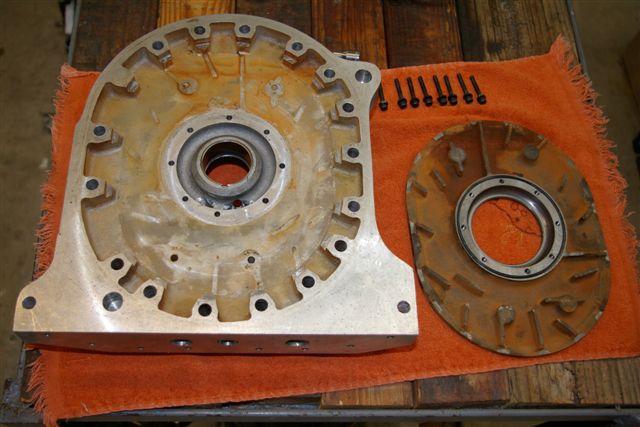
looking for the best casting material for center and end housings,
possibly one to the ceramic metal matrix hyper alloys and
beralcast 363
for rotor material. It appears to be the only beryllium alloy on the
market and can be investment cast to near net. Do you have any
knowledge
on this stuff? I've been reading about it for about a day, and
looking
for a supplier.
Ed Carver
I have heard of aluminum/beryllium alloys .70% the density of
aluminum.
Makes great rotors. What is the density of beralcast 363?
Paul Lamar
Ed Carver,the 363 sounds like a good rotor material depending on
it' coefficient of expansion. It might require pressure assist
or vaccum
casting. For vaccum assist you can fill a 12" diameter 25 ft
tall pipe
with water, tap off the top header for the vaccum and open a 90
degree
plate valve at the bottom with the valve submerged in the
capture tank
water. We used this system to raise liquid steel for vaccum
degassing
and bubbled argon in one side to make it circulate. Three passes of
a 424 ton heat in 7 minutes. The tower was 150 feet high.I was
thinking of 390 aluminum for end housings.
That is what
the Briggs and Stratton and chevrolet vega blocks are made from.
No wear
coating is required since the silicon carbide is in the alloy. I am
currently looking int to NASA alloy designated 398 which has much
higher strength than 356 and other commonly used alloys and also
needs
no wear coating. It will work with gravity assist which is just a
standpipe at the pouring sprue. No rocket science. I haven't run my
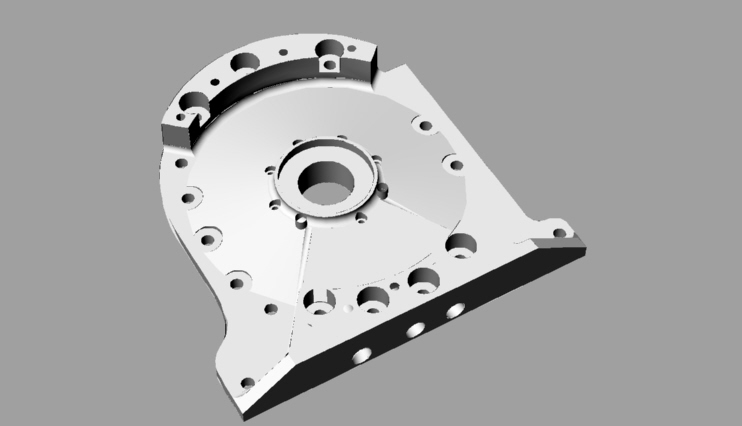
patterns on the gantry router yet but the design is finally
frozen and G
code files are done.
george grimes
The rotor runs too hot for 363. Be/Al has higher strength at 500 F.
Aluminum loses over half it's strength at 500 F.
http://www.suppliersonline.com/propertypages/6063.asp#Spec
Paul Lamar
Yea George!,
I've spent the past 3 days reading up on which casting alloys are best.
I was hoping I would get some feedback on the 390 stuff. I'm going to
have to find out which alloy Porsche used in their 928/944/968 cyl.
blocks. The rings rode directly on the alum wall with excellent wear
characteristics. The cyl walls were either impregnated with a silicone
substance during the final surface finishing, or, the silicone was
simply used as a lube during the honing process. I think it was 390 they
used. This raises the issue of which rotor side compression seal
material should be used to ride on 390.
I have seen hypereutectic alloy used as brake rotors with special pad
material clamping onto them. A local los angeles engineer developed it
for light weight race cars back in the mid 90s. Porsche developed
aluminum rotors about 12 years ago for their twin turbo 996 and their
super cars. I would have to really dig to find out which substance they
used to treat the rotor surfaces.
I'm not an engineer. It's easy to make comparisons using the tech data
sheets online. It appears to me that the beralcast 363 BeAl alloy is
really superior to all other options for rotor usage. Perhaps the 390
hyper alloy would work as a rotor under low power usage. That is the
purpose in it's usage in oem pistons.
What is of greatest interest here is whether we can use a casting
process to make the rotor. If we can, it will make light work once on
the machine table.
Paul, are you telling us that 6063 alum should not be used for rotors,
or is it the beralcast 363 BeAl alloy you are warning about? All the
aluminums have approximately the same melt point, the beralcast 363
should hold up better and longer. I believe I read that beryllium melts
at about 2100f. Not the same as the 363 alloy.
Time to look into the 398 alloy.
Ed Carver
The only aluminum alloy other than be/al that has a chance for rotors
is NASA 390. Not the same problem as cylinders.
http://www.rotaryeng.net/aluminum-alloy-rotors.pdf
http://www.rotaryeng.net/aluminum-alloy-rotors2.pdf
http://www.rotaryeng.net/Be-Al.pdf
Don't get silicon and silconE confused. In the Vega engine the
high silicon content aluminum used for the cylinders were etched to
raise
the silicon to the surface. As I recall a special coating was used
on the pistons. The scheme largely failed.
In the Porsche cylinder a process called Nikasil by Mahle was used.
http://www.ebsracing.com/content.wws?fname=Porsche-Cylinders.html
I think this was done by exploding a nichrome wire down the
down the center of the cylinder with high current. This was tried
on certain Wankel engines with bad results. Quality control was
less than satisfactory.
Porsche also used:
"Depending on their silicon content, aluminum alloys are
referred to as either hypoeutectic or hypereutectic. Alusil
has a hypereutectic aluminum content of 16% to 18% so that
primarily silicon is precipitated. The Cayenne engine
manufactured to precipitated during solidification. A
special three step honing process is applied. The silicon
grains in the cylinder bores in form of microscopically
small, very hard particles, giving the necessary
wear-resistance of the cylinder surfaces for the pistons
and piston rings, are laid bare in the final step."
Probably etched like the Vega.
Mazda successfully used a expensive process called detonation gun
coatings for
alloy end housings for the LeMans winning engine. To my knowledge
that is the
only process proved over long hours at high power. We await the 16x
to find out
what will be used on that. If I were Mazda I would stick to the
steel inserts.
http://www.rotaryeng.net/Mazda_R26B_US.pdf
http://www.rotaryeng.net/material-tech.pdf
http://tinyurl.com/26yhecj
The rotor housings have a die cast in hard steel chrome plated
insert of course. Highly successful.
Paul Lamar
Ok, the nasa 398 alloy is designed to hold up to about 750f, and that's
much better than the other common hyper alloys for piston use listed on
the nasa 398 tech page on your main site. There is no specific data on
the same issue with any of the other castable alloys I can find. The 398
may also be best for the center and end plates. I doubt anyone will
create new iron side rotor seals to ride on the etched 398 aluminum like
the Porsche rings on the 390. This leaves us with flame spray coating,
or ferris plate inserts.
The albemet162 is not their castable alloy, but specs out about the same
as the beralcast 363, which is castable. The albemet IC910 is castable
at a much lower Be content, and has much lower specs. There are other
castable Be/Al products, but beralcast 363 appears to me to be better.
There is a rather odd spec about melting points of these Be alloys.
Can't figure out why, but they put two melting points on some of the
pages that are wildly different. The albemet162 specs show a 2000f melt
point and a 1200f melt point on the same column! Whats with that? I have
read similar on other spec pages.
If it has some 30% alum in it; it will melt at 1200f, no matter what.
Yea? Pure Be melts at ~2000f~.
For the moment, it appears we use the nasa 398 as rotor material, or
beralcast363.
For center and end plates, several materials will work, but why not
stick with what Mazda uses for the rotor housings. Isn't that a356?
Should I consider it conclusive that we now have 2 potentially good
castable materials to try light weight rotors? Or do I keep looking?
Ed Carver
I think we are talking about three different things here.
Mazda used the high silicon content Al alloy to reduce heat expansion
and contraction in the rotor housings. The old Al alloy would over heat
to 250 F and then permanently compress under the restraining force
of the steel tension bolts. The rotor housing was then junk.
Then there is the question of the Al wear surface.
Unfortunately the term flame spray is used on a lot of coatings.
One must be more specific as there is a world of differences
in coating procedures with vastly different characteristics.
The major problem with coatings in general is no way to check
adhesion non destructively in the manufacture process.
You have to build thousands and then see what percentage fail.
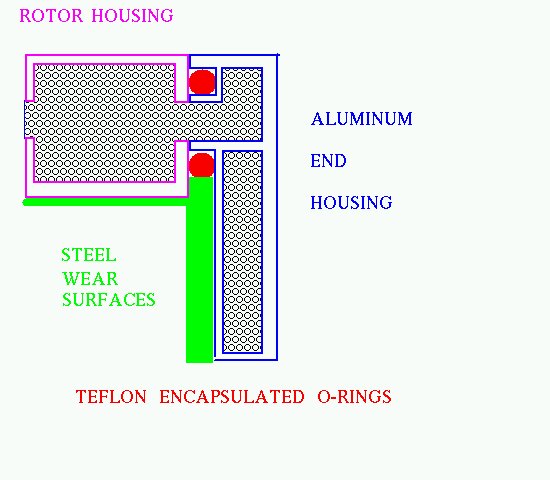
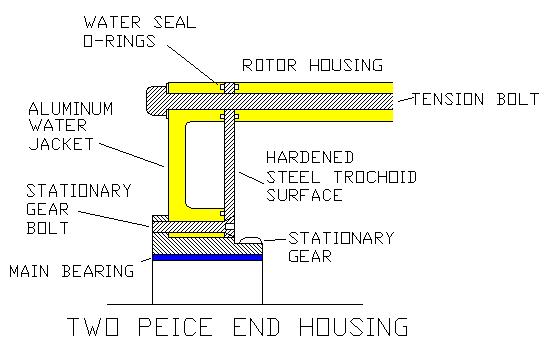
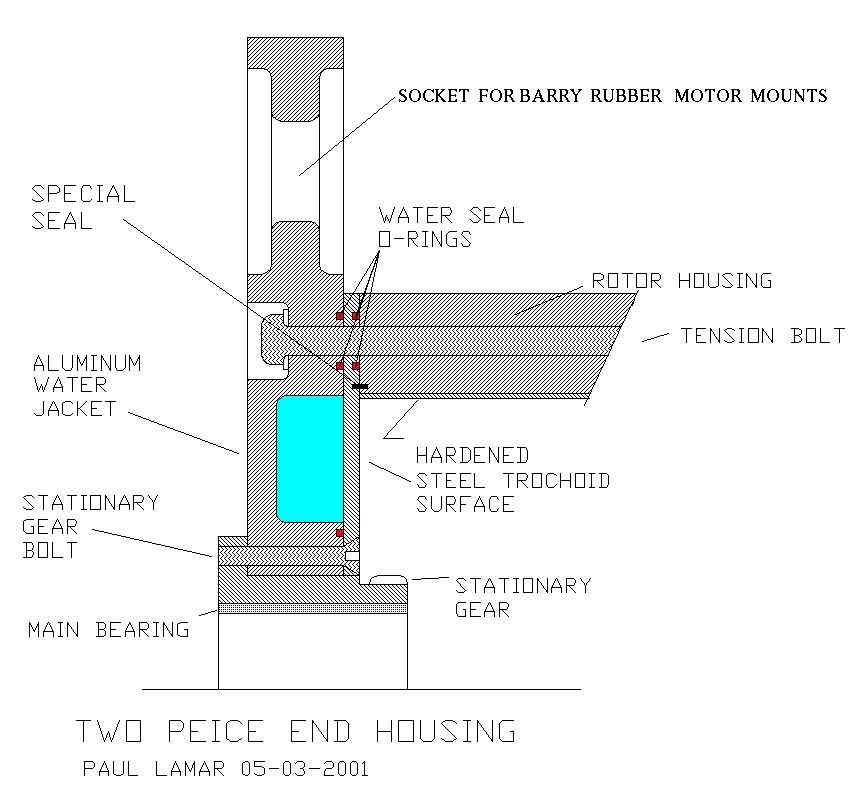
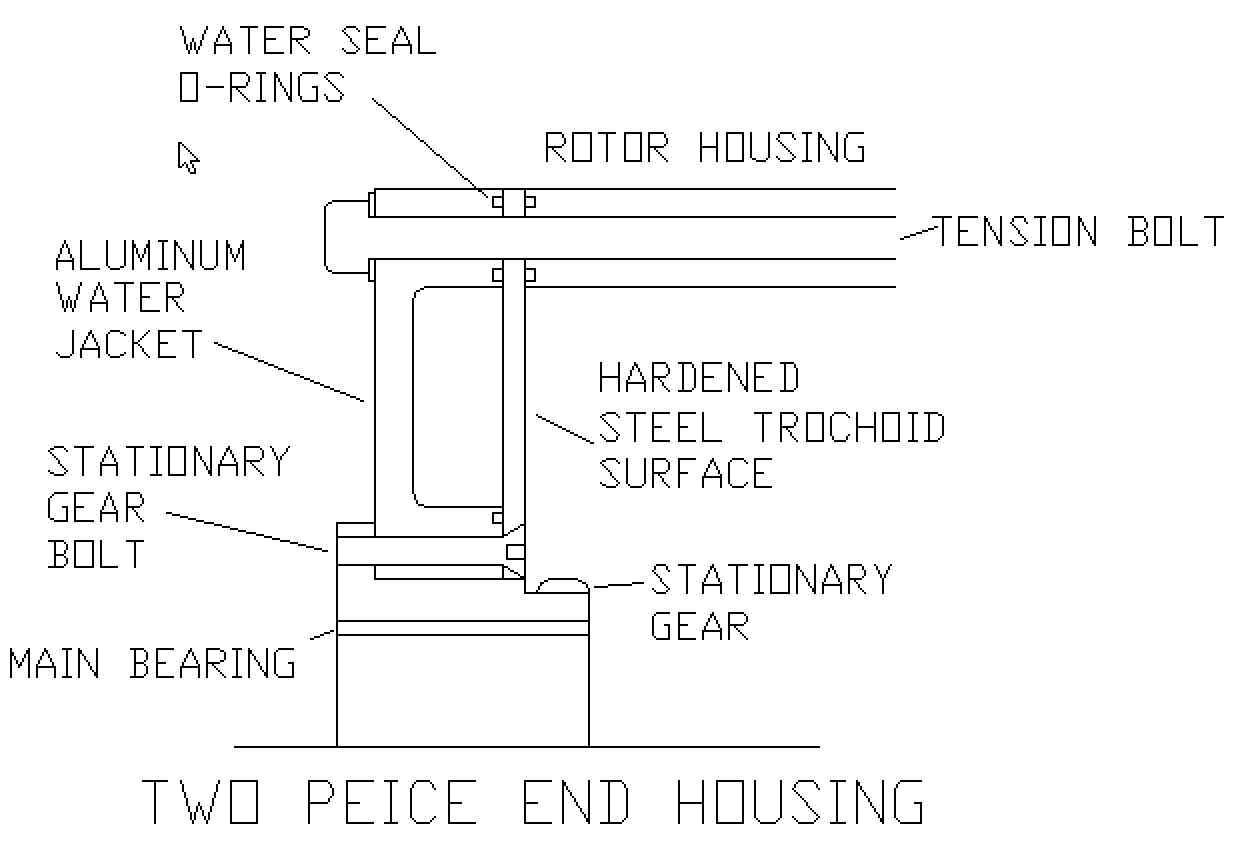
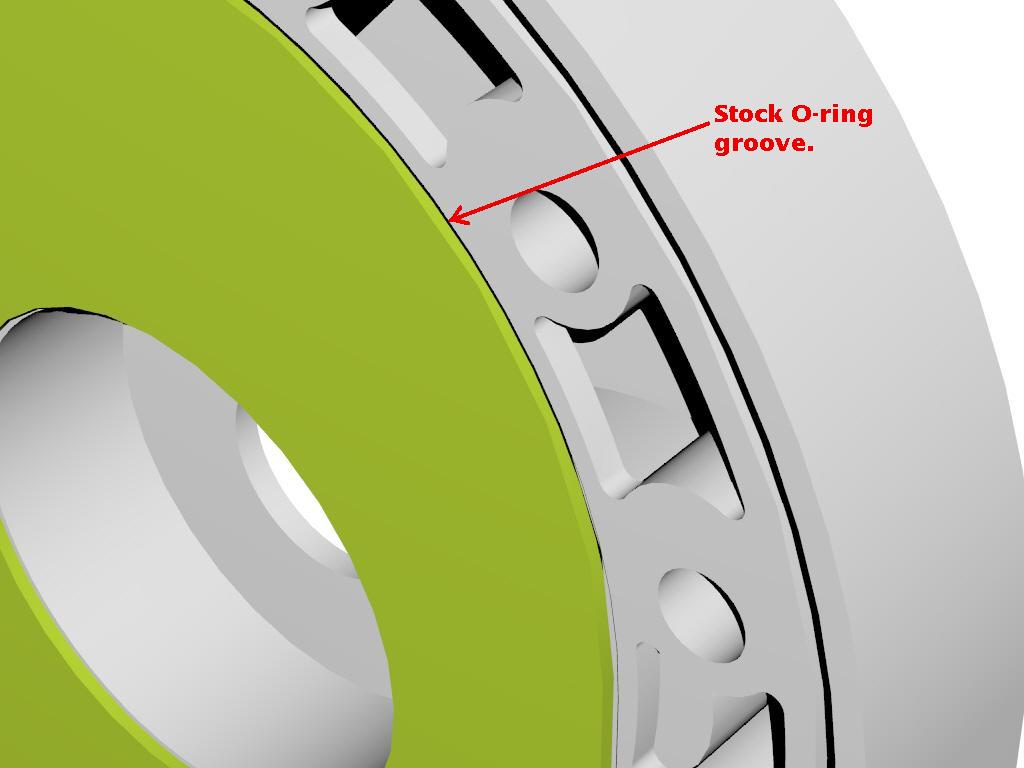
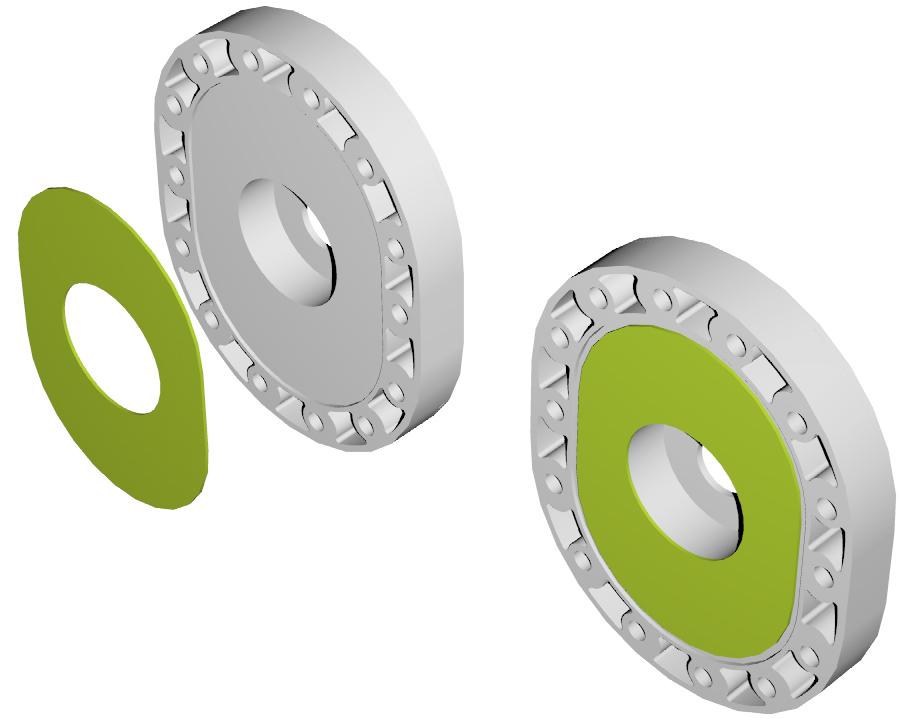
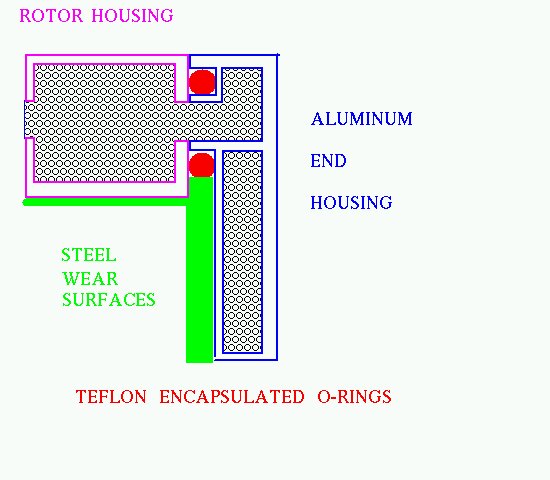
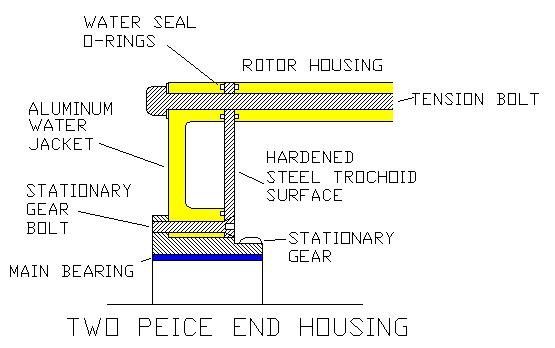
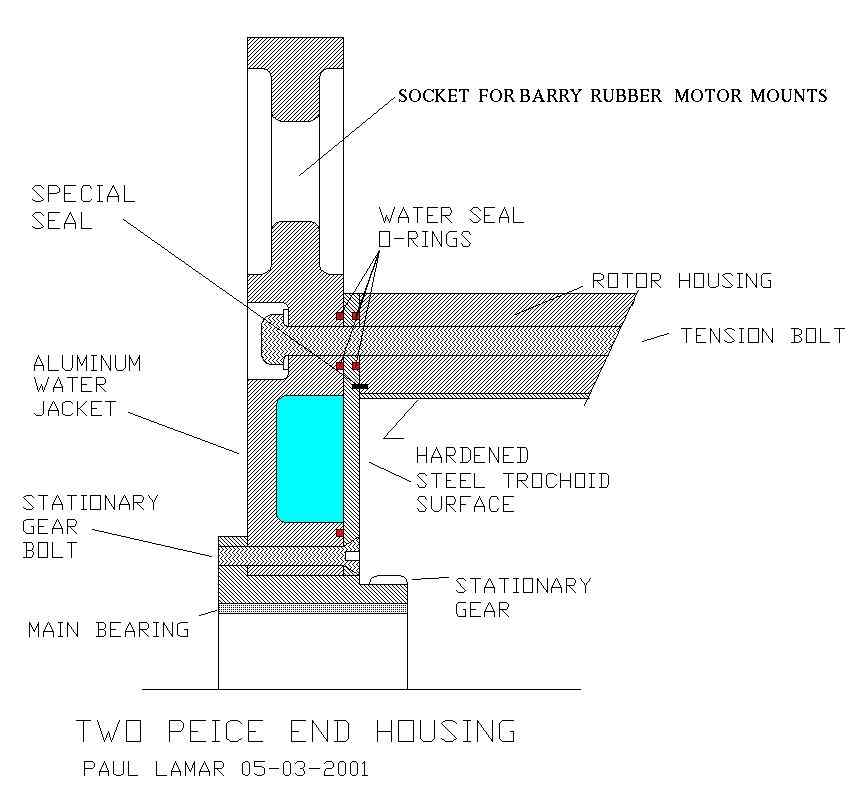
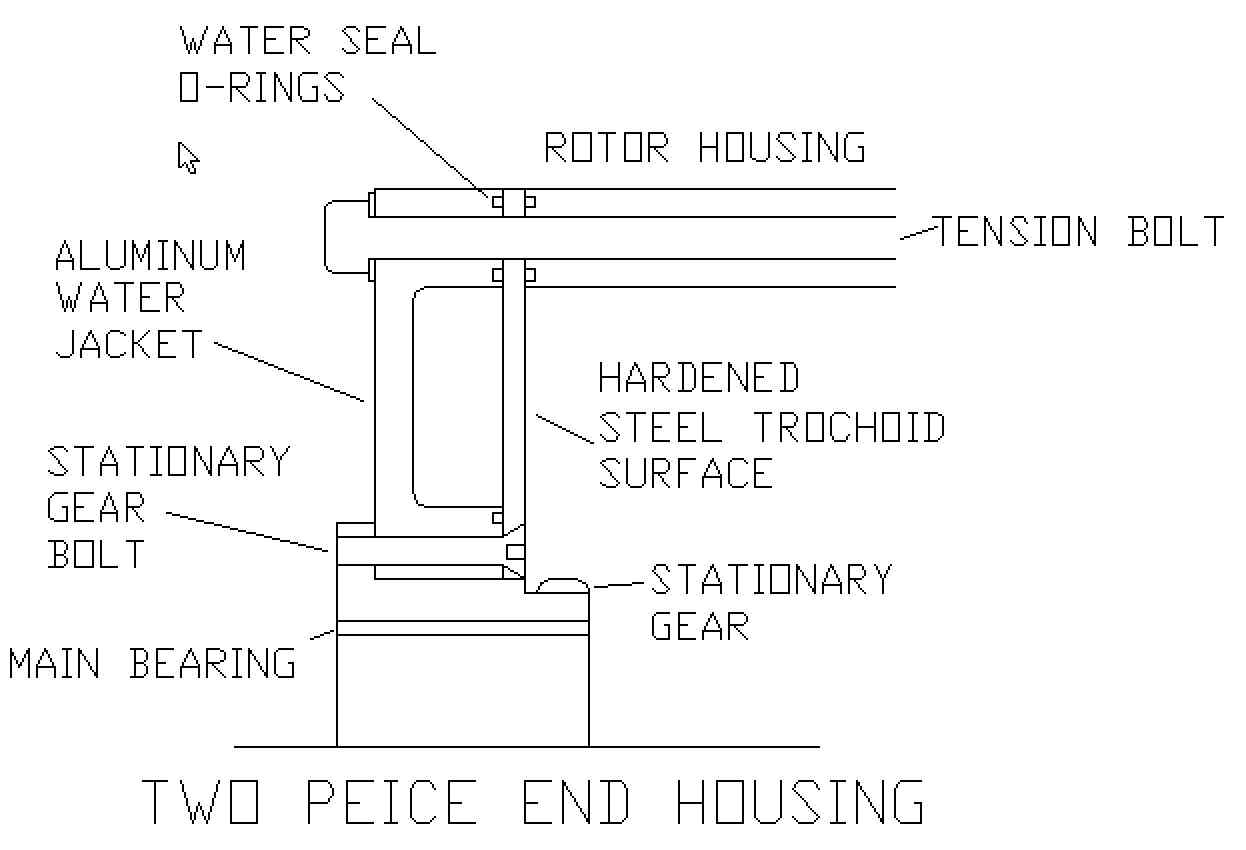
That is why I am a fan of two piece end housings one of which is
a replaceable steel wear surface.
Then there is the question of what to make the rotor out of.
This should be three different threads. Lets separate them.
Paul Lamar
--
The Rotary Engine NewsLetter. Powered by Linux.
ACRE NL web site.
http://www.rotaryeng.net
Youtube key word PaulLamar2
Copyright 1998-2010 All world wide rights reserved.