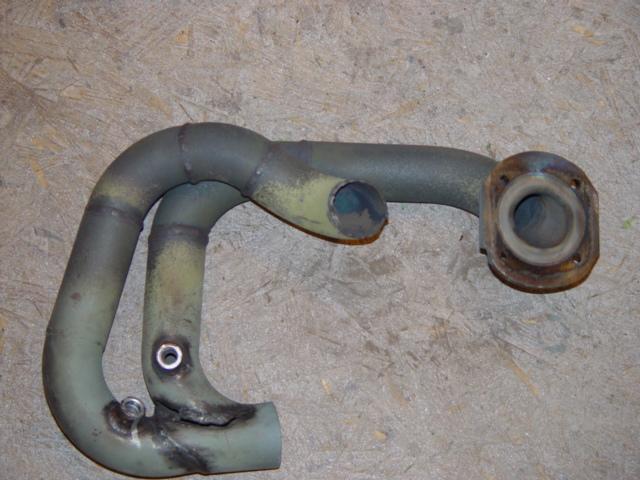
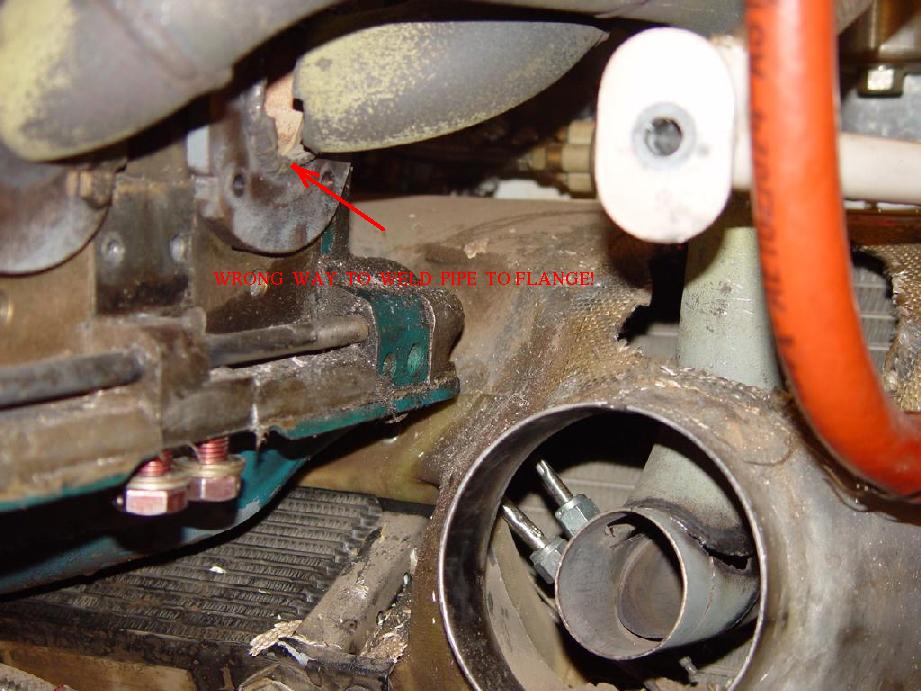
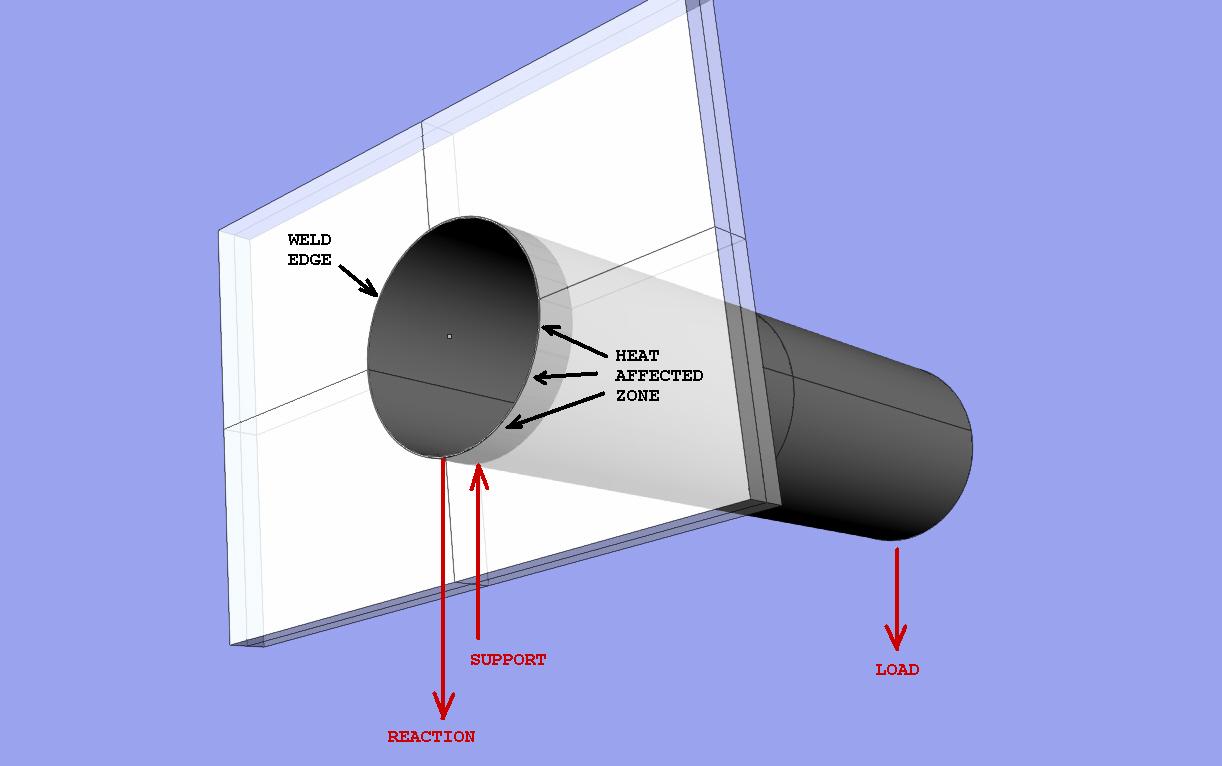
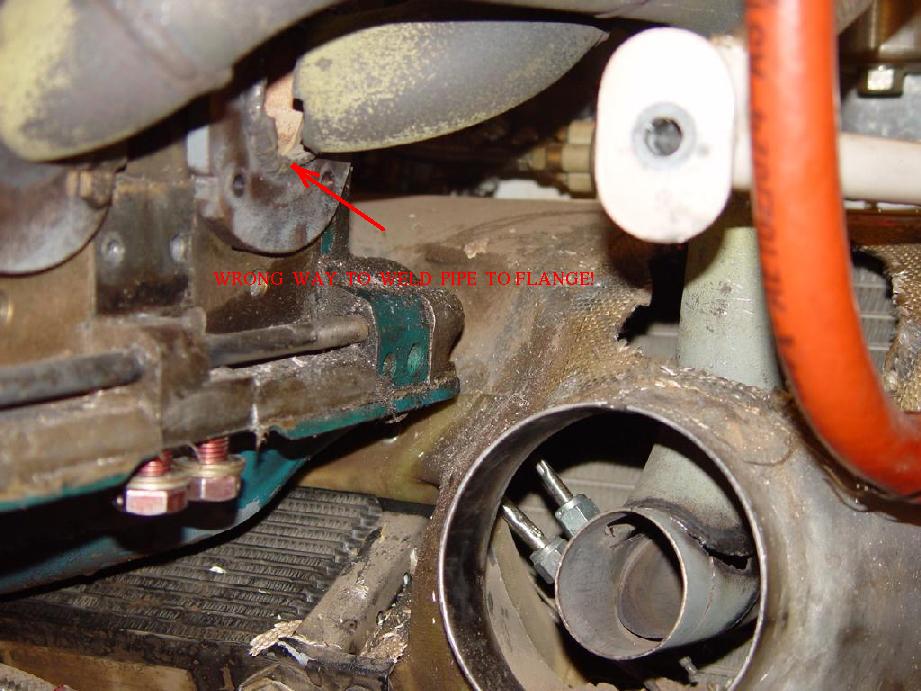
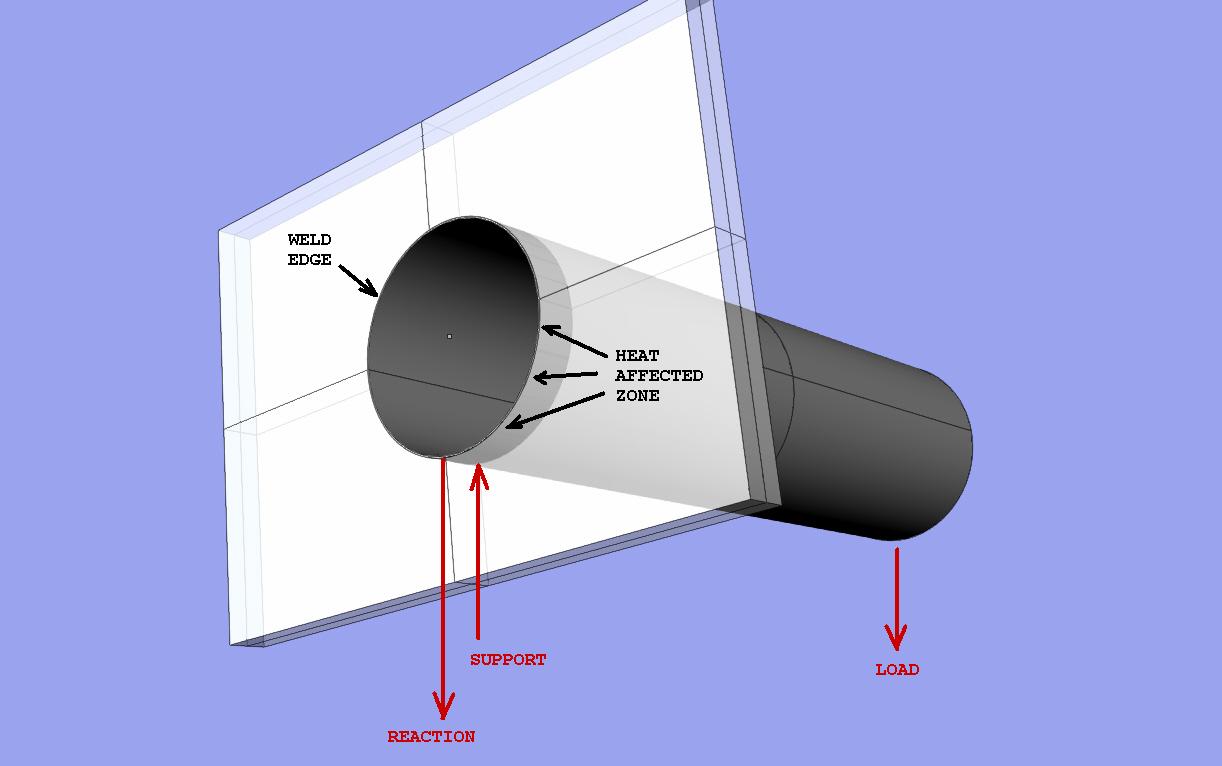
When I TIG weld something like this, I normally would poke that tube
through
The hole and leave about 1/64^th of an inch protruding. I then weld it
using no
Filler rod, using the small protrusion as the “filler rod” and” fusion”
weld it.
The finished weld should require little or no finishing. I have done
this many times
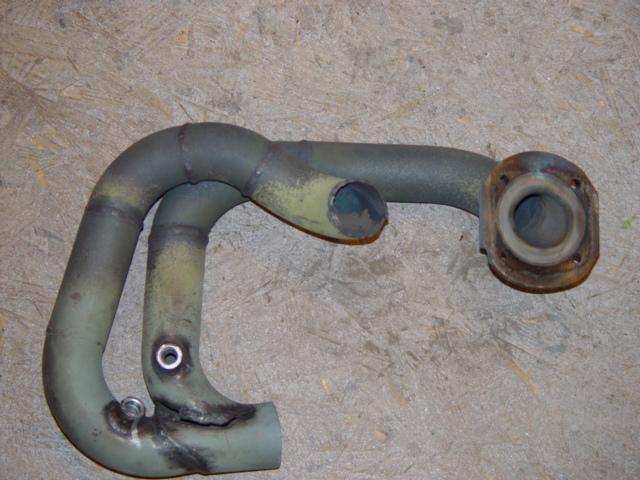
with good results. Just like you would weld in an exhaust tube
Into it’s flange. I used to make tuned headers for a living.
Chris in NZ
I agree Chris. That trick works really well on tig welding aluminum
too.
You bring up exhaust flanges and tig welding them like that appears
to be mandatory for the rotary.
Paul Lamar
--
The Rotary Engine NewsLetter. Powered by Linux.
ACRE NL web site.
http://www.rotaryeng.net
Youtube key word PaulLamar2
Copyright 1998-2010 All world wide rights reserved.