Good morning Paul
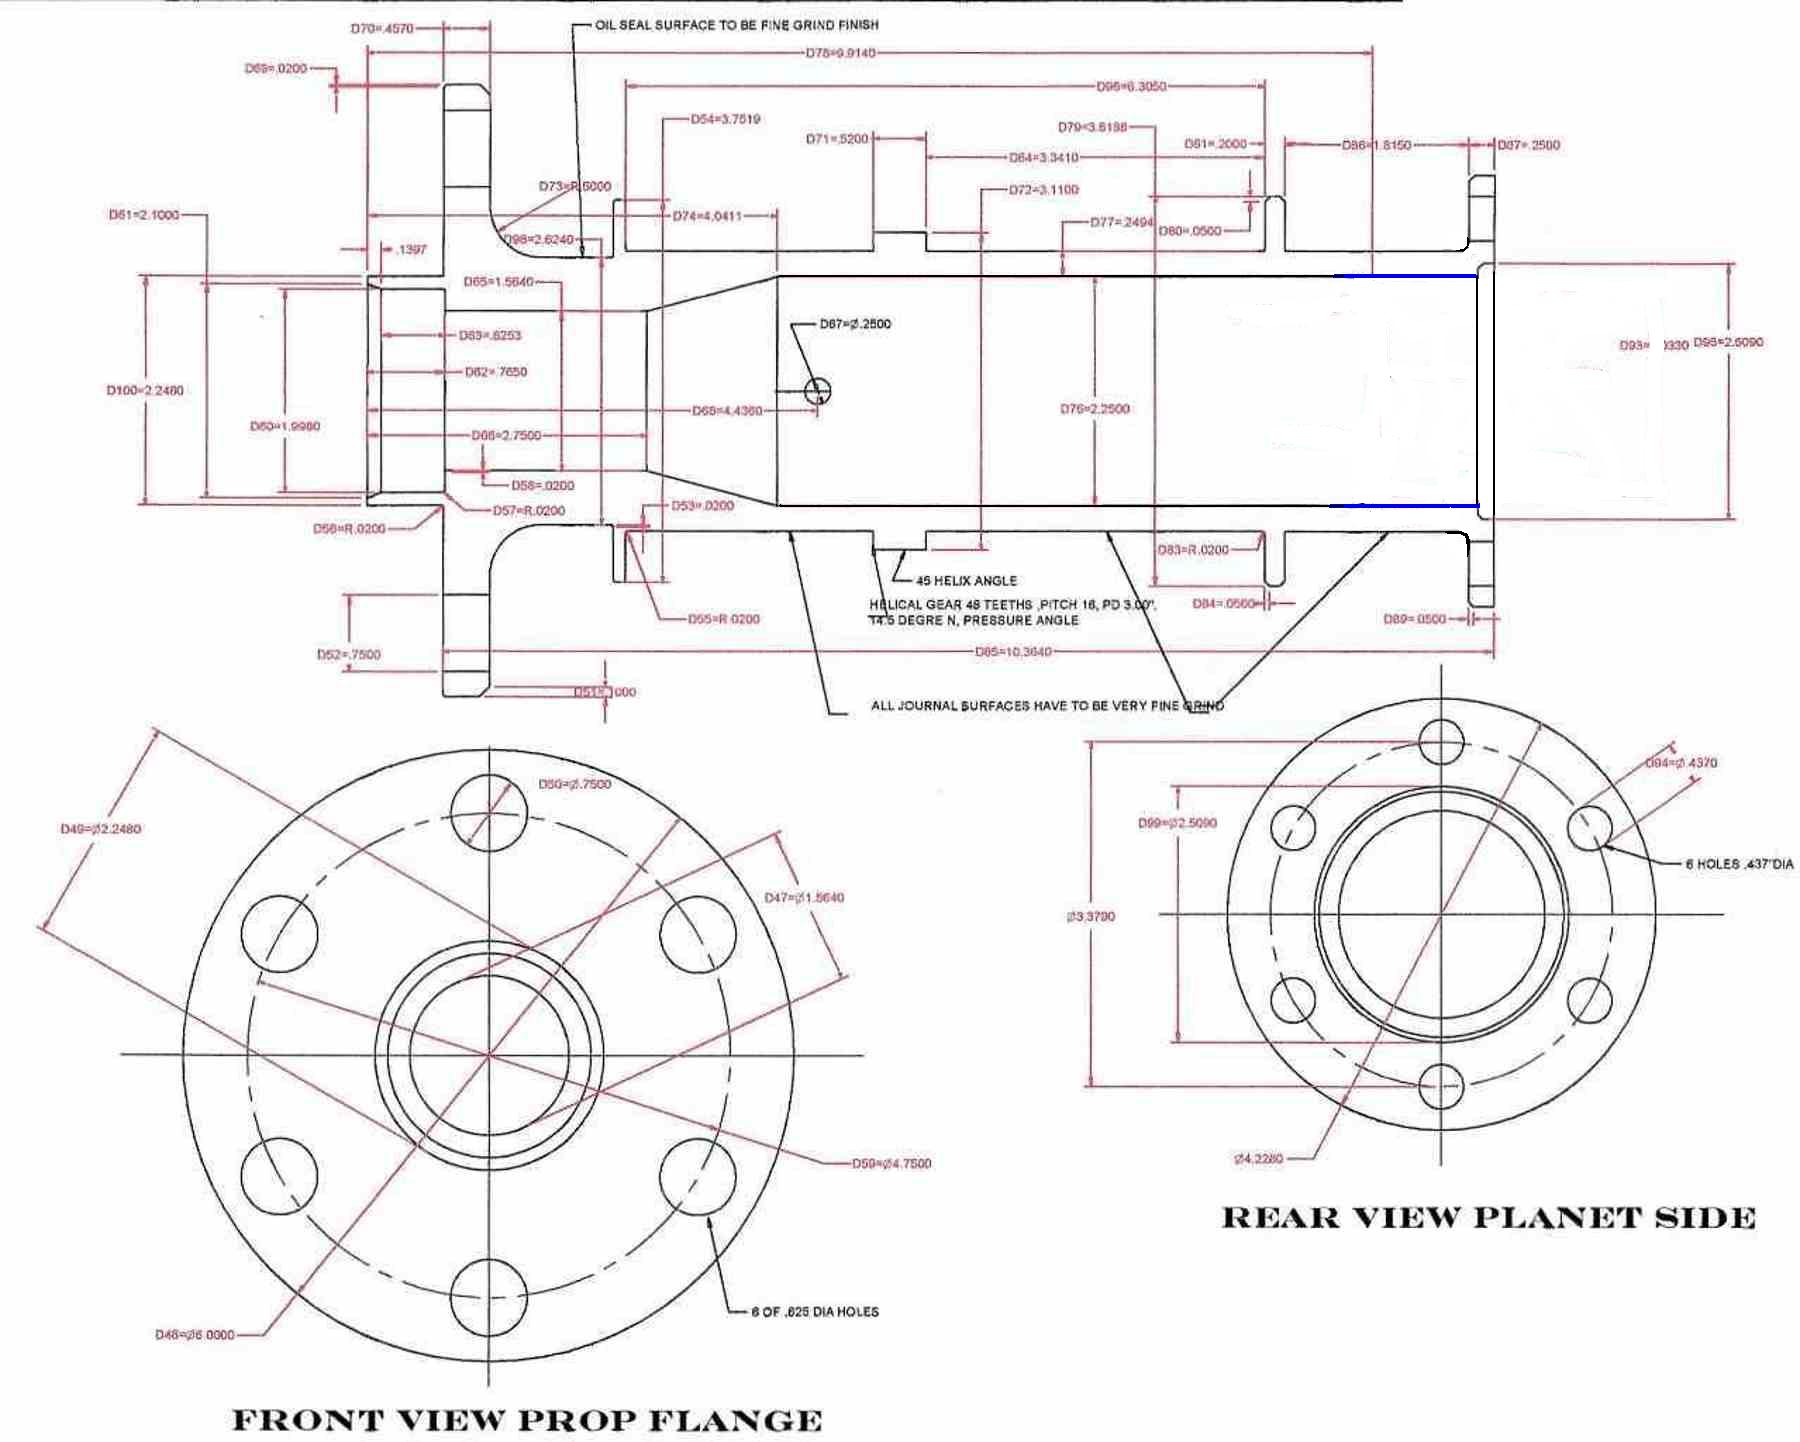
I am sending you the propeller shaft design and i would like to know if
Jeff can machine this shaft and how much.
I specified sae 4130 but you can recommend a better choice for shafting
and treatment.
I modified my housing design for a larger surface bearing at prop side
and also a better ring gear attachment with back plate and rivets plus
bolts.
The ring gear back plate is already machined .
With Alibre i can not convert for Rhino files but dwg can be open with
Solid Works eDrawing
Jean Prudhomme
Looks good Jean. Is it an exact copy of a Lycoming or Continental
shaft?
If so that is good. Do you mean planet carrier back plate? If you
want a 2.85:1 gear box you will need to drive the planet carrier
and hold the ring gear stationary.
You will have to contact Jeff directly and see if he will do it.
If you are only making one or two you don't need an NC lathe.
jeff doddridge <
4starr@cox.net <mailto:4starr@cox.net>
Paul Lamar
Yes Paul this is the exact Lycoming 10-540 big journal from the seal to
the flange included, i did turn around 180 degree the planet outer ring
and machined the back plate and fix with rivets a larger plate in dia so
i can bolt it to the housing and the fact the planet stay forward i
will need a thin oil impregnated flat washer between the outer ring and
the back plate and panet housing.
I did drive out the small gears shaft from the planet and i will make 6
longer shaft for the small gears to been driven by the propshaft and
the planet embossed reset shaft will be press fit into the
propeller shaft.
I intend to built one unit for testing and built a second one may be
more.
I will request also a quote from a drive shaft manufacturer if they have
the material available
Jean Prudhomme
Jean,IMHO the rear flange that the planetary attaches to needs a
large radius fillet where it meets the shaft OD for the same reasons as
the flange on the other end. Also the internal bulkhead might be easier
to fabricate if the center had a conical 120 degree depression the same
shape as the largest drill bit you will use before changing to the
boring bar A boring bar small enough to machine the center flat would
be seriously overhung at that depth. The shallow end could be cut to
constant thickness by setting the compound to 30 degrees.You might
save on machining costs if you cut the billet down to .100 from all the
surfaces and have the fine finish cuts done by someone like Jeff. The
bearing journals will likely be done by a crankshaft repair shop who
could chrome the journals as well.
george grimes
Good points George. The aft steel bulkhead could be replaced by an aluminum
plug pressed in. That would make it much cheaper to build as a large drill can
do most of the work. See the attached jpg.
Paul Lamar
--
The Rotary Engine NewsLetter. Powered by Linux.
ACRE NL web site.
http://www.rotaryeng.net
Youtube key word PaulLamar2
Copyright 1998-2011 All world wide rights reserved.