Due to the difficulty of finding replacement ring gears at a
reasonable price for the Mazda auto tx flex plate I suggest we use
the current flex plate and merely tig weld the damper to it. Your
current starter is sure to still fit and work.
I was quoted ring gears $95 each from a company in NZ with $95
shipping by boat. No telling how long that would take.
Mark Steitle brought up the issue of room for a thrust bearing
between Tracy's spline flange (brown in the 3D) and the PSRU adapter
plate. Simple solution. Reverse it.
That gives more than enough room for a thrust bearing.
Here are the 3D's.
Some of the 2nd gen current flex plates have large holes near the
center that weaken them. The solution is tig weld in a plug. The 3rd
gen did away with the holes.
I just bought a 13B auto tyranny flex plate on ebay for $12. Shipping
and handling was $30 :)
Lots on ebay for $50.
Paul Lamar
Just a thought, the ring gear can be easily cut from an existing flex
plate, welded to new one. easier than cutting many plugs and welding
them into the old plate. C. Smith
That would add about $150 to the cost as there is labor involved
cutting off the ring gear and making and entirely new flex plate. If
that is OK for everybody I will do it that way. The plugs would be NC
laser cut out of 4130 scrap.
My guess on the cost right now is $250 +- $50
Paul Lamar
Paul,
I have a ring gear that I separated from a cracked flex plate. Let me
know if you want me to send it.
FWIW, these are fairly easy to remove, There are a few short welds
that must be ground off and then you can tap them a little at a time,
going around the perimeter and get them apart. A little heat and the
ring would probably fall off on its own.
My thoughts regarding the welding... we need to be very careful so as
to not to cause warpage. I believe they should first be tacked
multiple spots around the circumference, then welded a short
distance, move across to the other side, and weld a short distance,
then move back and repeat the process, keeping the heat even. And
they still may warp. A small amount of runout will cause the flex
plate to eventually crack. Been there, done that.
Mark S.
Ye4s I want it.
Three options in order of cost. A Weld to existing flex plates B Find
a new ring gear and buy it. Weld a new flex plate. C Remove ring gear
for flex plates and weld up new flex plate.
Vote :)
Paul Lamar
A-Tig? Marc
Plan E. No flex plate. No warping. No welding. No run out. No dial
indicator.
Bolt it directly to the counter weight. I have three guys with NC
mills. Jeff, Larry and John. Mill the parts out of 6061 T6 bar stock
7.5 inch in diameter and bolt it on using six new 10 mm metric
bolts.
It will be about $30 for material.
You just need to send me Tracy's spline plate so we can drill out
the rivets and bolt it to the aluminum damper coupling with a bunch
of screws.
Paul Lamar
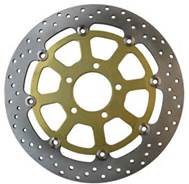
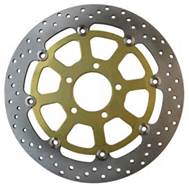
Paul, I am attaching a photo of a motorcycle disk brake as an
example so
folks will understand what I mentioned about the ring gear
before. We would
replace the hollow connectors on the brake disk with bolts. Even
spacing
using the same size shouldn't effect the balance.
Bill Jepson
The Rotary Engine News Letter. Powered by Linux. ACRE NL web site.
http://www.rotaryeng.net You Tube
http://tinyurl.com/beqqxas
Copyright 1998-2013 All world wide rights reserved.