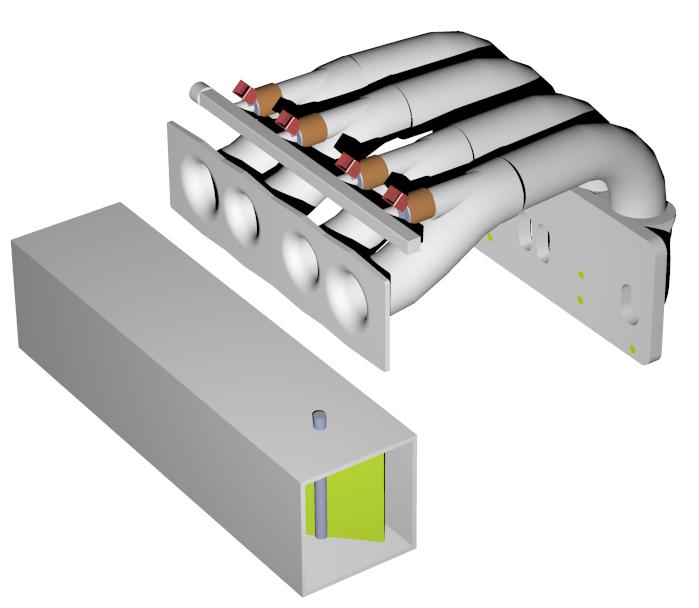
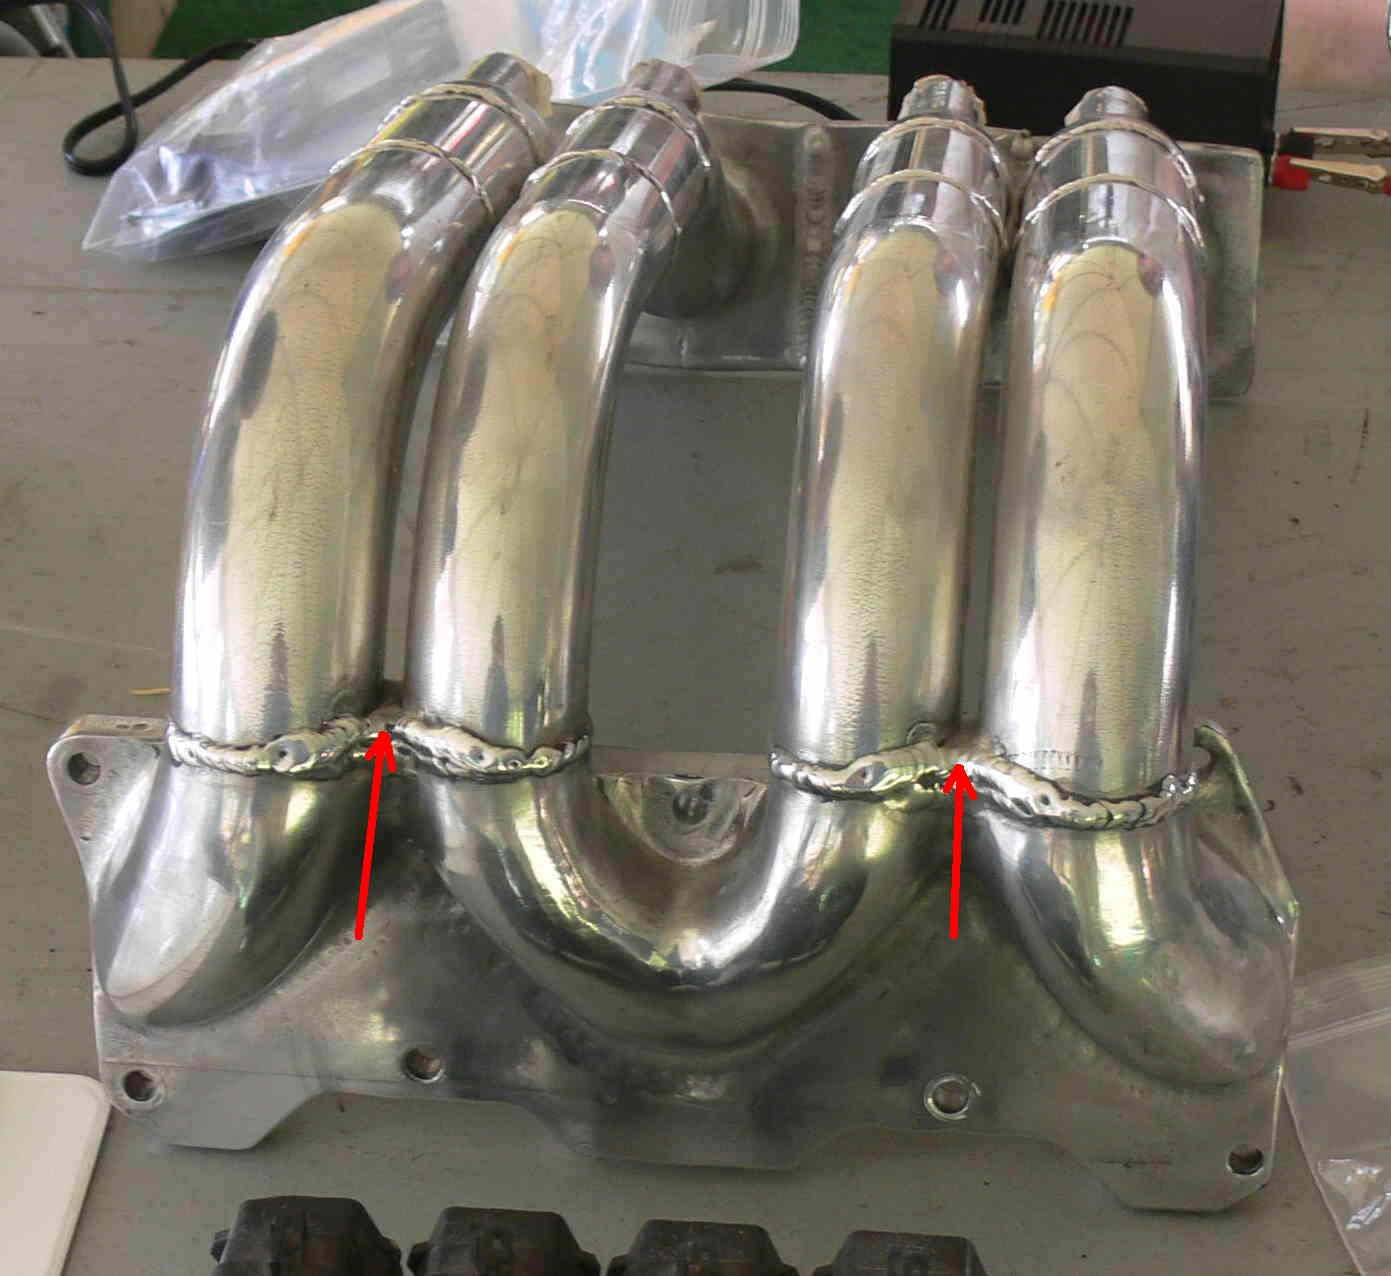
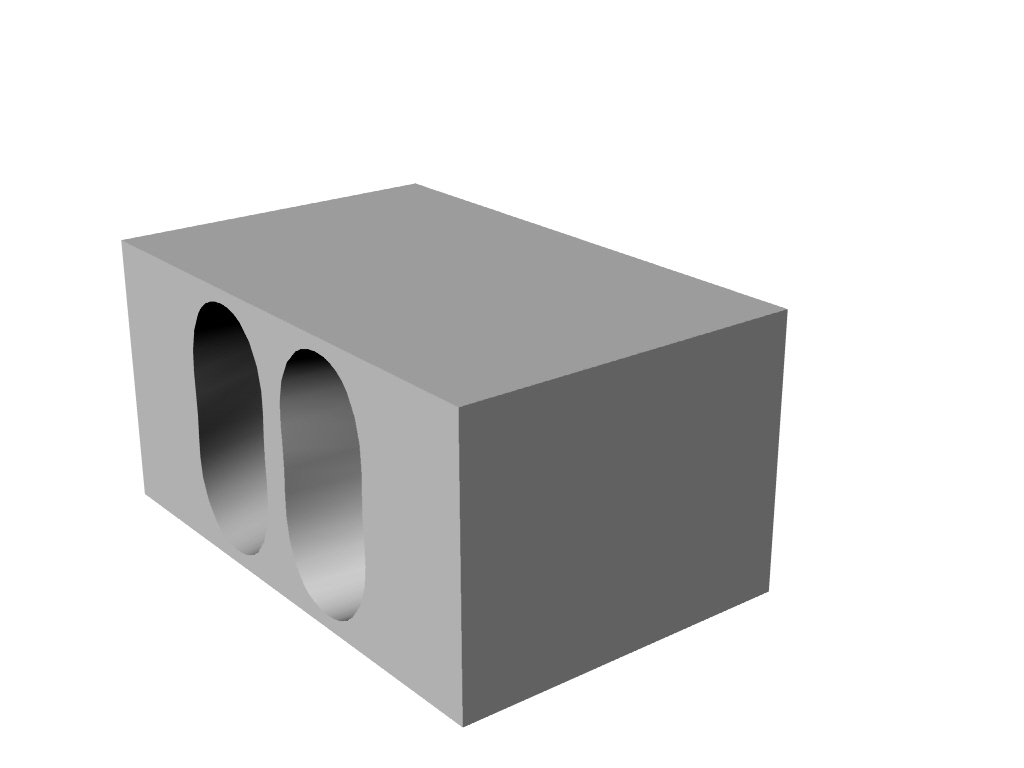
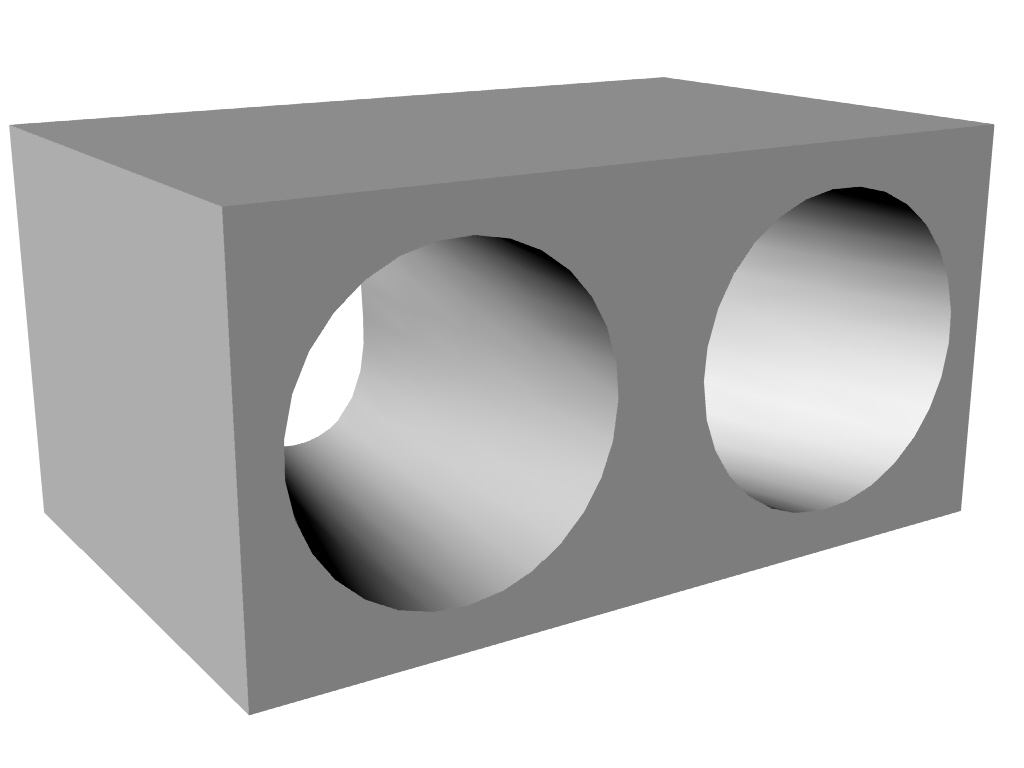
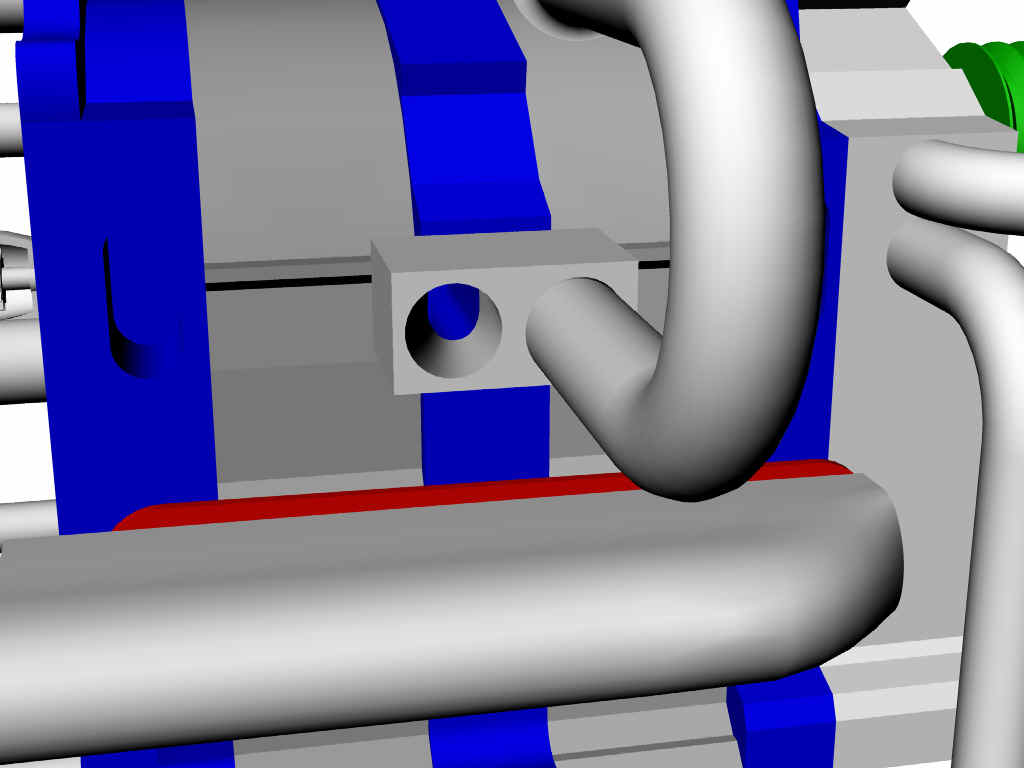
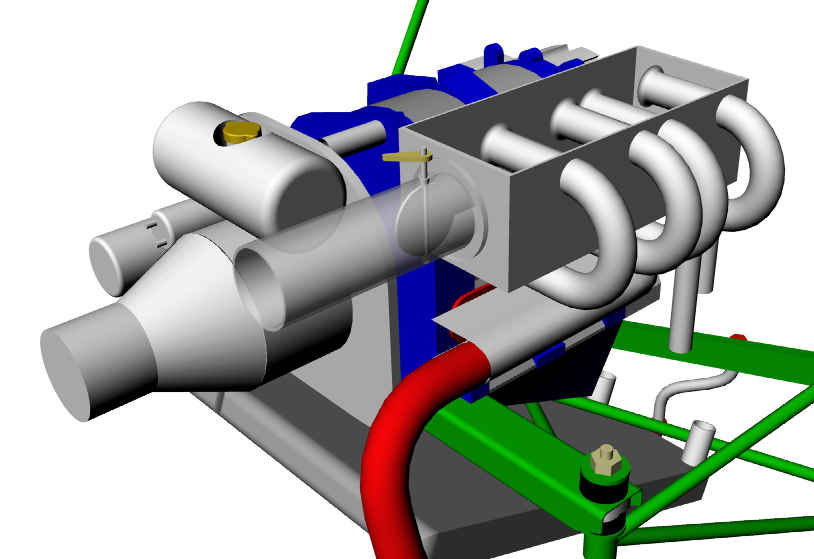
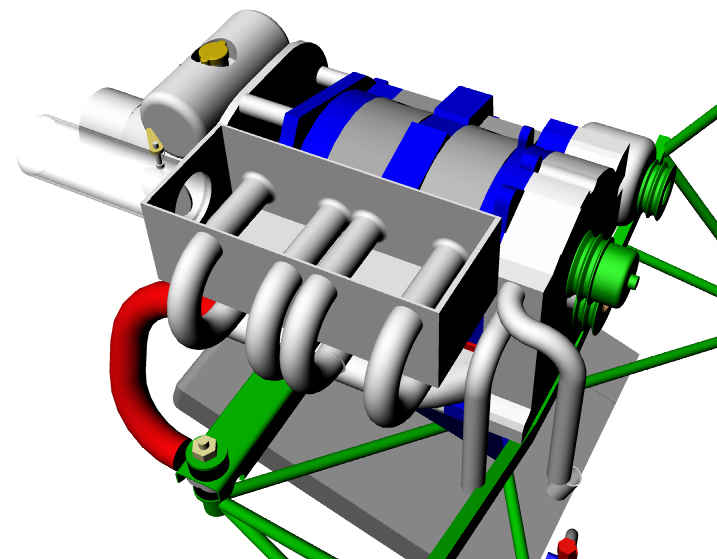
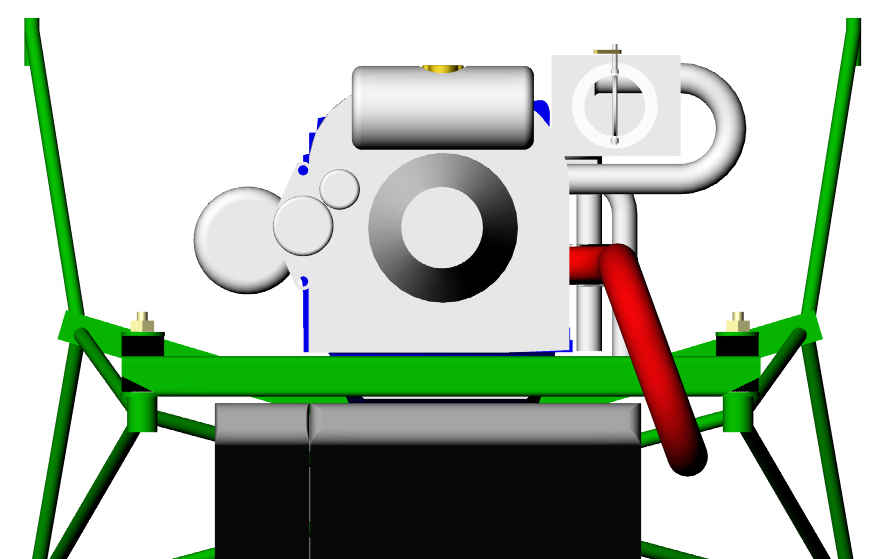
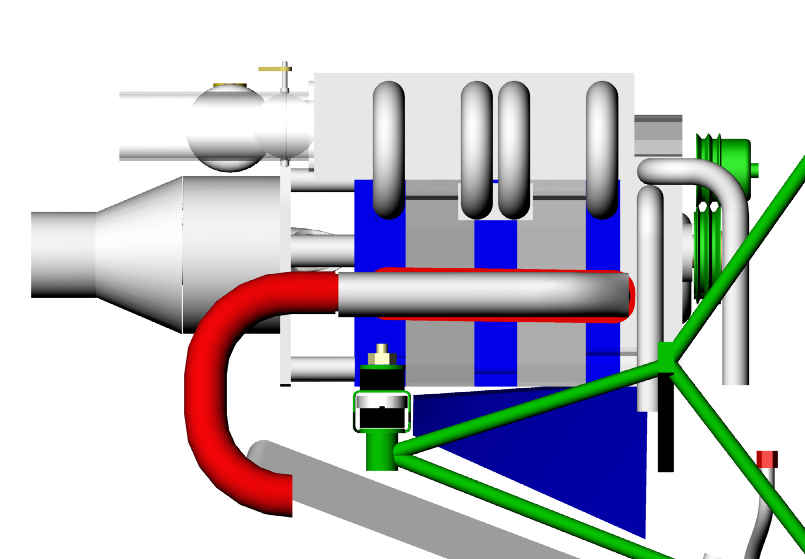
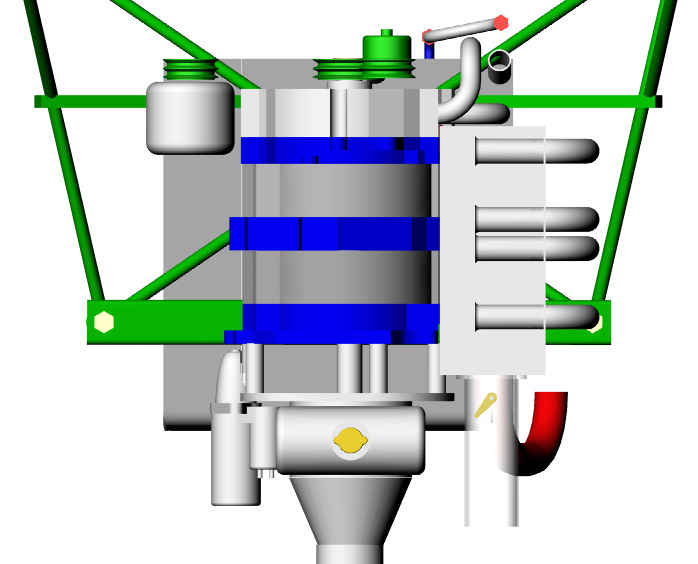
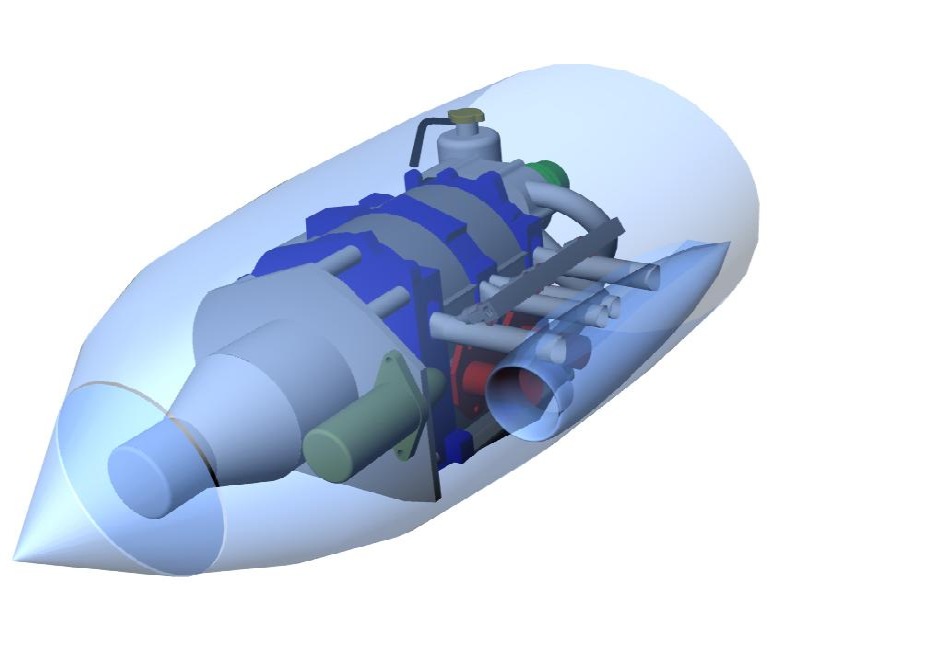
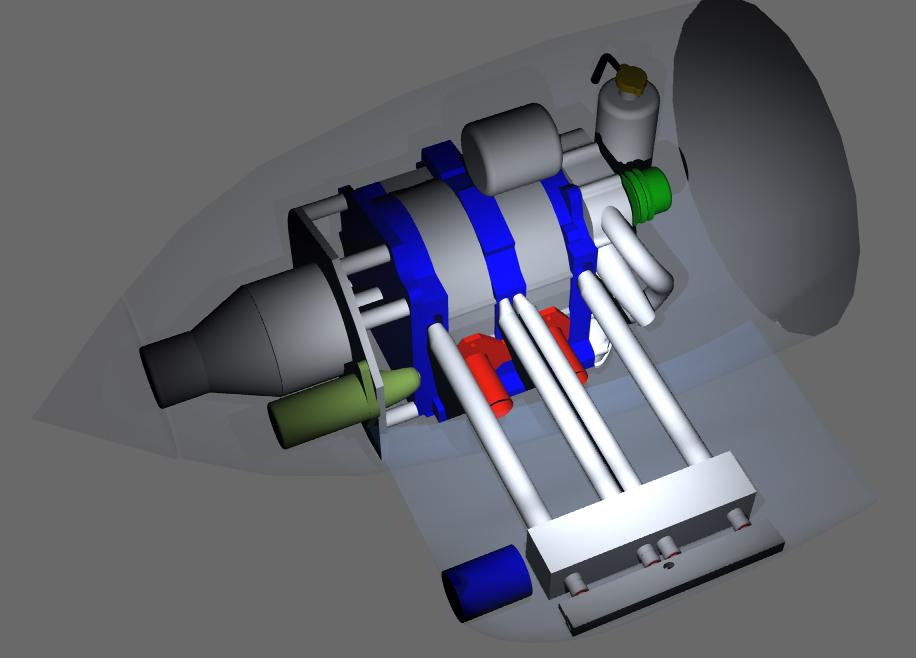
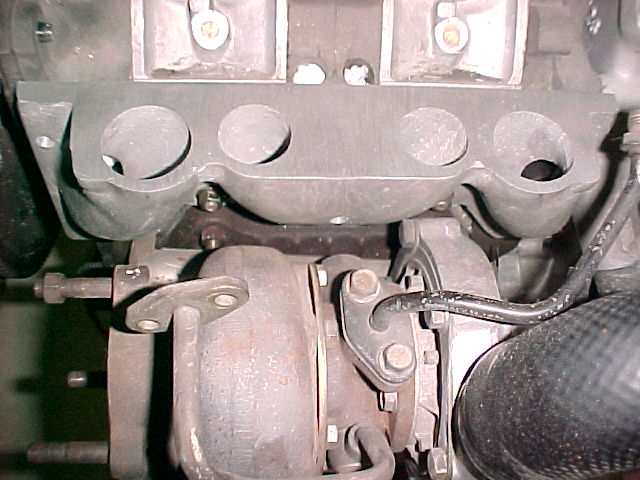
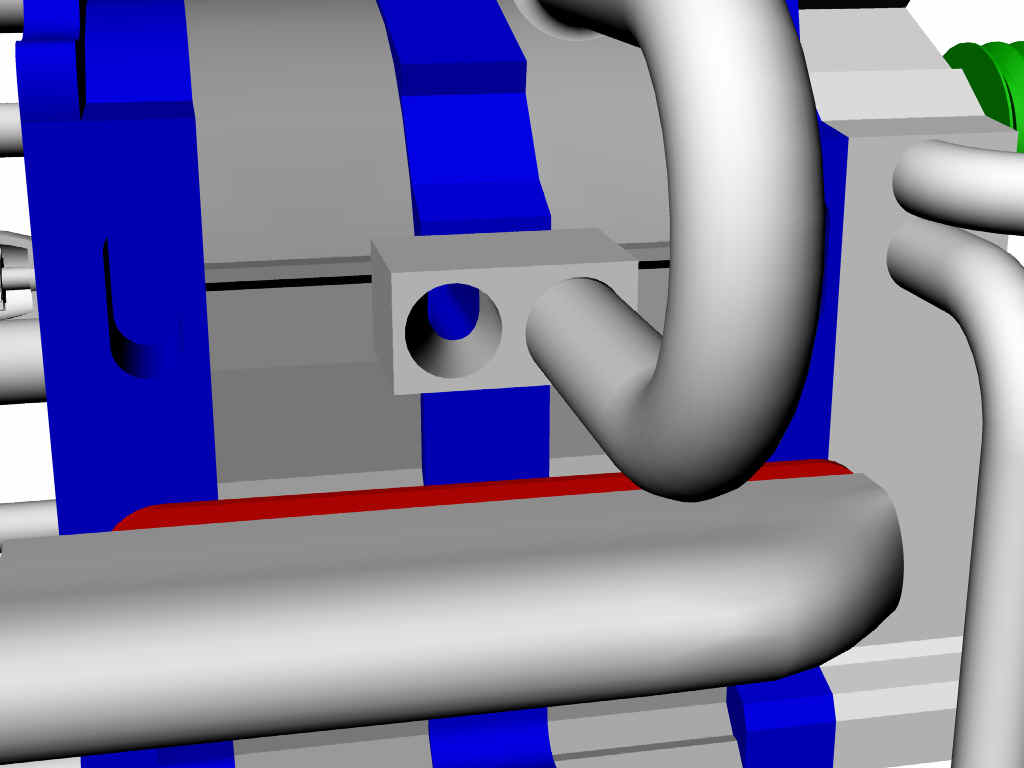
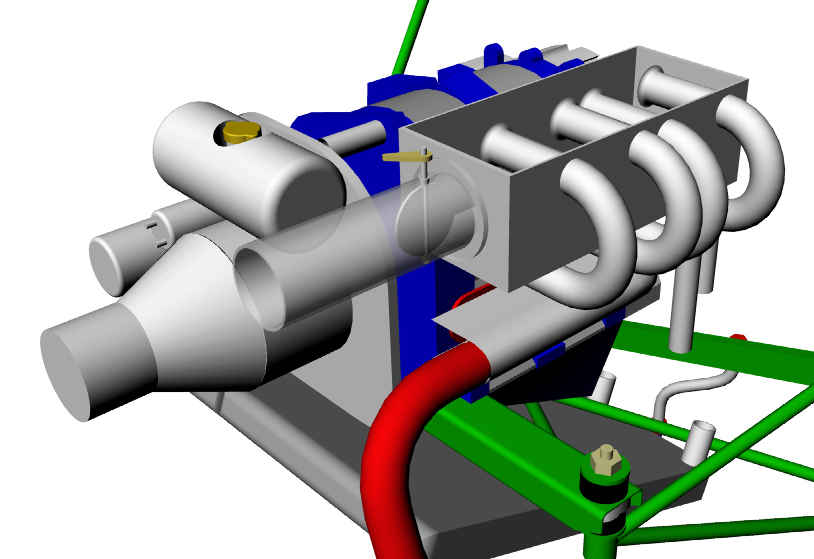
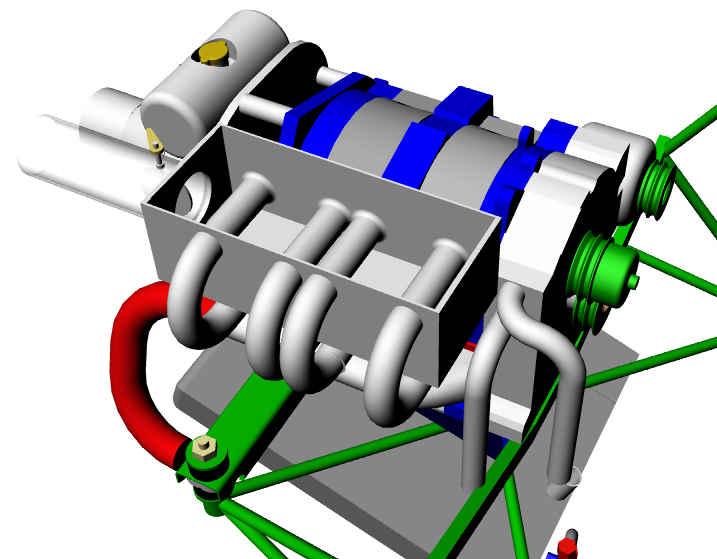
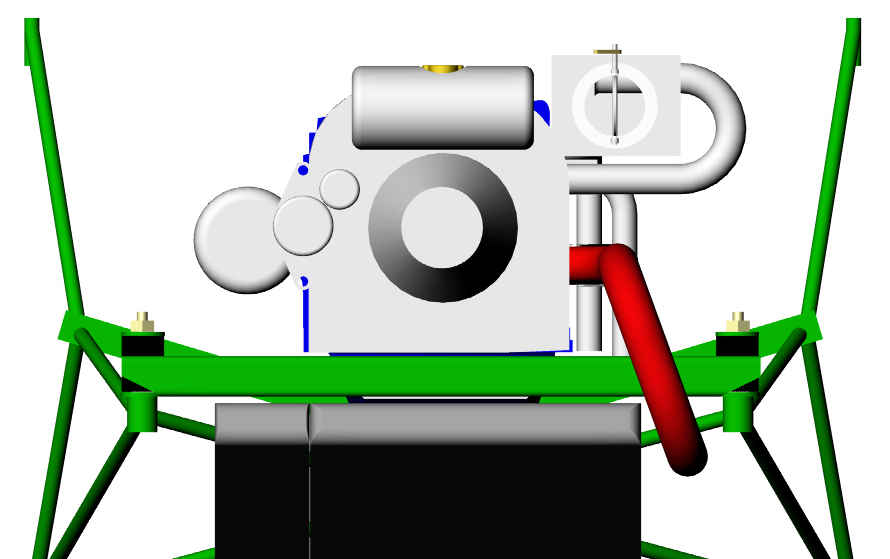
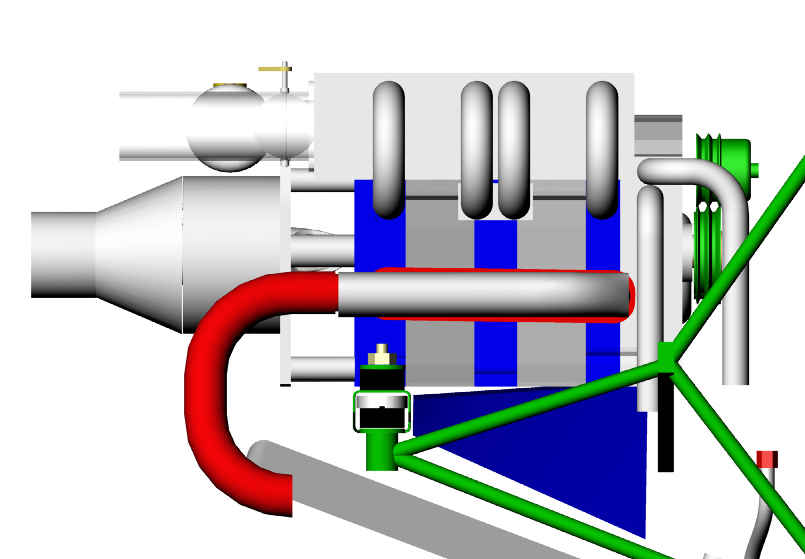
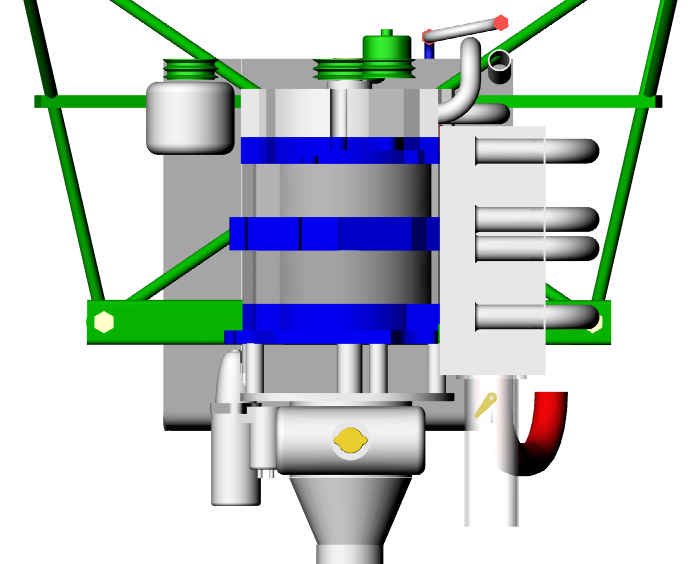
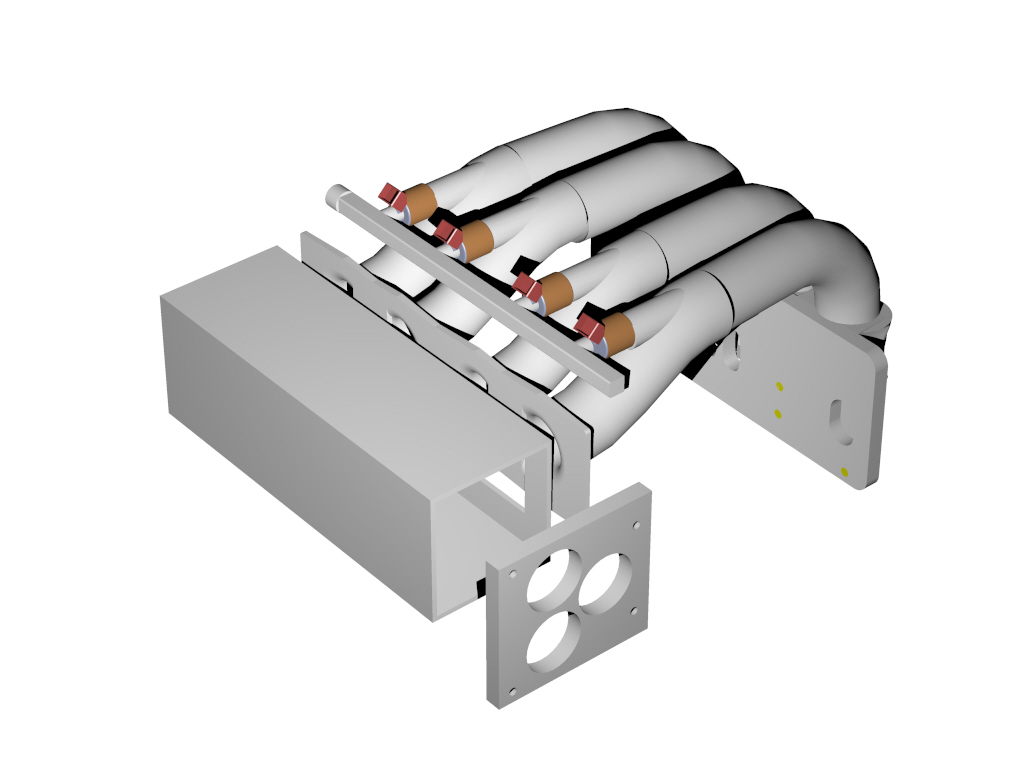
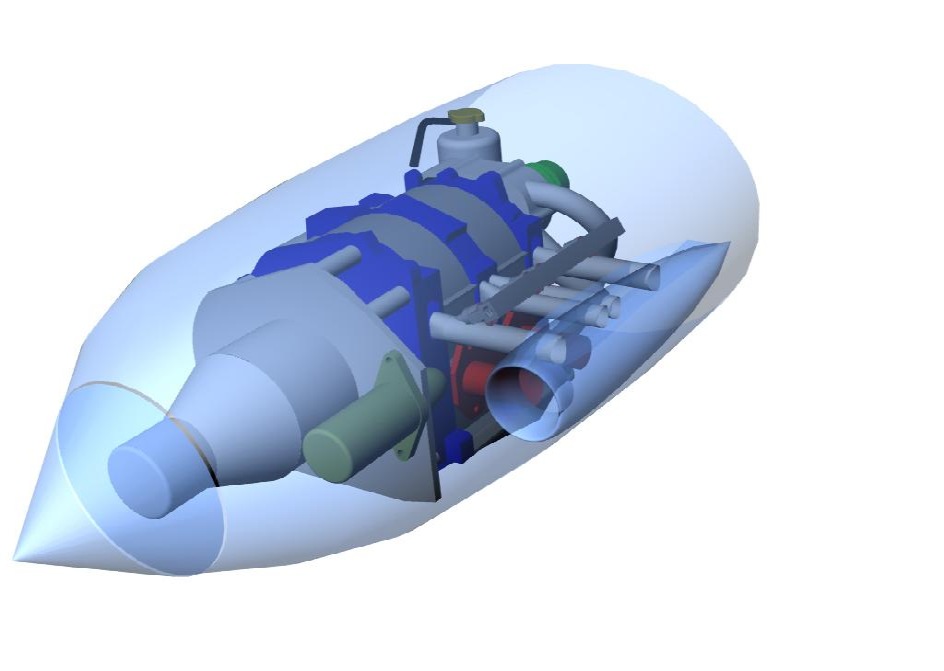
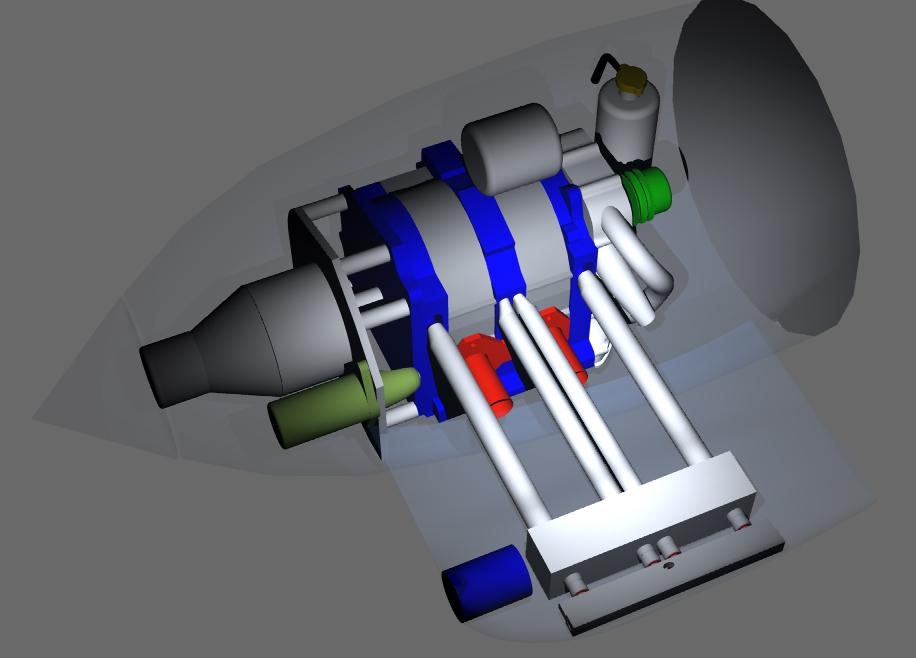
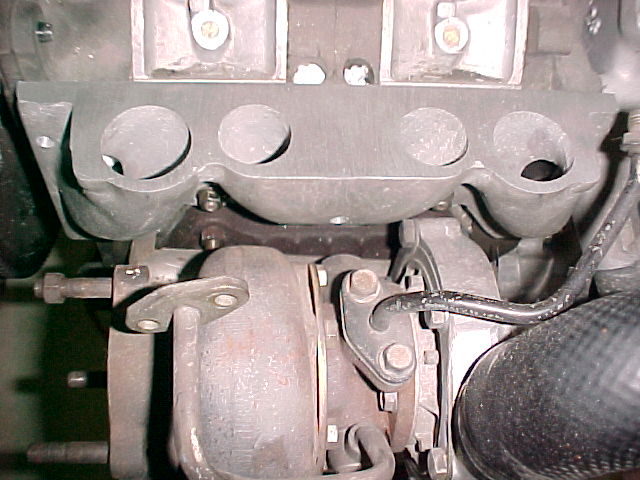
I am working on a kit for an RX8 manifold.
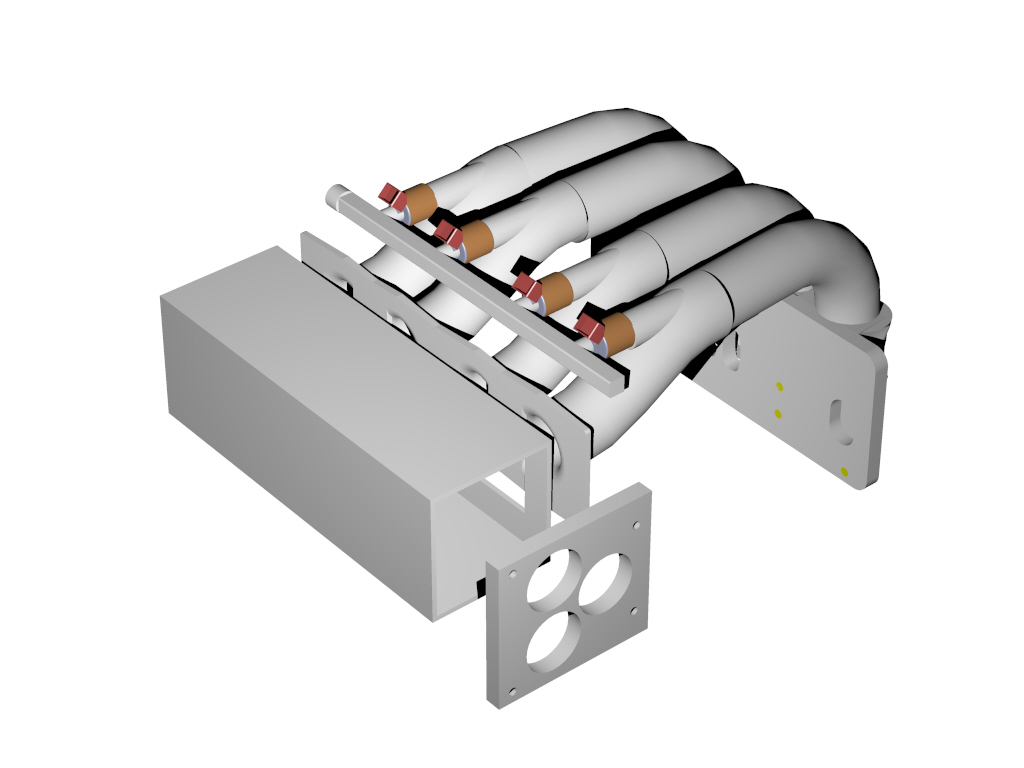
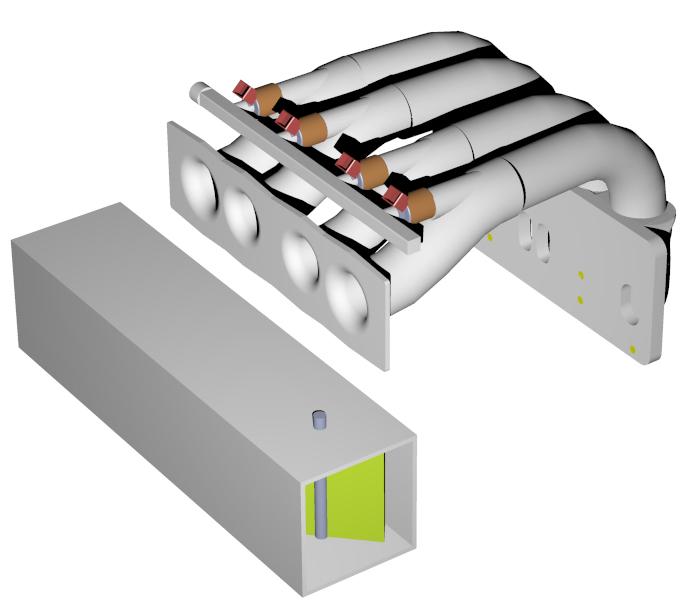
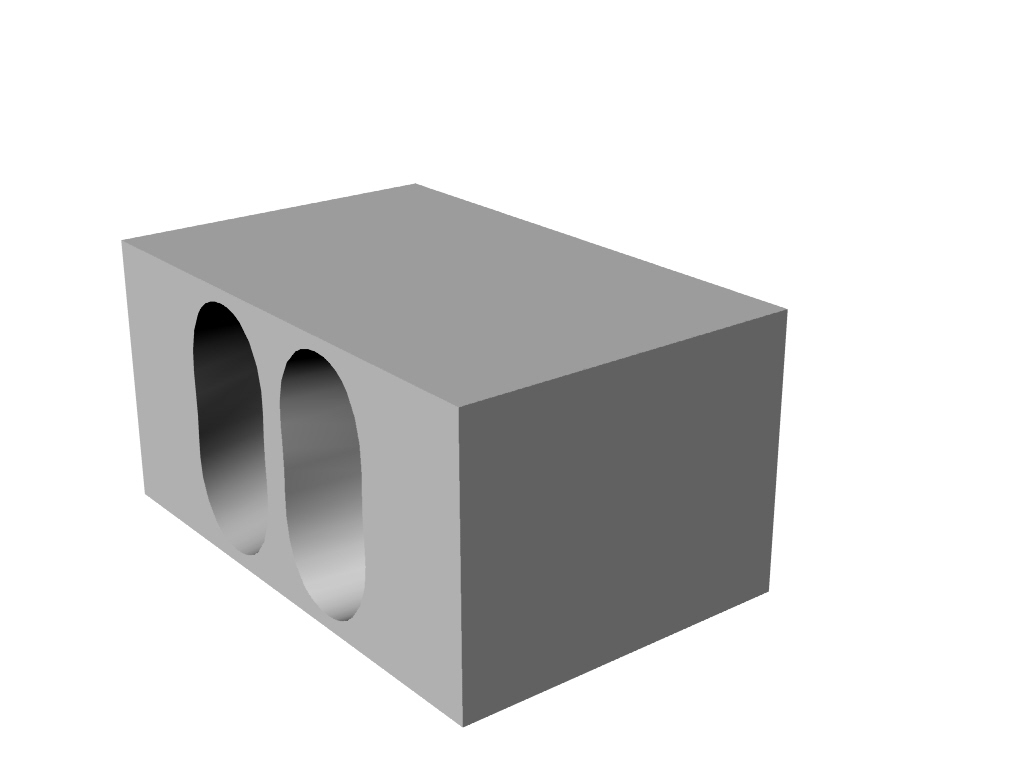
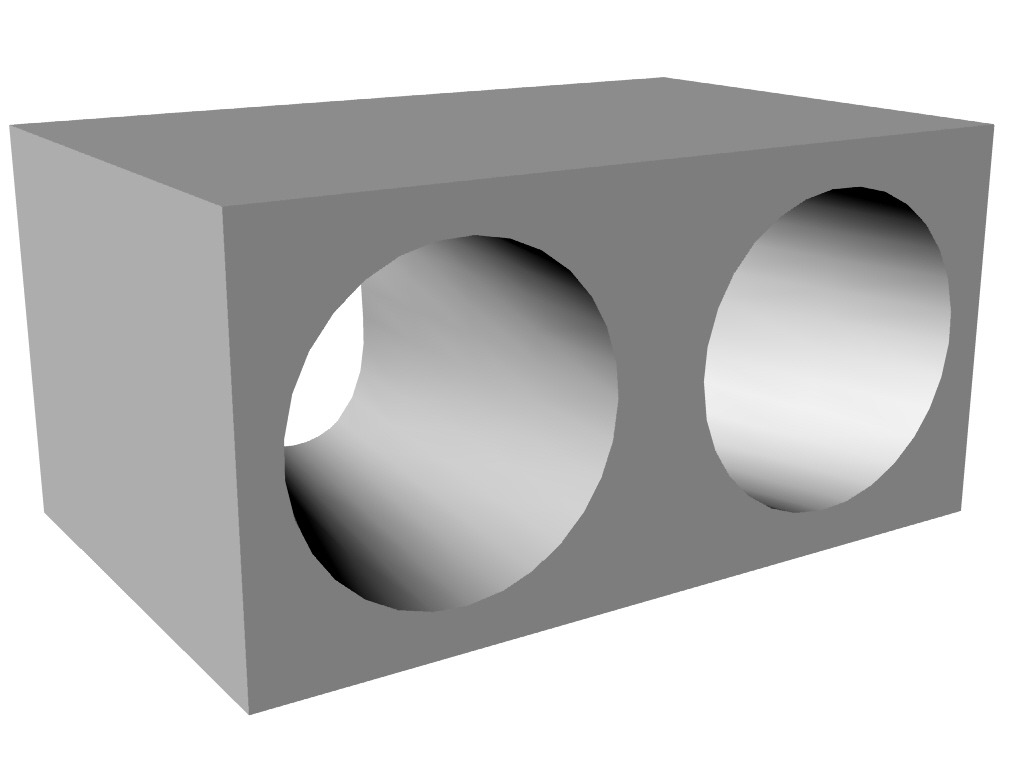
It consist of NC milled transition blocks from RX8 engine side ports to
round tubing
and a mounting flange.
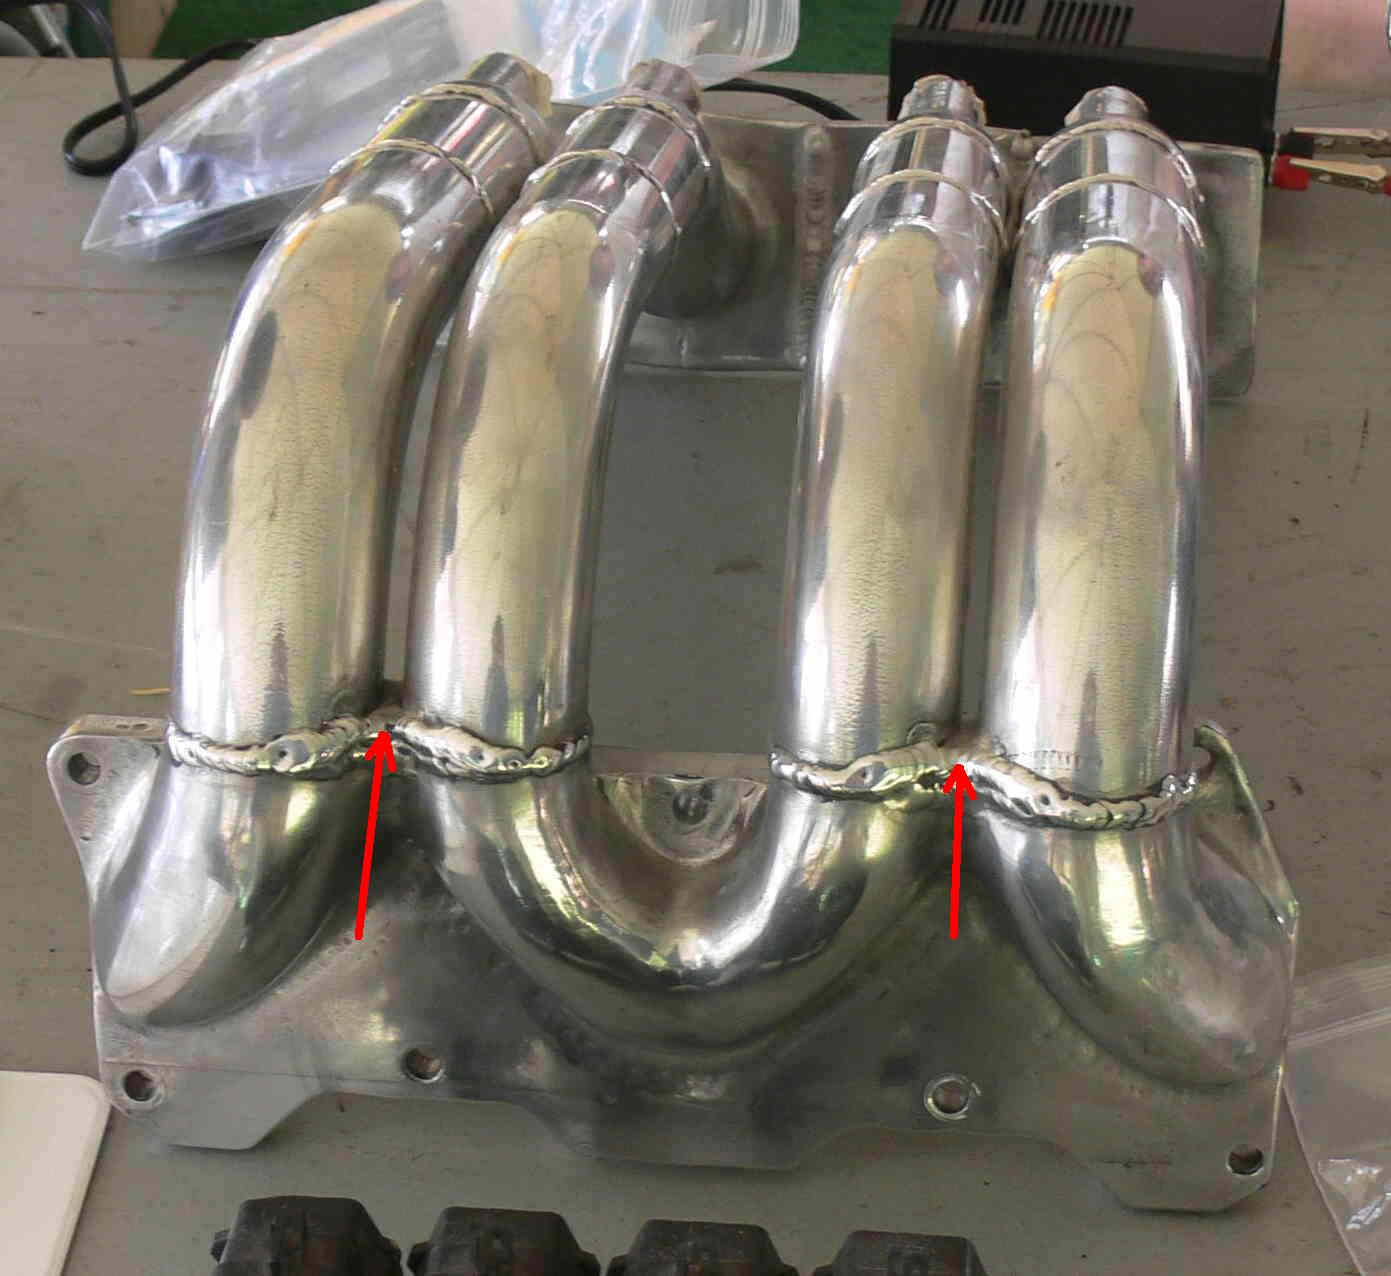
One problem is tig welding side by side tubes to the center housing block.
We first ran into this problem years ago when we cast a four port 13B
manifold.
There were ways around it but it was not pretty :)
Aluminum oven brazing can solve the problem. Brazing is strong and all
aluminum radiators are furnace brazed. Aluminum brazing paste melts at
750 degrees F.
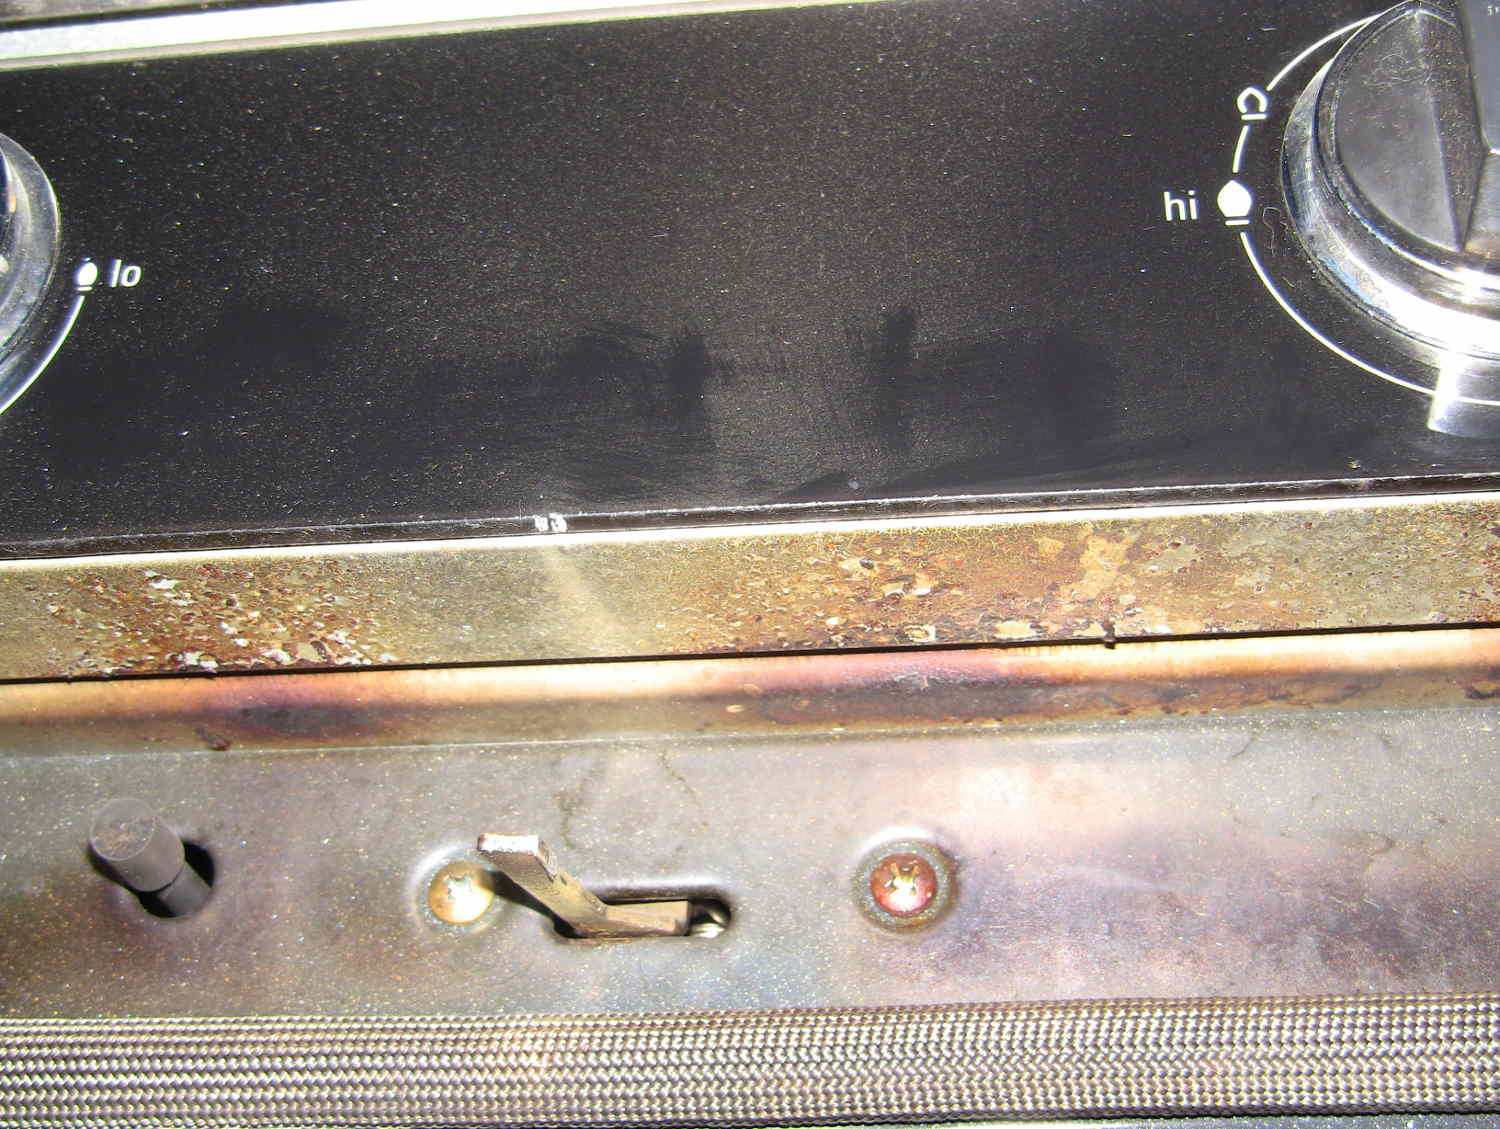
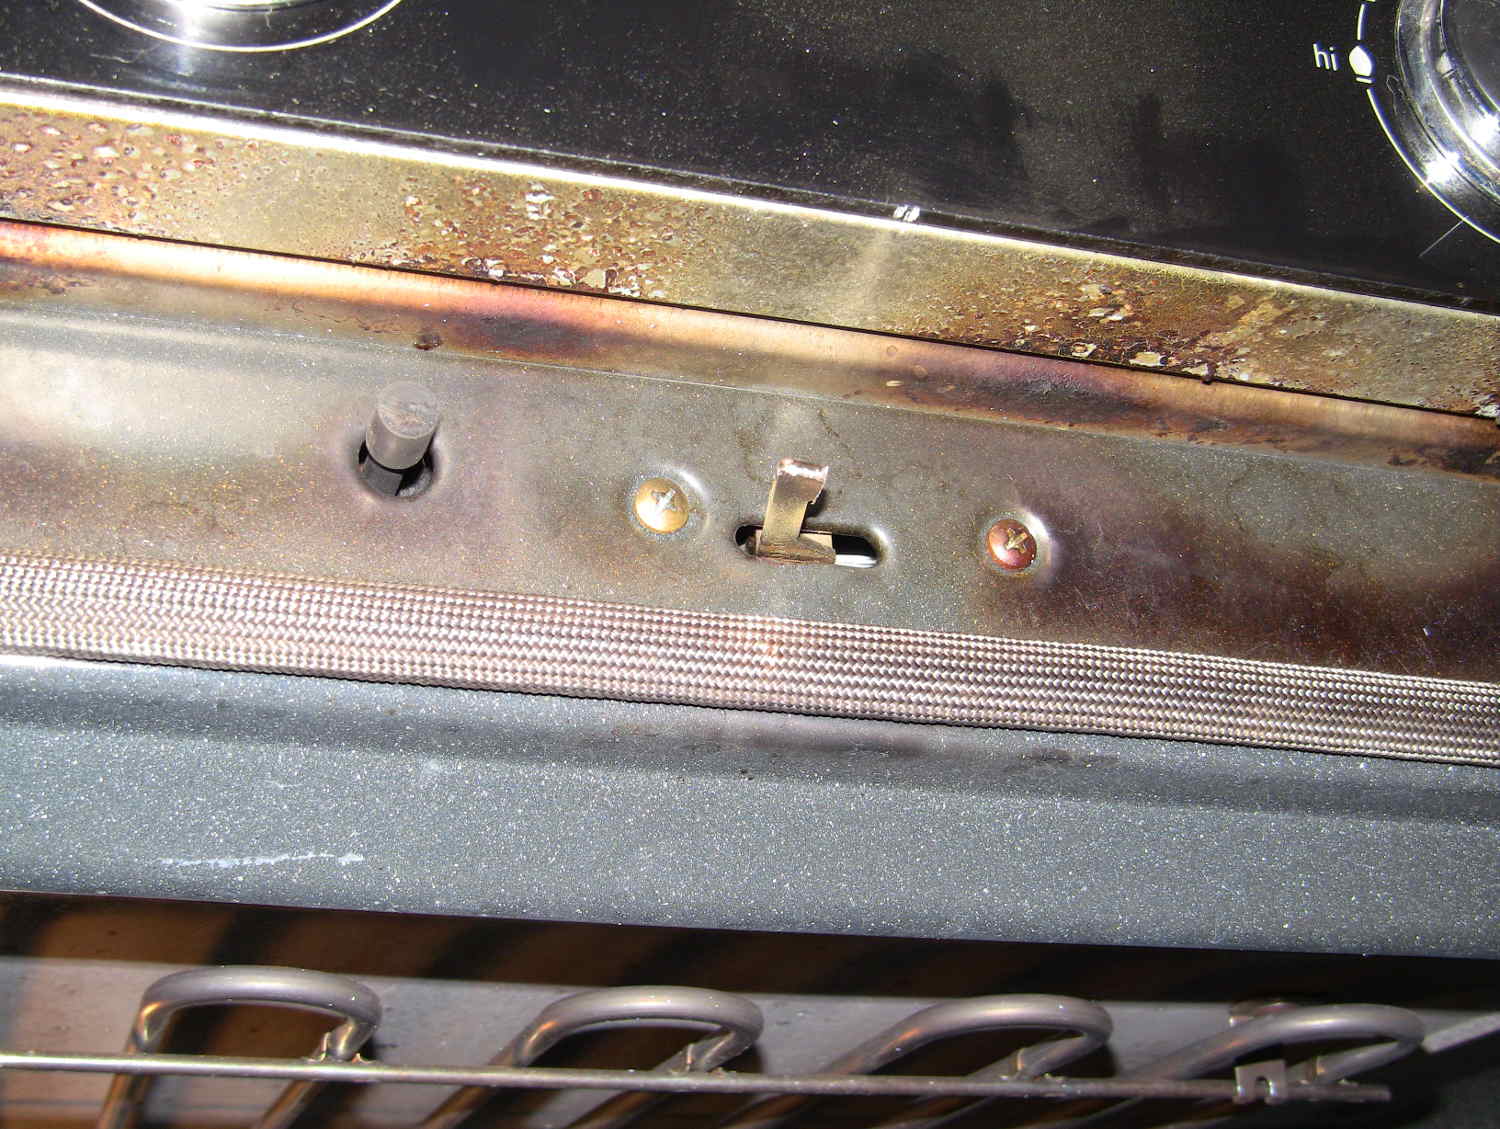
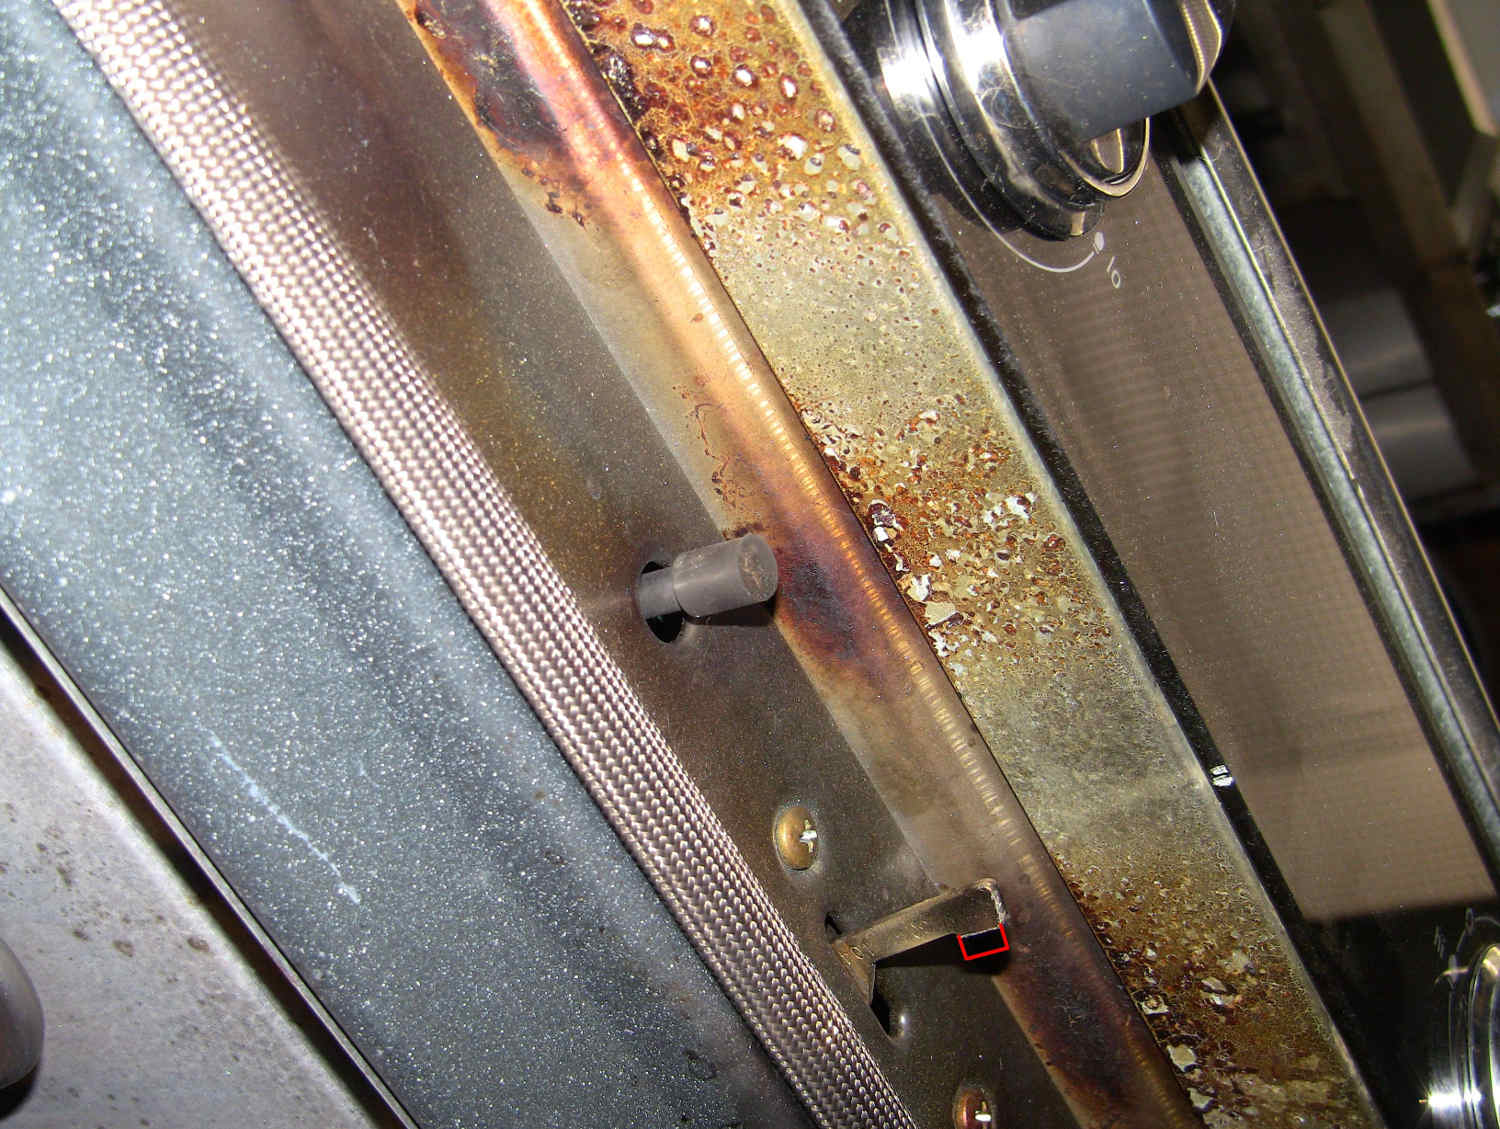
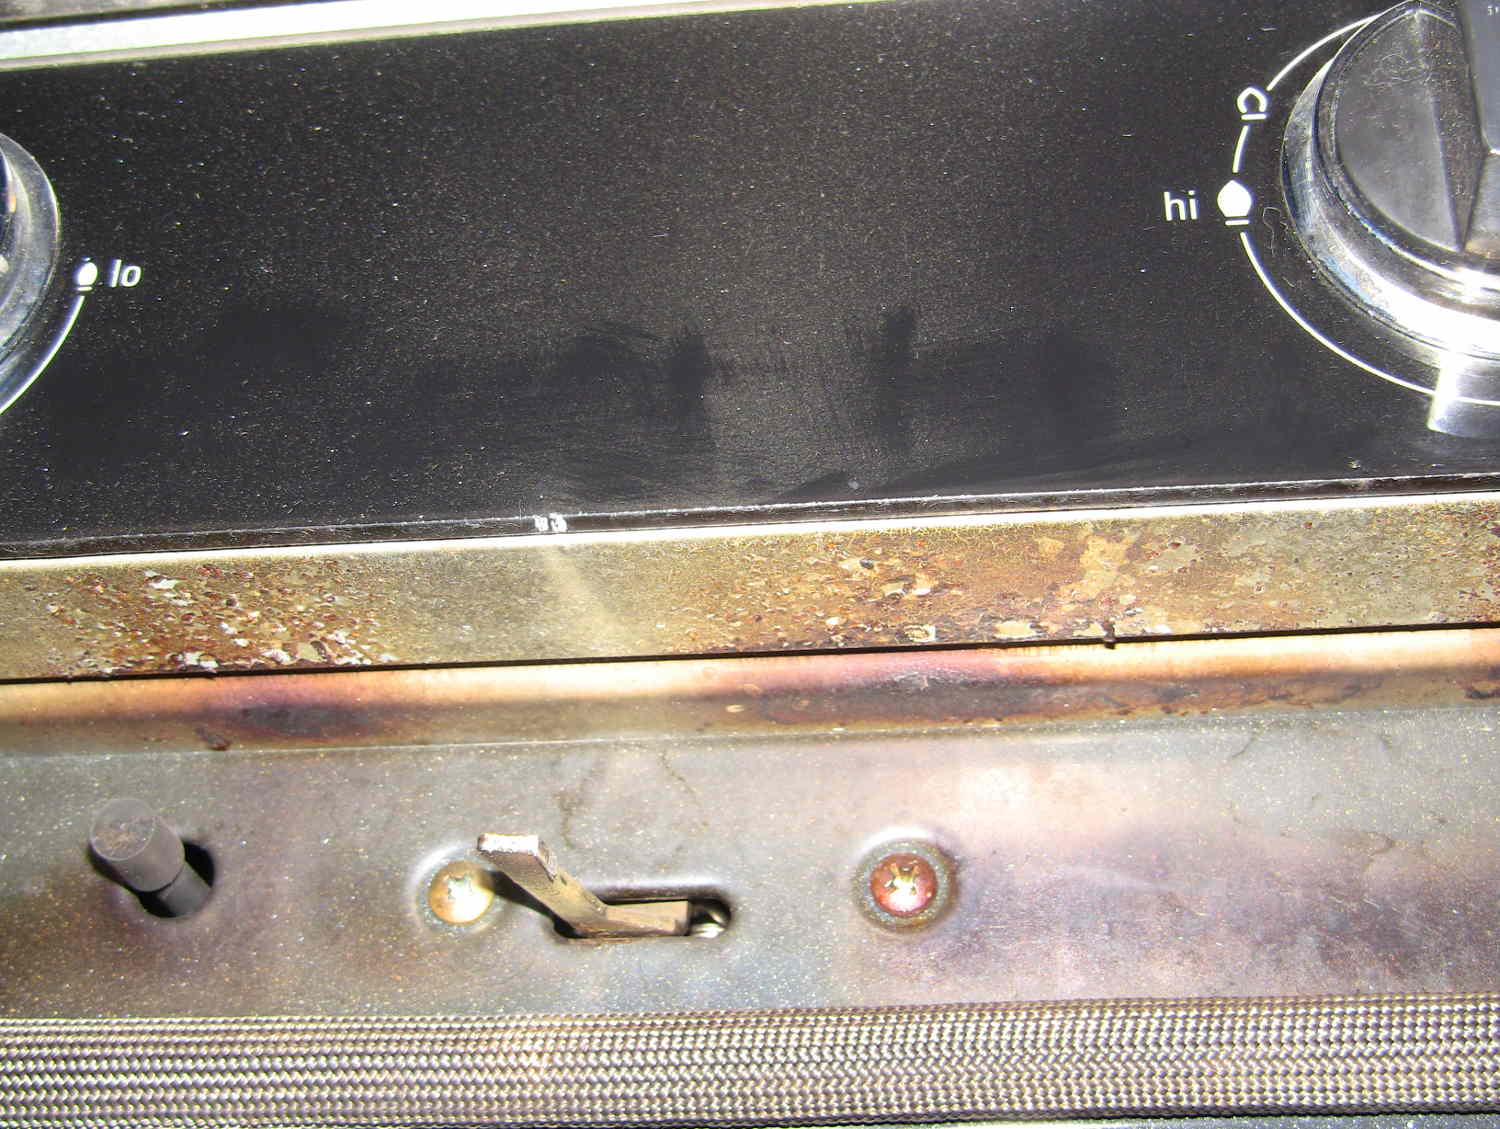
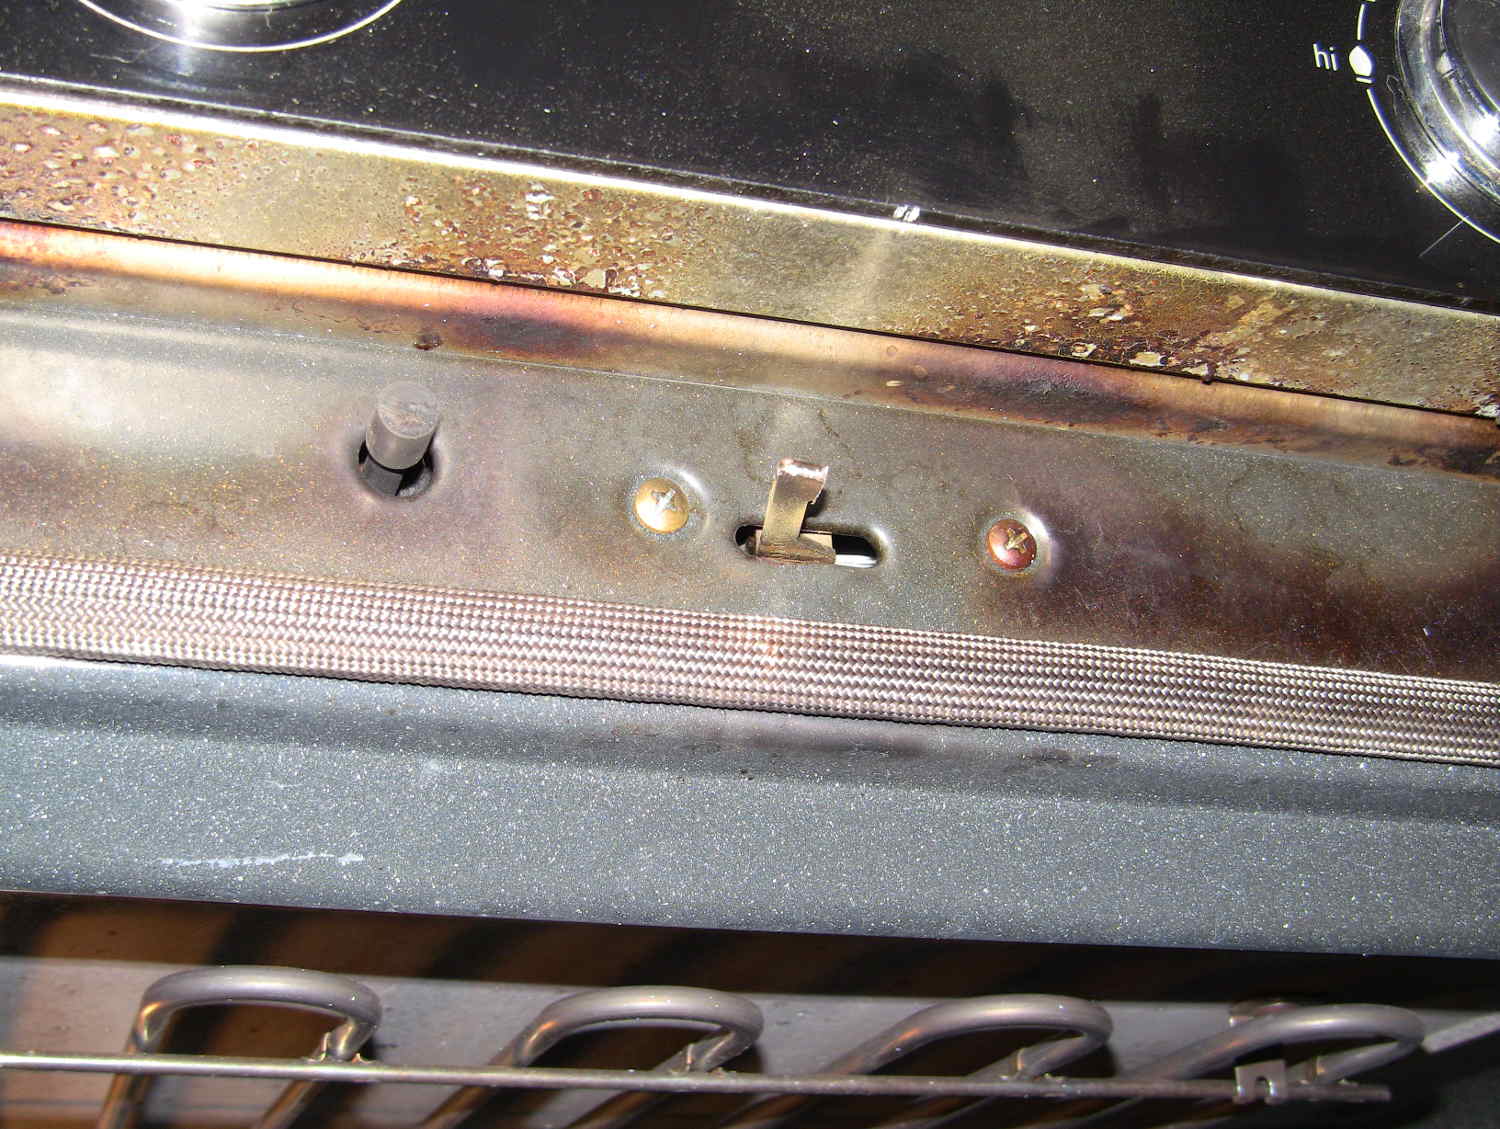
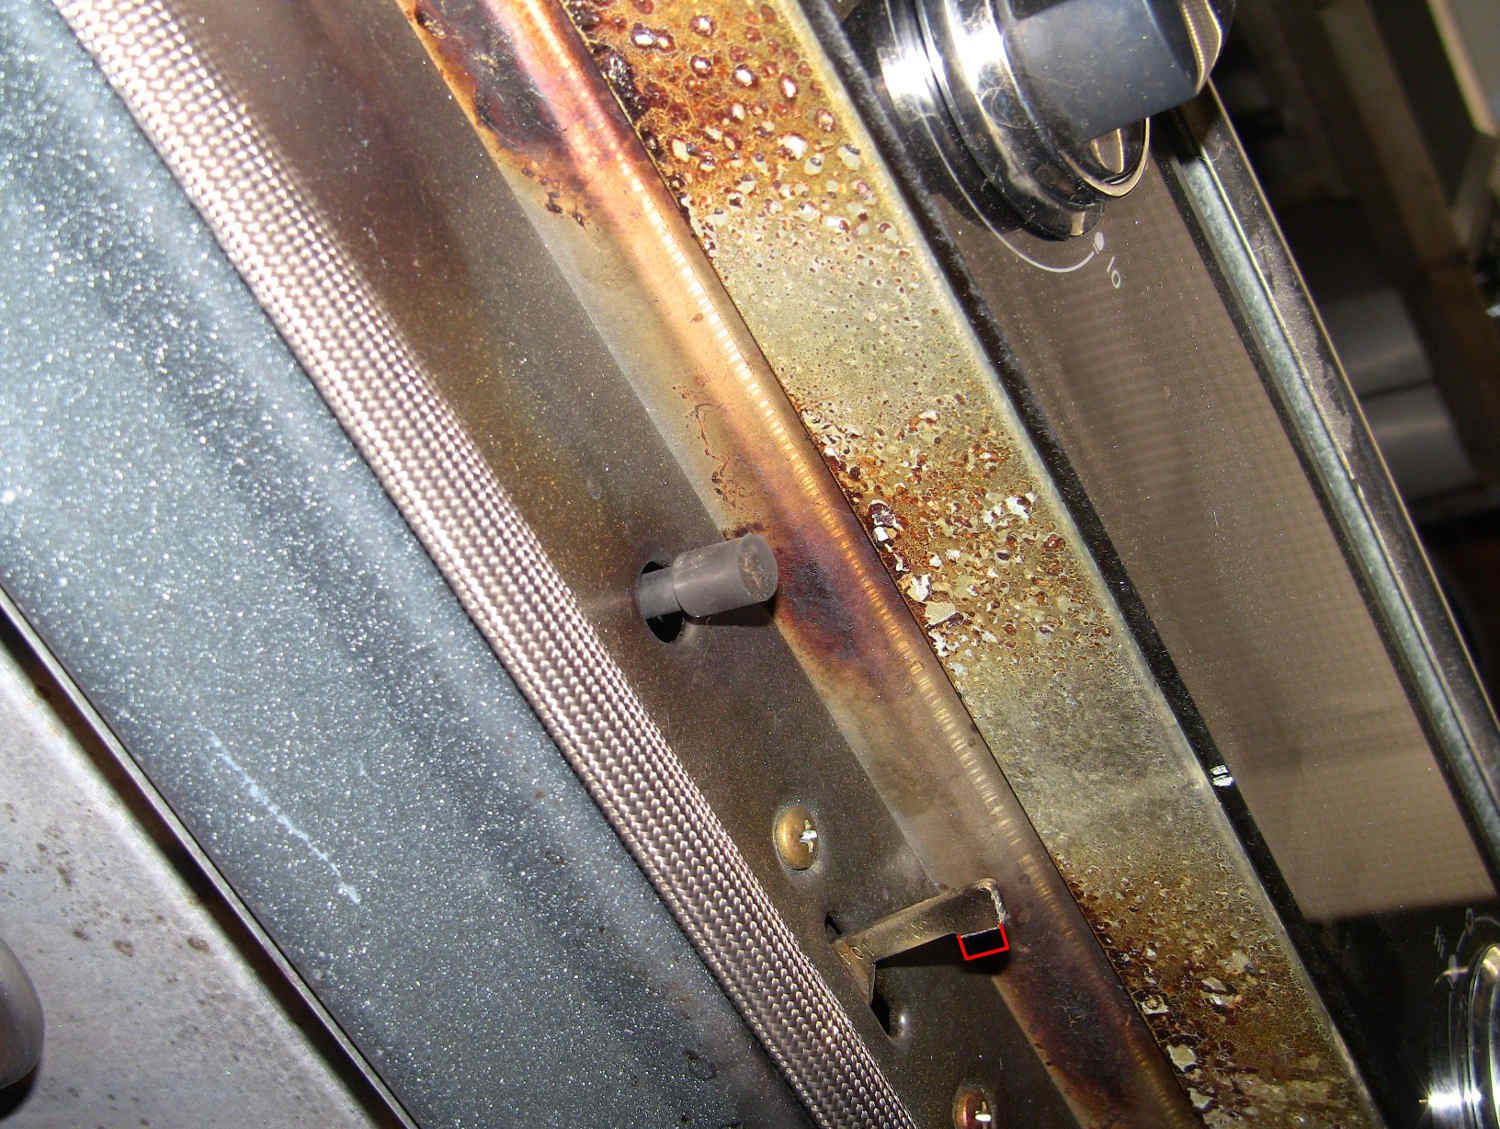
Here is the trick for modifying the self cleaning oven so you don't have to
burn a lot of juice or wait hours for things to happen or to cool off.
Cut the locking hook off with a hand held chop saw. Every shop should
have one as they are good for a lot things including making up AN SS
braided hose.
Be very VERY careful when messing around with a self cleaning oven.
The temperatures run to 800 F. Severe burns are likely and probable.
Use welders gloves and large water pump pliers to take parts out.
Also great for normalizing or softening aluminum so you can bend or form
it it with
out cracking it.
I am thinking of offering the manifold as a kit so you can braze it or
tig weld it.
Your choice. Or I can braze it for you for a fee.
lots of configurations are possible. EFI or carb.
Paul Lamar
The Rotary Engine News Letter. Powered by Linux.
ACRE NL web site.
http://www.rotaryeng.net
You Tube
http://tinyurl.com/beqqxas
Copyright 1998-2013 All world wide rights reserved.