Looks like you pressed the planet carrier shafts out and sheared the
retaining roll pins. Surprisingly and apparently that works :-)
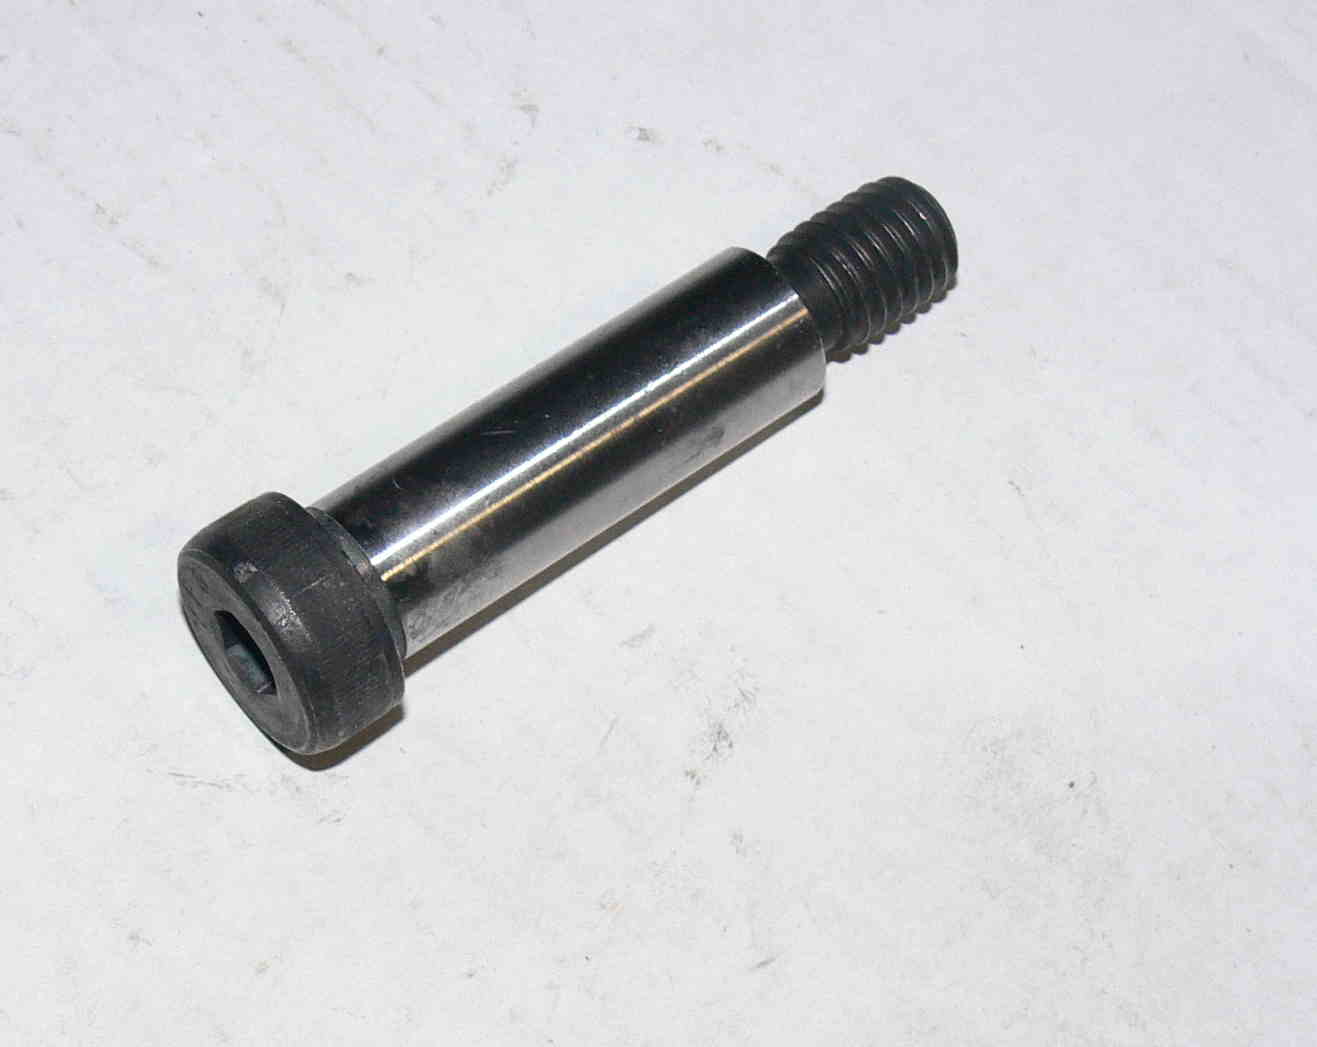
Looks like you are going to replace them with a hardened and ground
down sholder bolt.
Good Idea. That should cut the cost somewhat as there is no need to
EDM a hole in the planets shafts.
Paul Lamar
Paul
I am going to see a metal treatment cie at Boynton Beach tomorrow to
find out what hardness the shaft are in the mean time checking the
hardness on those bolt plus if need to be retreated for proper hardness.
the pins are easy to shear.
The cv shaft are machinable the only hard treatment is about 116" deep
where the ball bearing travel, I can grind it only at the location which
I do have to use the end mill to remove the excess of metal on indexing
table with the milling machine.
those bolts used as a shaft can be lock with pressure pins at the same
place or spot weld the exceeding treads sideway.
The prop flange you saw is only a dommy which I practice on the milling
for logs locations, a good one is already done with 58"dia lugs.
It is very cheap on Ebay the flange about $32 and the cv shaft $60 plus
$100 for bearings and seal ,the shaft can be used with center holes 316"
for constant speed prop and true the copper sleeve.
JEAN PRUDHOMME
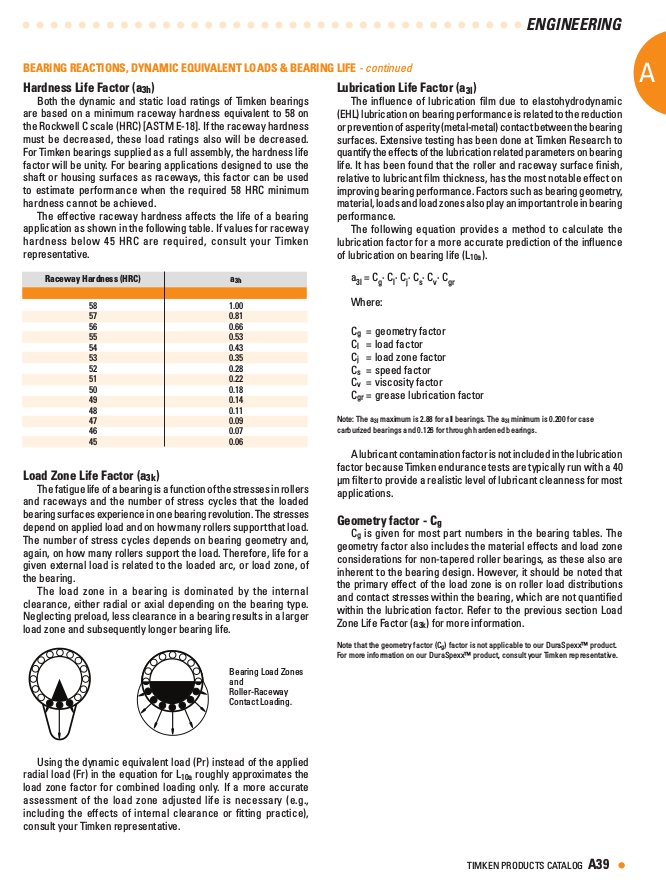
Won't hurt but the spec for needle bearings shaft hardness and finish
is in the the bearing catalogs.
Rockwell C 58 is the required hardness and the shaft finish is 15 RMS
maximum.
I will have the 5/8th dia. shoulder bolts ground down to 15.5 mm for
the 3.12:1 Ford rear planet
carrier. They may already be hard enough however it is wise to check.
Paul Lamar
The Rotary Engine News Letter. Powered by Linux.
ACRE NL web site.
http://www.rotaryeng.net
You Tube
http://tinyurl.com/beqqxas
Store
http://www.rotarpower.com/#!
Copyright 1998-2015 All world wide rights reserved.