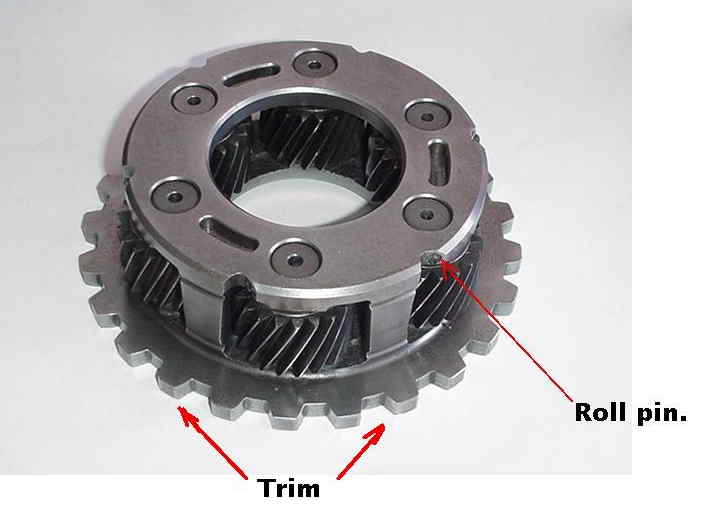
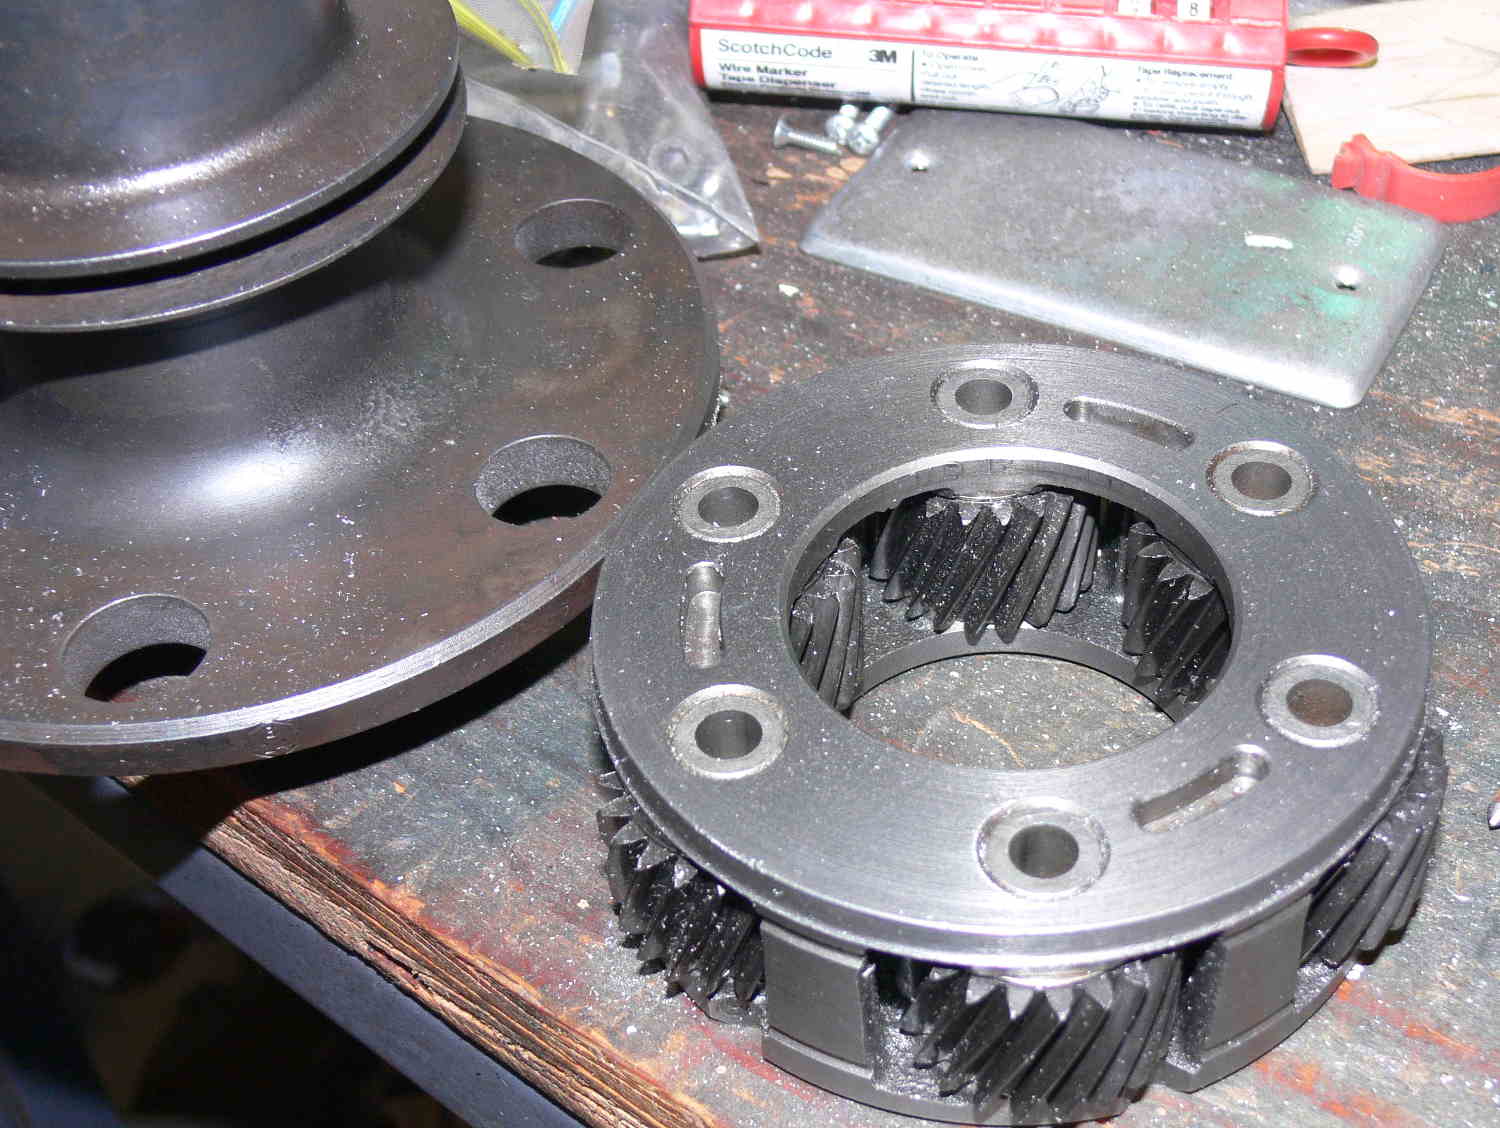
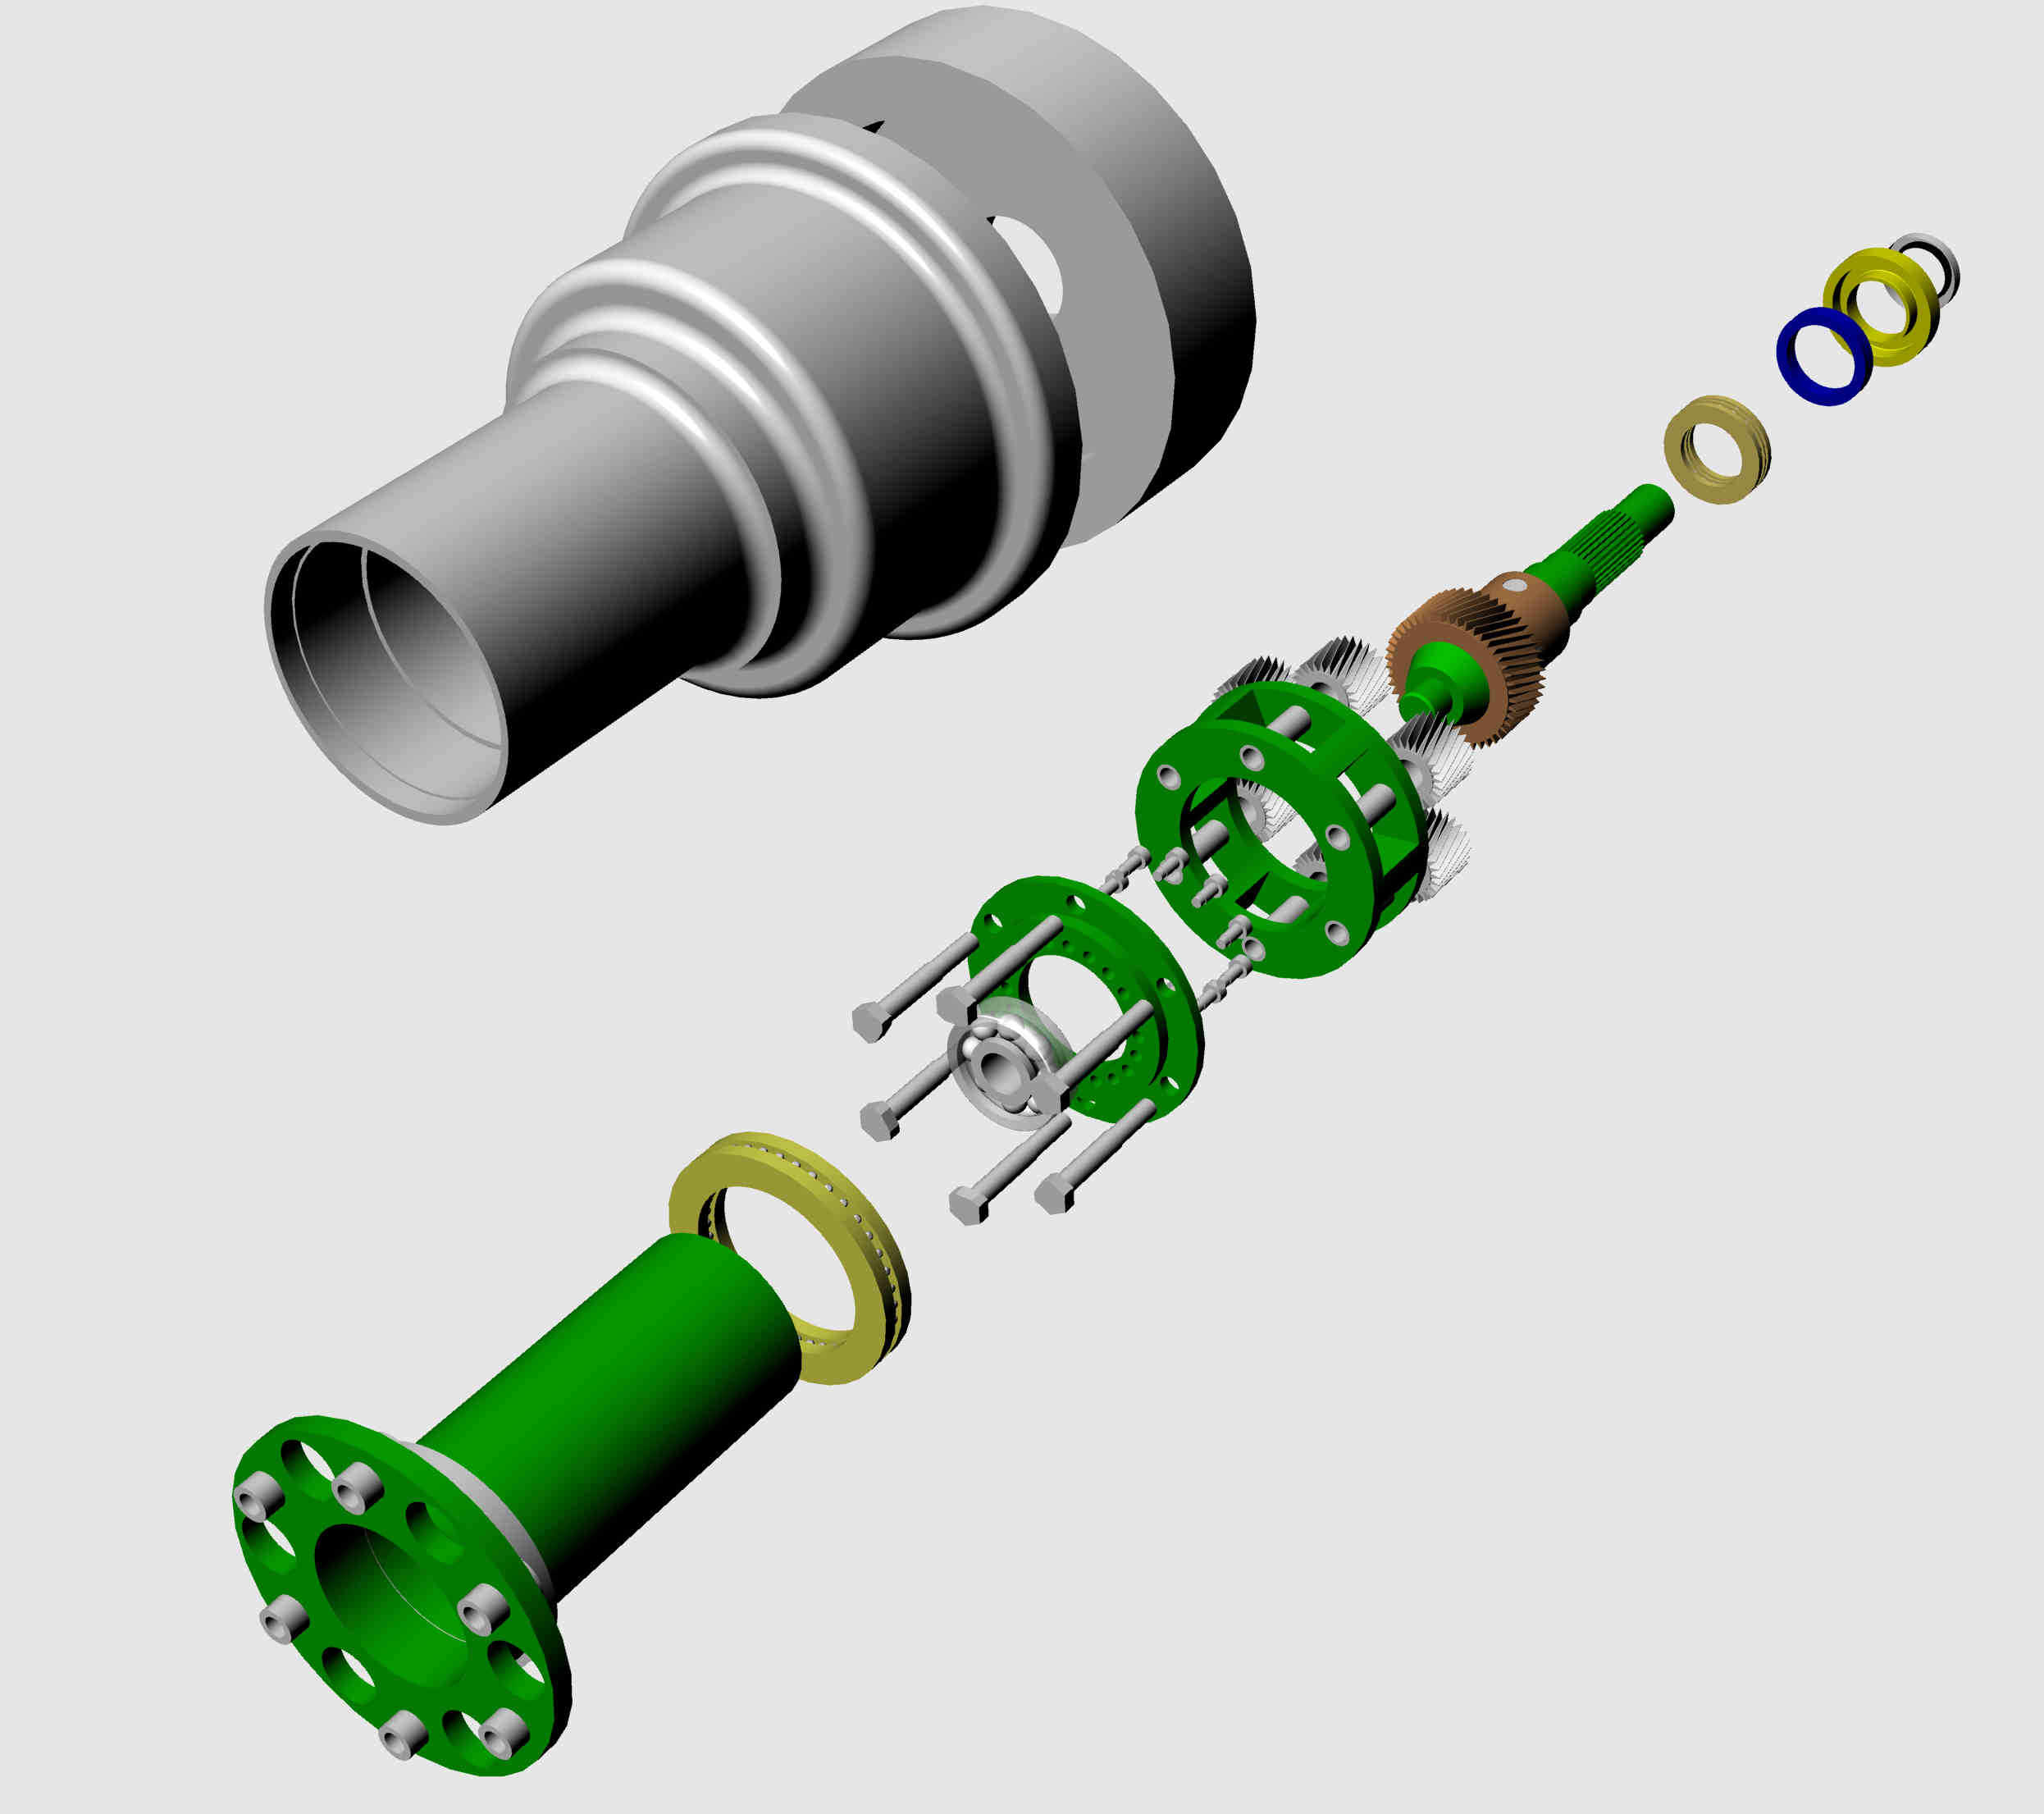
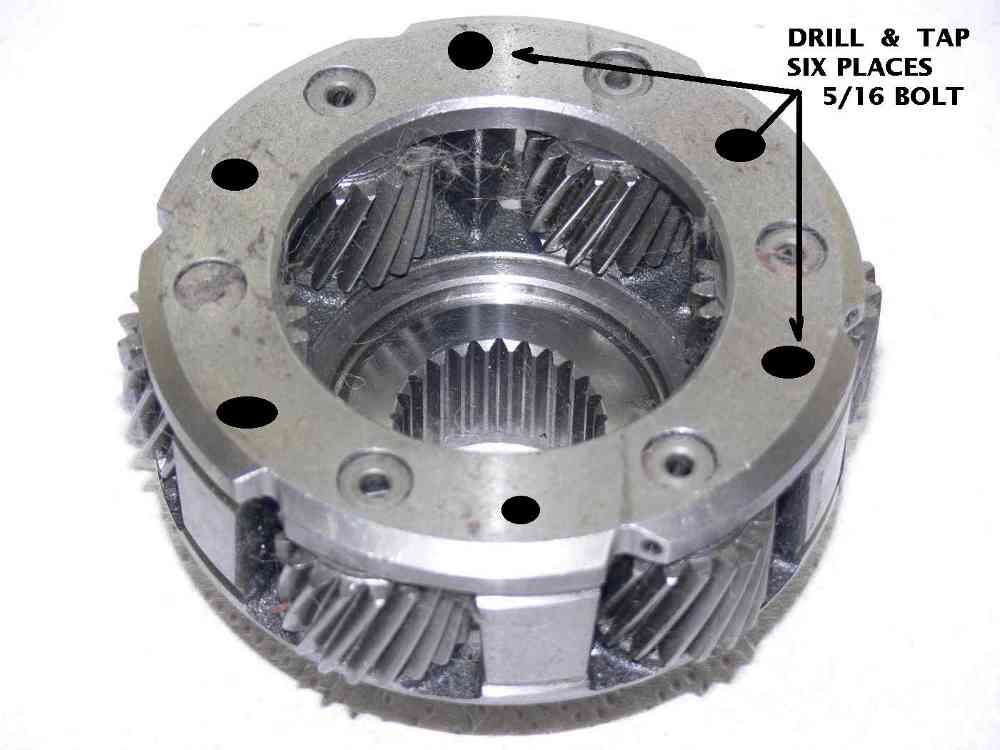
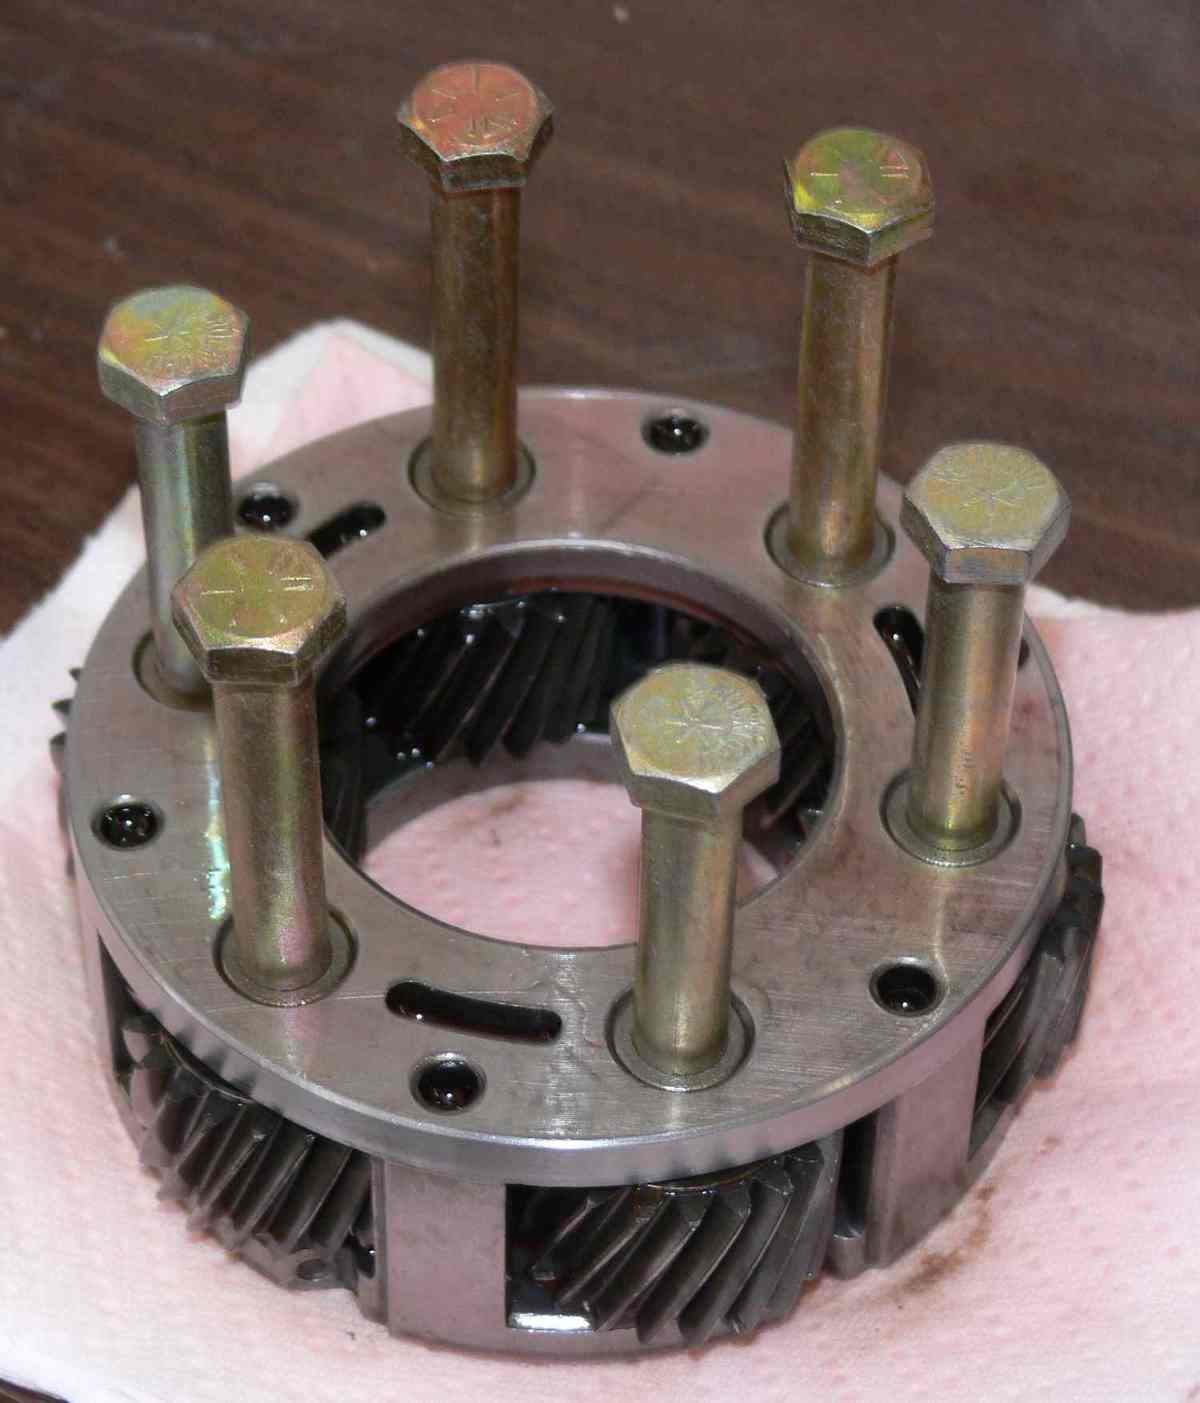
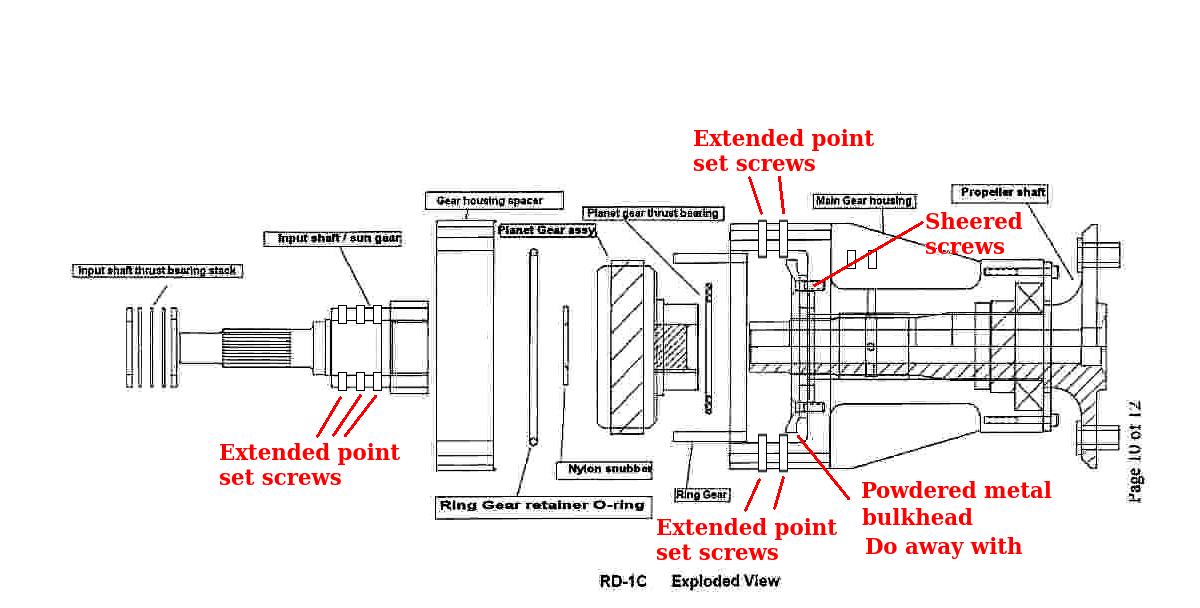
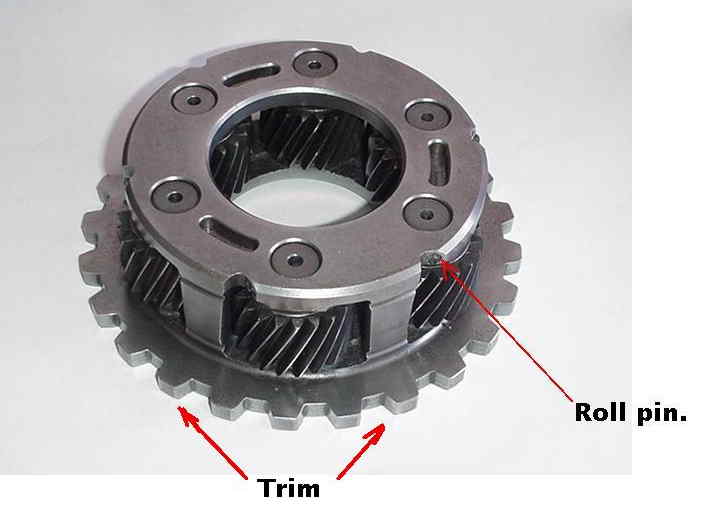
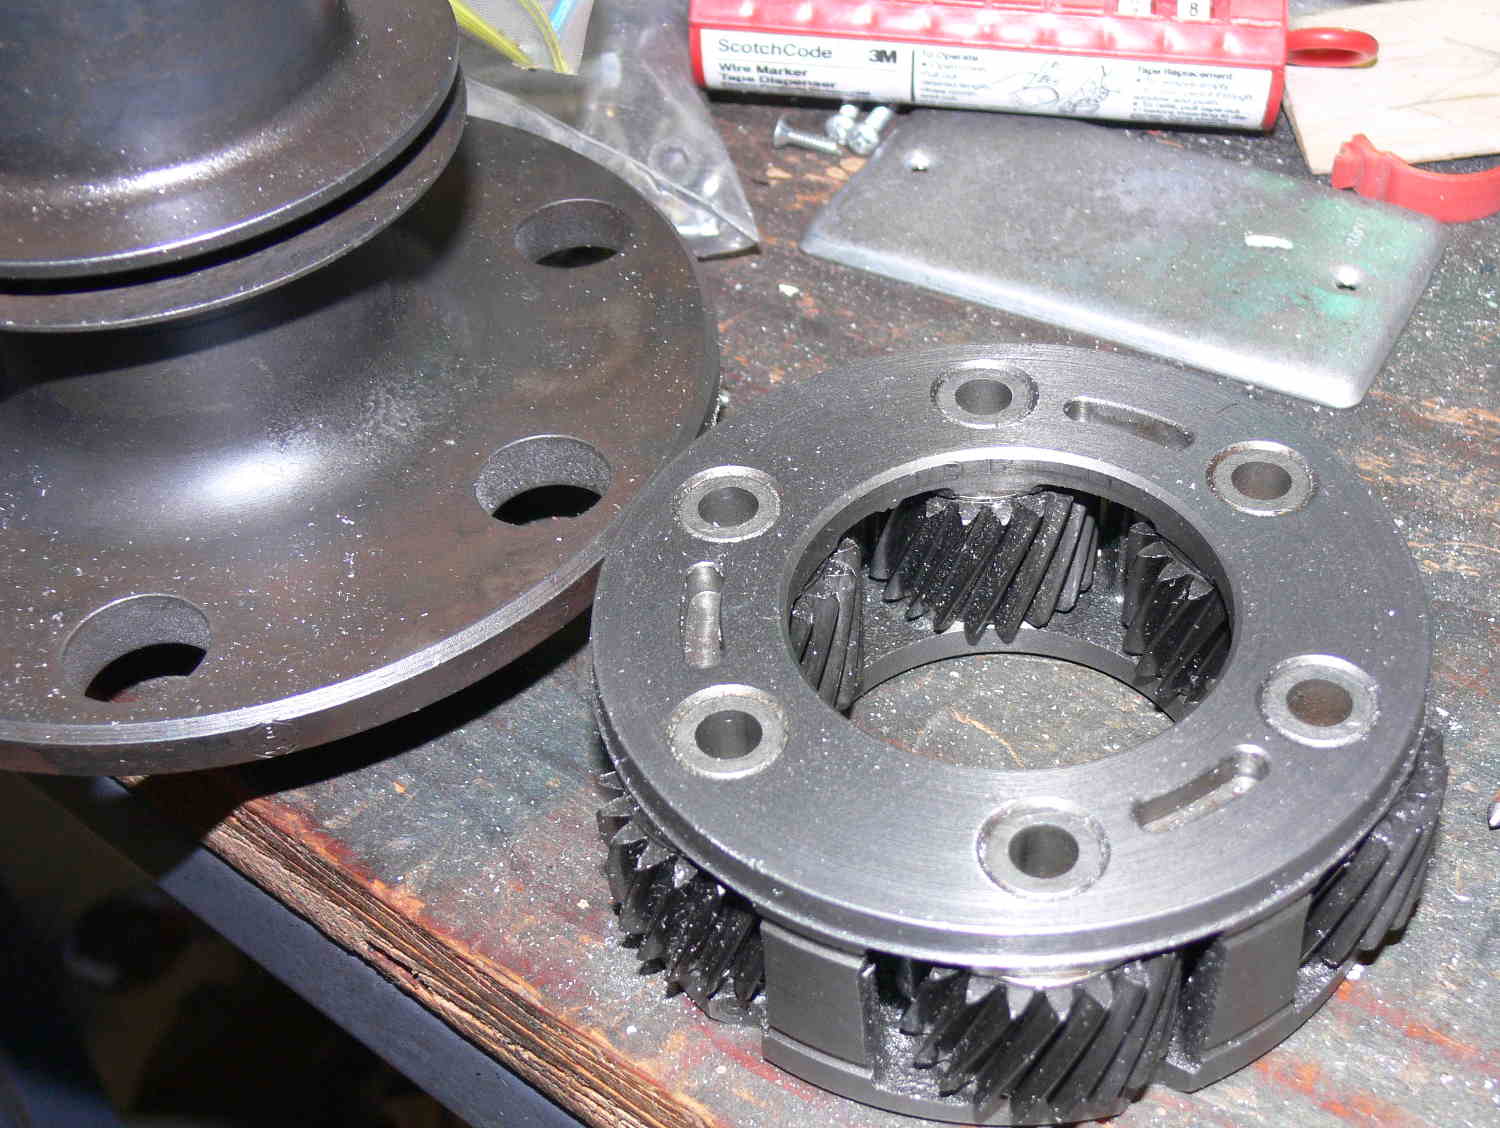
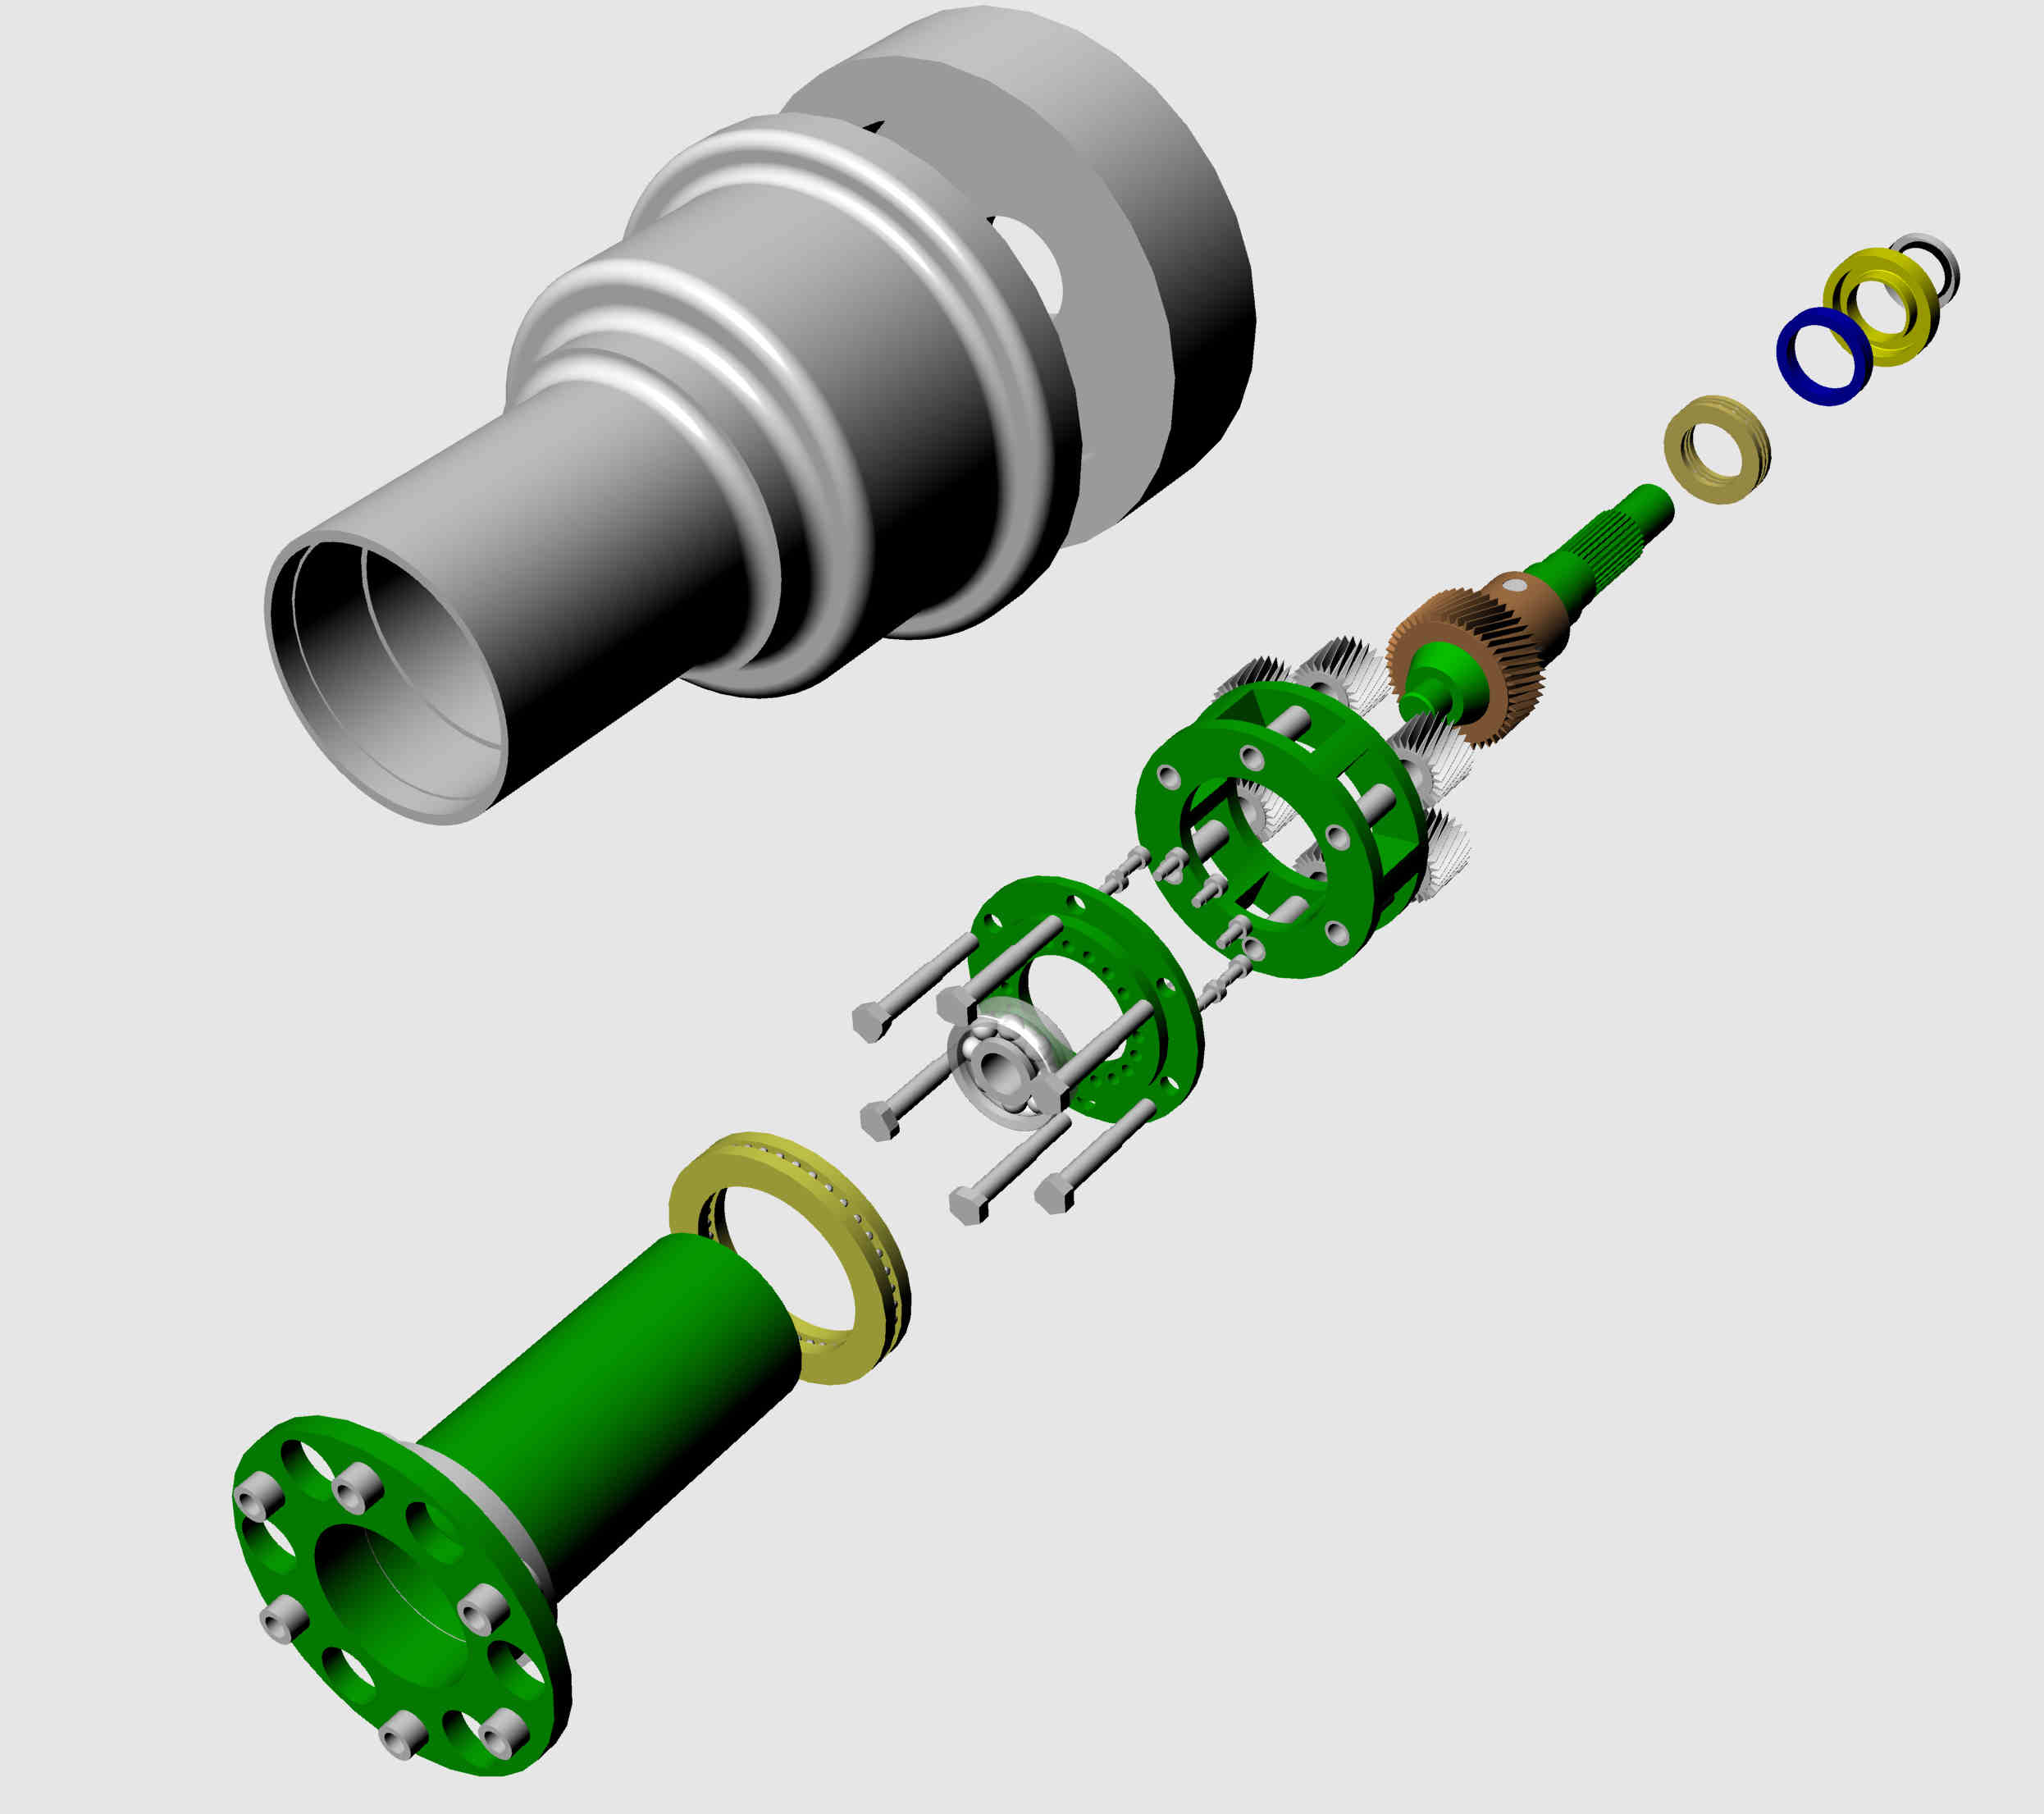
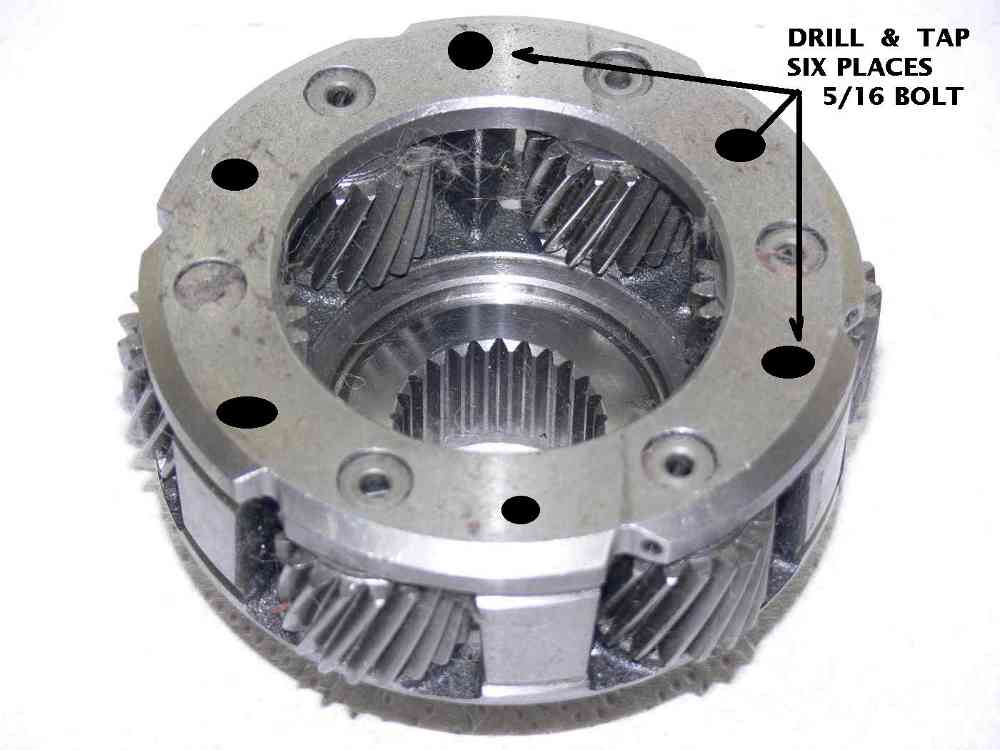
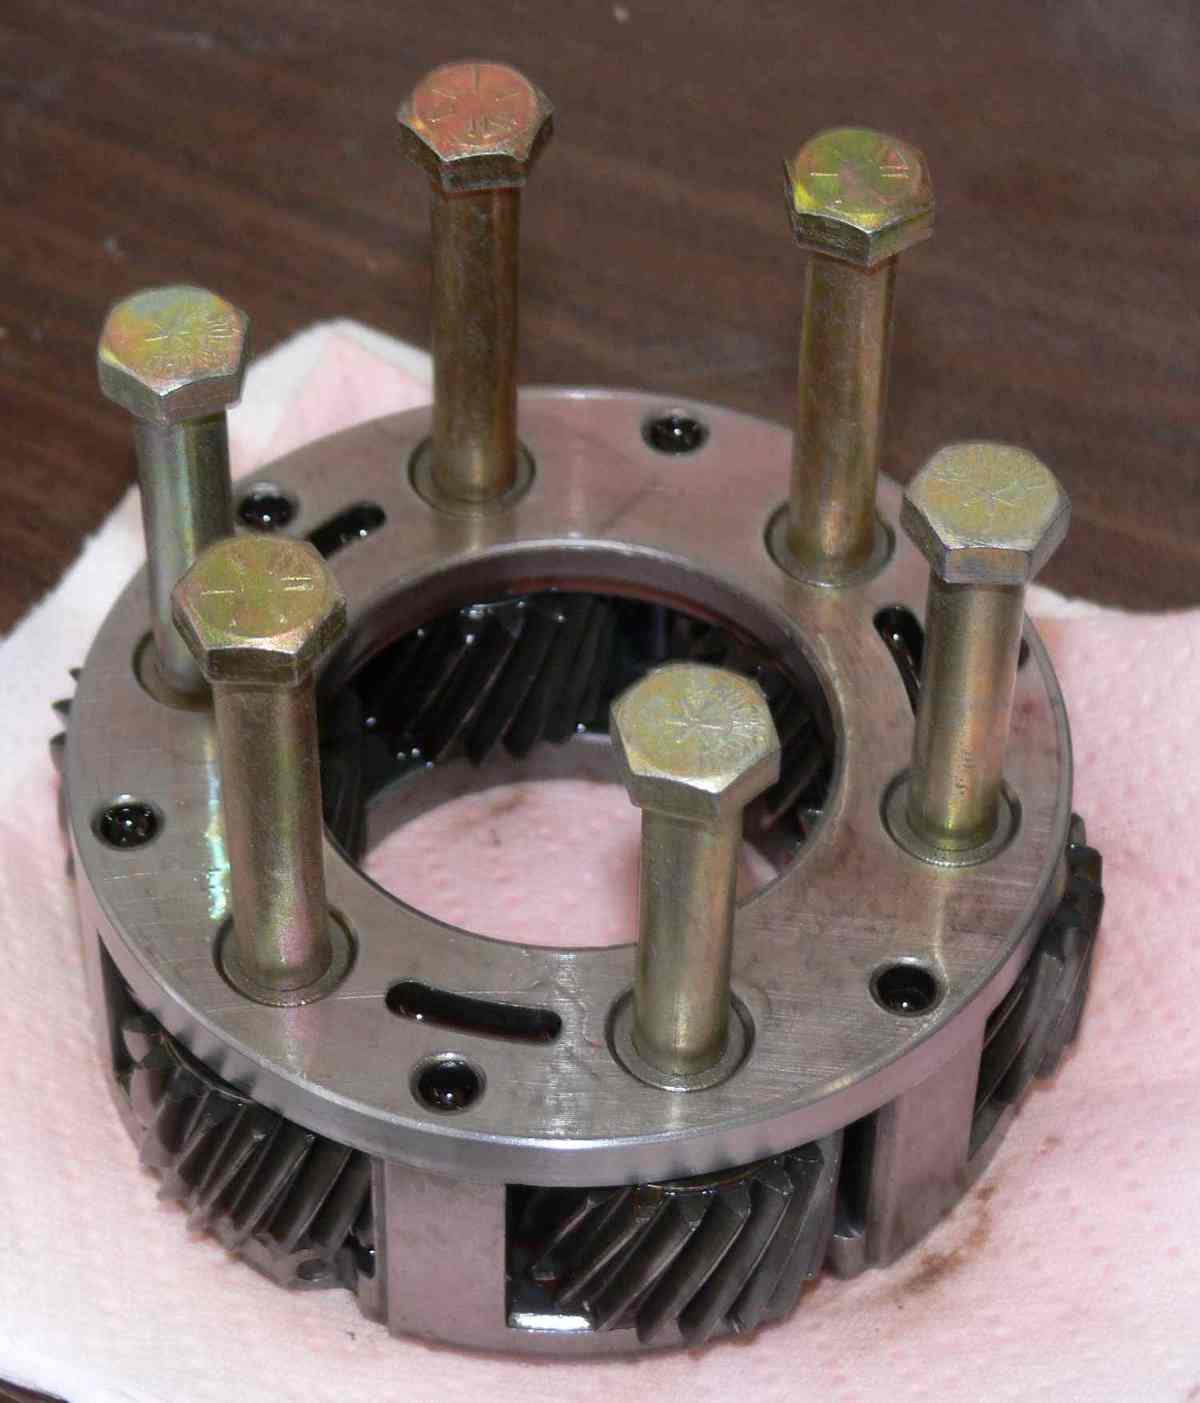
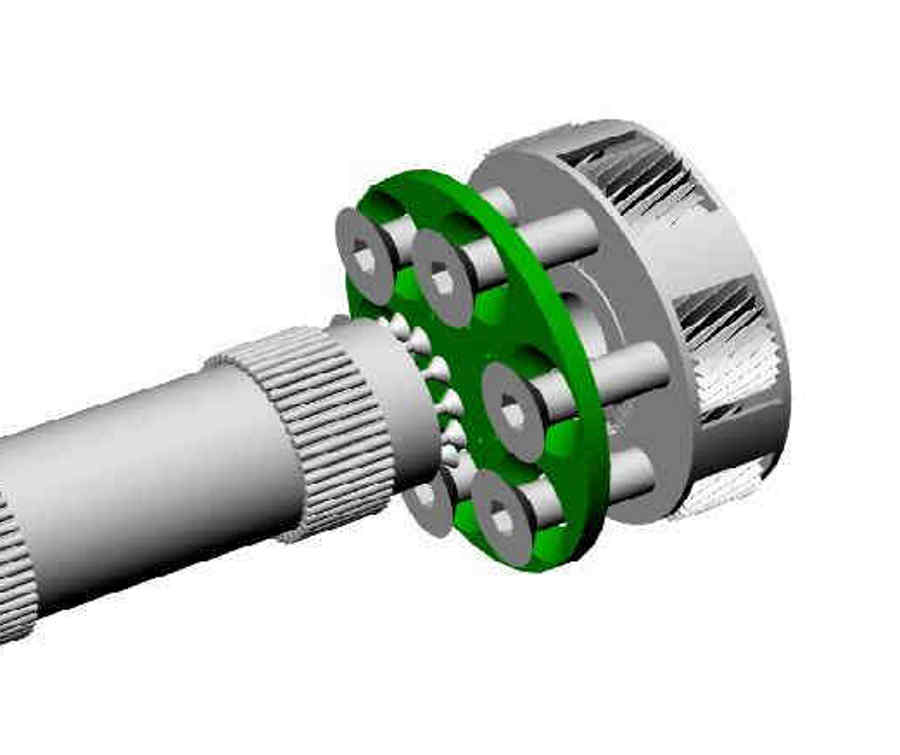
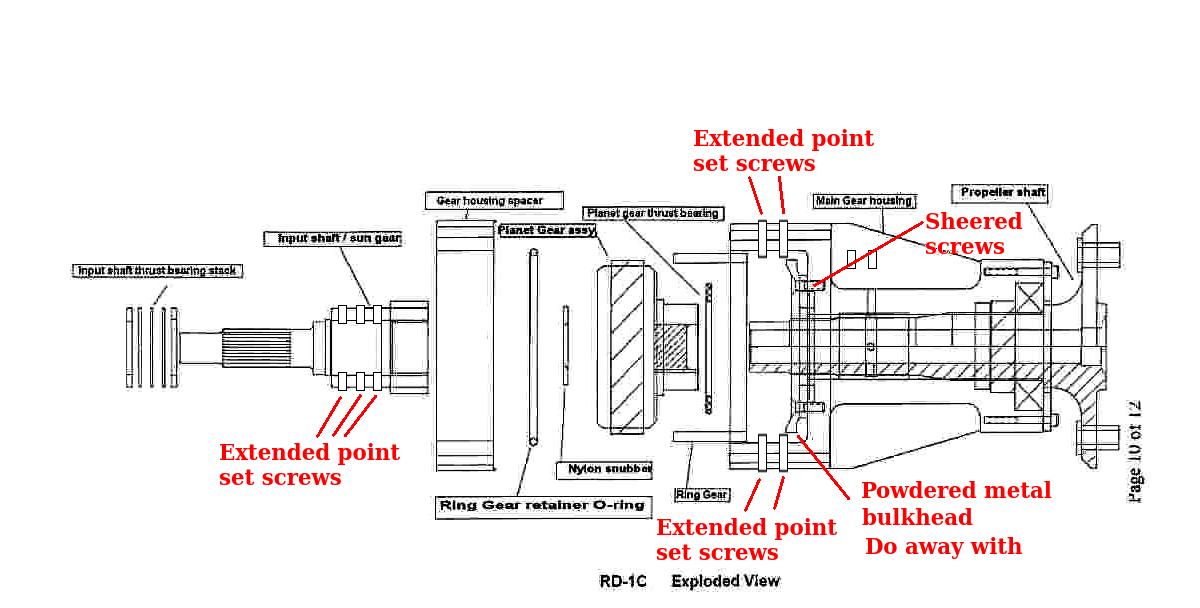
Looks like you pressed the planet carrier shafts out and sheared the
retaining roll pins. Surprisingly and apparently that works
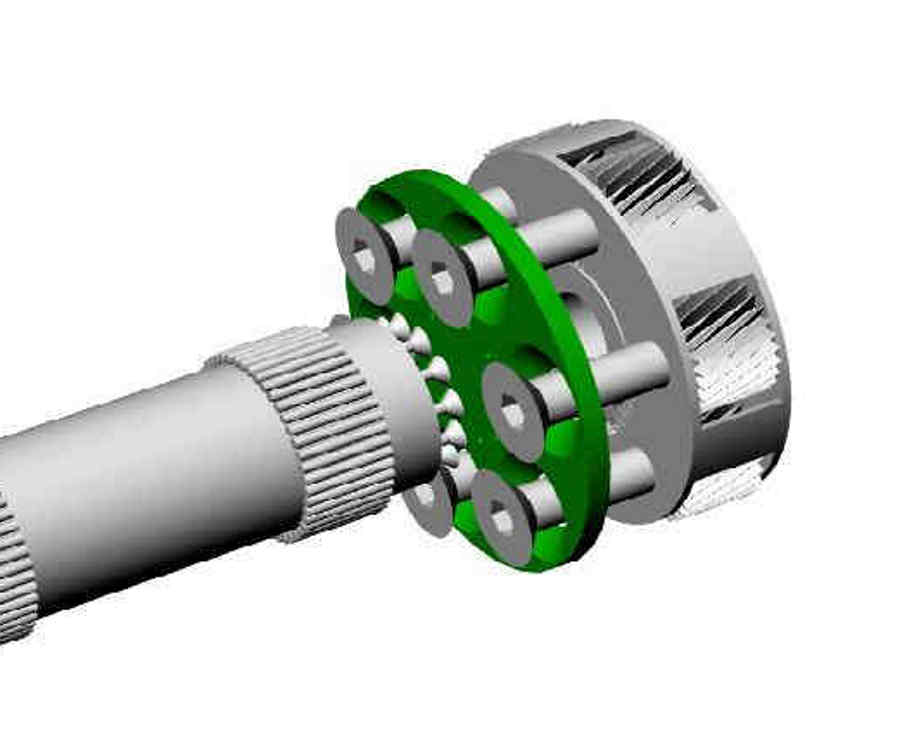
Looks like you are going to replace them with a hardened and ground
down sholder bolt.
Good Idea. That should cut the cost somewhat as there is no need to
EDM a hole in the planets shafts.
Paul Lamar
Paul
I am going to see a metal treatment cie at Boynton Beach tomorrow to
find out what hardness the shaft are in the mean time checking the
hardness on those bolt plus if need to be retreated for proper hardness.
the pins are easy to shear.
The cv shaft are machinable the only hard treatment is about 116" deep
where the ball bearing travel, I can grind it only at the location which
I do have to use the end mill to remove the excess of metal on indexing
table with the milling machine.
those bolts used as a shaft can be lock with pressure pins at the same
place or spot weld the exceeding treads sideway.
The prop flange you saw is only a dommy which I practice on the milling
for logs locations, a good one is already done with 58"dia lugs.
It is very cheap on Ebay the flange about $32 and the cv shaft $60 plus
$100 for bearings and seal ,the shaft can be used with center holes 316"
for constant speed prop and true the copper sleeve.
JEAN PRUDHOMME
Won't hurt but the spec for needle bearings shaft hardness and finish
is in the the bearing catalogs.
Rockwell C 58 is the required hardness and the shaft finish is 15 RMS
maximum.
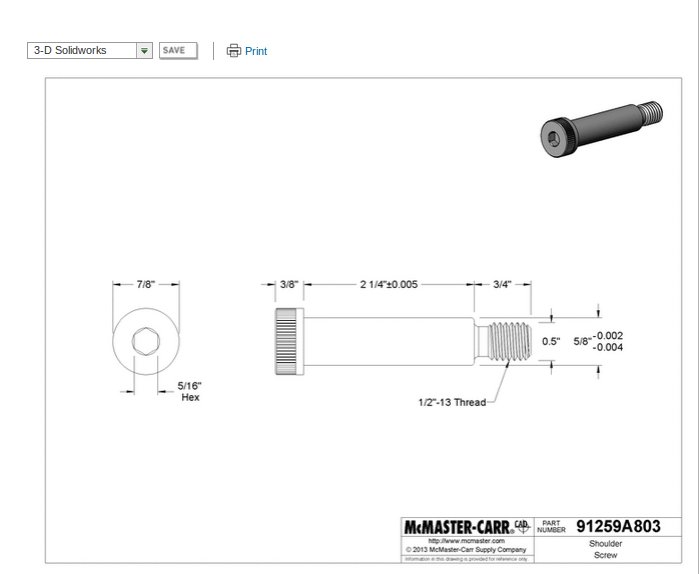
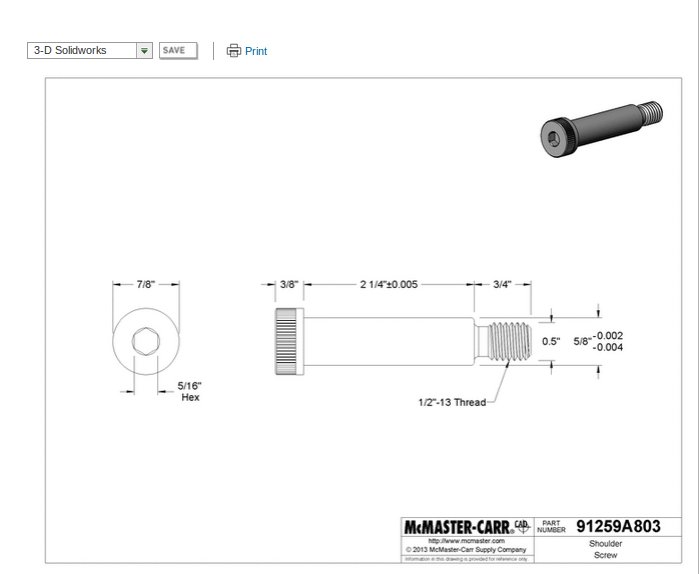
I will have the 5/8th dia. shoulder bolts ground down to 15.5 mm for
the 3.12:1 Ford rear planet
carrier. They may already be hard enough however it is wise to check.
Paul Lamar
Paul
I made a research and talk to the manufacturer regarding the hardness
and alloy steel number and this all information I get, they mention
the bolts been use as bearing pin.
Now I can see the treating company with all this
infos to increase the hardness to 52 c
JEAN PRUDHOMME
I think this is the wrong diameter.
As I recall the 2.85:1 shaft is 13.5 mm
Paul Lamar
Paul
There more information which it prove the real harness treatment for
those shoulder
bolts see mark at 12.9 as treatment certification , it can be use as it is
JEAN PRUDHOMME
The surface finish on the shaft is important as well as the hardness.
Paul Lamar
Paul
I did removed lot of weight on the shaft by grinding the inside and
after completed with retaining plate I still to be remove some material.
I weight the shaft i made before with both side splines with planet cage
and the Durango shaft and came up at 6.5 pounds but I have to add those
6 gears and shaft less and holding plate more metal to be remove again,
I guessing it will weight about 2 pounds more.
Paul I need the outside diameter of the Tracy casting and bolts holes
circle and size, I found a pce of
8"dia by 8" long 6160 alum bar and I want to know if it will fit with
Tracy hole and out side dia pattern before I buy it.
JEAN PRUDHOMME
Nice grinding trick.
The tricky parts of mechanical design are always getting the weight and
cost down.
Paul Lamar
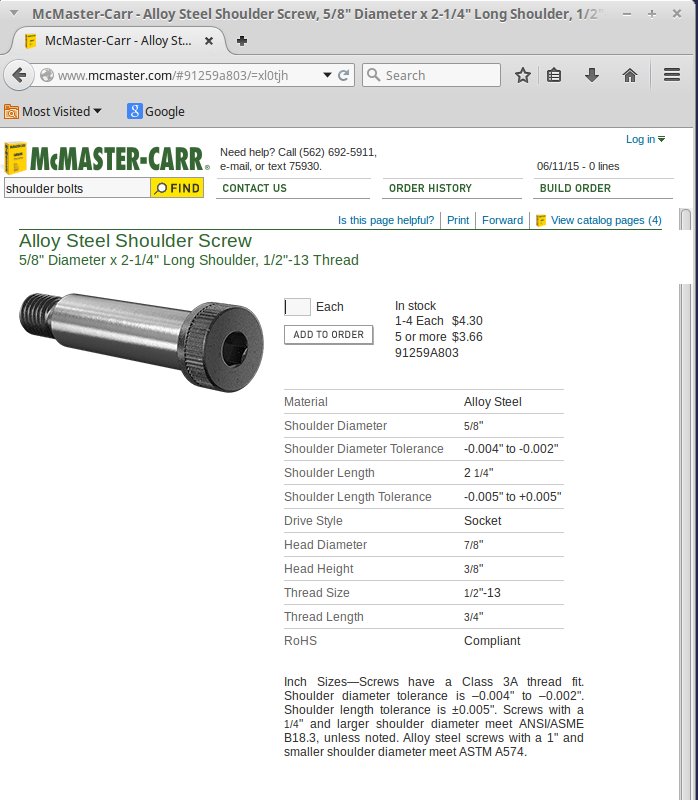
I did a little R&D on the planet shaft cost situation.
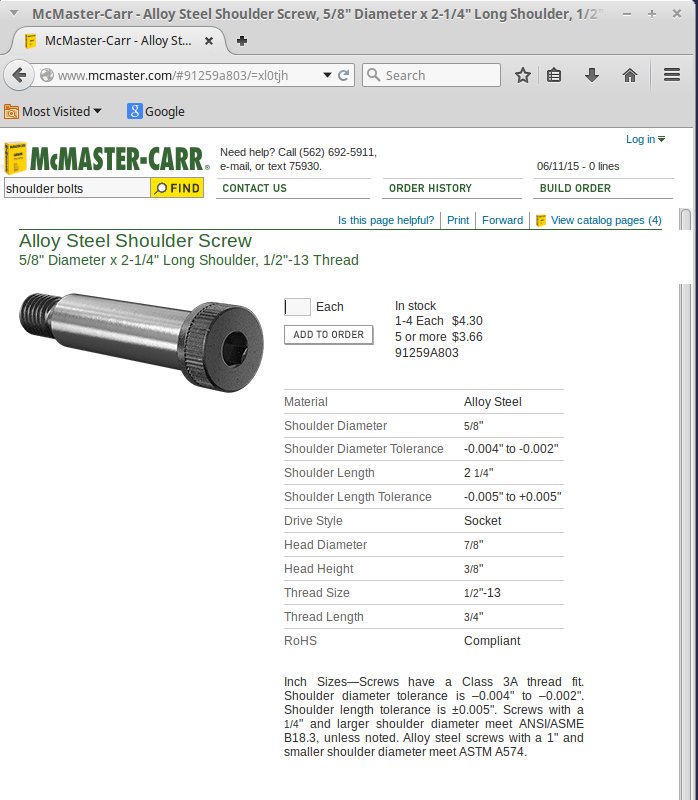
McMaster Carr Has 5/8th inch diameter shoulder bolts 2.25 inches long
for $3.66 each high strength alloy steel. Not hard enough however.
If I have 60 at a time centerless
ground to 15.5 mm and a super smooth finish the cost is about a buck
and a half for each bolt. Lets say batch heat treating to bring them up
to C57 would
be at the most a couple more bucks. Lets say $7 USD for each bolt. Say
$40 dollars
total for 6 bolts. That beats $300 for EDMing a hole in each planet shaft.
Paul Lamar
The Rotary Engine News Letter. Powered by Linux.
ACRE NL web site.
http://www.rotaryeng.net
You Tube
http://tinyurl.com/beqqxas
Store
http://www.rotarpower.com/#!
Copyright 1998-2015 All world wide rights reserved.