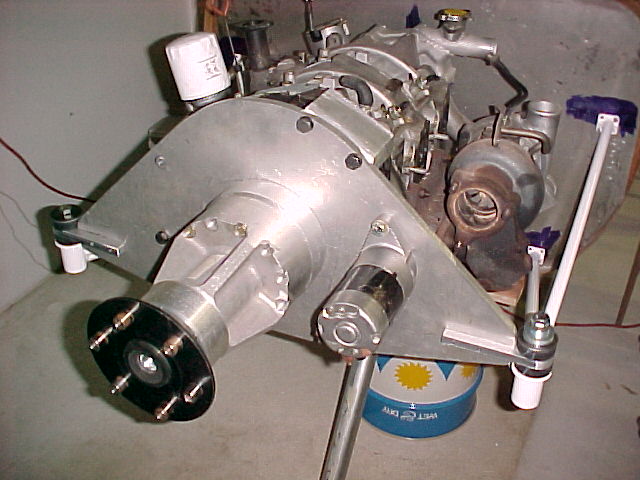
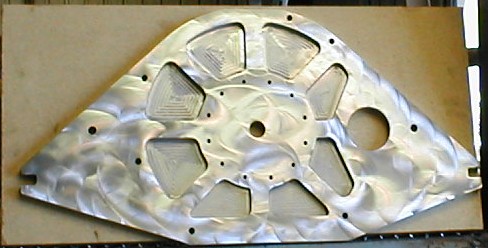
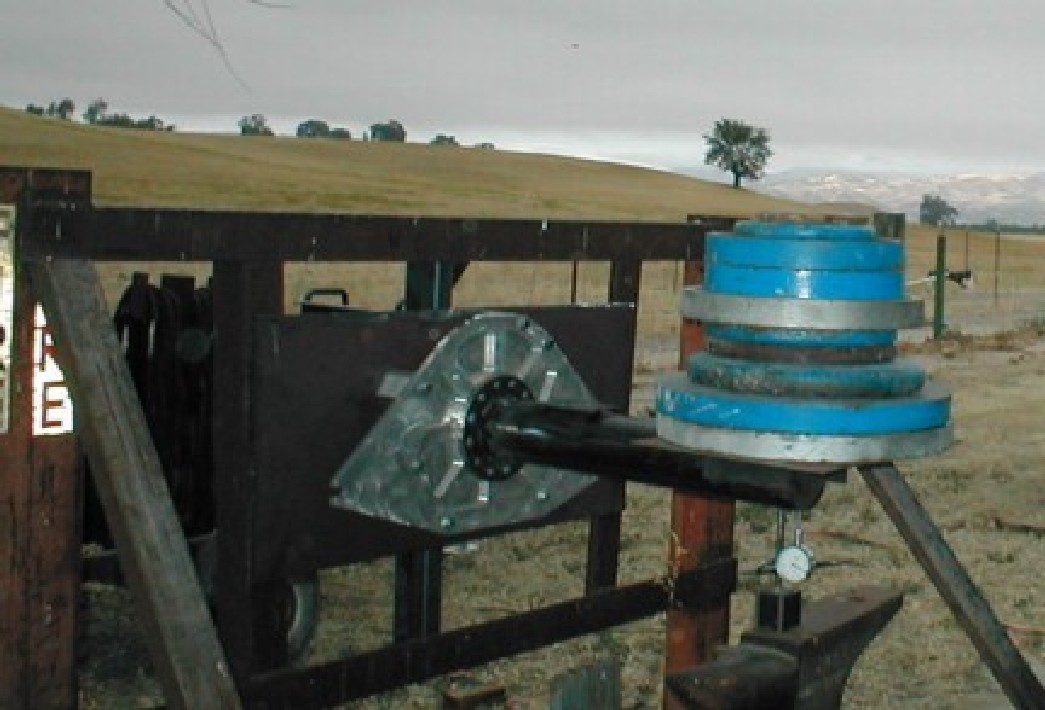
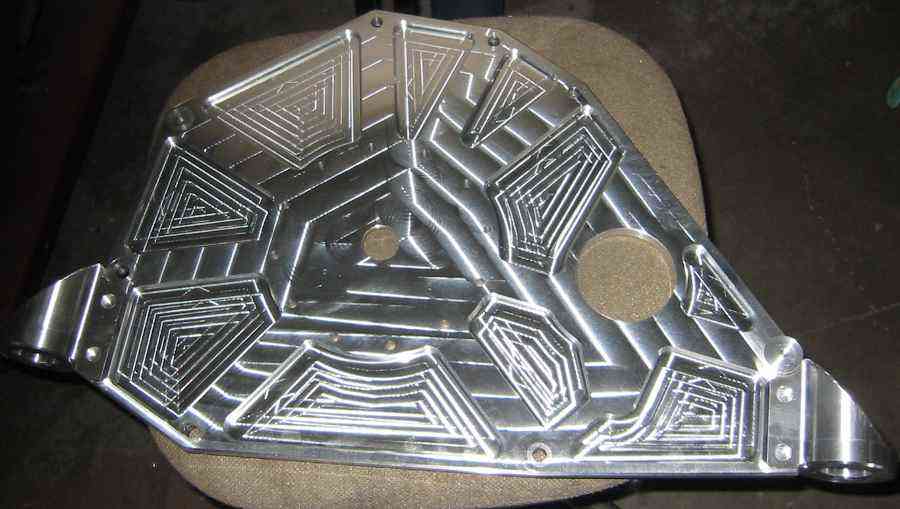
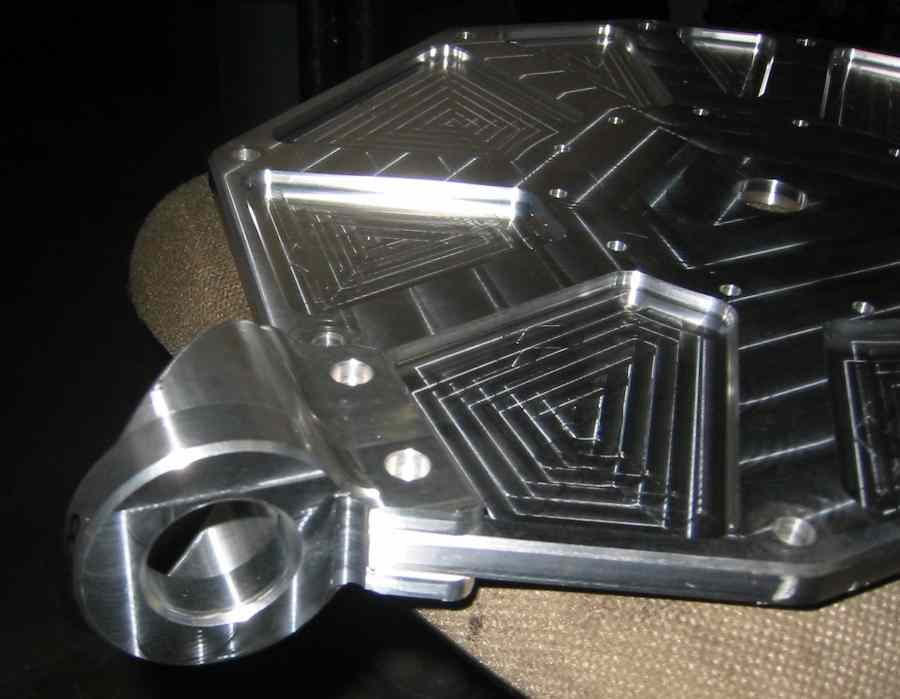
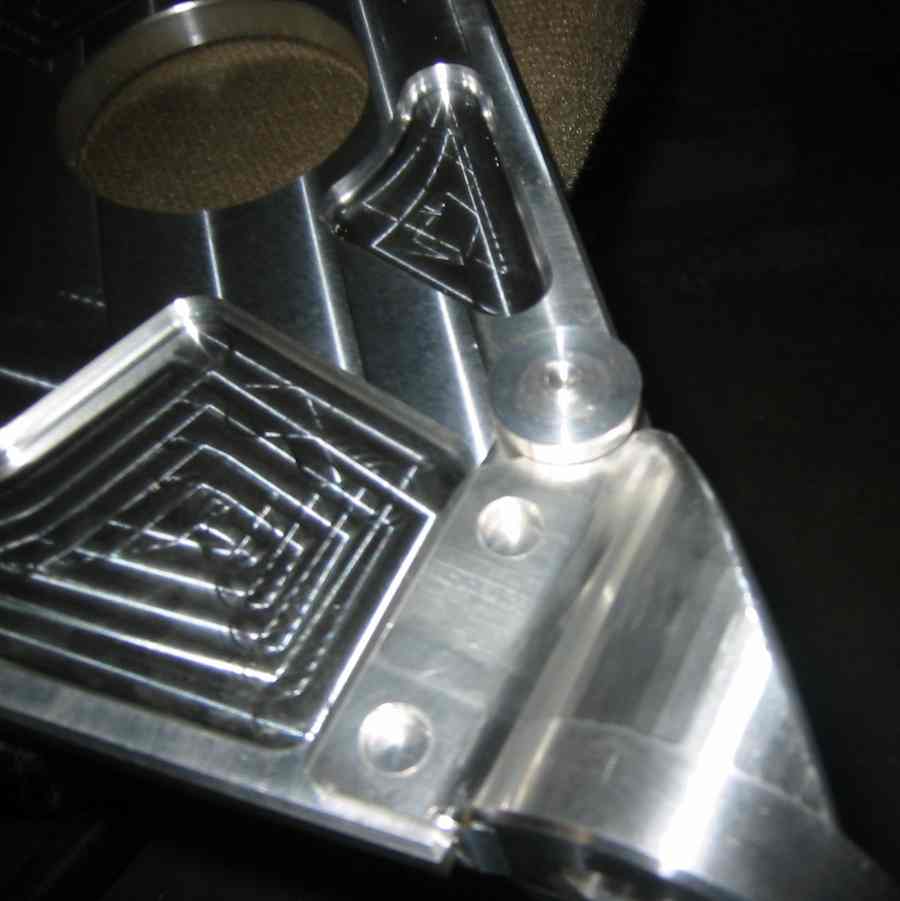
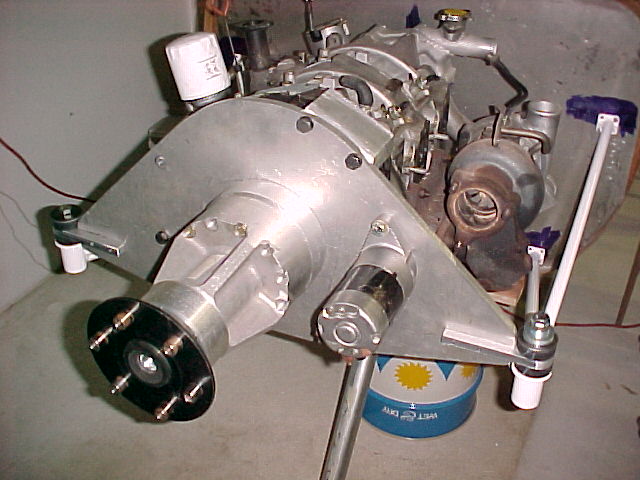
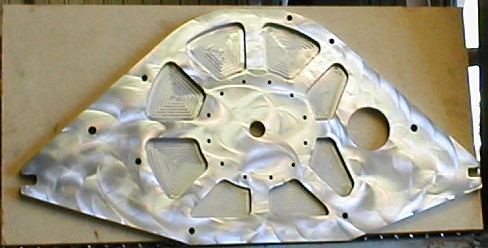
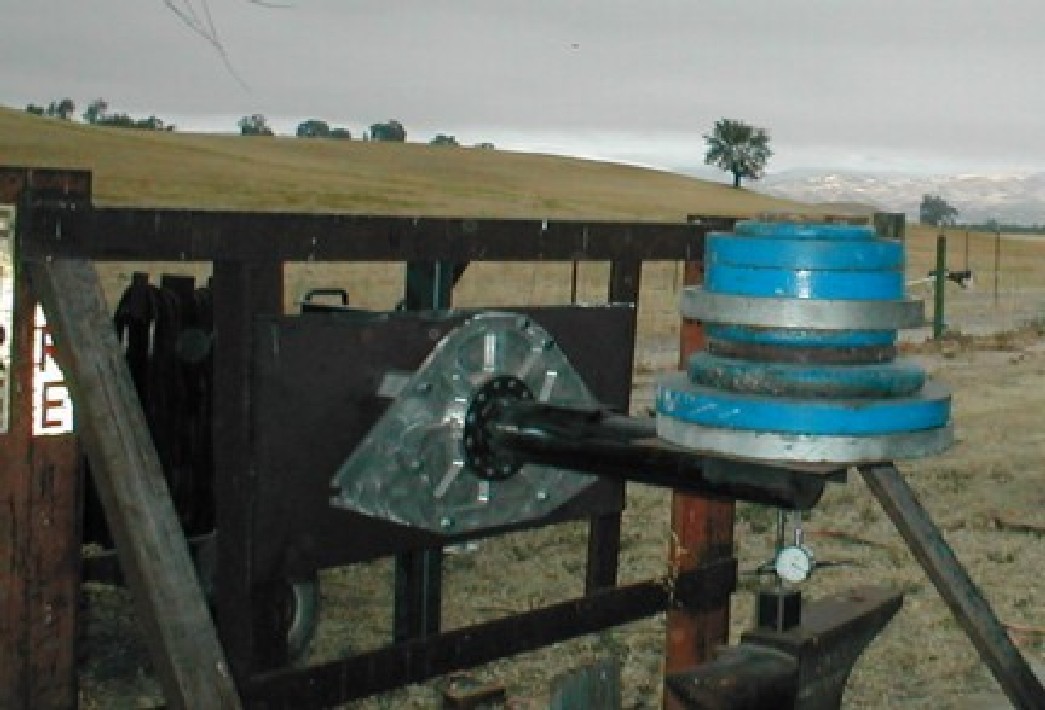
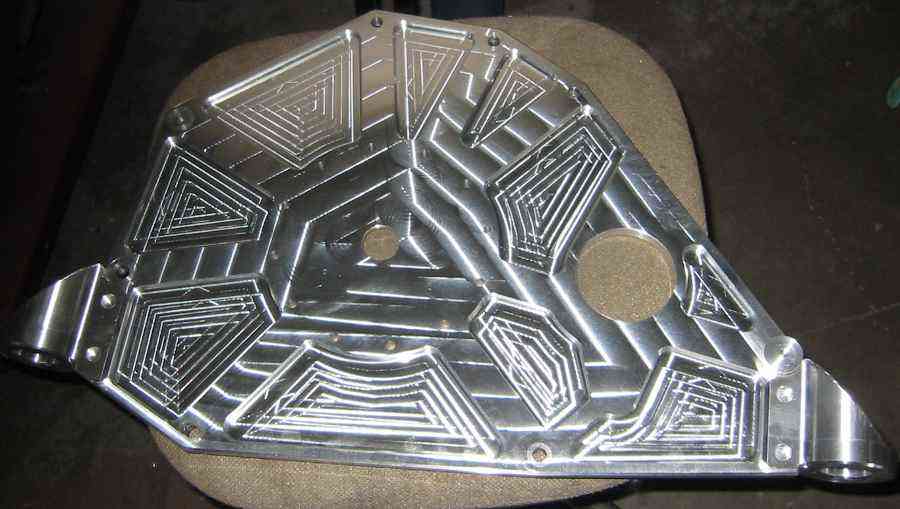
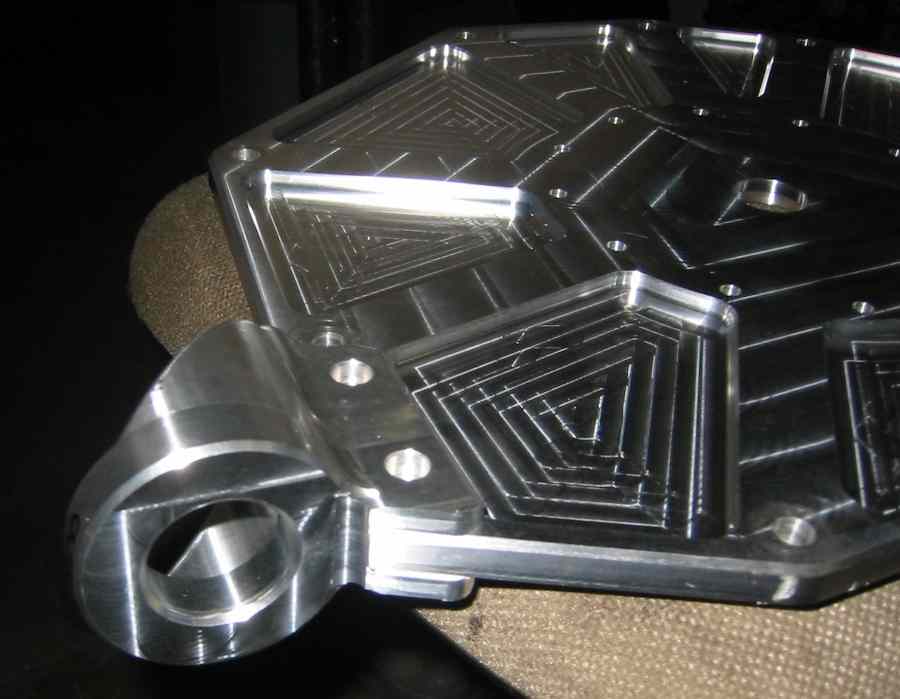
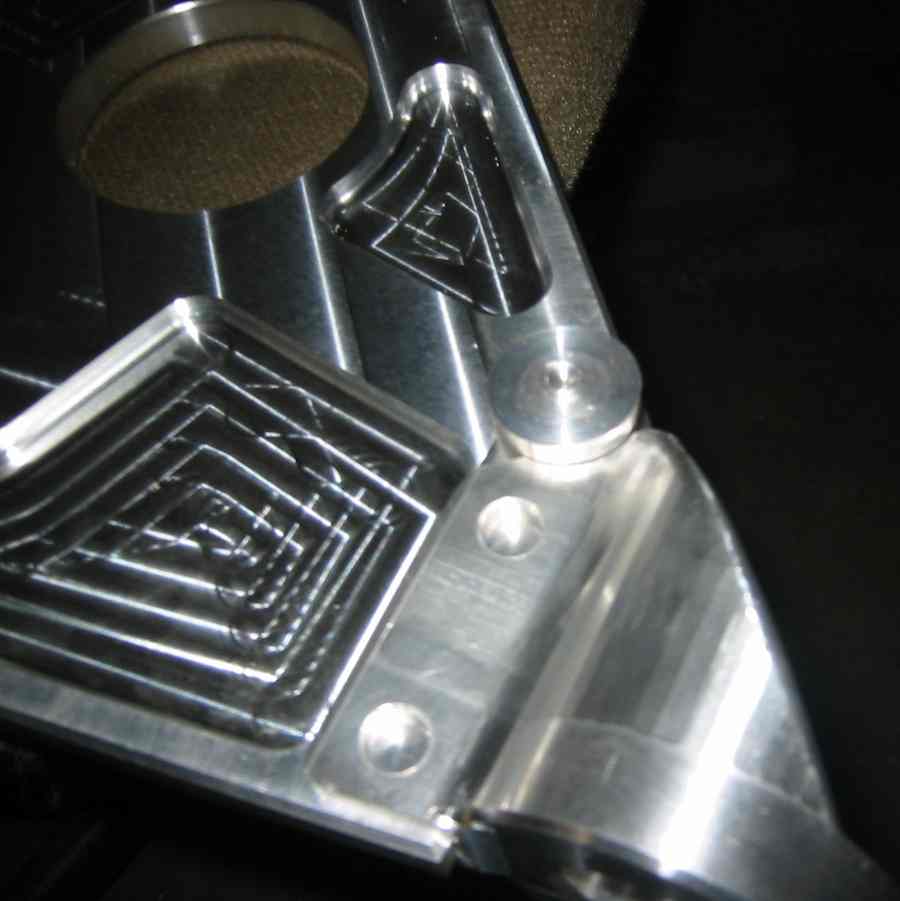
I spent a couple of hours this morning working on the new
prototype gear box housing. Here are some pictures.
I wore myself out operating that huge lathe. That takes a lot of
muscle to turn those big wheels.
I also discovered a new NC shop a mile or so from the airport.
The machines they have are the most fantastic huge NC machines
I have every seen out side of an NC show. The whole bed the part is
bolted to pivots.
They are almost large enough to walk around inside. The billet gear
box housing would be a piece of cake,
Amazing machines.
Paul Lamar
Hi Paul,
How big and how much $ for that piece of al that is in your lathe
right now.
Oh and what is the grade 6061? I might do mine the same way, saves
doing a pattern.
Cheers Chris.
6" dia by 11" long 60661 T6 $150 US including $15 cutting charge and
8.5% Cal tax.
50 pounds.
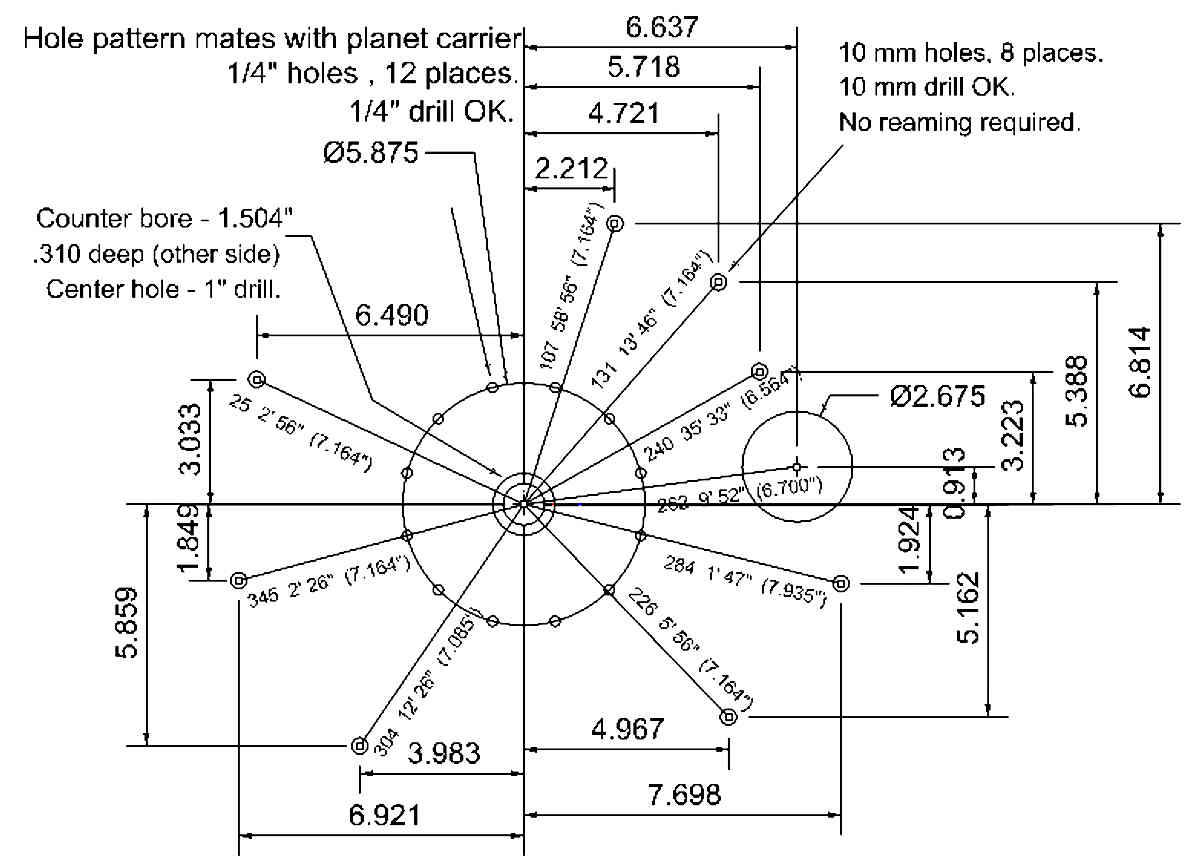
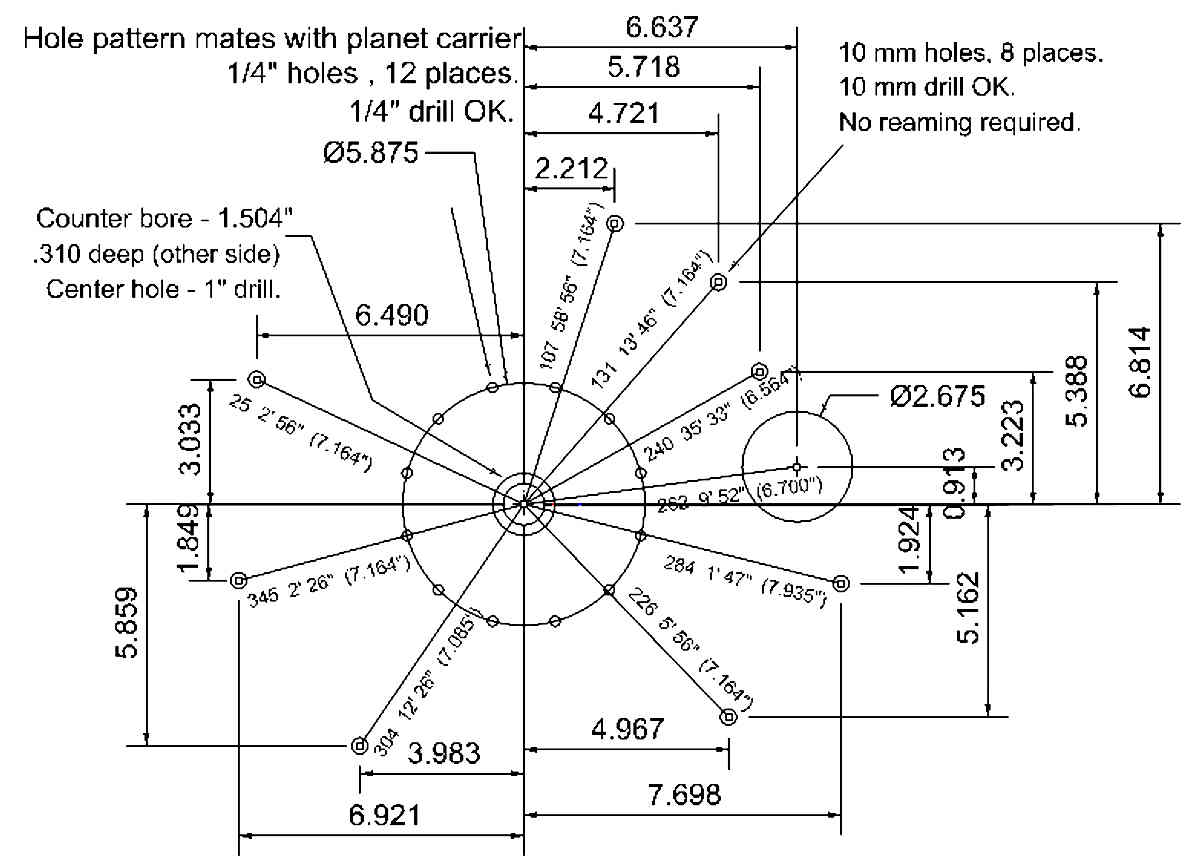
BTW Tracy's bolt circle dia. on the adapter plate is too large. It cost
a lot more
money for 6.25" diameter billet. I will drill a new slightly smaller
bolt circle
on my adapter plate. I think it should be 5.500" in diameter. His is 5.875".
He used a casting.
The ring gear is 5" OD so that gives us a 1/2 inch wall to work with.
Drilled head 1/4 " 20 course thread bolts can fasten the gear box to the
adapter
plate by drilling and taping the gear box housing. That's about 6 mm but I
don't think I can find them drilled or course thread in the US. You want
to use
course thread in taped aluminum.
Tracy used long 1/4 inch bolts about 10 inches long. Heavy and expensive
just drilling the holes :-)
Let me know if billet it is cheaper in Oz or NZ.
Paul Lamar
The Rotary Engine free News Letter. Powered by Linux. If you want off
the list PLEASE let me know and I will remove you. ACRE NL web
site.
http://www.rotaryeng.net You Tube
http://tinyurl.com/beqqxas
Copyright 1998-2016 All world wide rights reserved.