I have a friend that has owned a machine shop for decades.
He told me every lathe must have a 4 jaw chuck. Four jaw chucks are
a pain in the ass to center but 3 jaws have almost inevitable run out
of a least 2 thousands of an inch. I am working on a prototype
gear box and 2 thousands run out is unacceptable.
My 1977 CC lathe is still in good shape but so far I have been unsuccessful
in finding another chuck backing plate for it. None of the more modern
standard backing plates
fit. I don't have the money to pay a machine shop to machine a low
tolerance
new steel backing plate. The intention was to grind another backing
plate for the 3 jaw with a tool post grinder on the CC lathe to get the
run out to zero.
With a 4 jaw in theory one can adjust the run out to zero.
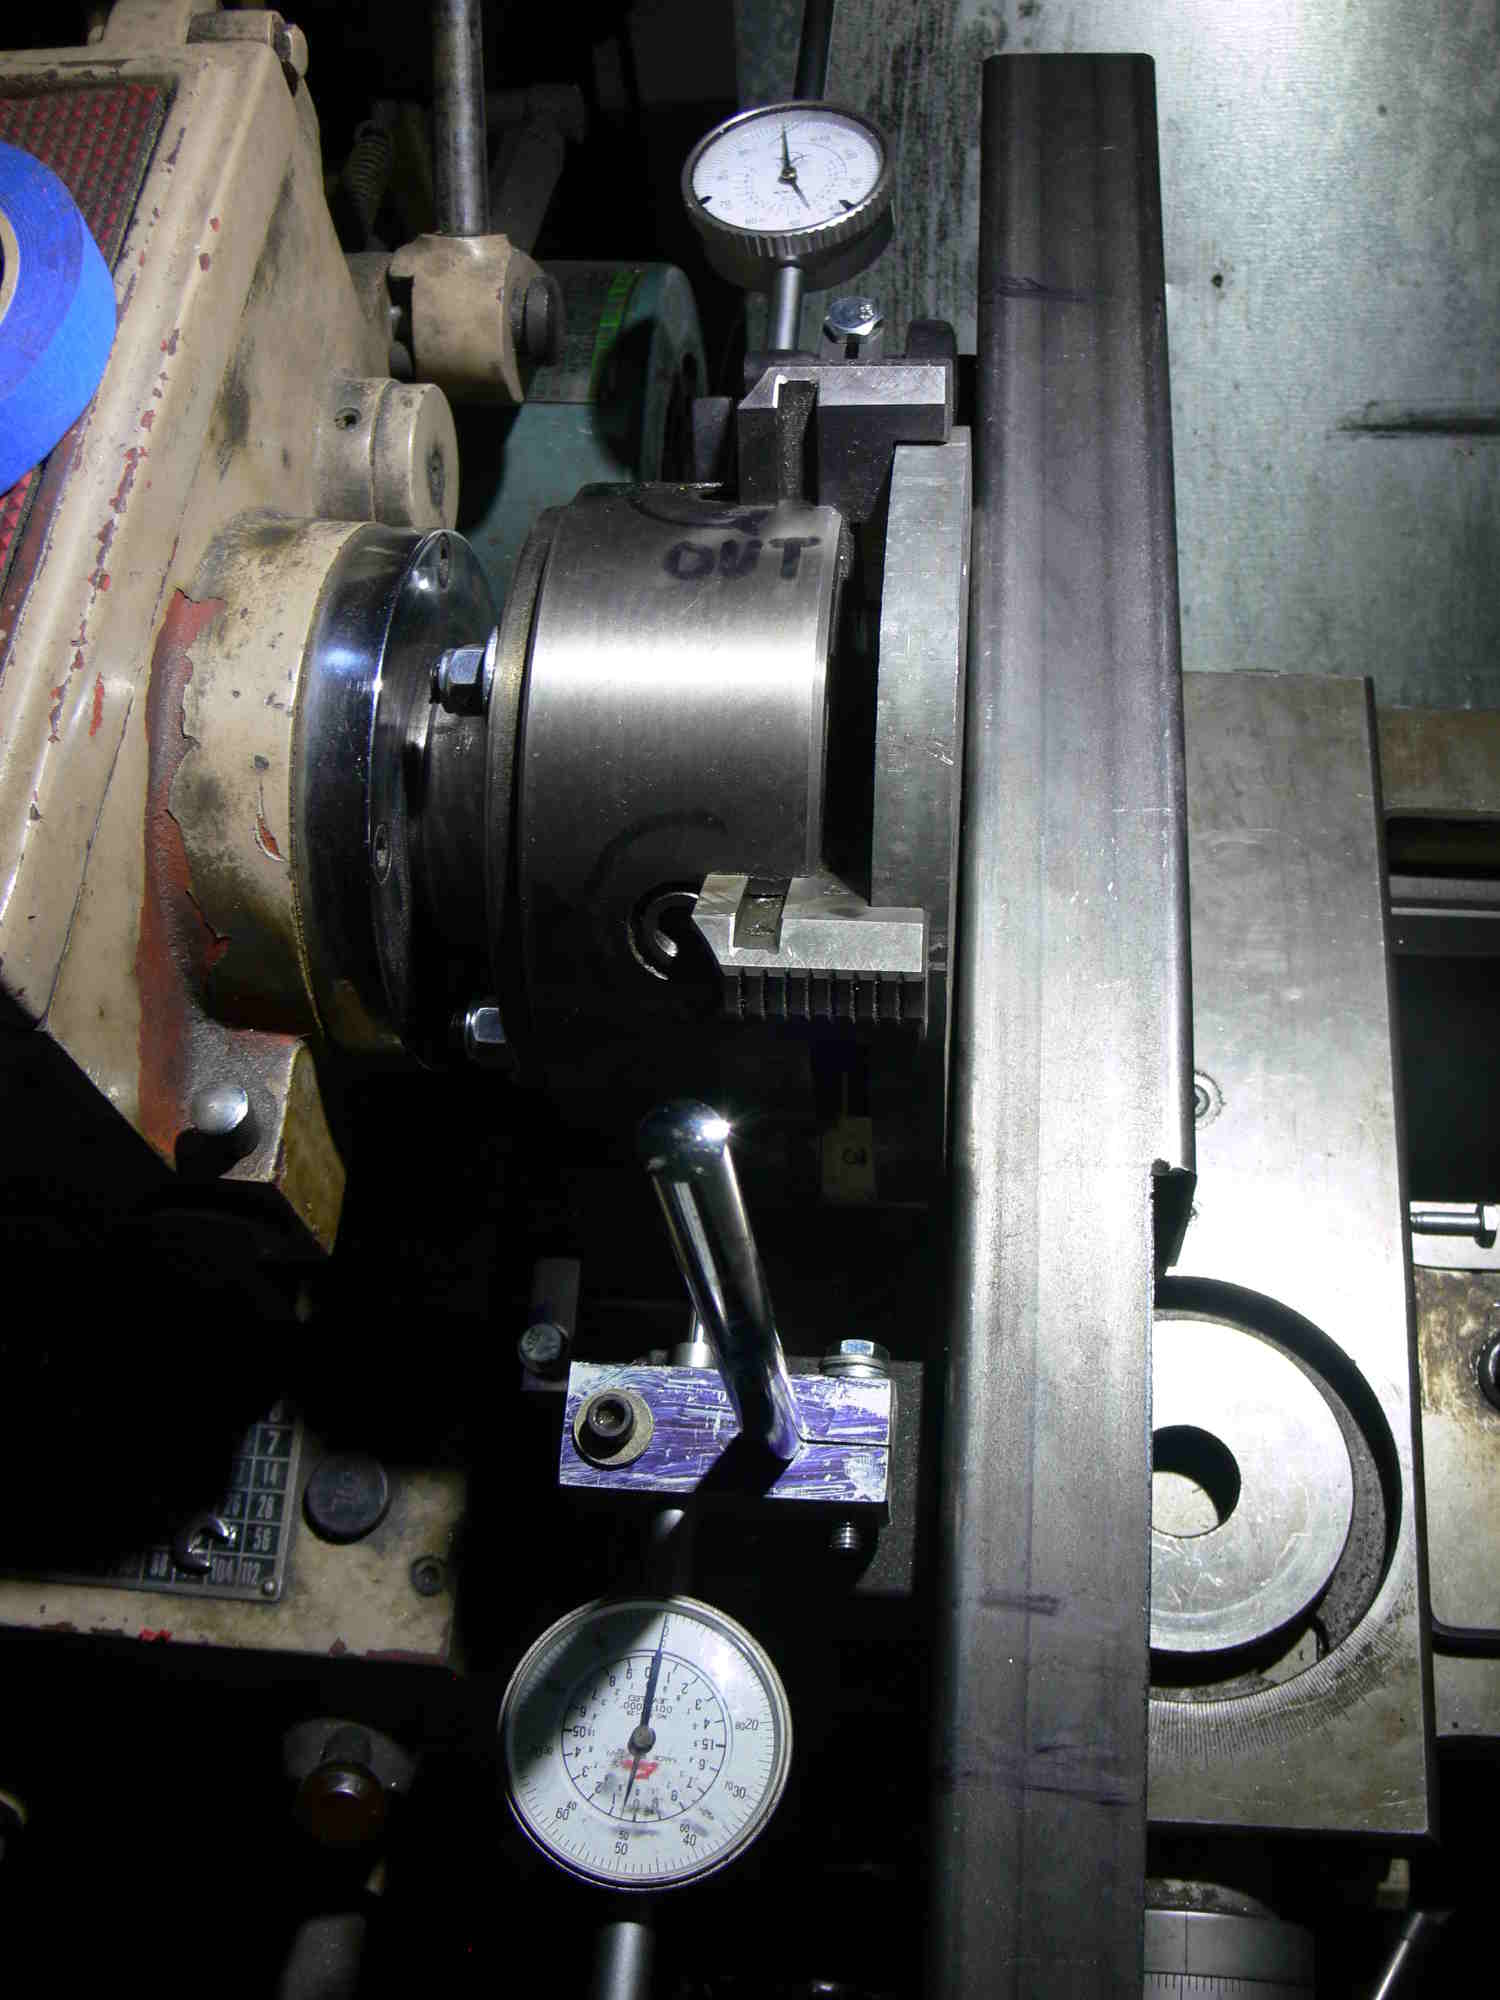
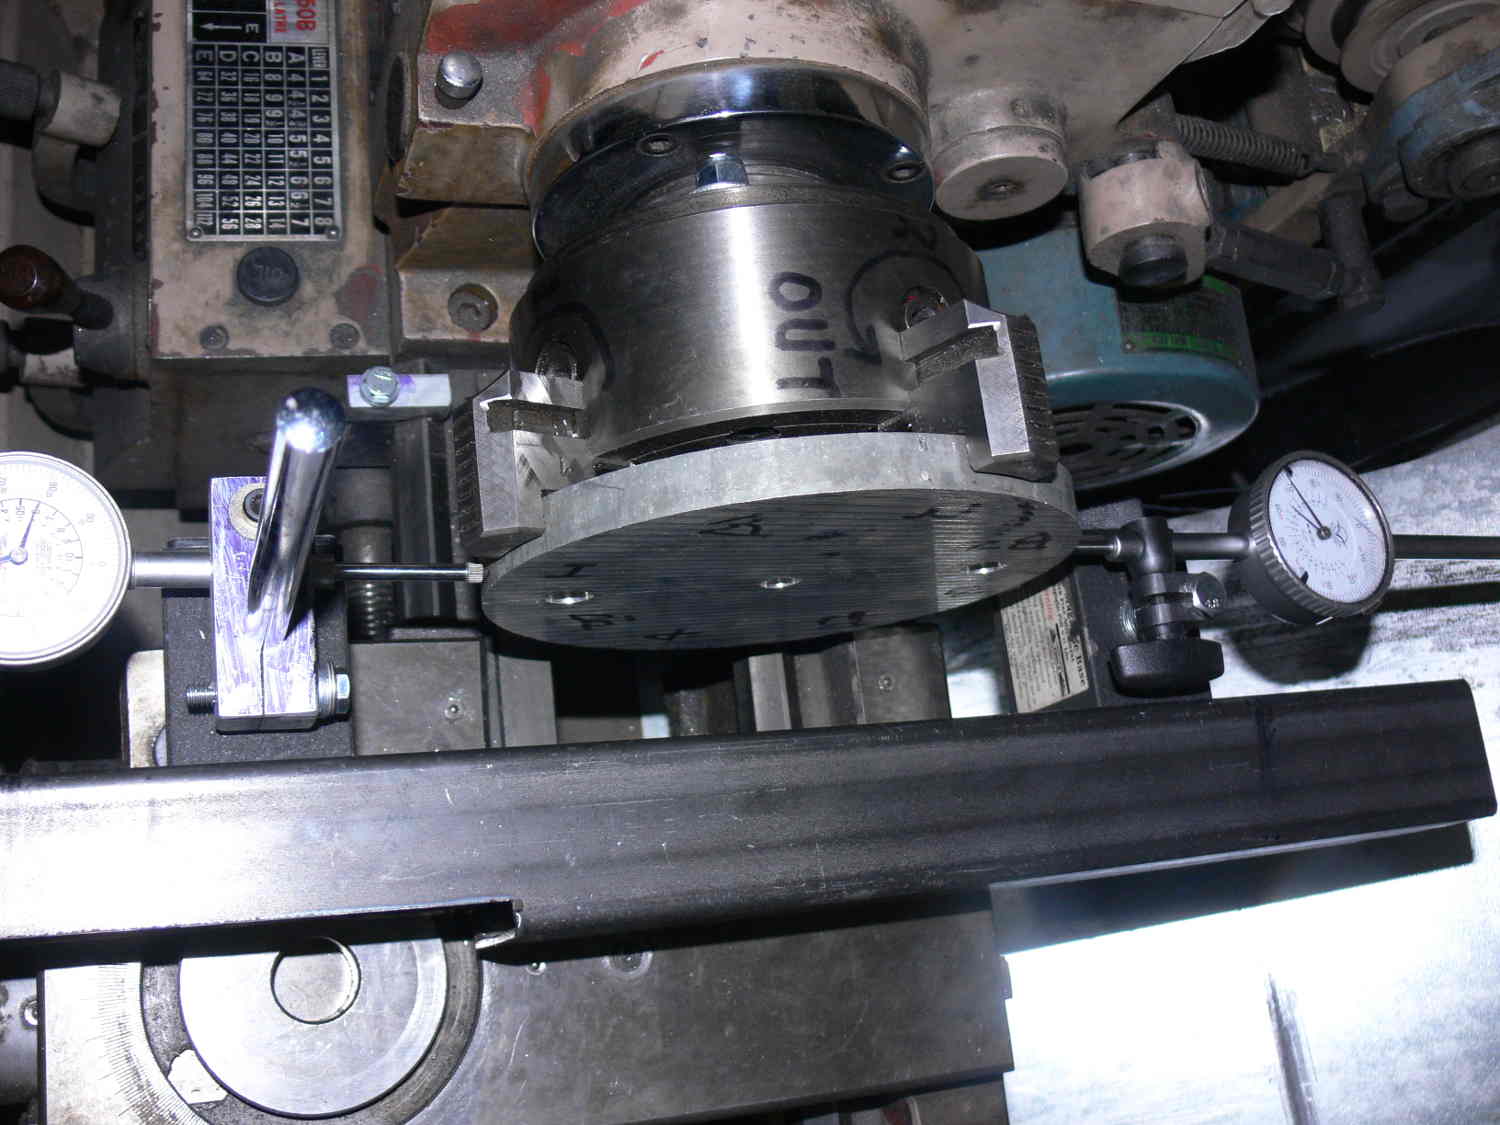
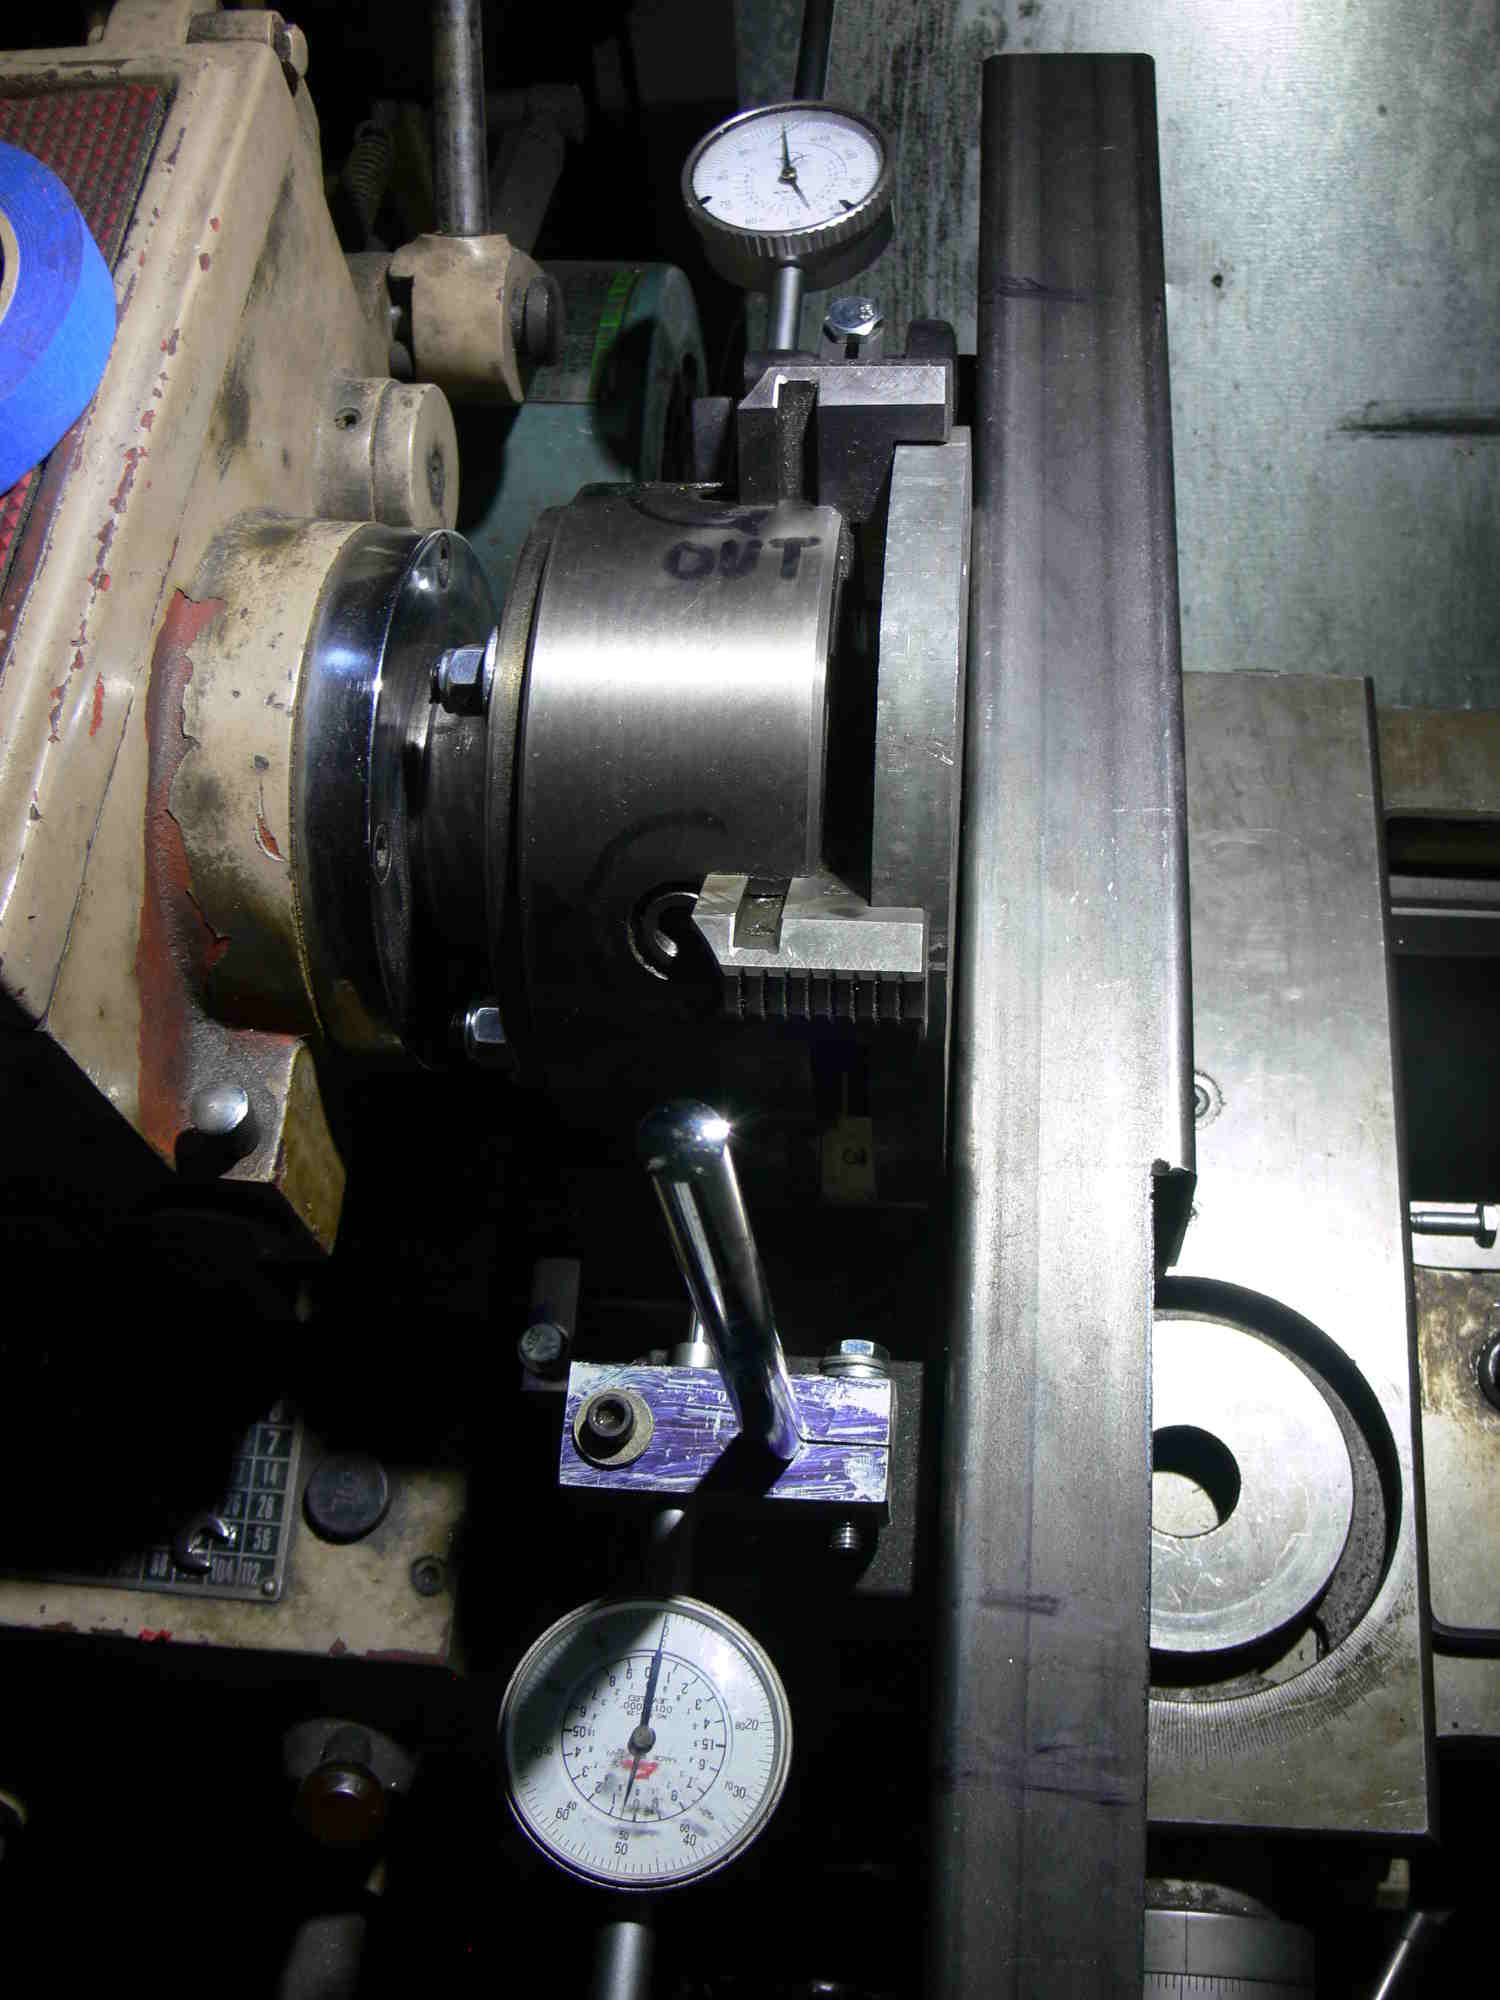
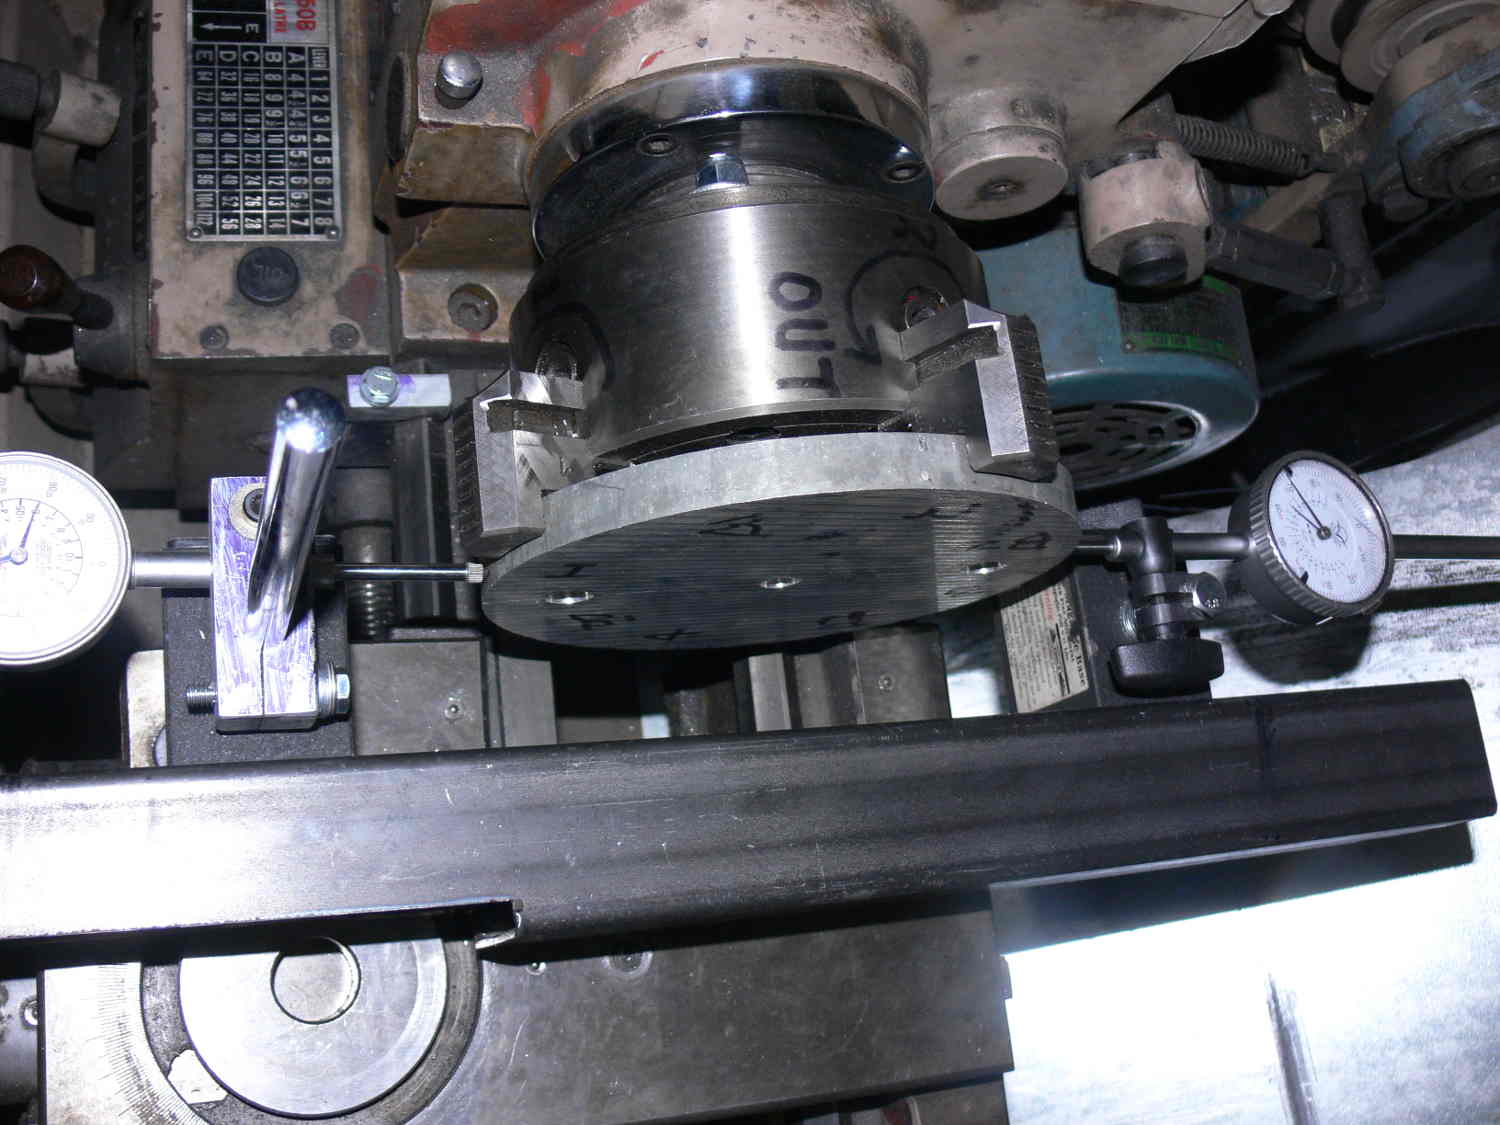
I came up with a plan to hopefully make it easier to adjust 4 jaws.
It is just a start as it assumes the 4 jaw body does not run out
as well. That is probably not the case. The last few thousandths must
be taken out with the old methods. There are many shown on YouTube.
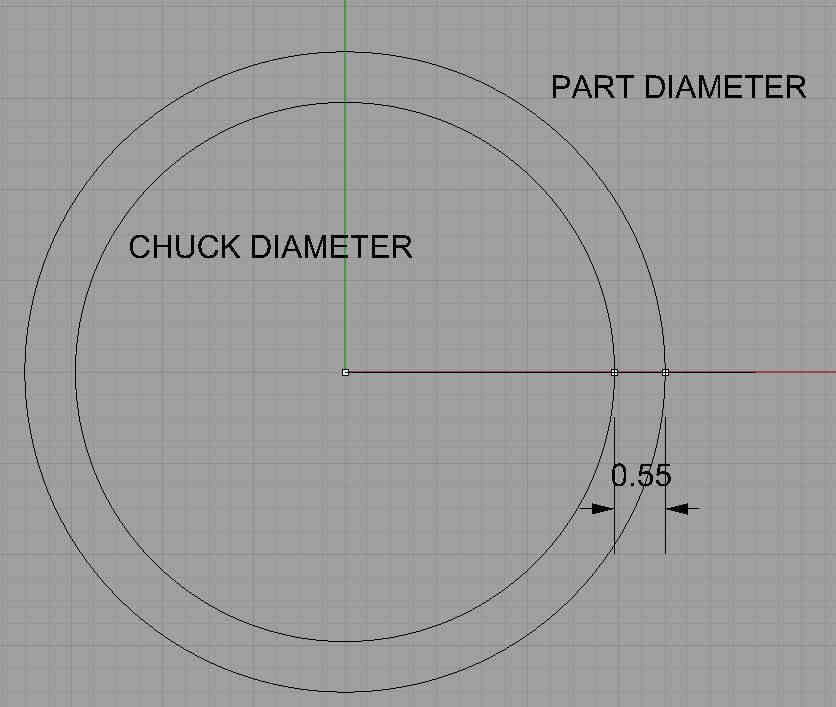
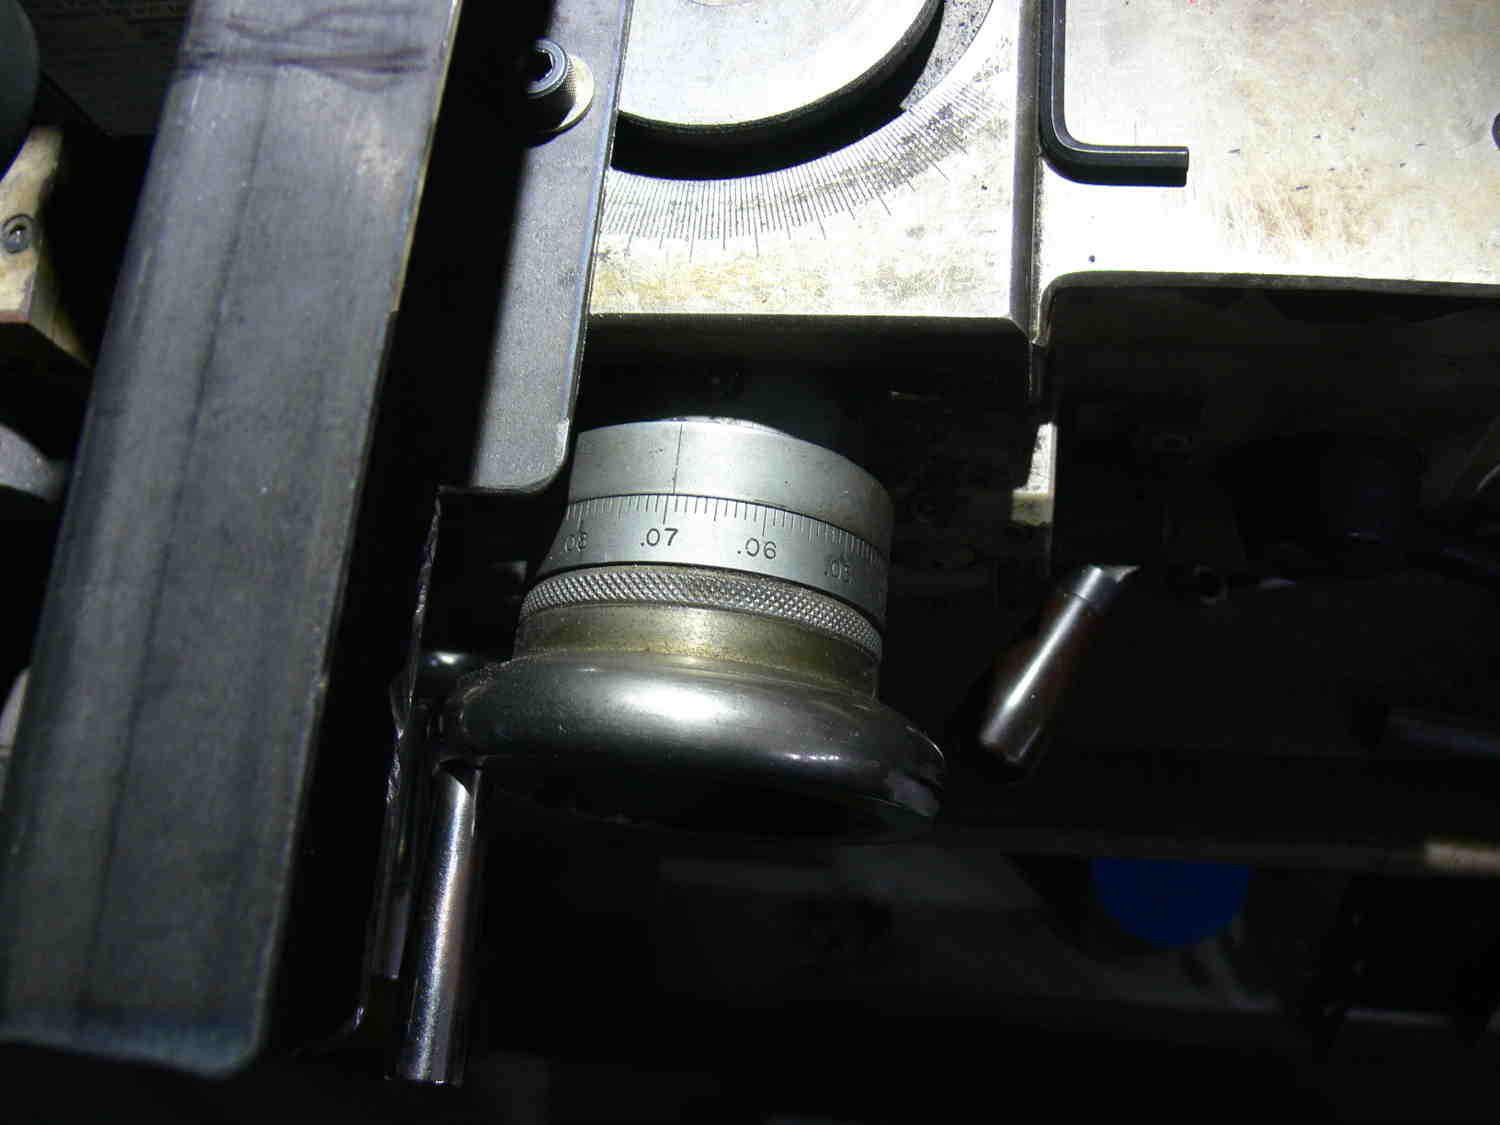
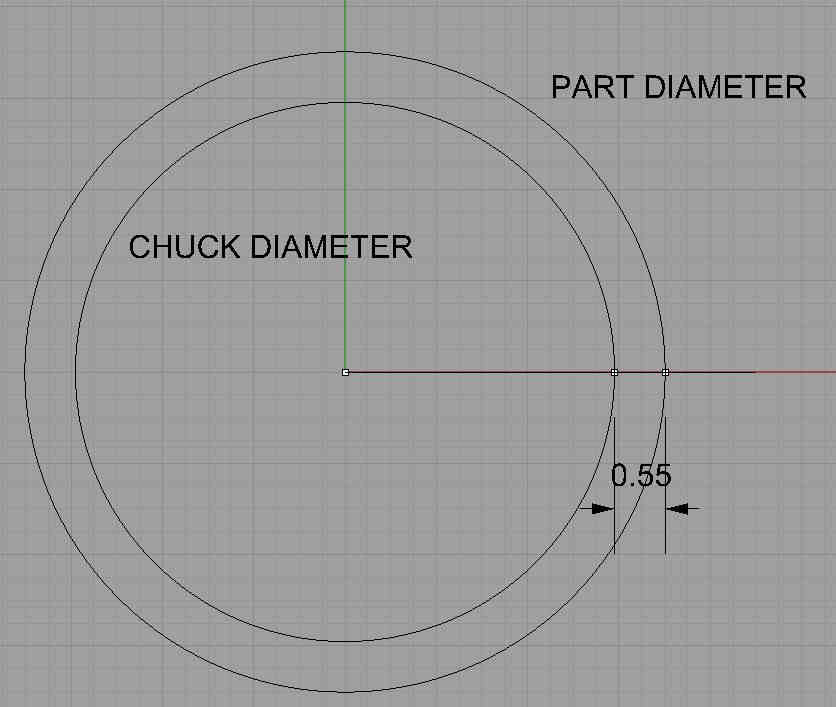
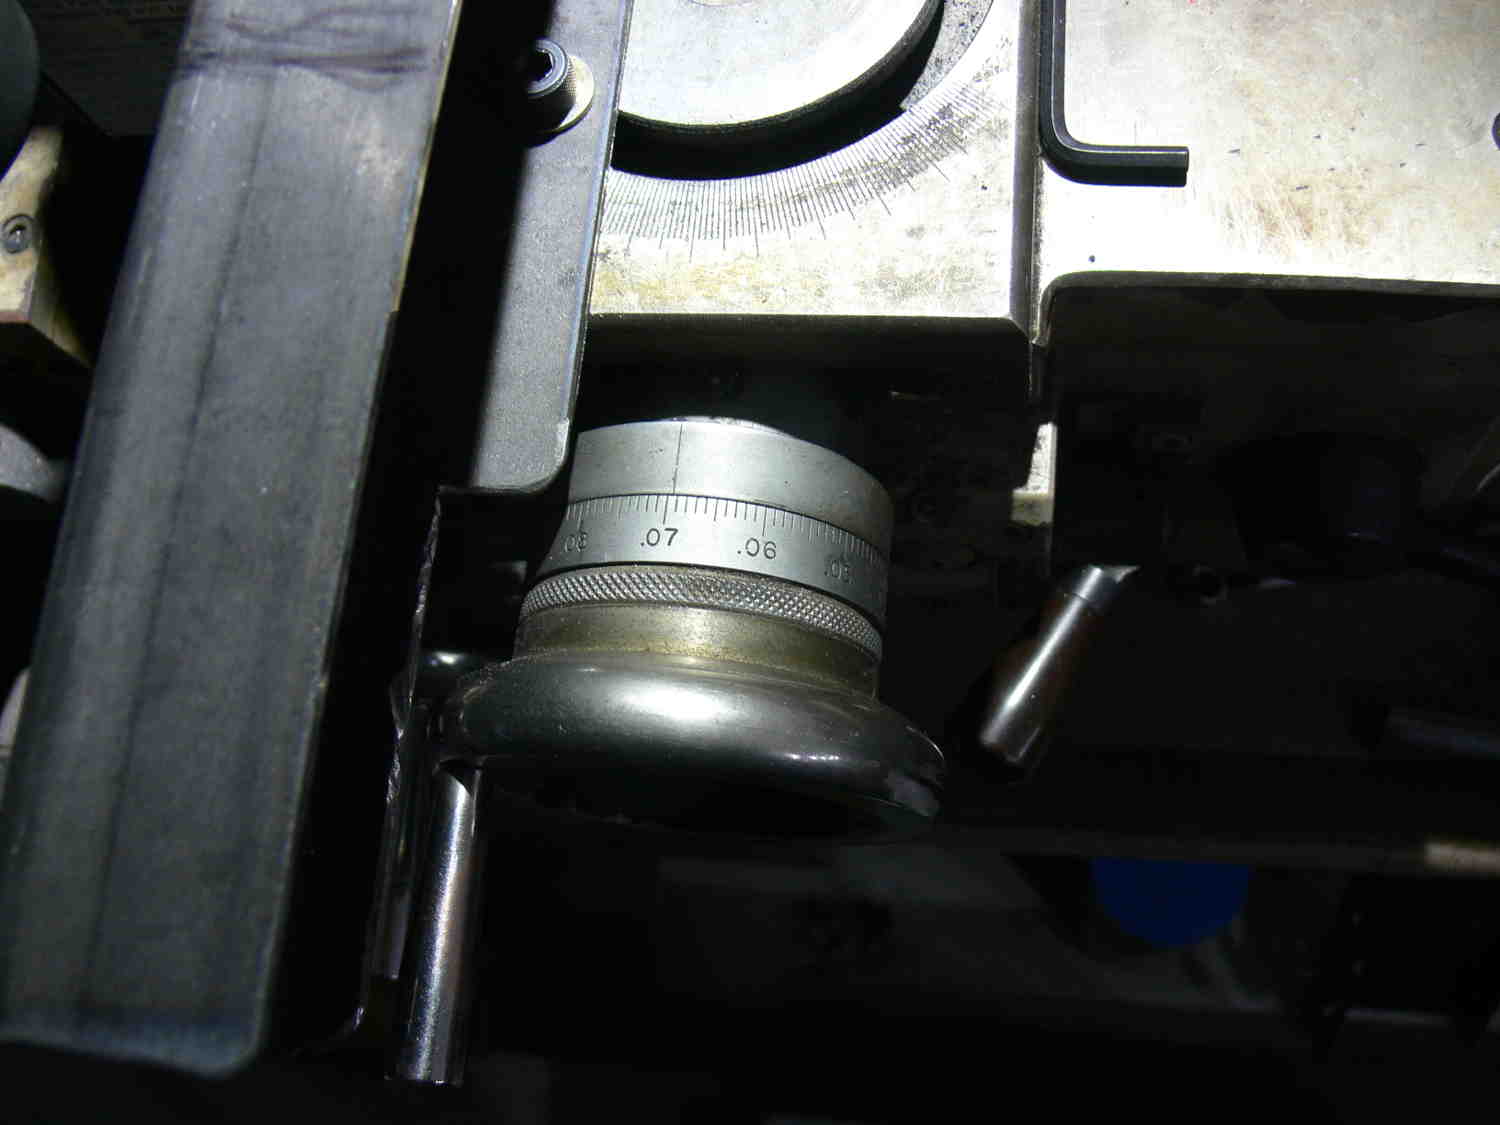
The trick is to center and zero the dial indicators on the 4 jaw body,
lock the
cross slide and then add and subtract the part radius difference to the
dial indicator
part readings.
Paul Lamar
The Rotary Engine free News Letter. Powered by Linux. If you want off
the list PLEASE let me know and I will remove you. ACRE NL web
site.
http://www.rotaryeng.net You Tube
http://tinyurl.com/beqqxas
Copyright 1998-2016 All world wide rights reserved.