Actually the second. If I had a million dollars I would hire a full time
patent attorney and file.
I have an old CC lathe built in 1977 and the 3 jaw runs out about .002.
Unacceptable
for gear box work. What is worse is adjusting a 4 jaw to zero the run out.
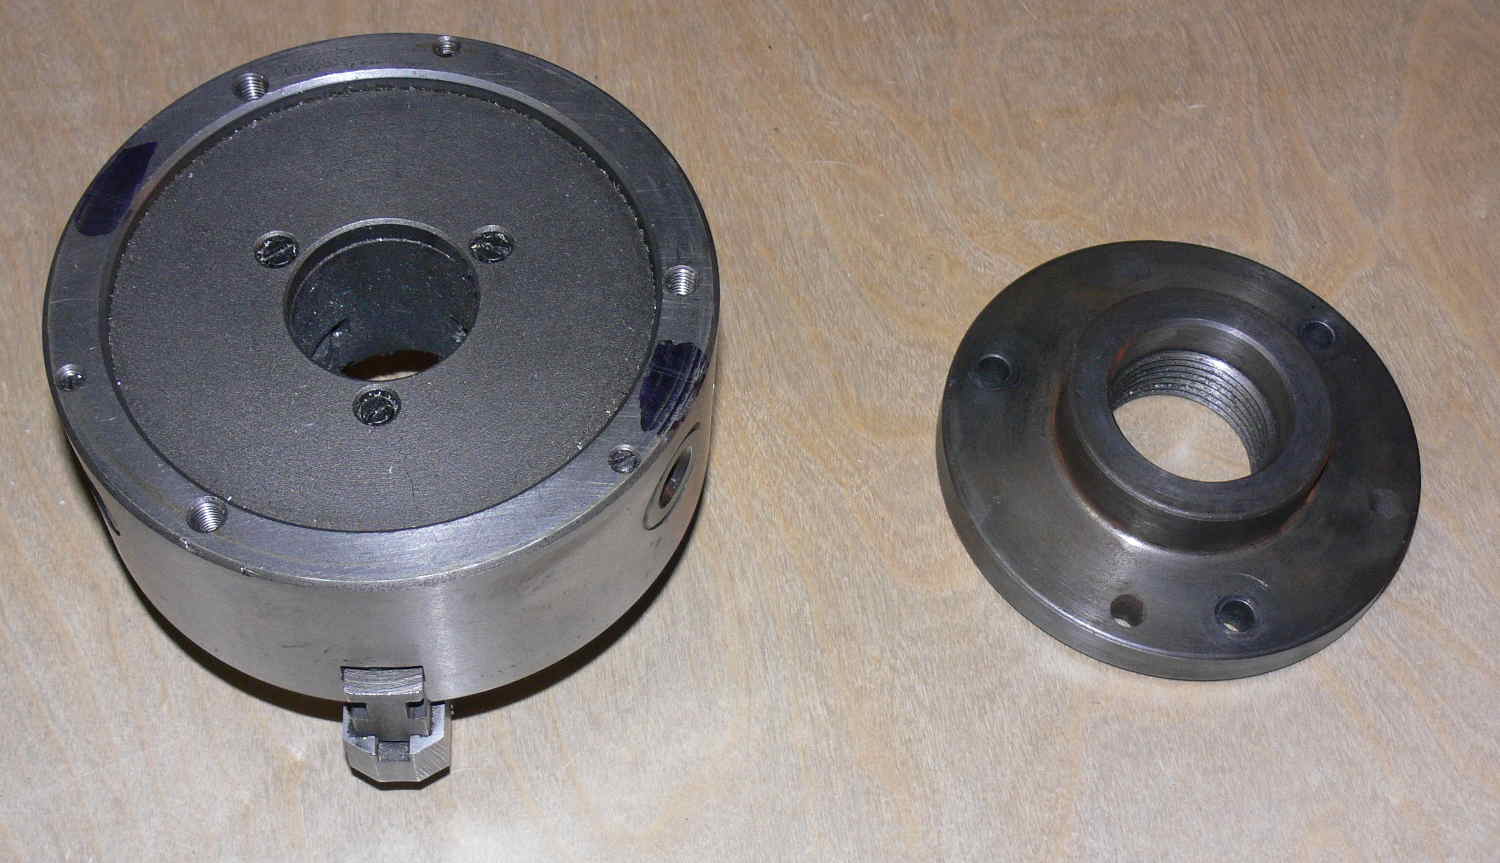
So I combined some of the features of the 4 jaw and the 3 jaw.
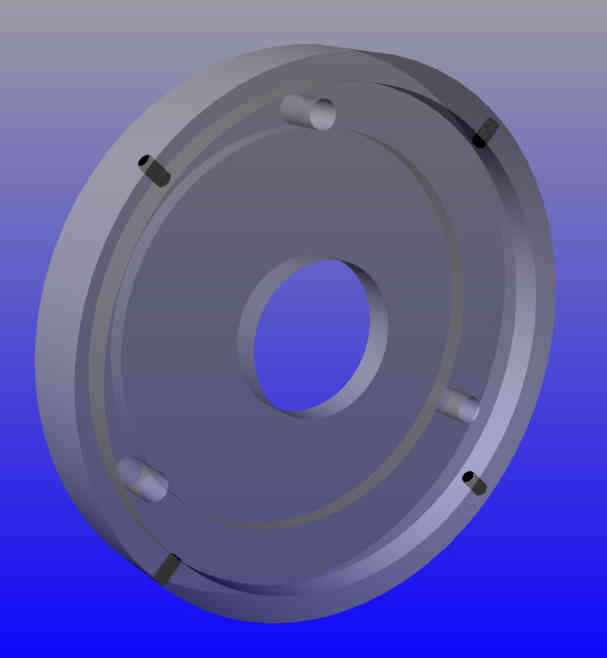
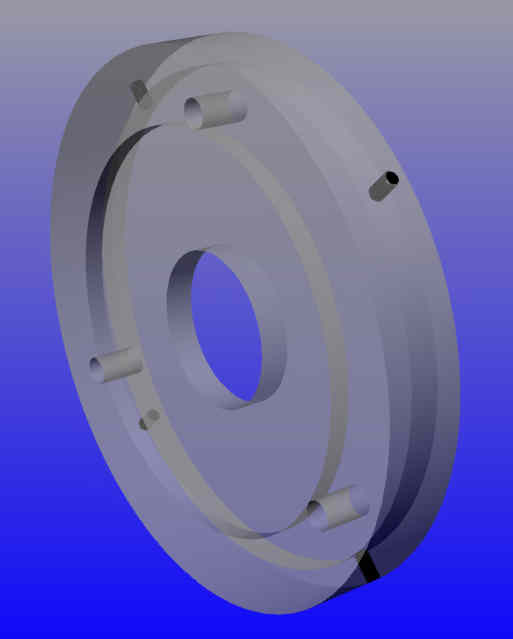
This is an adjustable backing plate adapter.
Besides that the locating bore in the back of the 3 jaw was not even round.
This is located on the OD of the chuck which in this case 6.25 inches
roughly.
Probably metric. It matters not if the OD of the chuck runs out as well.
Once it is locked down you have a super accurate 3 jaw.
There are four 10-32 set screws that do the adjusting then the chuck is
locked
down with three 8 mm screws. 32 threads per inch is far better than the
adjusting barrels on the four jaw which are about 6 threads per inch.
The one inch thick CR steel round was bought from Industrial Metals in
Sun Valley
for $37.
It takes days to machine this. One of the problems with my lathe is the
cross
slide feed is only in one thou increments. (.001) To build a near zero
run out adapter one needs
1/10 th thousands feed. (.0001)
Paul Lamar
The Rotary Engine free News Letter. Powered by Linux. If you want off
the list PLEASE let me know and I will remove you. ACRE NL web
site.
http://www.rotaryeng.net You Tube
http://tinyurl.com/beqqxas
Copyright 1998-2016 All world wide rights reserved.