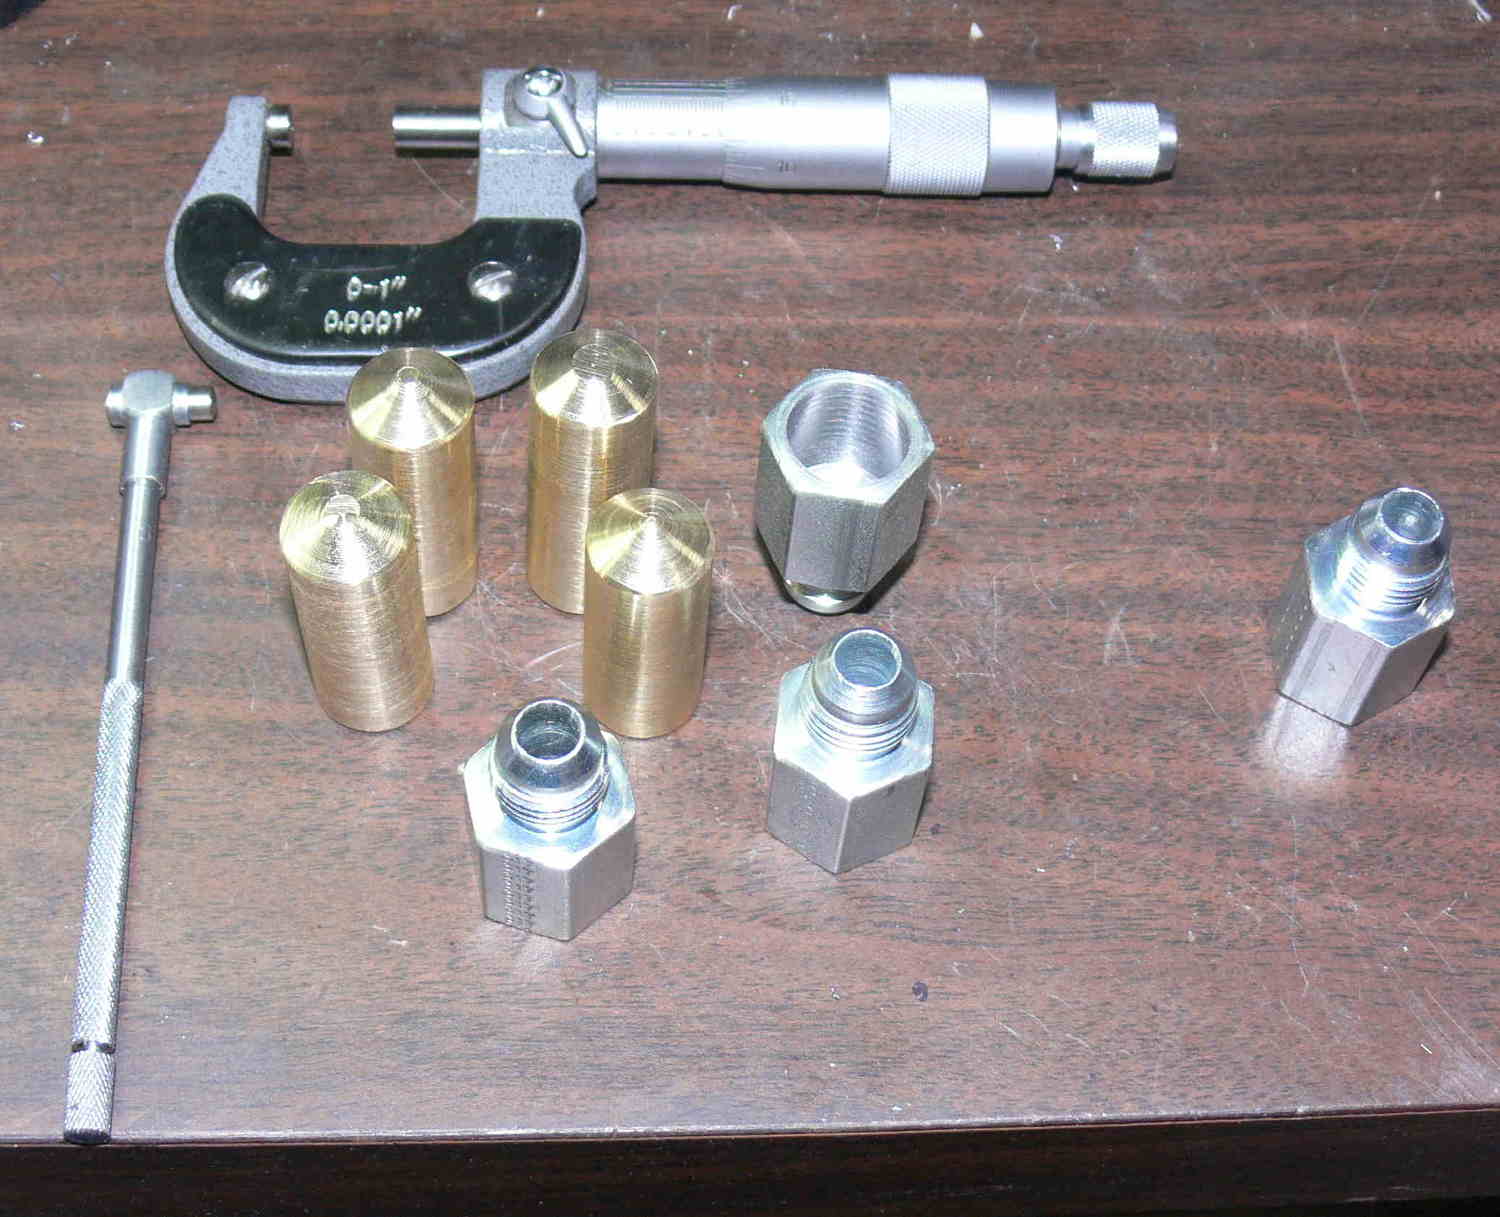
My Morse taper gave out when drilling brass on my CC lathe. The drill
digs
into the brass and then the taper slips. It took me hours to drill a 2
inch hole in
the 3/4 thick aluminum bar shown keeping the taper chuck from rotating.
It holds when drilling aluminum or steel.
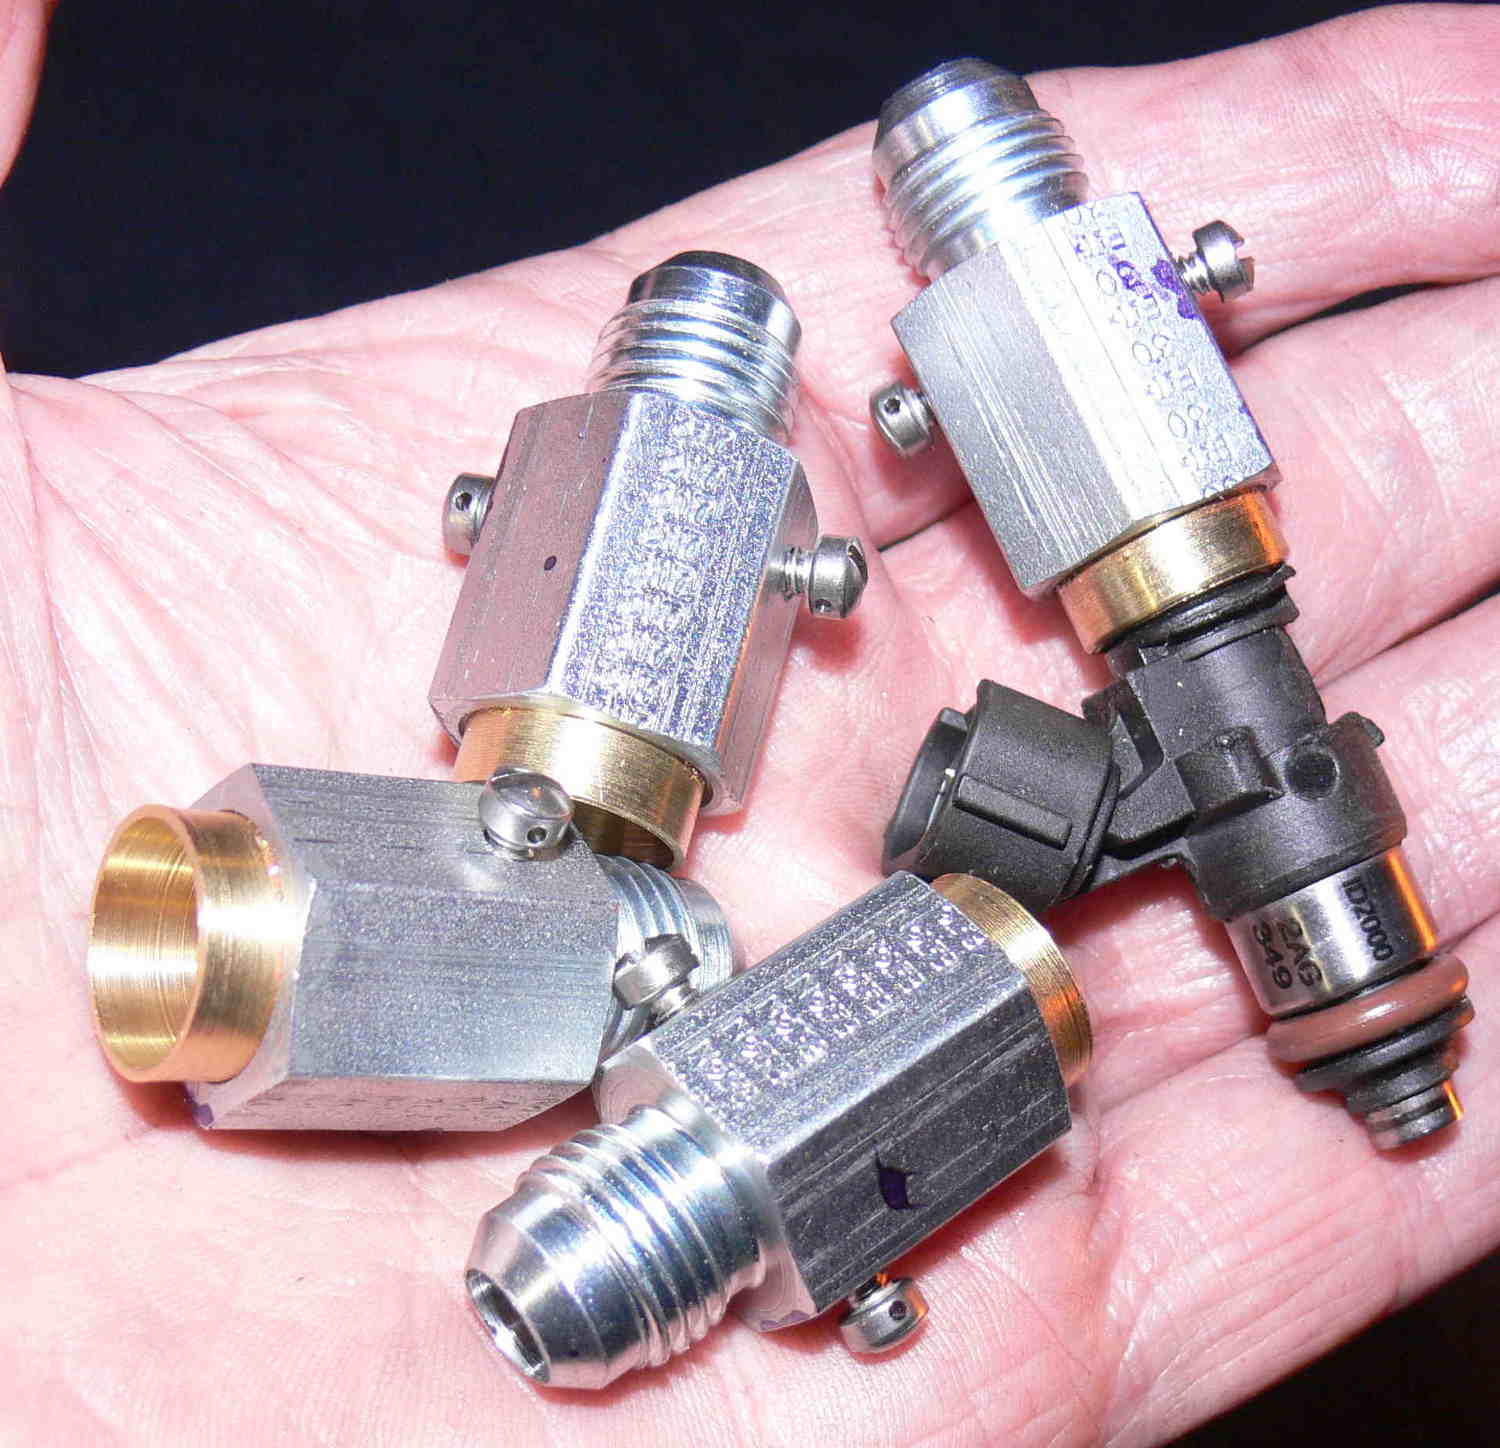
The reason for the brass interior part was because aluminum
would generate yellow snot when flowing methanol.
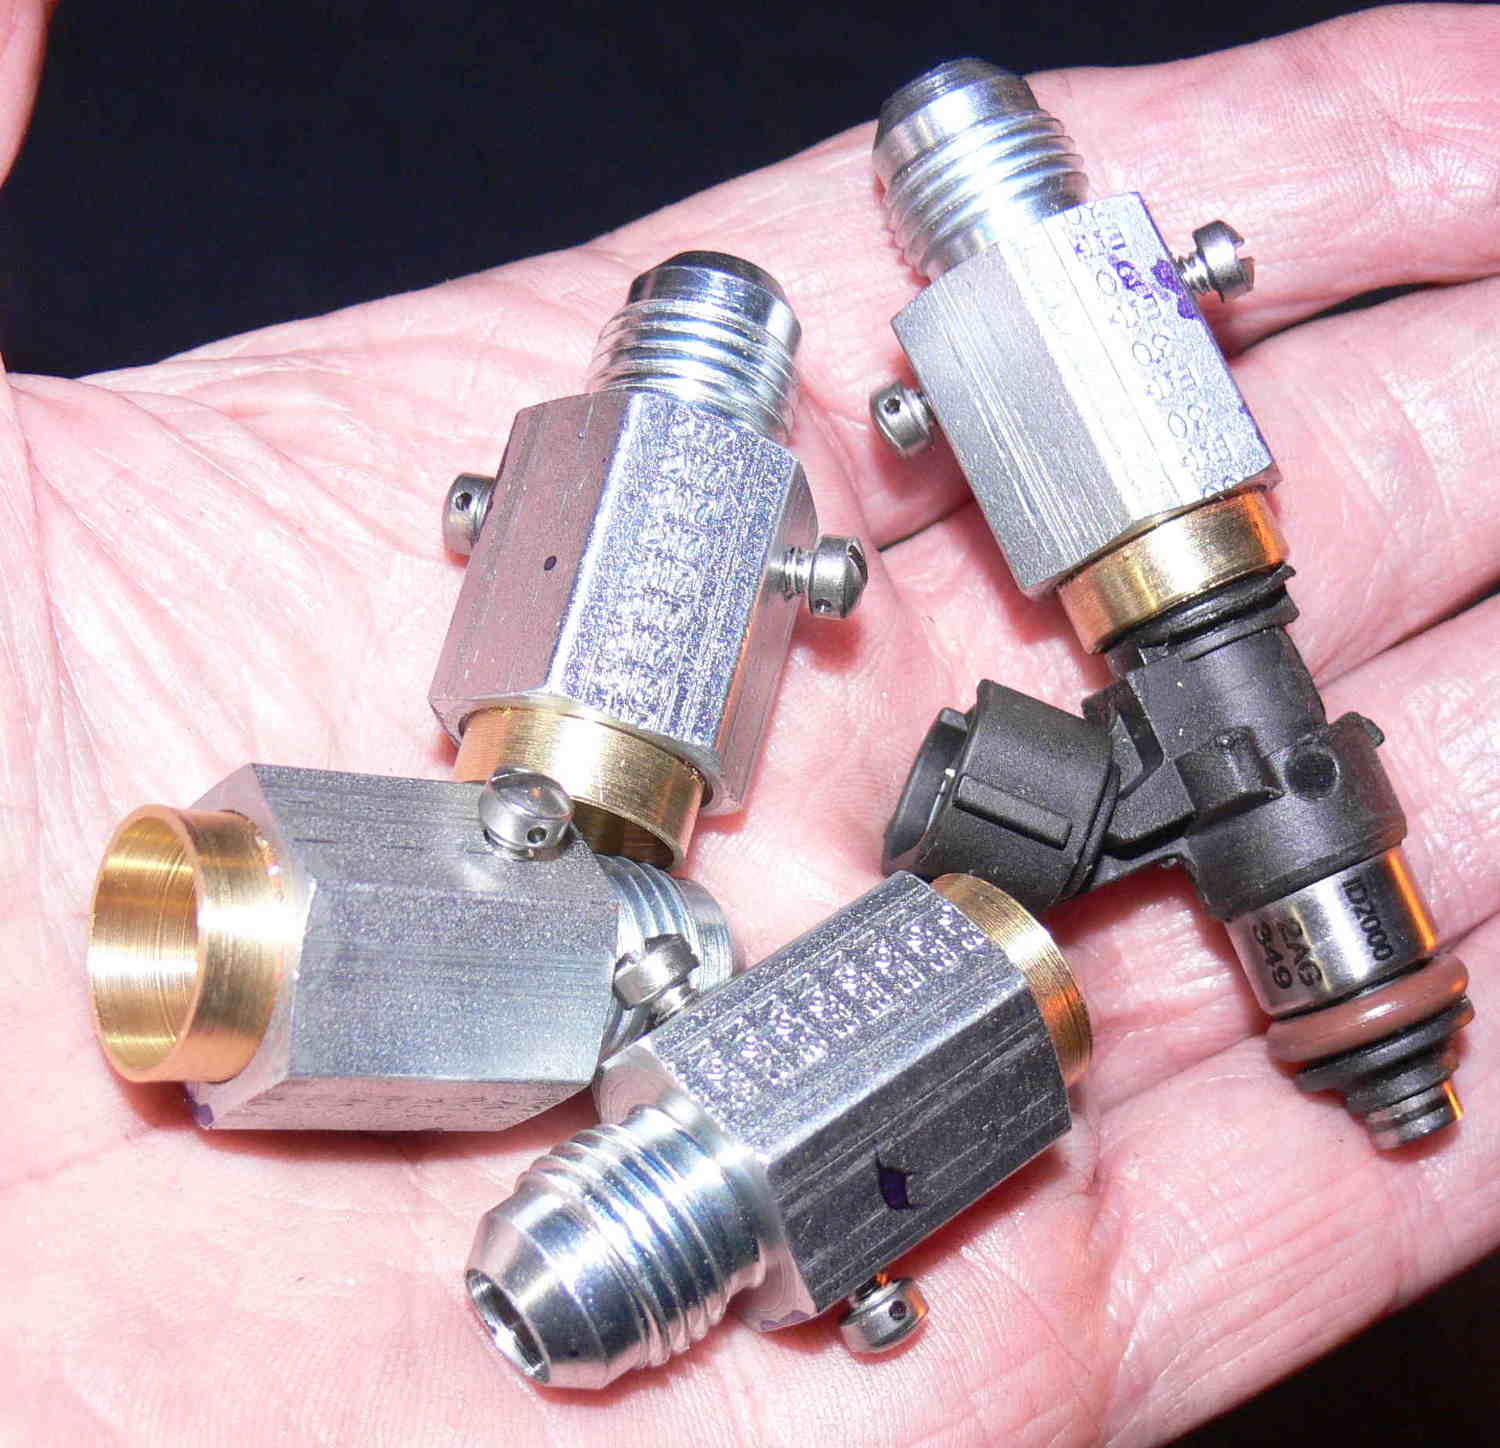
These injector holders are high precision. The adjustable 3 jaw
chuck on my CC lathe was under a 1/2 thou run out. This design would
not be possible with out that.
Basically it is built around 37 degree flare fitting AN-6 to 1/4 inch
pipe steel adapter from McMaster Carr. Under $3 each.
And 5/8 diameter brass rod insert. That had to be machined down
as the diameter tolerance was all over the lot.
In terms of hours of engineering, design and machining at $50 an hour
they are
worth well over $500 each :-)
The tiny drilled head SS 6-32 screws are also from MacMaster.
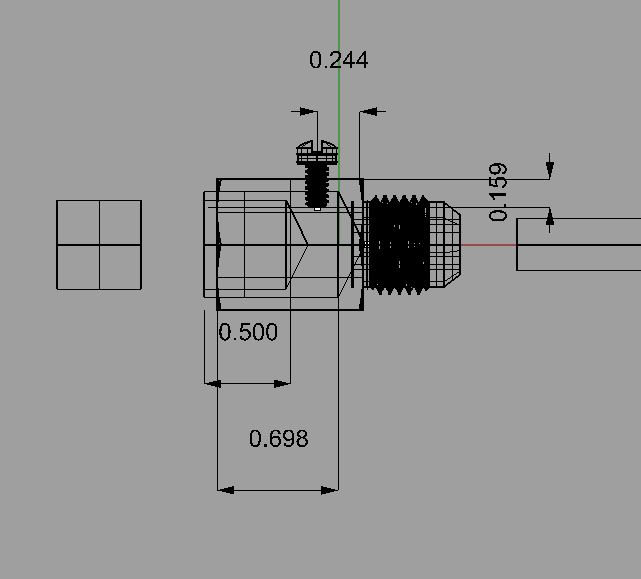
This was a precision operation as well as the hole depth for the
screws was limited to exactly .2 inches or one would have a
150 psi leak. There are only about 6 threads in the hole.
Once they are safety wired they just act as retaining pins.
The mechanic better go easy with the screw driver :-)
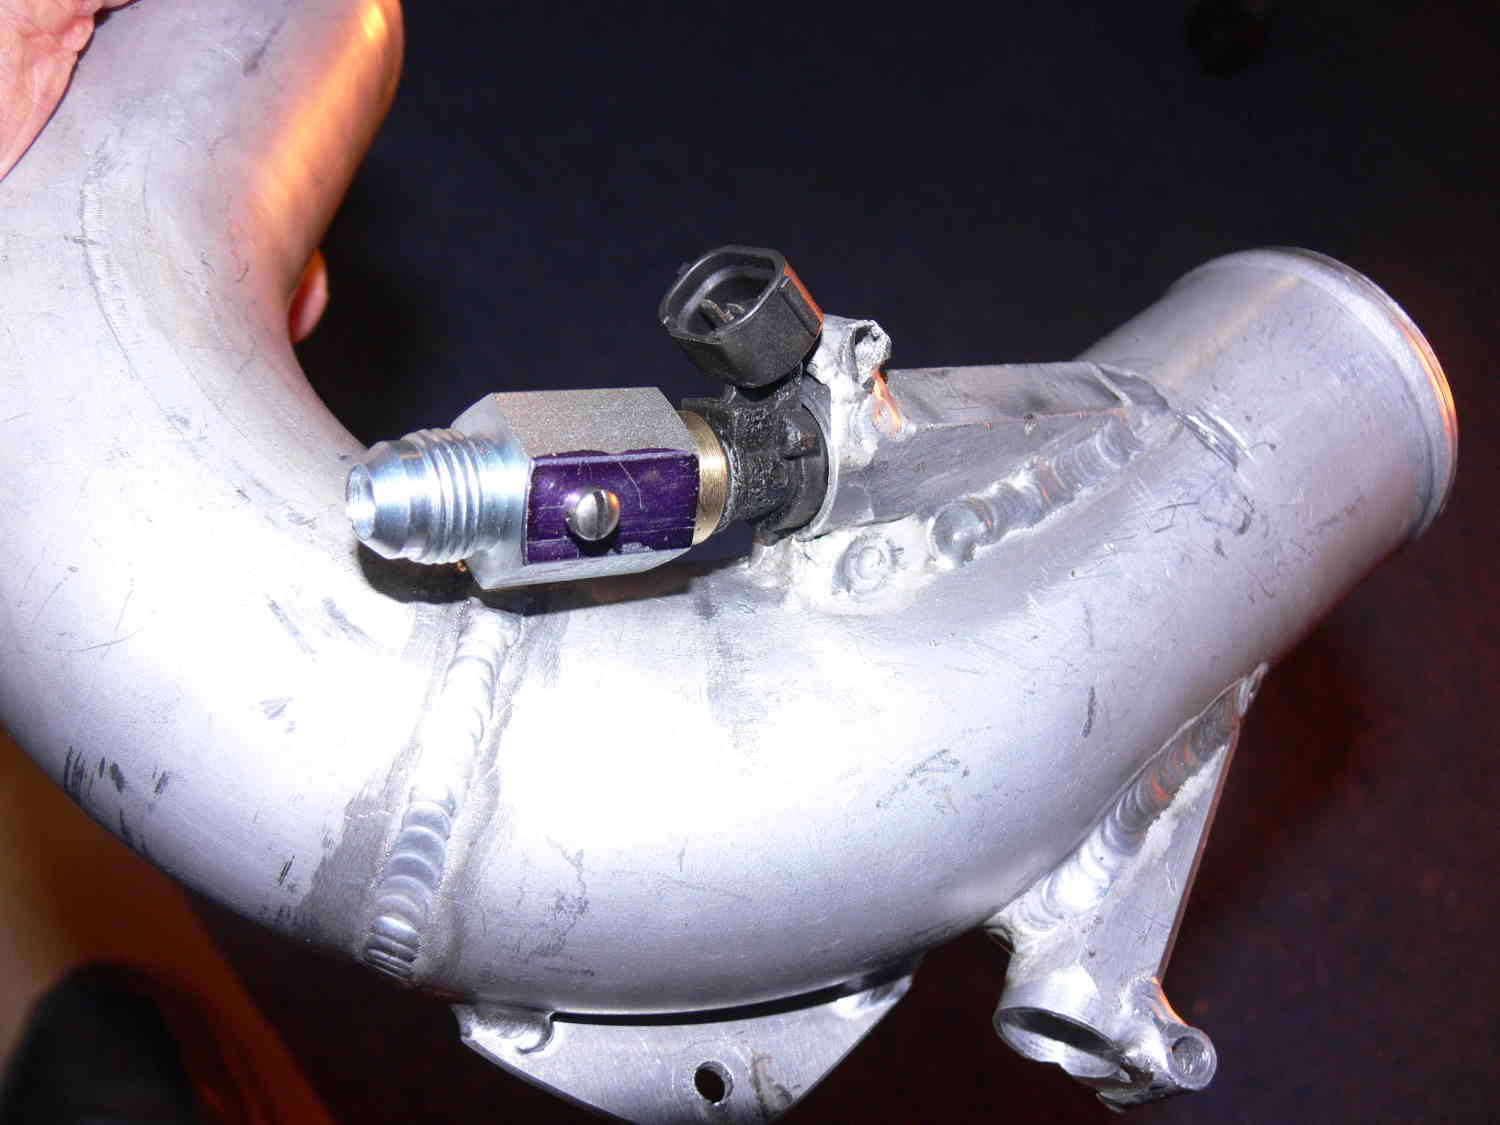
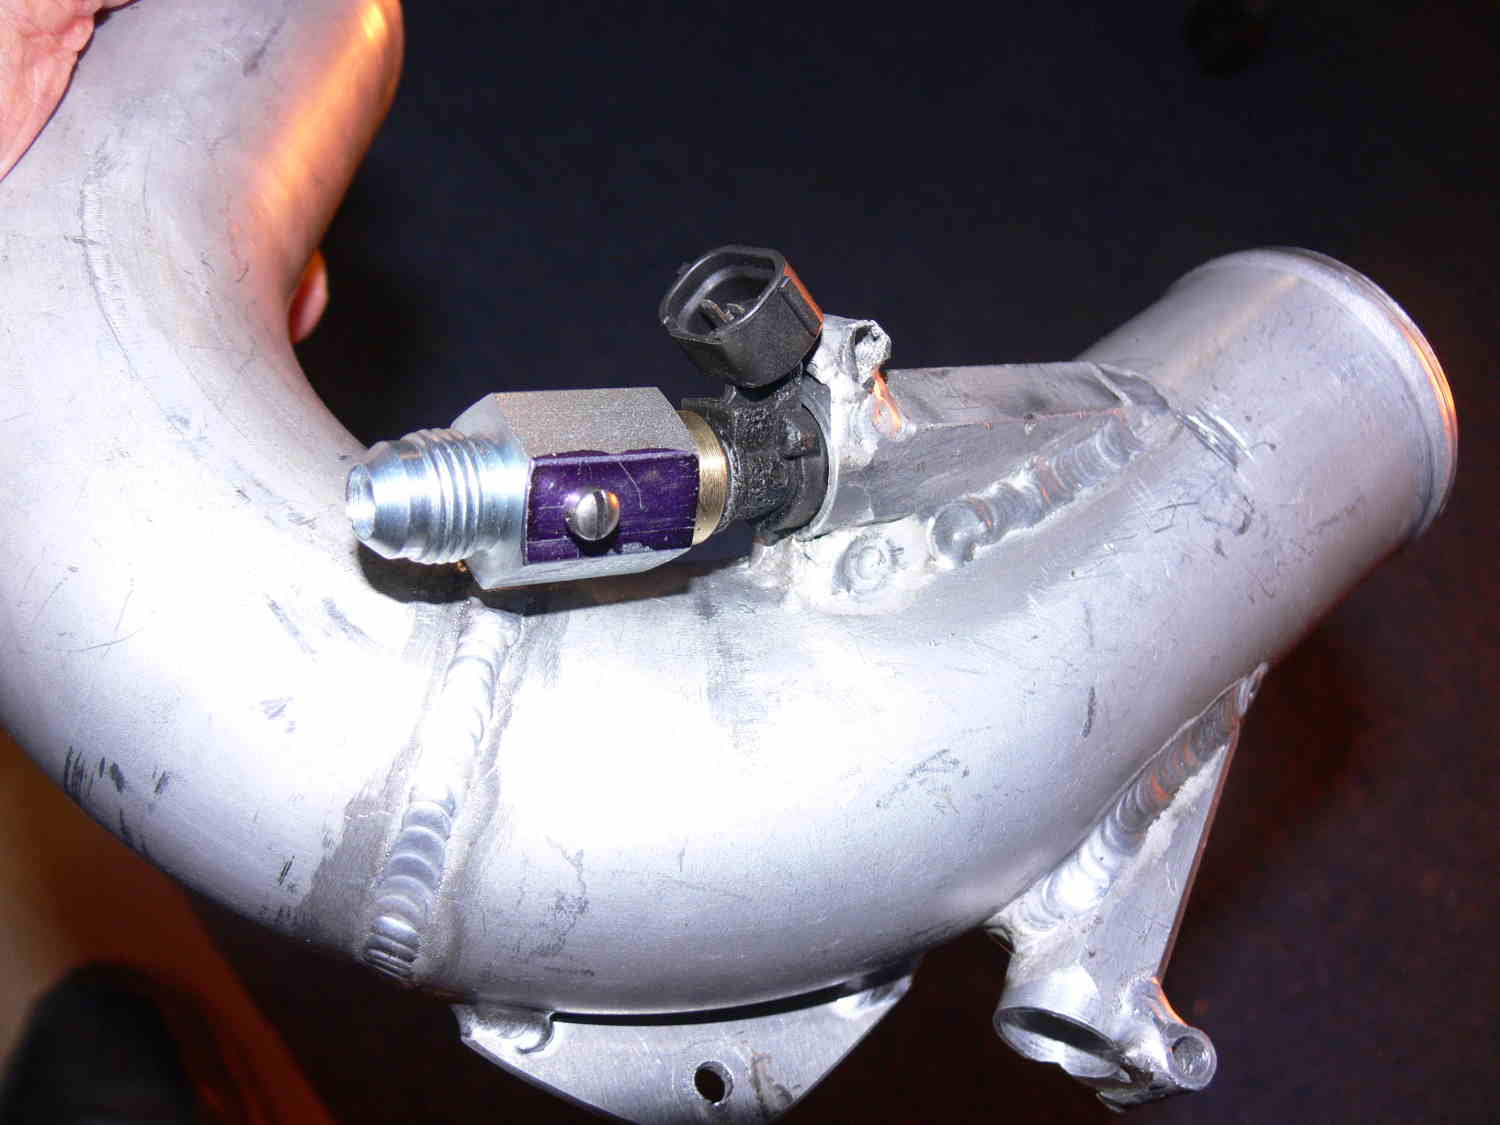
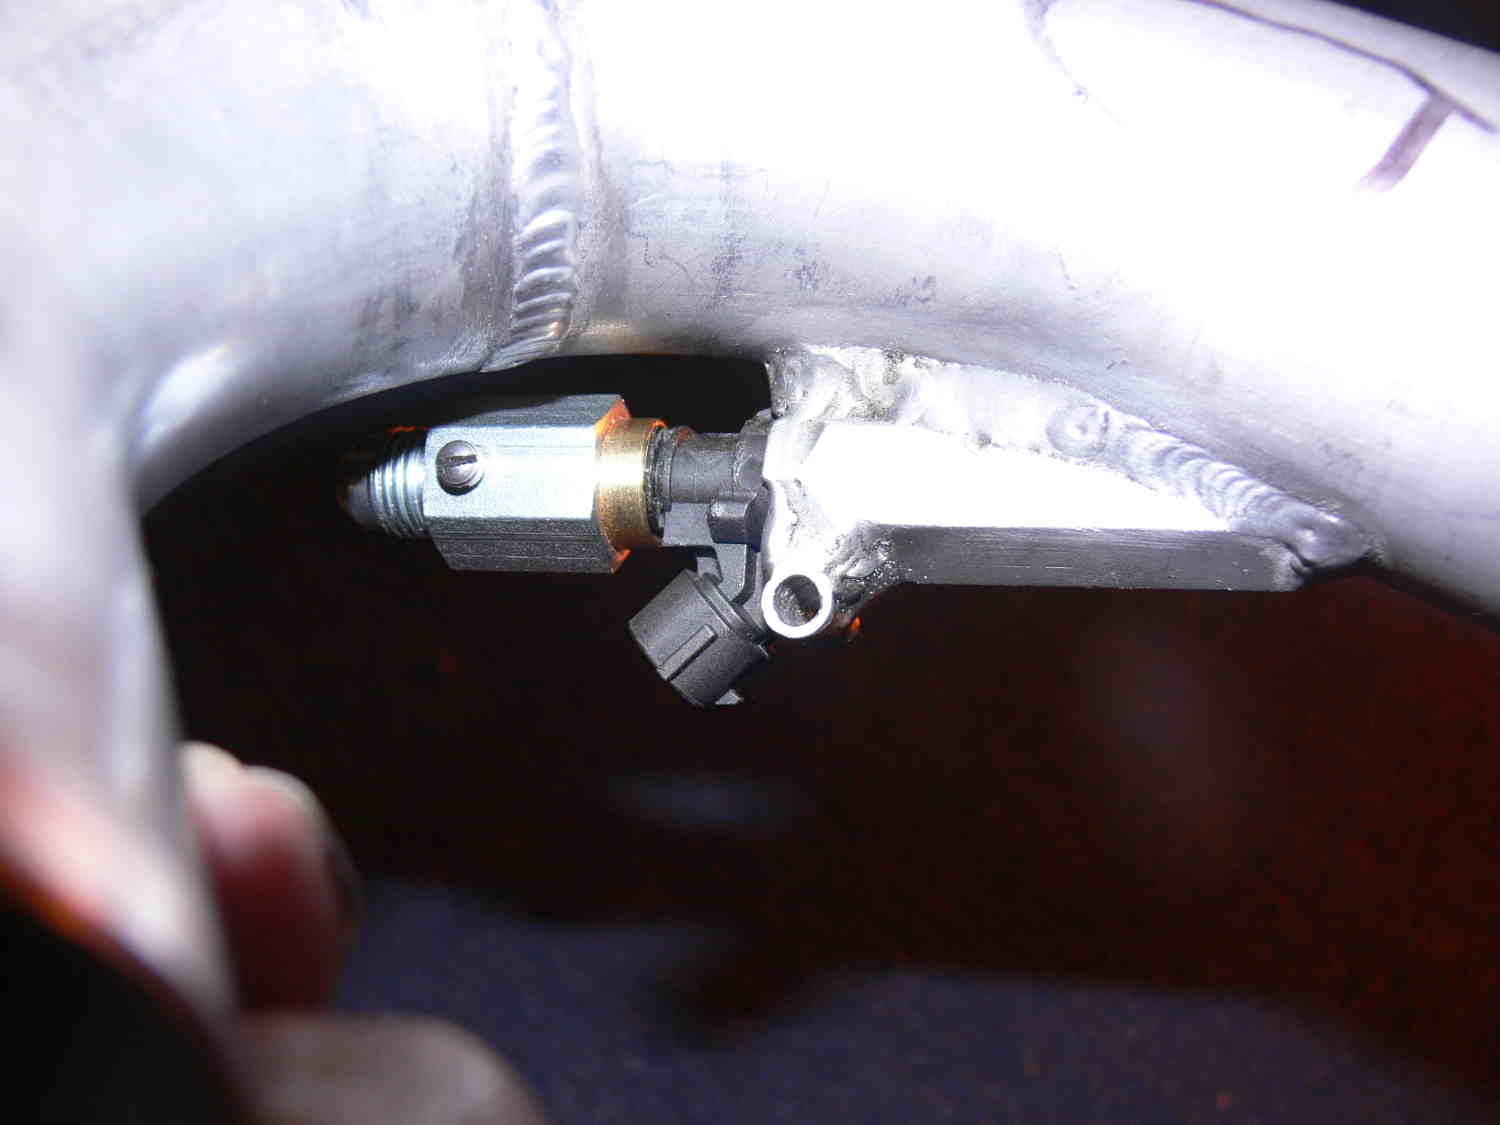
The .040 aluminum straps holding the whole works together are not shown.
They will be tig welded to the large intake tubes.
This 200 pound 2 rotor engine is generating 650 HP with only four
injectors. PAC in Oz used
eight for some strange reason. Maybe they have not heard about the
Bosch 2000 injectors :-) Maybe that was for a 4 rotor.
Paul Lamar
The Rotary Engine free News Letter. Powered by Linux. If you want off
the list PLEASE let me know and I will remove you. ACRE NL web
site.
http://www.rotaryeng.net You Tube
http://tinyurl.com/beqqxas
Copyright 1998-2016 All world wide rights reserved.