I think I just learned something.
I am trying to bore a 5 inch diameter hole in 6 inch diameter aluminum
bar stock about 5 inches deep.
I was getting tool chatter. At first I thought I needed a stiffer
boring bar. My boring bar is about .75 inch in diameter.
I discovered if you speed up the carriage feed the chatter goes away
more or less.
Some of you guys on here are expert machinist.
Have you heard of this before ?
Paul Lamar
Paul,
The added chip load stabilizes the cutter and gets it on a different
frequency.
Larry Childs
Thanks Larry.
Nice to know.
Paul Lamar
Paul,
There is no substitute for rigid tooling, particularly when boring holes -
The unavoidable tool deflection causes the tool to "dig in" and sets up a
vibration due to the geometry of the hole - As the tool digs in it deflects
more which causes additional digging in - This progresses until the load
due
to deflection becomes greater than the resistance to making a chip - When
the chip occurs the load is released somewhat causing the "chatter"
This doesn't occur when turning the outside unless the tool is set above
the
centerline of the work - One trick on internal boring with relatively
non-rigid tooling is to raise the tool slightly above the centerline so
that
deflection doesn't cause the tool to dig in - Also tools should be dead
sharp and have a sharp point and the cutting face relatively square to the
direction of feed - Flood coolant helps along with light cuts -
That's my experience - Your mileage may vary - Others may disagree -
(political waffling)
Roland Friestad
Thanks. I was considering making a stiffer boring bar. I had some one
inch square
cold rolled that fit in the tool holder.
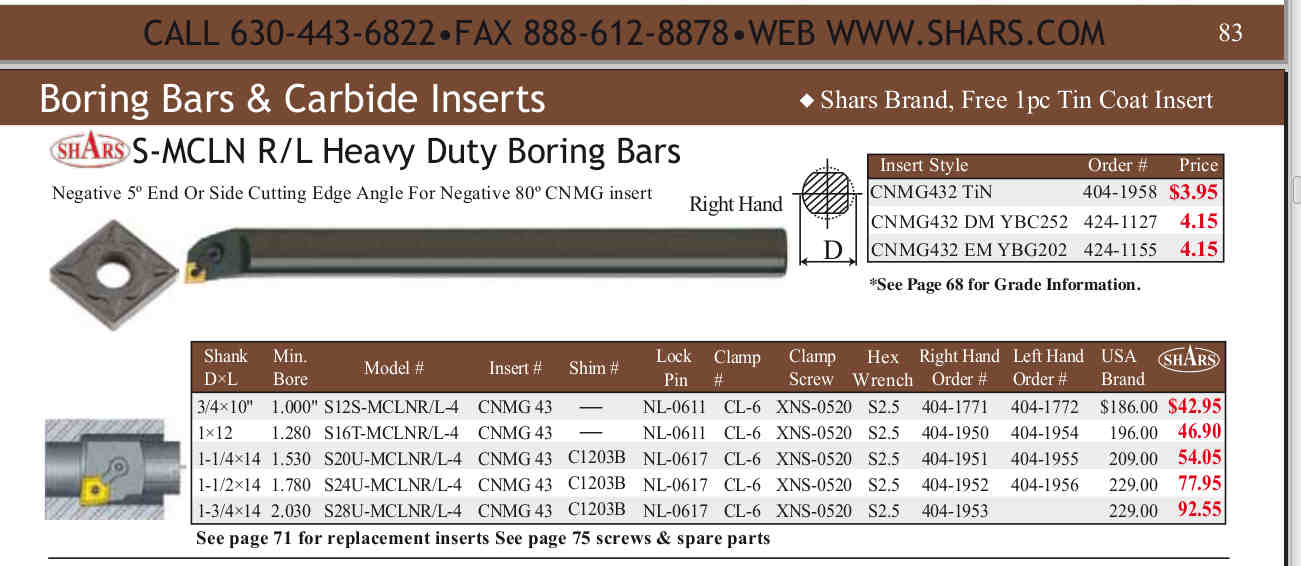
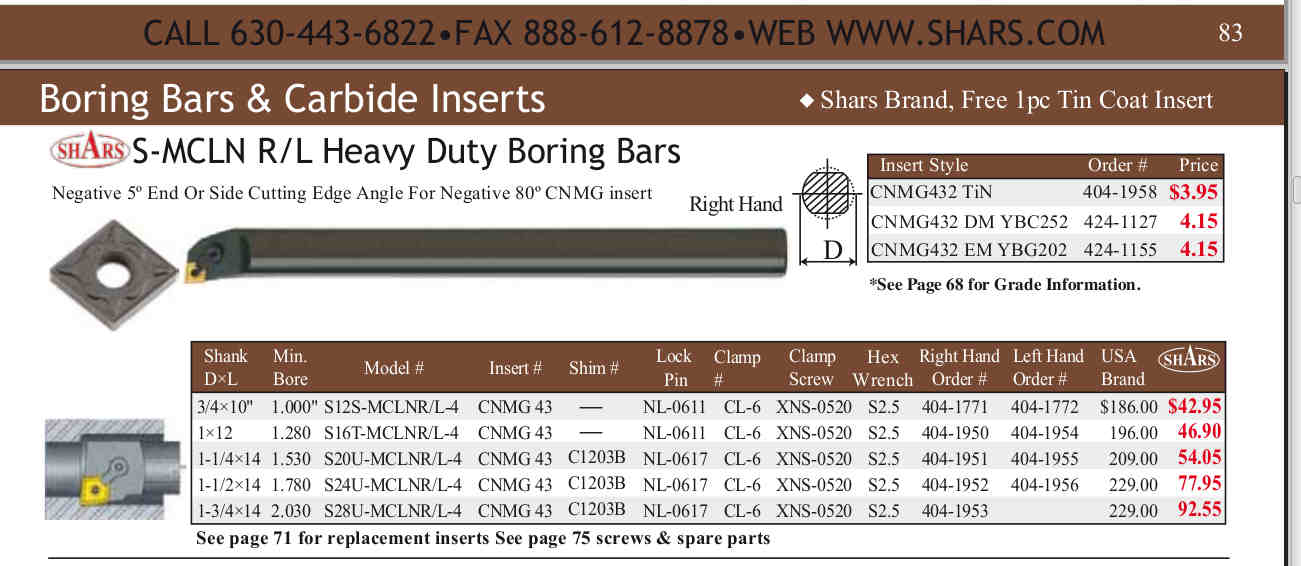
I found this 1.25 by 14 inches long at Shars for 54 bucks.
Paul Lamar
The Rotary Engine free News Letter. Powered by Linux. If you want off
the list PLEASE let me know and I will remove you. ACRE NL web
site.
http://www.rotaryeng.net You Tube
http://tinyurl.com/beqqxas
Copyright 1998-2017 All world wide rights reserved.