I think I just learned something.
I am trying to bore a 5 inch diameter hole in 6 inch diameter
aluminum bar stock about 5 inches deep.
I was getting tool chatter. At first I thought I needed a stiffer
boring bar. My boring bar is about .75 inch in diameter.
I discovered if you speed up the carriage feed the chatter goes away
more or less.
Some of you guys on here are expert machinist.
Have you heard of this before ?
Paul Lamar
Paul, The spindle speed formula RPM= Surface Feet per Minute x 4/
tool Diameter SFM for aluminum is 400 & R is .002/.009 And the feed
rate formula Feed (rate per minute)= RPM x T (number of teeth) x
R (chip load)
Ray Hellstrom
Thanks Ray,
Interesting.
Paul Lamar
Paul, Are you using a carbide cutting tool? If so, a large nose
radius can cause chatter. Also, I didn't mention that the depth of
cut, which should be the adjusted with the speed to produce a
continuous chip which forms due to plastic deformation of the crystal
structure in the unmachined work surface and the shear occurs along
the shear plane. As the cutting tool compresses the metal immediately
ahead of the cutting tool, the deformation of the crystal structure
elongates, the material above the cutting edge is forced along the
chip tool interface and away from the tool.
Ray Hellstrom
No it is a sharp point.
BTW do any of you guys know where I can get a six inch diameter
steady rest?
Paul Lamar
Paul
To the best of my knowledge, steady and follow rests are machine
specific and not universal. I would start with the lathe manufacturer
and get the model number.
Bolton tools sells inexpensive Chinese made ones. It may be possible if
your ways are reasonably close to the ones they offer- it might work for
you.
Alan Mullen
Colorado
My CC lathe is 40 years old. It came with a steady rest that is too small.
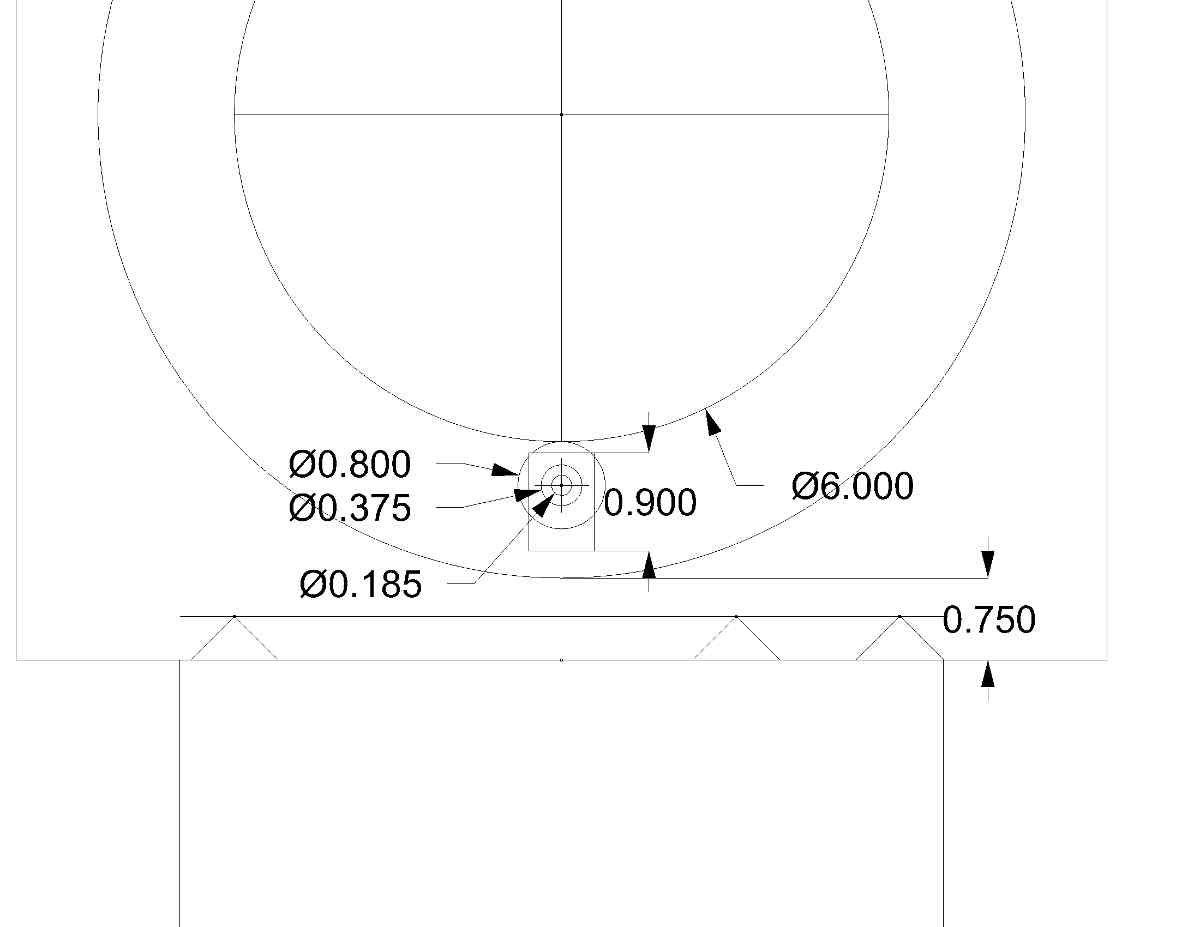
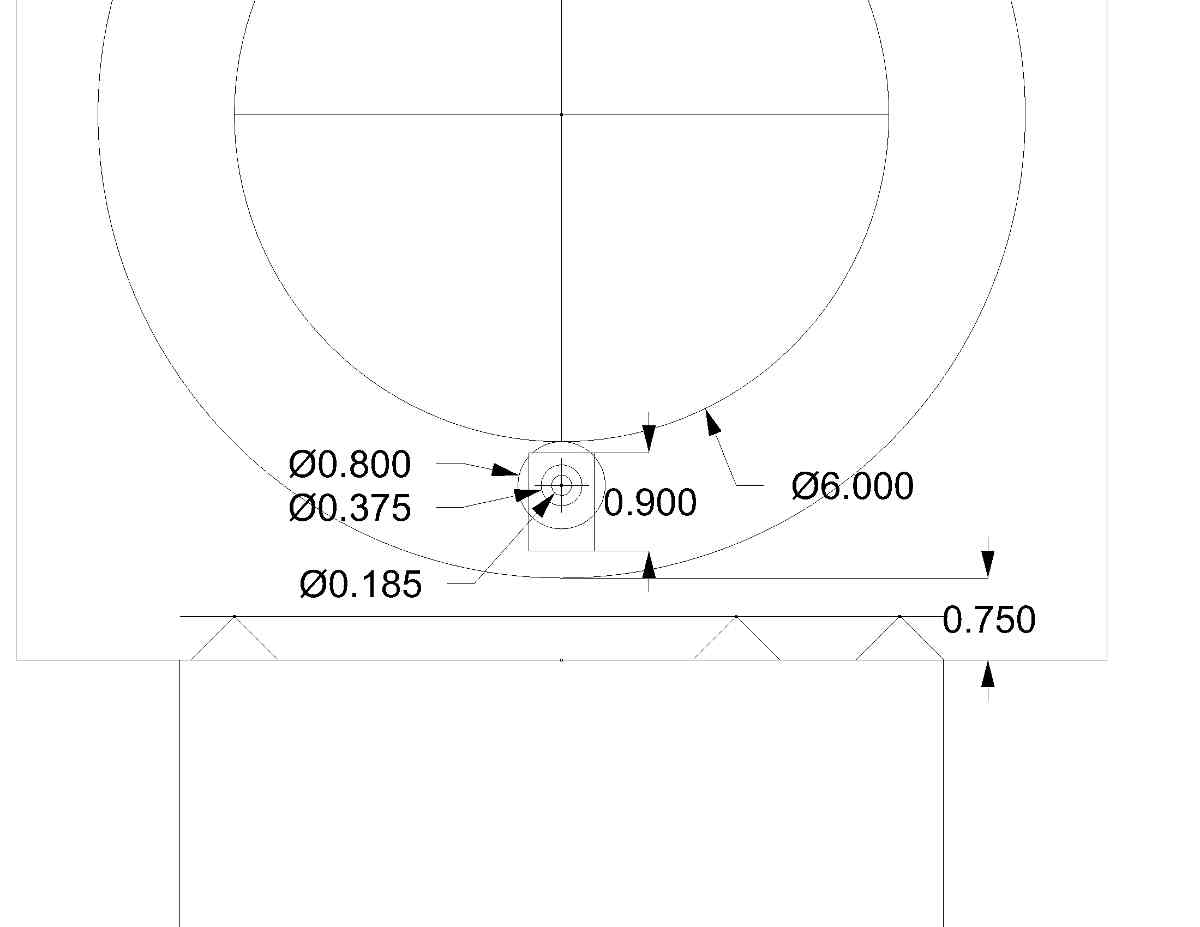
I will make one out of a 10" by 10" steel plate .75 inches thick. A 8
inch diameter hole will
be cut in the plate with flame cutter. More on this shortly.
Here is a picture of why I need it.
Paul Lamar
Paul,
What about using a DoAll vertical bandsaw? From their website, most
have a 13" vertical height, the bigger ones get more horizontal
distance. Find a shop with one with the blade welder at the machine,
With your height, DoAll might suggest the best blade and the pilot hole
could be sized accordingly.
Another thought. My old horizontal Kalamazoo bandsaw has a 19"
horz. x 8" vertical space and takes a 3/4" x .032 blade. Bore a center
hole plus one just inside the ID, cut pie slices Once you get the first
pie slice out, the others don't need a rim hole.
Jim Rudholm
I have a Cheap Chinese copy of a DoAll. I am rather surprised that
the quality of Chinese products has greatly improved
recently. Ironically that is part of the lack of U.S. jobs problem.
China is a dictatorship and they are not playing fair when it
comes to trade. They control the monetary exchange rate. Floating
currency in most countries is an automatic
means of balancing trade between countries. When the price on a
given countries products goes up the demand goes down
and that changes the monetary exchange rate and tends to balance
the trade. Not so in China. They fix the rate.
We need a large tax or import tariff on Chinese goods to promote
manufacturing here in the US. A small tax
initially making it larger and larger until a balance in trade is
reached.
Now getting back to the machining problem. The band saw would work
on both the six inch billet of aluminum
and the new 3/4 inch thick steady rest. In both cases it would take
a lot of time. The six inch billet is a one time
operation and it is almost done. In the future I will use thick
wall aluminum tubing for that part.
I would still need the steady rest for my small lathe.
The .75 inch thick steel plate for the steady rest would take a
long time to cut an 8 inch diameter hole.
I have a friend with a computer controlled flame cutter and he can
do that in just a few minutes. No need to
push the band saw slowly through thick steel. The saw needs to run
at low feet per second rate to cut such thick
steel other wise the blade gets dull. Also the radius is a bit
tight for a band saw blade.
Another option is water jet. In this geographical area that too
is very expensive. On the airport we have a laser
cutter and I will investigate that option next week.
Thanks for making me think of my options :-)
Paul Lamar
Make your center support frame from 1/8" steel plate, welded up on the
corners, hinged through the middle, with bearings for support faces.
Steve Carlisle
You read my mind :-)
That is what I had in mind more or less except it is 3/4 inch thick
steel plate.
Paul Lamar
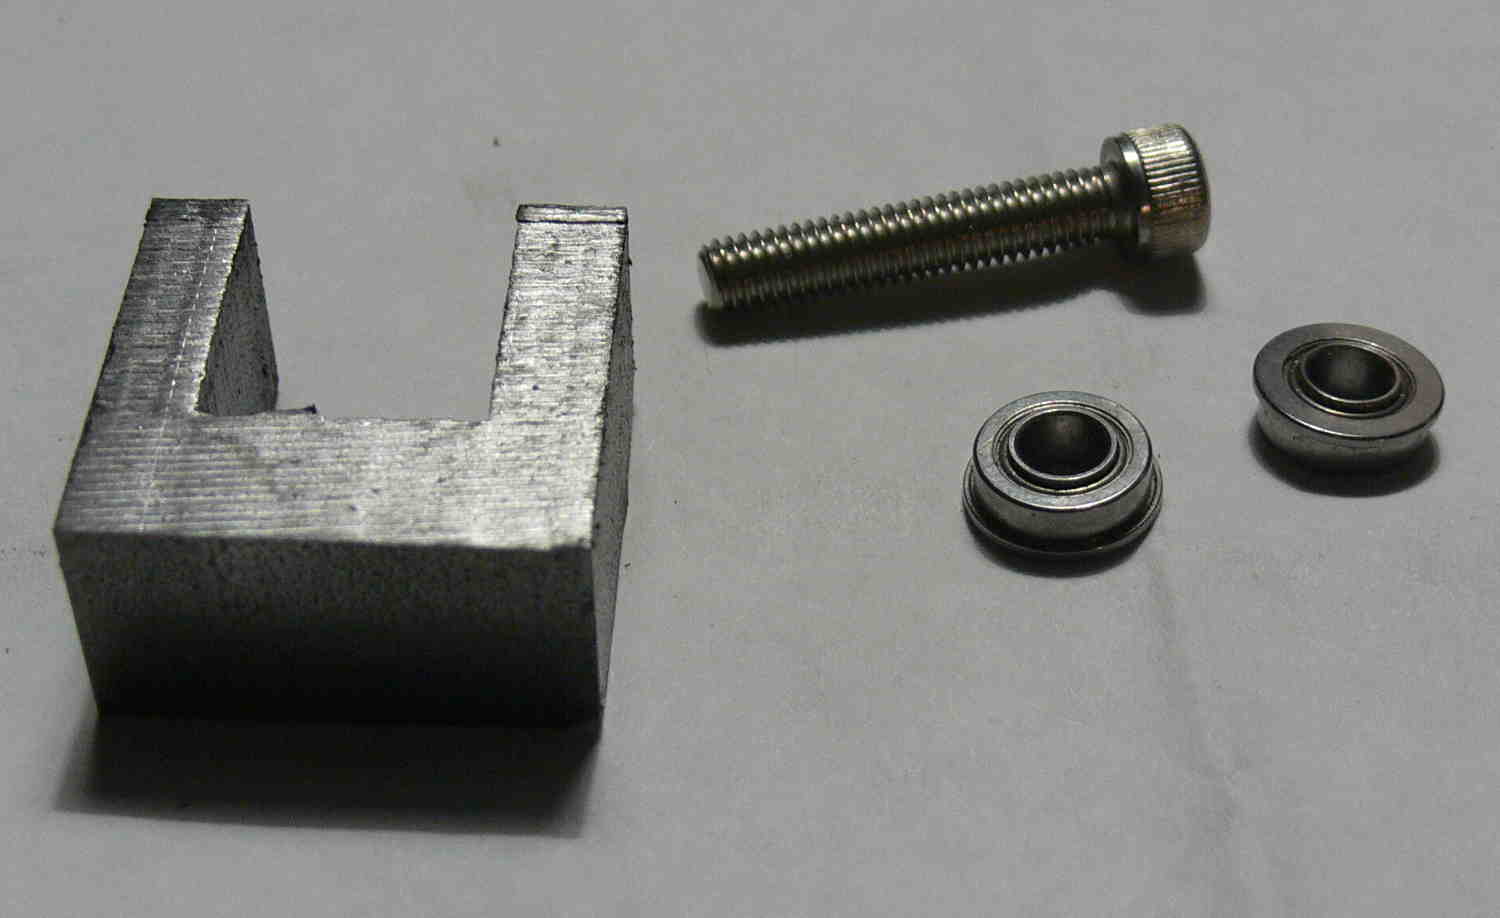
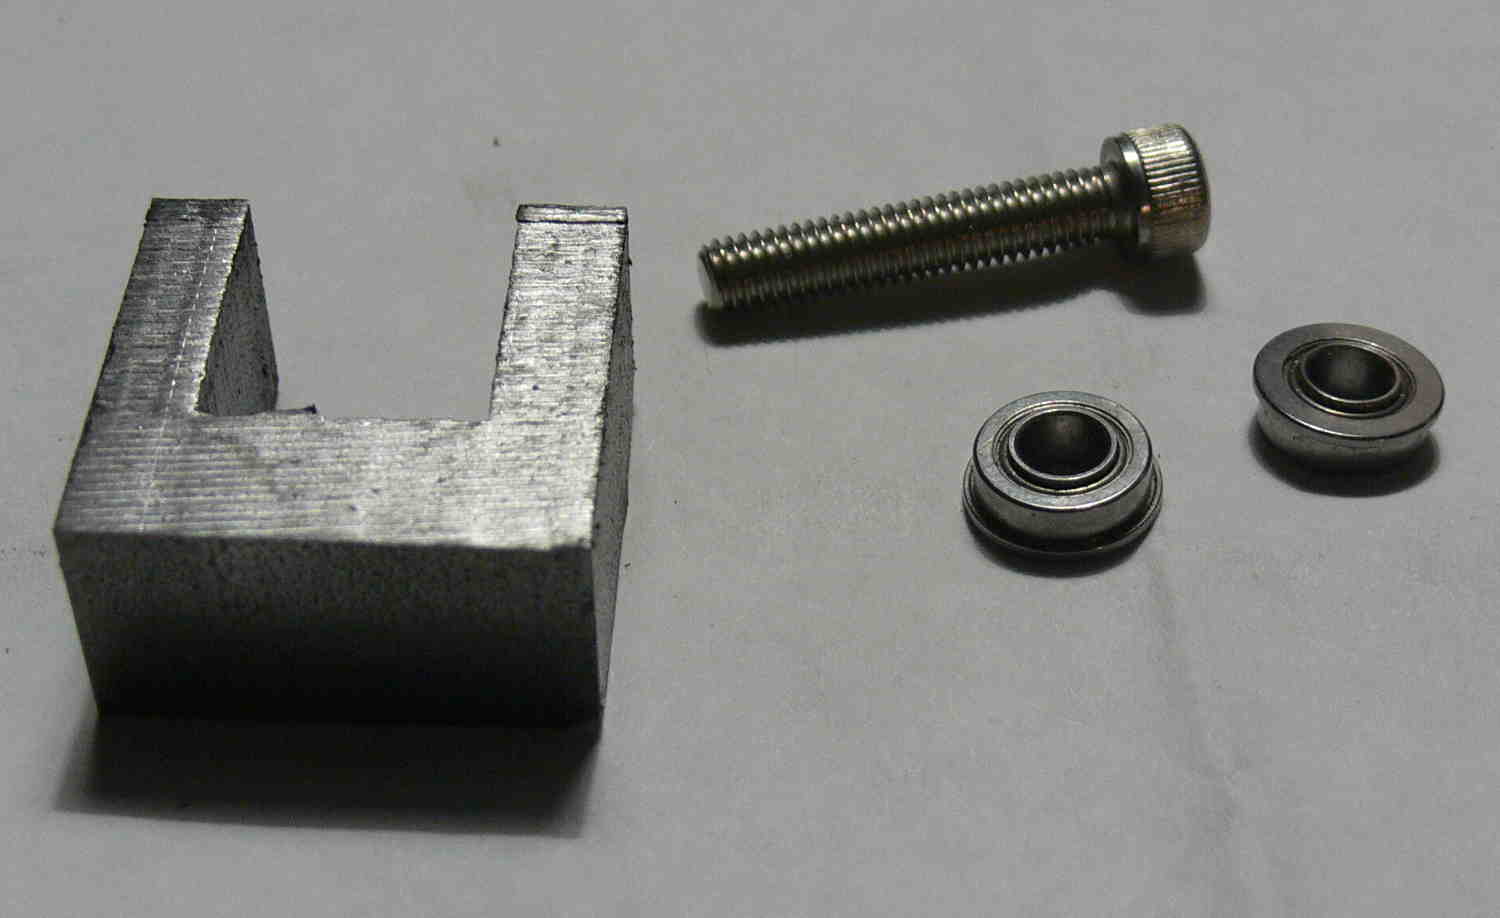
There will be four rollers about a half inch wide with small ball bearings.
This will allow checking the run out and fixing it.
The adjusting screws are 1/4 28. With fine thread screws like that it is
possible
to get the run out close to zero.
Paul Lamar
The Rotary Engine free News Letter. Powered by Linux. If you want
off the list PLEASE let me know and I will remove you. ACRE NL web
site.
http://www.rotaryeng.net You Tube
http://tinyurl.com/beqqxas
Copyright 1998-2017 All world wide rights reserved.