Getting up too speed on my LinuxCNC installation and I ran across
this well written explanation of why Windows does not work for
machine control in pncconf.pdf. (attached)
The Maximite and DOS QB do not have this problem.
Way back in in 1975 when I wrote a hardware interrupt driven
multitasking OS for my Road Test system I figured this out. I
designed a priority encoder for the hard ware interrupts using
discrete integrated circuits. This was years ahead of it's time. Only
in the past 20 years or so has this implemented in microcomputers
like the PIC and ARM and I suspect it is yet to be implemented in
Intel products. The pulse from the speed sensor had the highest
priority in the Road Test system. I looked like an idiot Muslim in
those days :-(
http://www.rotaryeng.net/RT1.pdf
"The servo period sets the heart beat of the system. Latency refers
to the amount of time the computer can be longer then that period.
Just like a rail road, LinuxCNC requires everything on a very tight
and consistent time line or bad things happen. LinuxCNC requires and
uses a real time operating system, which just means it has a low
latency ( lateness ) response time when LinuxCNC requires its
calculations and when doing LinuxCNCs calculations it cannot be
interrupted by lower priority requests (such as user input to screen
buttons or drawing etc)."
Paul Lamar
You wouldn't want to use Microsoft Windows anyway, you could only
make malware ! Chris. Hoskins
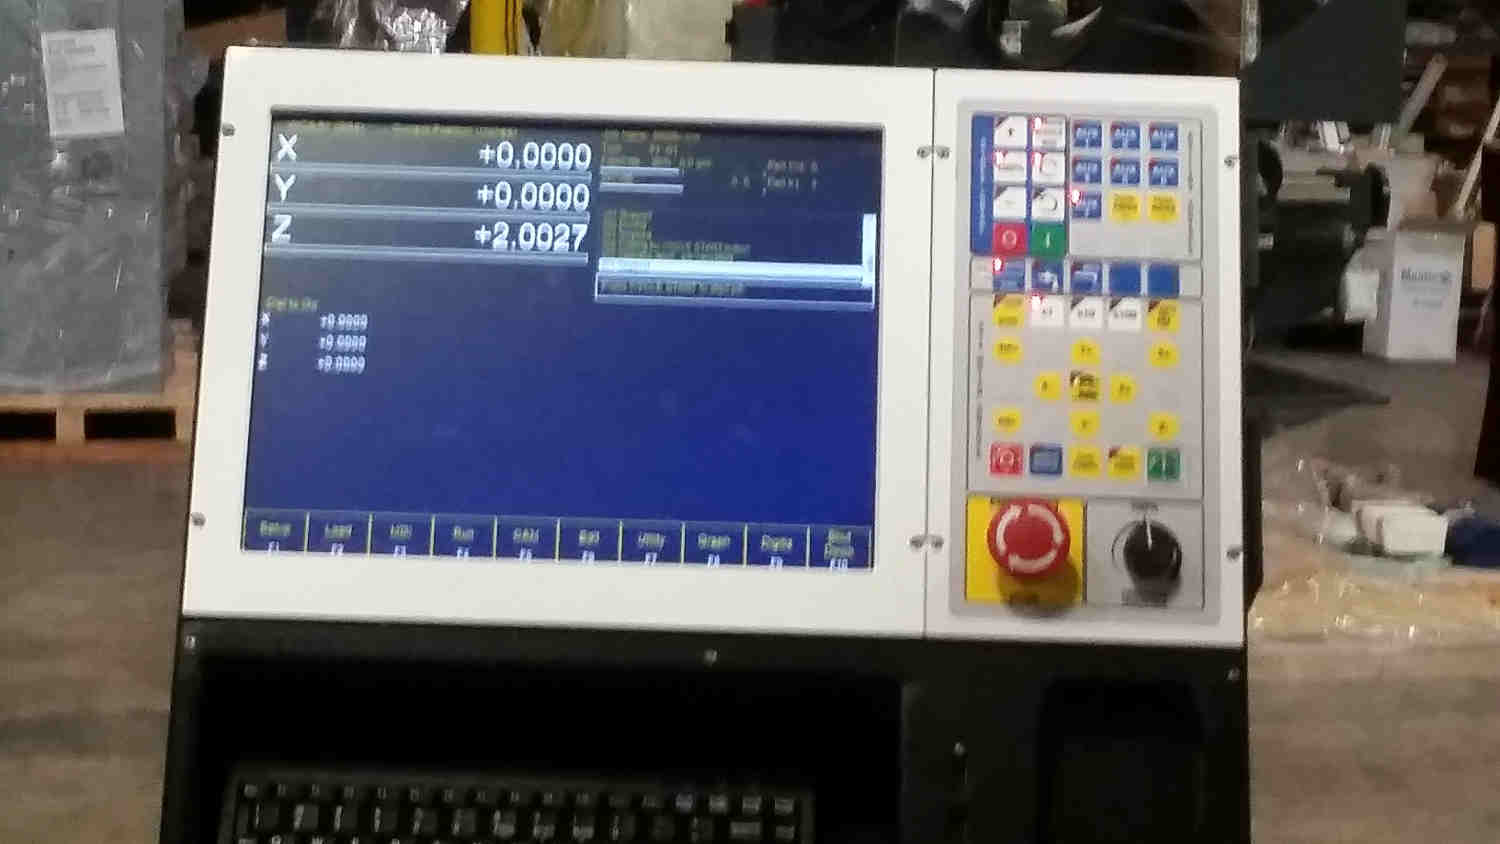
Many of the high end Japanese machine tools have Fanuc controllers. These
use Windows for the front end which includes all the file loading and
storage of the network. They also have full USB support and use PC type
hard drives in the machines. I believe a Motorola chip does the heavy
lifting.
Things are much easier now that the control isn't doing the housekeeping.
With the hard drive(s) in the control, memory is no longer as any large
(as most 5 axis programs tend to be) file can be fed directly to the
control from the disk. Drip feed is no longer limited to I/O speed.
Gary Knutson
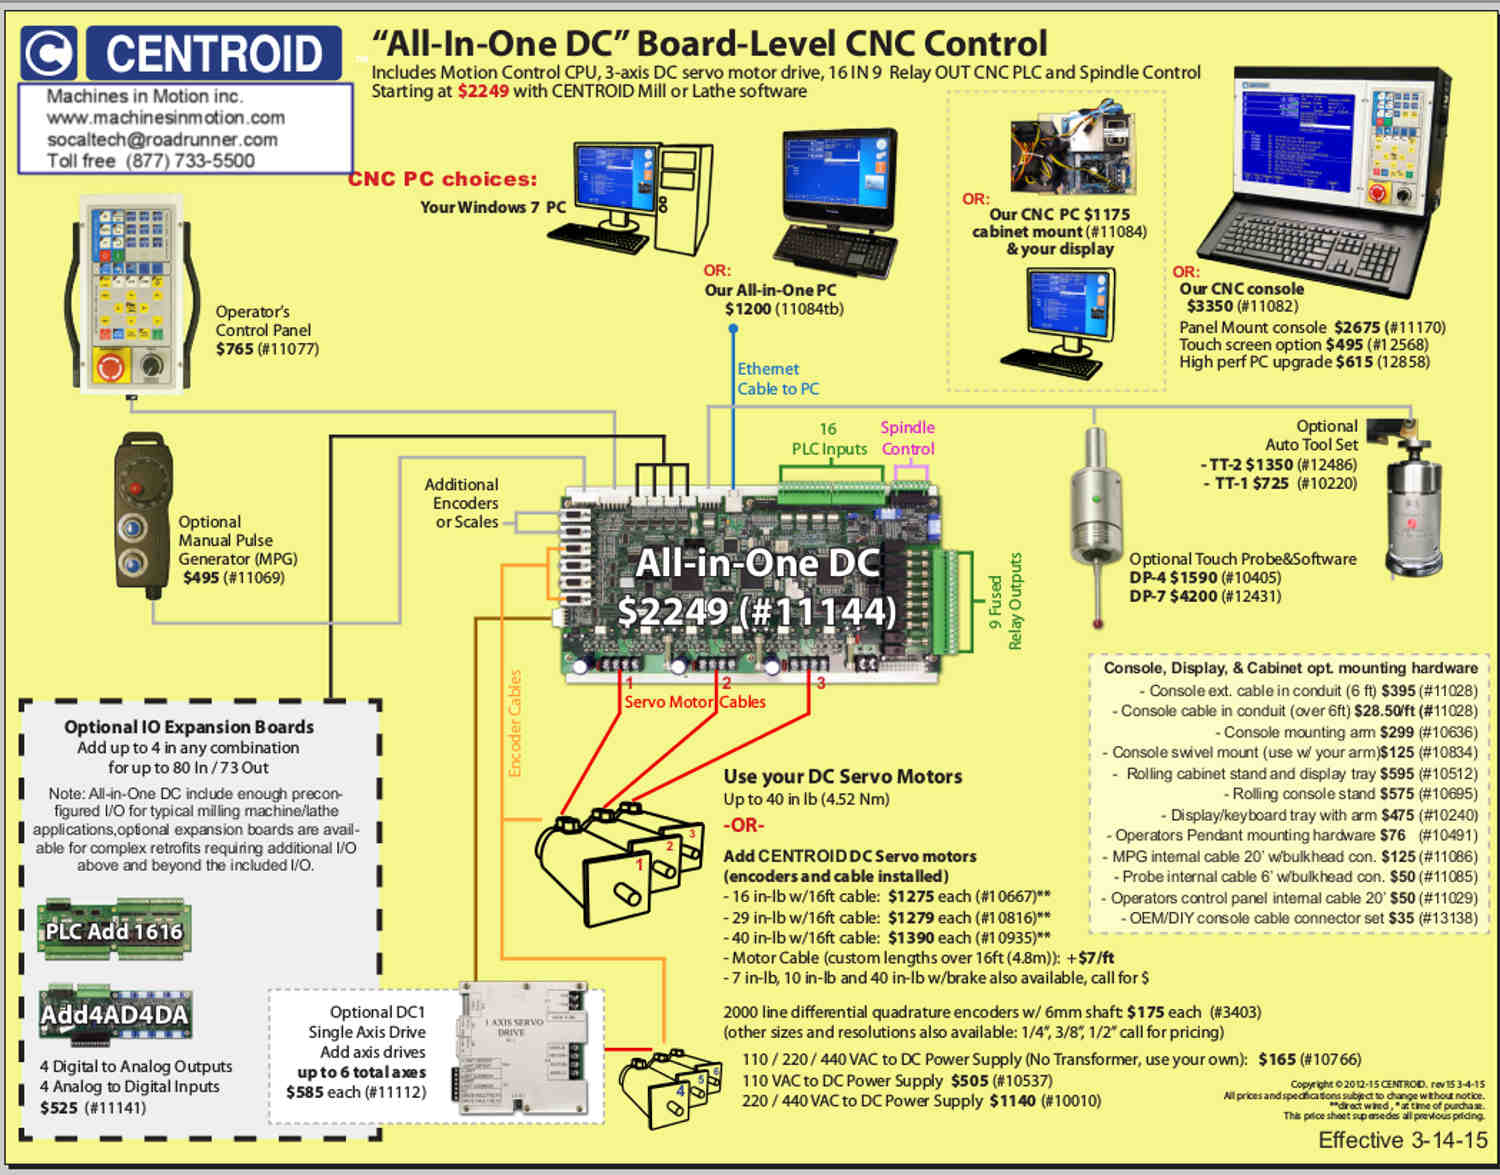
I looked at a Windows based NC upgrade and they wanted
$2,200 for proprietary hard ware plus a PC. If they went out
of biz I would be stuck for parts and service.
It was $500 for hard tapping software alone.
http://www.cnc-machine-controls.com/
LinuxCNC software is free. That includes hard tapping software.
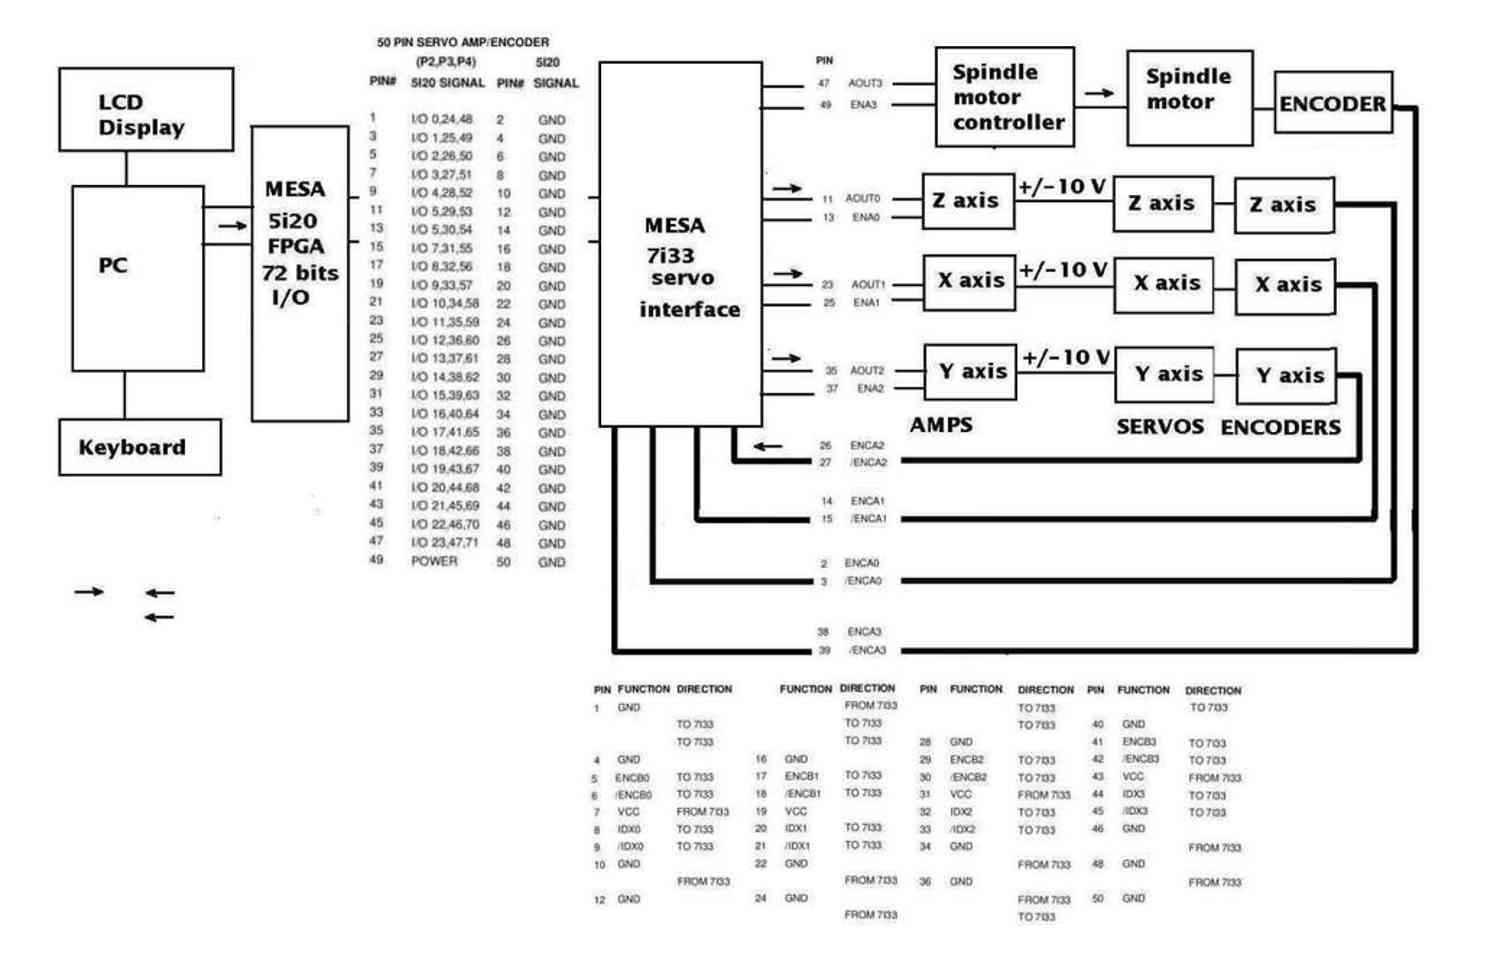
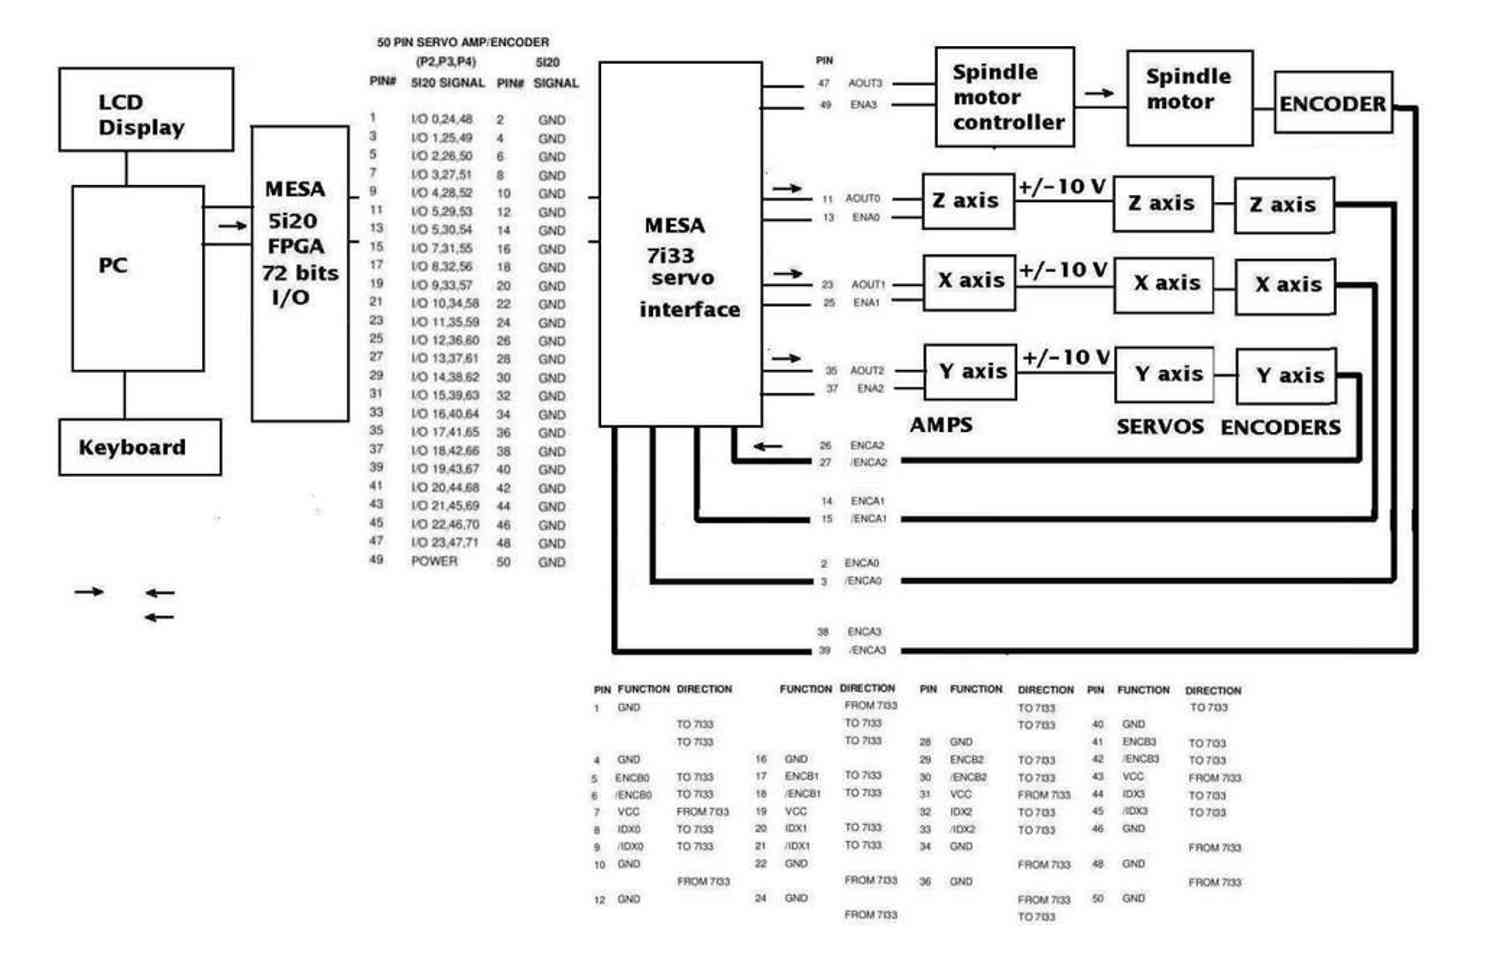
It requires only a PCI par port I/O card.
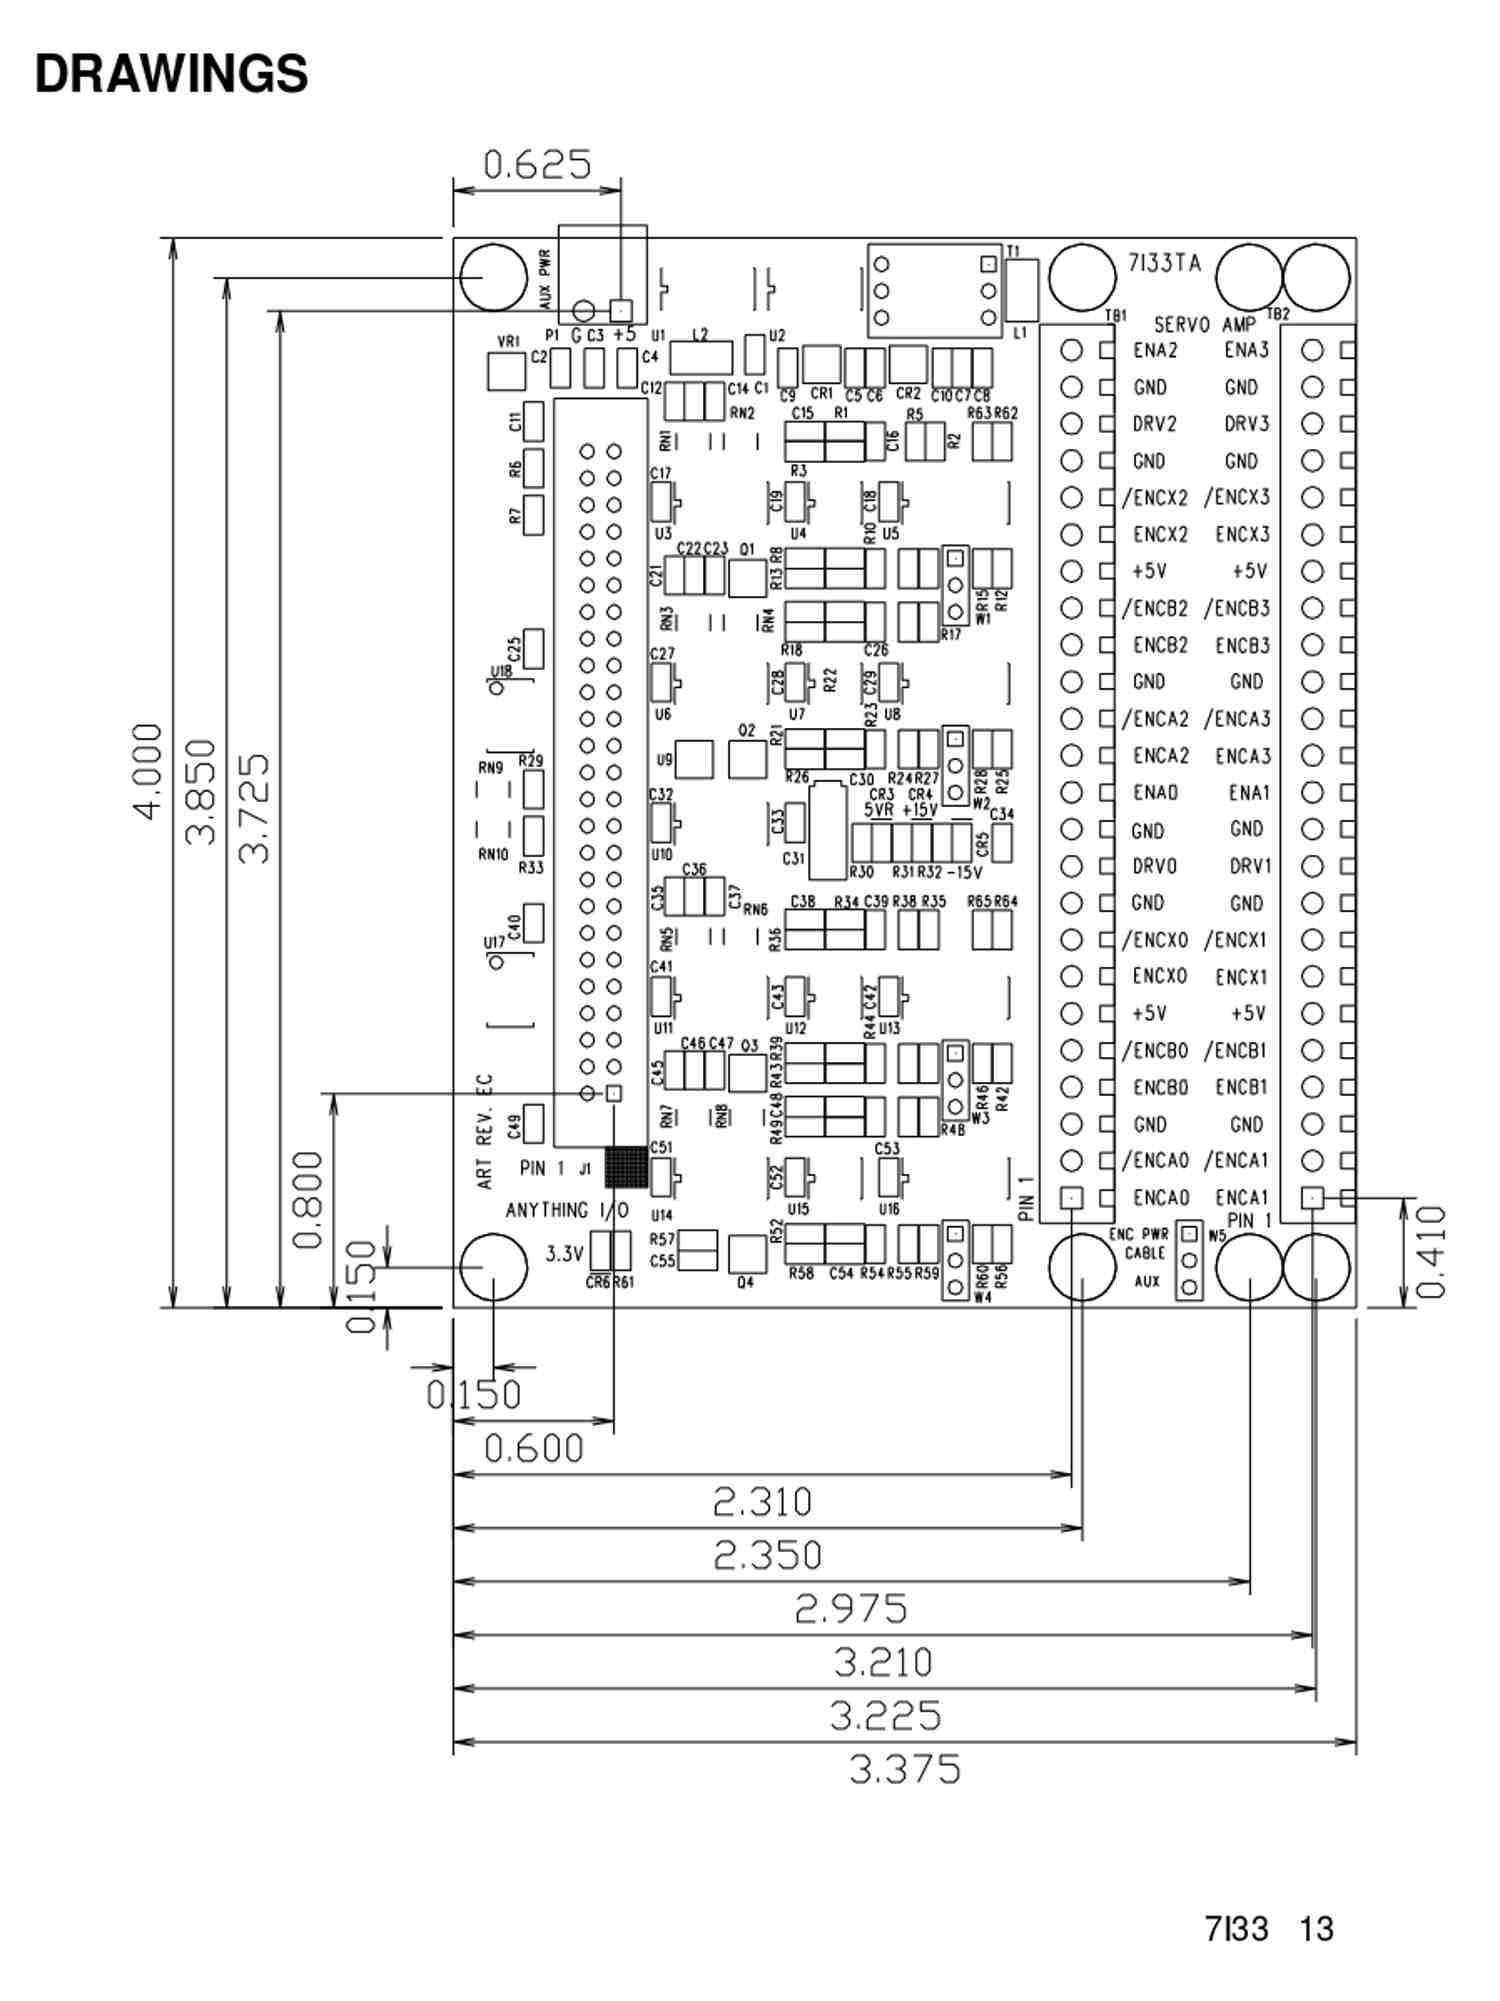
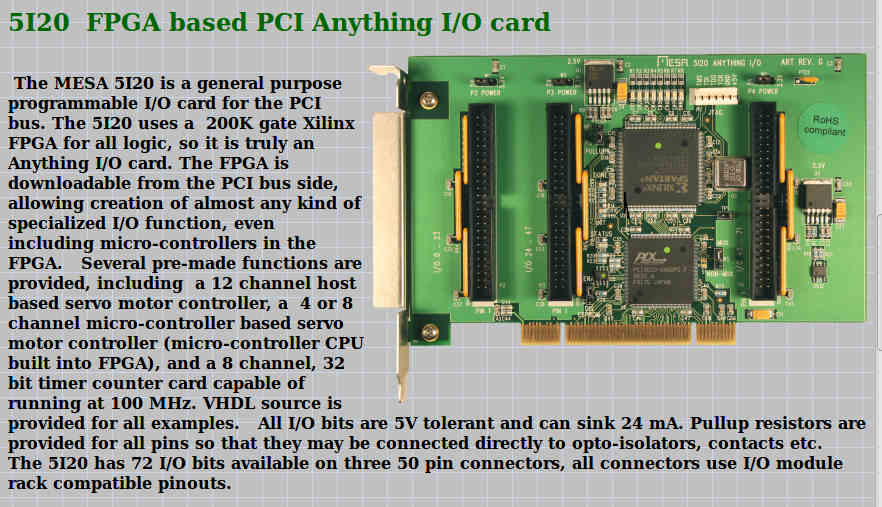
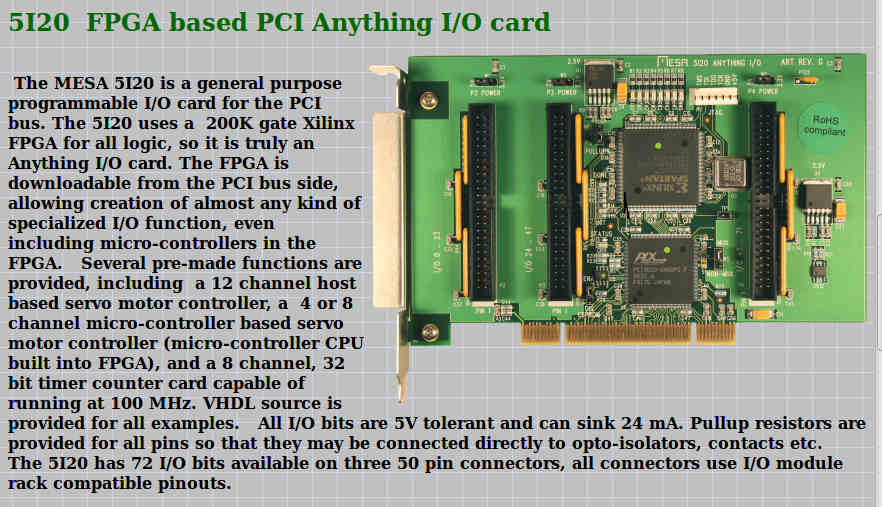
Mesa Electronics has a 72 bit, $260, par port I/O card
called anything I/O.
http://www.mesanet.com/
There is a whole list of other brands of par port cards that work.
Linux is open source. The university of New Mexico wrote
a real time version of Linux and put it in the public domain.
Been around for at least ten years. LinuxCNC is based on that.
I will have less than $600 invested in my NC Mill upgrade
including the PC. The real heavy duty 7,000 pound Kasuga
NC mill cost me $7,000 originally with its Bandit 6502 controller
about 6 years ago. The bandit failed soon after. It has
a relatively rare (for the time) auto tool changer.
http://www.rotaryeng.net/Nc-Mill-How-To.html
The cheapest comparable NC mill now is a about $30,000.
That is why NC shops charge so much. They are making
payments :-)
Paul Lamar
The Rotary Engine News Letter. Powered by Linux. If you want off the
list PLEASE let me know and I will remove you. ACRE NL web site.
http://www.rotaryeng.net You Tube
http://tinyurl.com/beqqxas
Copyright 1998-2015 All world wide rights reserved.